
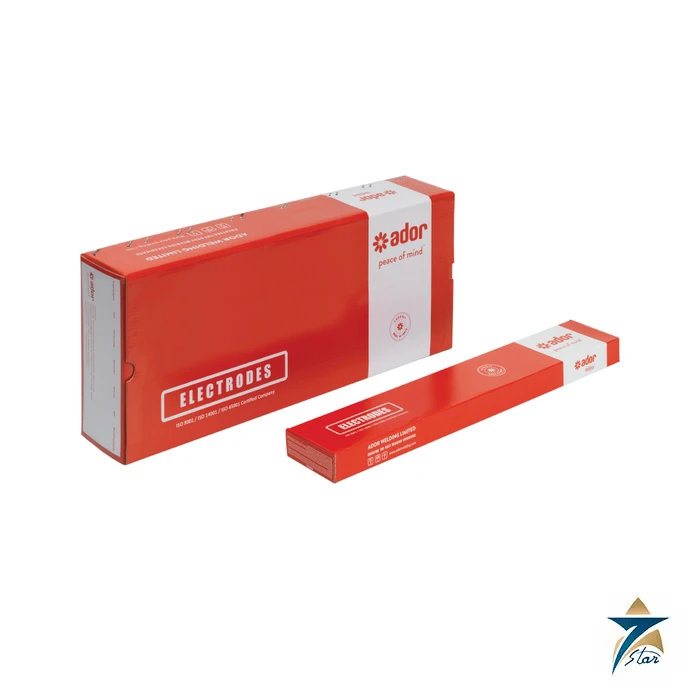
Ador Tenalloy Z Plus is a low hydrogen stick electrode for carbon-manganese steel where impact toughness at sub-zero temperature is part of the specification. Ador Welding classifies it AWS A/SFA 5.1 E7018-1 H4R, EN ISO 2560-A E 42 4 B 32 H5 and IS 814 EB5629H3JX. Compared with a standard E7018, the -1 designation means the weld metal is tested for Charpy toughness at -46°C, and Ador reports excellent toughness down to -50°C. The Ador Tenalloy Z Plus is also designed for the most demanding pipe qualification positions, 5G, 6G and 6GR.
Seven Star LLC supplies Ador Tenalloy Z Plus to piping contractors, tank builders and pressure equipment fabricators in the Sultanate of Oman and the GCC. Gas plants, LNG and petrochemical facilities, refinery tie-ins and power station piping in Sohar, Sur, Duqm and Muscat frequently specify E7018-1 for its toughness margin, and our team in Muscat provides datasheets, selection support and lead time coordination.
Explained in general terms, toughness is the ability of a weld to absorb energy without fracturing in a brittle way. Steels and their welds become less tough as temperature falls, so codes for pressure equipment, tanks and pipelines often require a Charpy V-notch test at a defined temperature. Even in a warm country, equipment can see low metal temperatures through gas expansion, depressurisation, refrigerated storage or simply cold desert nights, which is why designers in the Gulf still call for impact-tested consumables.
An E7018-1 electrode such as the Ador Tenalloy Z Plus meets that need through a clean, fine-grained basic weld deposit with a higher manganese level. Ador gives typical manganese of 1.5 percent, compared with 1.1 percent on its standard E7018 product, and that composition, together with the basic slag and very low hydrogen, supports the 60 J typical impact at -46°C reported on the datasheet. As with all basic electrodes, keeping the coating dry is what preserves the low hydrogen level in practice.
Typical undiluted weld metal for Ador Tenalloy Z Plus contains 0.06 percent carbon, 1.5 percent manganese and 0.3 percent silicon. As welded, the datasheet shows tensile strength typically 560 MPa, yield 480 MPa and elongation 27 percent, with specification minimums of 490 MPa, 400 MPa and 22 percent. Impact energy at -46°C is typically 60 J against a 50 J minimum. Hardness over three layers is 200 BHN maximum, diffusible hydrogen is below 5 ml per 100 g and HIC and SSCC testing to NACE is listed as a special test.
The electrode runs on AC with 70 V open-circuit voltage or on DCEP, in 2.5 × 350, 3.15 × 350, 3.15 × 450, 4.0 × 450 and 5.0 × 450 mm sizes. A 20 kg box holds four 5 kg cartons, and vacuum packing is also offered. Ador lists related consumables for other processes: Tigfil 70S-2 SPL, 70S-3 and 70S-6 for GTAW, Automig FC 71T-5 for FCAW, and for SAW the flux and wire pairs Automelt B20 Plus with EH12K, B41 with EH10K and B41 with EH14.
These are the main points that Ador gives for the Ador Tenalloy Z Plus, with short explanations:
Ador lists storage tanks, pipes and boilers, bridges and heavy structures subject to dynamic loading, and the joining of ASTM SA 414/414M Gr. C and D, SA 516/516M Gr. 55 and 60, IS 2002 and IS 2062 steels. SA 516 plate is the standard material for pressure vessels in refineries and gas plants across Oman, and the Ador Tenalloy Z Plus is a common choice where the vessel or piping specification calls for impact testing at -46°C. Pipe fabrication shops also use it for 6G welder qualification and for fill and cap passes over a TIG root on process piping.
Seven Star LLC supplies the Ador Tenalloy Z Plus together with complementary consumables and machines. For fabricators running stick and MIG from one unit, the ESAB Rebel EMP 285ic is a compact option; for automatic seams on vessels and tanks, wire such as the LongTeng EL8 SAW wire is used; and solid wire like the Lincoln Electric SuperArc L-59 covers GMAW. Browse our welding electrodes category for other stick grades.
Ador recommends 60–90 A for 2.5 mm, 90–140 A for 3.15 mm in both lengths, 140–180 A for 4.0 mm and 180–240 A for 5.0 mm. For 6G pipe work, welders generally use the smaller diameters for root support and hot passes and a stringer or narrow weave technique to keep heat input and inter-pass temperature within the procedure limits, which also helps protect toughness.
Redrying, per the datasheet, is 250–300°C for a minimum of one hour. In Oman humidity along the coast can be high, so in general practice the electrodes are held in a heated oven after redrying and issued to welders in heated quivers, with exposure times controlled by the welding procedure.
The Ador Tenalloy Z Plus data below are taken from the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Tenalloy Z Plus |
| Type | Basic coated iron powder, low hydrogen C-Mn electrode |
| AWS classification | AWS A/SFA 5.1 E7018-1 H4R |
| EN ISO / IS classification | EN ISO 2560-A E 42 4 B 32 H5; IS 814 EB5629H3JX |
| Approvals listed | ABS / BV / DNV / IRS / LRA / NPCIL / BHEL / NTPC / BIS / CE |
| Typical weld metal chemistry | C 0.06, Mn 1.5, Si 0.3 (wt %) |
| Tensile strength | Typical 560 MPa; specification 490 MPa min |
| Yield strength | Typical 480 MPa; specification 400 MPa min |
| Elongation | Typical 27%; specification 22% min |
| CVN impact at -46°C | Typical 60 J; specification 50 J min |
| Hardness / hydrogen | 200 BHN max (3 layer); diffusible H2 below 5 ml/100 g |
| Special test | HIC and SSCC (NACE) |
| Current | AC (70 OCV) / DCEP |
| Sizes and amperage | 2.5 × 350 mm: 60–90 A; 3.15 × 350 and 450 mm: 90–140 A; 4.0 × 450 mm: 140–180 A; 5.0 × 450 mm: 180–240 A |
| Positions | All positions except vertical down; 5G, 6G, 6GR pipe |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg box of 4 cartons of 5 kg; vacuum packing available |
Request a quotation for Ador Tenalloy Z Plus from Seven Star LLC by sending the diameters, packing type and quantity needed for your project in Oman or the GCC. We will include the Ador Tenalloy Z Plus datasheet with our offer and can recommend matching TIG, flux-cored and submerged arc consumables, with engineering support and lead time coordination from Muscat.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.