
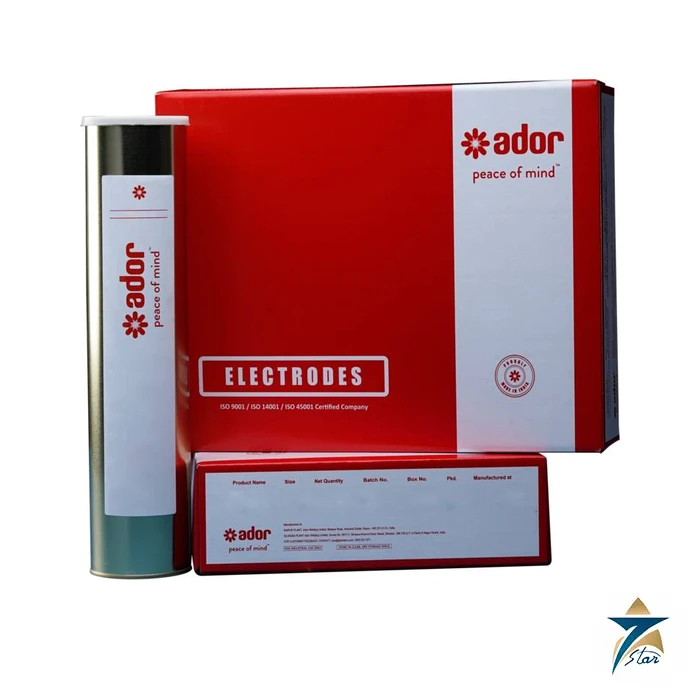
Ador Celwel 70P is a pipeline electrode from Ador Welding Limited with a cellulose type coating, classified to AWS A/SFA 5.5 E7010-P1 and EN ISO 2560-A E 42 2 C 21. It sits one strength level above a plain E6010 rod: the weld deposit carries a small molybdenum addition, so it can match line pipe up to API 5L X65 while keeping the forceful arc and quick-freezing behaviour that pipeliners expect from a cellulosic product. Ador describes the Ador Celwel 70P as ideal for root pass and capping runs and designed for the stove-pipe technique, the vertical-down method used on most onshore spreads.
Seven Star LLC supplies Ador Celwel 70P from Muscat to contractors building and repairing pipelines across the Sultanate of Oman and the GCC. Export gas lines, crude trunk lines, gathering systems in the interior fields and the new hydrogen and industrial gas corridors planned around Duqm and Sohar all involve higher-strength line pipe, and we help buyers pair the electrode with the right diameter range and the rest of the welding package.
Stove-pipe welding, explained here as general welding knowledge, means welding a fixed horizontal pipe joint from the top of the pipe downwards on each side, usually with several welders working at once. Because travel is downhill, the puddle must solidify fast enough to stay in place, and the arc must be strong enough to reach the root through a narrow gap. A cellulosic coating gives both: the burning cellulose forms a gas cloud that drives a deep, stiff arc, and the light slag lets the welder see and control the keyhole.
The molybdenum in the Ador Celwel 70P deposit is what separates it from an E6010. Molybdenum raises tensile and yield strength without needing much more carbon, so the weld metal can overmatch X52 to X65 pipe. As with any cellulosic electrode, the hydrogen-rich shielding means the welding procedure must manage preheat, the delay before the hot pass and the inter-pass temperature, and these limits come from the qualified procedure for the project rather than from the electrode alone.
Ador gives the typical undiluted chemistry of the Ador Celwel 70P as 0.1 percent carbon, 0.8 percent manganese, 0.3 percent silicon and 0.4 percent molybdenum. As welded, the all-weld-metal results are typically 560 MPa ultimate tensile strength, 450 MPa yield strength at 0.2 percent offset and 24 percent elongation, with 40 J Charpy V-notch impact at -30°C. The datasheet shows specification minimums of 490 MPa, 415 MPa, 22 percent and 27 J for the same tests.
Each diameter is supplied 350 mm long and welded on DC electrode positive. The standard pack is an 18 kg box or tin containing three cartons of 6 kg. In general field practice, cellulosic rods are used straight from their sealed packing because their coating is designed to hold a controlled amount of moisture; they are not re-baked at low-hydrogen temperatures, and opened stock should be kept dry and shaded on site.
The main characteristics of Ador Celwel 70P listed by Ador are summarised below:
The datasheet names cross-country pipelines subject to dynamic loading and mechanical restraint, and lists base materials ASTM SA-283 Gr. A, B, C and D and API 5L X42, X46, X52, X56, X60 and X65. In the Omani market this covers most of the line pipe used by upstream operators for flowlines and trunk lines, by gas transmission projects feeding power stations and industrial estates, and by water utilities using steel mains. The Ador Celwel 70P is commonly chosen where the specification requires the root and cap to overmatch an X52 to X65 pipe that a plain E6010 would not cover.
Seven Star LLC supplies Ador Celwel 70P alongside the equipment and consumables that pipeline and fabrication contractors use for the remaining passes. Workshops prefabricating spools often switch to wire processes using power sources such as the Lincoln Electric Power Wave S500 with a solid wire like the Lincoln Electric SuperArc L-59 ER70S-6, and double-jointing yards use submerged arc with wires such as the LongTeng EL8. More root and hot pass rods are collected in our cellulosic pipeline electrodes range.
For Ador Celwel 70P the manufacturer specifies DCEP and amperage windows of 50–70 A for 2.5 mm, 80–120 A for 3.15 mm, 110–160 A for 4.0 mm and 160–210 A for 5.0 mm. Narrower settings on the small sizes reflect the fine control needed on thin root lands. As a general observation, welders on large-diameter pipe often root with the 4.0 mm size and fill with 4.0 or 5.0 mm, while smaller pipe and tighter bevels use 3.15 mm for the root.
Project procedures for higher-strength line pipe usually specify preheat, a maximum time between root and hot pass and minimum inter-pass temperature, all qualified through procedure testing to the applicable pipeline code. Electrodes should be issued in quantities that will be used during the shift and protected from rain, dust and direct sun.
The values below are taken from the Ador Celwel 70P manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Celwel 70P |
| Coating type | Cellulose type, cellulosic pipeline electrode |
| AWS classification | AWS A/SFA 5.5 E7010-P1 |
| EN ISO classification | EN ISO 2560-A E 42 2 C 21 |
| Approvals listed | CE |
| Typical weld metal chemistry | C 0.1, Mn 0.8, Si 0.3, Mo 0.4 (wt %) |
| Tensile strength | Typical 560 MPa; specification 490 MPa min |
| Yield strength | Typical 450 MPa; specification 415 MPa min |
| Elongation | Typical 24%; specification 22% min |
| CVN impact at -30°C | Typical 40 J; specification 27 J min |
| Base materials listed | ASTM SA-283 Gr. A/B/C/D; API 5L X42, X46, X52, X56, X60, X65 |
| Current | DCEP |
| Sizes and amperage | 2.5 × 350 mm: 50–70 A; 3.15 × 350 mm: 80–120 A; 4.0 × 350 mm: 110–160 A; 5.0 × 350 mm: 160–210 A |
| Positions | All positions, specifically vertical down |
| Packing | 18 kg box / tin containing 3 cartons of 6 kg |
Seven Star LLC can quote Ador Celwel 70P for pipeline projects anywhere in Oman and the GCC. Share the pipe grade, diameters and quantity, and we will return a formal quotation with the Ador Celwel 70P datasheet, suggest matching consumables for the remaining passes, and coordinate lead time and engineering support from Muscat.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.