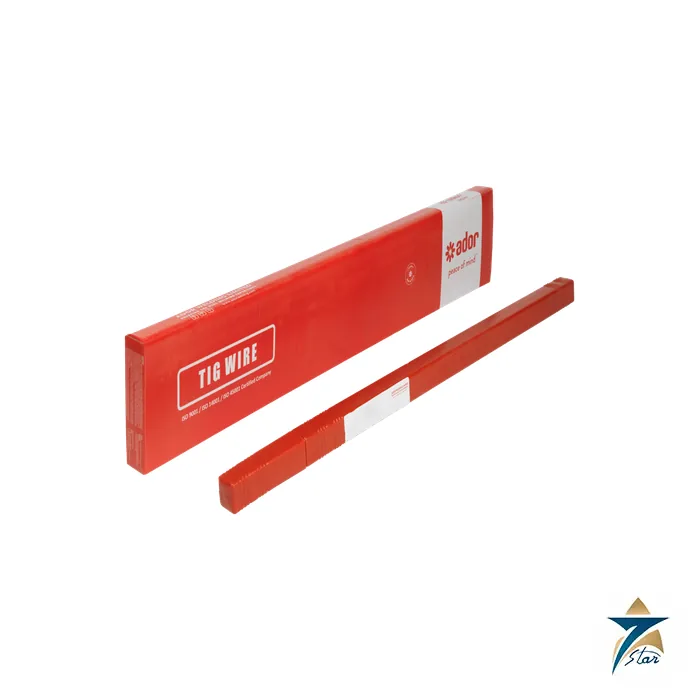
Ador Tigfil 90S-B3 ER90S-B3 Chrome-Moly TIG Welding Rod Supplied by Seven Star LLC

TIG Welding Wire

TIG welding wire, supplied as straight cut-length rods for the GTAW process, is used where root quality and corrosion resistance matter more than deposition rate. Seven Star LLC in Muscat, Oman currently lists three TIG filler rods from Ador Welding: ER2209 for 22Cr duplex stainless steel, ER2594 for super duplex, and ER90S-B3 for 2.25Cr-1Mo chrome-moly steel. The range is small and growing. Carbon steel, austenitic stainless and nickel alloy TIG rods can be sourced on request.
Read more about TIG Welding Wire

Category guide

About TIG Welding Wire

3 products 1 brand

TIG welding wire, supplied as straight cut-length rods for the GTAW process, is used where root quality and corrosion resistance matter more than deposition rate. Seven Star LLC in Muscat, Oman currently lists three TIG filler rods from Ador Welding: ER2209 for 22Cr duplex stainless steel, ER2594 for super duplex, and ER90S-B3 for 2.25Cr-1Mo chrome-moly steel. The range is small and growing. Carbon steel, austenitic stainless and nickel alloy TIG rods can be sourced on request.

Duplex, super duplex and chrome-moly TIG rods

Duplex fillers contain more nickel than the base metal, so the weld keeps a balanced ferrite and austenite structure after cooling. Root passes need an inert back purge, and heat input and interpass temperature are held within the limits of the procedure, because both too little and too much heat upset the phase balance. These rods are typical for seawater, produced water and desalination piping across the GCC. ER90S-B3, classified under AWS A5.28, is used for roots and small-bore joints in boiler and refinery piping, followed by post-weld heat treatment where the code requires it.

Information to include with a TIG rod inquiry

Give the AWS classification, rod diameter, quantity in kilograms and the certificate type. Mention any project requirement on the weld metal, such as a ferrite range or pitting corrosion testing, and the base metal grade, so we can check the match against the manufacturer datasheet.

What to include in your inquiry

These details let us quote the right item the first time.

  • AWS or EN classification
  • Diameter
  • Base material to be welded
  • Packaging (spool, drum, kg) and quantity
  • Approvals or certificates required

Missing some of them? Send what you have. A nameplate photo or an old part number is enough to start.
Brands in TIG Welding Wire

All brands →

Request a Quote for TIG Welding Wire

Looking for a specific model, part number or brand in TIG Welding Wire? Send us your requirements and quantities. Seven Star LLC sources genuine industrial equipment for customers across Oman and the GCC and replies with a formal quotation.

Free, no-obligation quotation · takes about 1 minute

Other enquiries: [email protected] · WhatsApp

Frequently Asked Questions

When is ER2209 used and when is ER2594 required?
ER2209 is the matching filler for 22Cr duplex grades such as UNS S31803 and S32205. ER2594 is a 25Cr super duplex filler for grades such as S32750 and S32760, where higher pitting resistance is needed. Using the lower-alloyed 2209 on super duplex gives a weld that is less corrosion resistant than the pipe, so procedures normally do not allow it.
Can ER2209 be used for joints between duplex and carbon steel or austenitic stainless?
It is a common choice for those dissimilar joints, and 309L-type fillers are another option. Which one applies depends on the design temperature, the corrosion requirement on the weld and what the client specification allows. The decision belongs to the qualified procedure. Send both base metal grades and we will check which fillers the manufacturer documentation recommends.
Which shielding and purge gas do duplex TIG welds need?
Argon is the standard shielding gas, and the root side must be purged until oxygen is low enough to avoid heavy heat tint. Some procedures add a small percentage of nitrogen to the shielding or purge gas to limit nitrogen loss from the root, which helps the austenite content. Use exactly the gases written in the qualified procedure.
How are TIG rods identified and kept from being mixed up?
Rods are normally stamped or flag-tagged with the classification, and packed in tubes labeled with the batch number. Keep them in the original tube, issue one grade per welder at a time, and never return loose unmarked rods to the store. On alloy piping, a mixed-up rod is usually found only at positive material identification, after the weld is finished.
Can you supply other TIG filler grades, and what data do you need?
Yes. Carbon steel, 308L, 316L, 309L, other chrome-moly grades and nickel alloy rods can be sourced on request. Send the AWS classification, diameter, quantity in kilograms, base metal grade and the certificate type required. If your procedure names a particular brand or trade designation, include it so the offer matches what was qualified.