
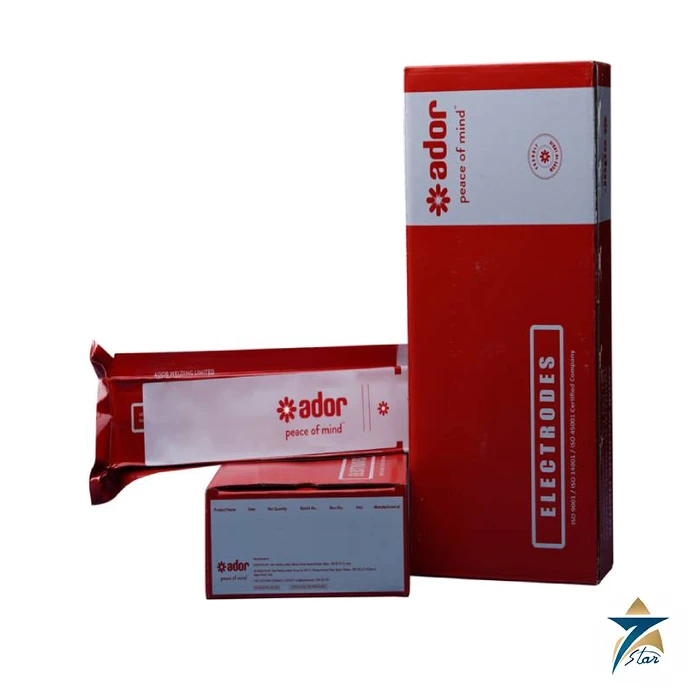
Ador Cromoten C is the 2.25Cr-1Mo grade in the Ador Welding range of high temperature low alloy electrodes. Classified AWS A/SFA 5.5 E9018-B3 and EN ISO 3580-A E CrMo2 B 32 H5, it is used where piping and vessels must hold their strength for decades at temperatures above the limit of P11 material. Ador states that the Ador Cromoten C deposit is resistant to creep and heat up to 600°C, is ductile, crack resistant and heat treatable, and gives radiography quality weld metal from a basic coated electrode.
Seven Star LLC supplies Ador Cromoten C to boiler makers, power station maintenance teams and refinery contractors in the Sultanate of Oman and the GCC. Main steam and hot reheat lines in combined cycle plants, superheater headers and hydroprocessing reactors and piping are typical P22 applications in the region, and our Muscat team supports buyers with the datasheet, procedure context and lead time coordination.
As general background, creep resistant steels are graded by their chromium and molybdenum content, and each step up allows higher design temperature or pressure. The 2.25Cr-1Mo composition, known as P22 for pipe and Grade 22 for plate, is one of the most widely used of these alloys. It has long served for main steam pipes, boiler superheaters and reheaters and for hydrogen-service reactors, because its higher chromium and molybdenum give better long-term creep strength and resistance to hydrogen attack than 1.25Cr-0.5Mo steel.
A matching weld must reproduce that chemistry so the joint does not become the weak link at temperature. The Ador Cromoten C deposits about 2.3 percent chromium and 0.95 percent molybdenum to do this. The alloy is air-hardening, so general practice for P22 includes elevated preheat and interpass temperature and mandatory post-weld heat treatment to temper the weld; the exact values are set by the governing code and the qualified procedure for each job, and Ador reports its test values after PWHT.
Ador gives typical undiluted weld chemistry of 0.08 percent carbon, 0.6 percent manganese, 0.4 percent silicon, 2.3 percent chromium and 0.95 percent molybdenum. After post-weld heat treatment at 690°C for one hour, the all-weld-metal results are typically 660 MPa tensile strength, 580 MPa yield and 22 percent elongation. The specification values required are 620 MPa, 530 MPa and 17 percent minimum. Three-layer hardness is limited to 220 BHN maximum and diffusible hydrogen is below 5 ml per 100 g.
The product runs on AC with 70 V open-circuit voltage or on DCEP. Sizes are 2.5 × 350, 3.15 × 450, 4.0 × 450 and 5.0 × 450 mm, packed in a 20 kg standard carton, with vacuum packing also available. Ador lists equivalent consumables for other processes: Automig 90S-B3 solid wire for GMAW, Tigfil 90S-B3 for GTAW, Automig FC 91T1-B3 for FCAW and the Automelt B20 Plus flux with Automelt EB3 wire for SAW.
Ador lists the following properties for Ador Cromoten C; brief explanations are added:
The datasheet names welding of 2.25Cr-0.5Mo and 2.25Cr-1Mo creep resistant steels; Cr-Mo and Cr-Mo-V bearing steels for high temperature applications; main steam pipes of boilers in electric power plants and boiler superheaters; joining of P5A materials; German steels 12CrMo9-10 and 10CrSiMoV7; ASTM A 335 Gr. P22 and A 387 Gr. 22; and use in refineries, power plants, pressure vessels and boilers. In Oman the Ador Cromoten C is relevant to steam turbine piping at independent power and water projects, waste heat boilers, and hydrocracker and hydrotreater circuits at refineries in Sohar and Duqm.
Seven Star LLC supplies Ador Cromoten C along with the equipment needed for alloy piping work. Contractors frequently use a portable multi-process unit such as the ESAB Rebel EMP 285ic for stick and TIG on site, while workshops may run the Lincoln Electric Power Wave S500. For associated carbon steel structures, submerged arc wire like the LongTeng EL8 is available. Further electrode grades are listed in our welding electrodes category.
Recommended amperage for Ador Cromoten C is 60–90 A for 2.5 mm, 100–140 A for 3.15 mm, 140–180 A for 4.0 mm and 190–250 A for 5.0 mm, in all positions except vertical down. For P22 pipe, a common general approach is a TIG root with matching B3 filler, then stick fill and cap with temperature monitored throughout, followed by local or furnace PWHT according to the procedure.
Redry the electrodes at 250–300°C for a minimum of one hour, keep them in a holding oven and issue them in heated quivers. Use only the quantity needed for the shift, especially on humid coastal sites.
All Ador Cromoten C values below come from the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Cromoten C |
| Type | Basic coated, Cr-Mo low alloy high temperature electrode |
| AWS classification | AWS A/SFA 5.5 E9018-B3 |
| EN ISO classification | EN ISO 3580-A E CrMo2 B 32 H5 |
| Approvals listed | ABS / IBR / NPCIL / NTPC / CE |
| Typical weld metal chemistry | C 0.08, Mn 0.6, Si 0.4, Cr 2.3, Mo 0.95 (wt %) |
| Condition tested | PWHT 690°C for 1 hour |
| Tensile strength | Typical 660 MPa; specification 620 MPa min |
| Yield strength | Typical 580 MPa; specification 530 MPa min |
| Elongation | Typical 22%; specification 17% min |
| Hardness / hydrogen | 220 BHN max (3 layer); diffusible H2 below 5 ml/100 g |
| Service temperature | Creep and heat resistant up to 600°C |
| Current | AC (70 OCV) / DCEP |
| Sizes and amperage | 2.5 × 350 mm: 60–90 A; 3.15 × 450 mm: 100–140 A; 4.0 × 450 mm: 140–180 A; 5.0 × 450 mm: 190–250 A |
| Positions | All positions except vertical down |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg standard carton; vacuum packing available |
To source Ador Cromoten C for boiler, steam piping or refinery work in Oman or the GCC, send Seven Star LLC the sizes and quantity required. We will provide a formal quotation and the Ador Cromoten C datasheet, and our Muscat engineers can suggest matching B3 TIG and MIG wires and confirm availability.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.