
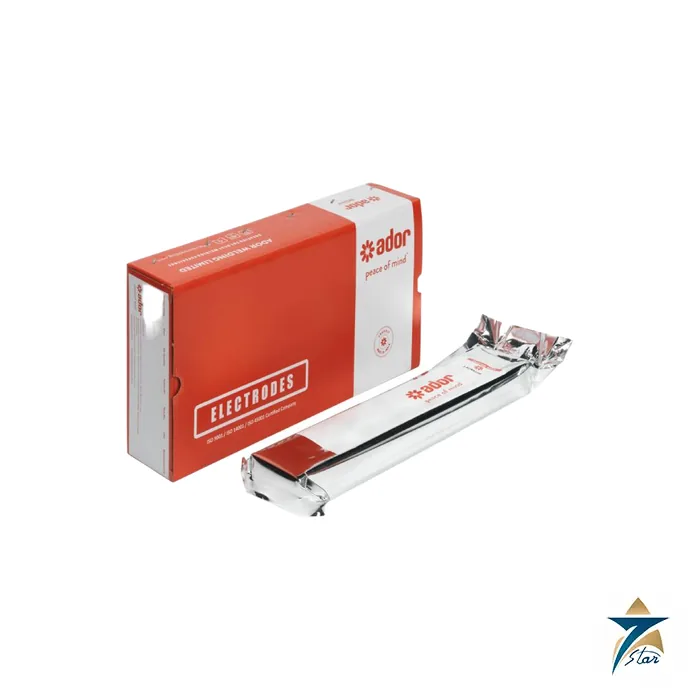
Ador Betanox 2594 is a rutile coated manual metal arc electrode for super duplex stainless steel, classified to AWS A/SFA 5.4 E2594-16 and ISO 3581-A E 25 9 4 N L R 12. It deposits a nitrogen-alloyed 25Cr-10Ni-4Mo weld with an austenitic-ferritic microstructure, and Ador states a minimum pitting resistance equivalent number (PREN) of 40. The manufacturer describes weld metal characteristics similar to super duplex wrought and cast alloys, combining high strength with improved resistance to pitting and sulphide stress cracking in chloride environments. CE approval is printed on the datasheet.
Seven Star LLC supplies the Ador Betanox 2594 to offshore, desalination and process piping contractors in Oman and the GCC. Because super duplex welding is usually tightly controlled by client specifications, we attach the official Ador datasheet so that engineers can review weld metal analysis, impact values and current ranges before ordering.
As general background, super duplex stainless steels such as UNS S32750 and S32760 are about half ferrite and half austenite. That balance gives roughly twice the yield strength of standard austenitic grades and strong resistance to chloride pitting and stress corrosion cracking. Welding can upset the phase balance and can lose nitrogen, so fillers are normally over-alloyed in nickel to restore austenite on cooling. The Ador Betanox 2594 has a typical undiluted analysis of 0.9 Mn, 0.7 Si, 25.9 Cr, 10 Ni, 3.9 Mo and 0.23 N, reflecting that approach.
Heat input and interpass temperature are critical with these alloys. Industry practice is to keep heat input within a qualified window and to limit interpass temperature, because too little heat produces excess ferrite while too much can form intermetallic phases that reduce toughness and corrosion resistance. Exact limits must come from the WPS and the client specification.
The covering is a rutile, non-synthetic type that Ador says gives easy slag removal and uniform, fine ripples, with radiographic quality welds. Electrodes are 350 mm long in three diameters: 2.5 mm at 50 to 80 A, 3.15 mm at 70 to 110 A and 4.0 mm at 90 to 140 A. They run on AC with 70 V open circuit voltage or on DCEP, in all positions except vertical down. Redrying is specified at 250 to 300°C for a minimum of one hour.
Typical as-welded all weld metal results are 880 MPa ultimate tensile strength, 27 percent elongation and 48 J Charpy V-notch impact at minus 20°C, against specification minimums of 760 MPa, 15 percent and 47 J. Packing is a 10 kg carton containing five 2 kg cartons, which helps keep opened stock small and limits moisture exposure on site.
Moisture control is a general concern with any coated electrode, and it is especially relevant in the humid coastal climate of Oman. Ador specifies redrying of the Ador Betanox 2594 at 250 to 300°C for at least one hour, and many contractors keep redried electrodes in heated holding ovens or quivers at the workstation. Damp coatings can cause porosity and unstable arc behaviour, so following the redrying instruction protects both weld quality and inspection pass rates. Welders should also clean joint faces thoroughly and remove all slag between passes, as trapped slag in a multi-pass Ador Betanox 2594 joint will show up on radiographs.
The Ador Betanox 2594 data sheet highlights these characteristics.
Ador lists welding of super duplex grades UNS S32750, S32760, SAF 2507, Zeron 100 and casting alloys such as ASTM A890 Grade 5A, plus materials 1.4410, 1.4460, 1.4462 and 1.4463. Named applications include pipe work systems, flow lines, risers, manifolds and process equipment in the offshore oil and gas industry, and chemical and petrochemical plant; the electrode may also be used on duplex 2205. In Oman, super duplex is widely used for seawater lift and firewater systems, produced water lines on oil fields, and high-chloride brine service in reverse osmosis desalination plants along the coast from Barka to Sur. Fabrication yards serving these sectors often keep a small qualified stock of super duplex electrodes on hand for repairs and late design changes that cannot wait for mechanised welding set-ups.
Manual metal arc welding is often the practical choice for tie-ins, repairs and field joints where TIG or MIG equipment is hard to deploy. Seven Star LLC supplies the Ador Betanox 2594 for those jobs, and the manufacturer lists equivalents in other processes, including Tiginox 2594 for GTAW, Miginox 2594 for GMAW, Miginox FC 2594 for FCAW and Subinox 2594 wire with Automelt S33 flux for submerged arc welding.
The specification table for the Ador Betanox 2594 below uses values from the official data sheet.
| Parameter | Specification |
|---|---|
| Model | Ador Betanox 2594 |
| Process | SMAW (MMA), super duplex stainless steel |
| AWS classification | A/SFA 5.4 E2594-16 |
| ISO classification | ISO 3581-A E 25 9 4 N L R 12 |
| Approvals | CE |
| Typical weld metal, wt % | Mn 0.9, Si 0.7, Cr 25.9, Ni 10, Mo 3.9, N 0.23 |
| PREN | 40 min |
| UTS, as welded | 880 MPa typical (760 min) |
| Elongation | 27 % typical (15 min) |
| CVN impact at -20°C | 48 J typical (47 min) |
| Sizes and current | 2.5 x 350 mm 50-80 A; 3.15 x 350 mm 70-110 A; 4.0 x 350 mm 90-140 A |
| Current type | AC (70 OCV) or DCEP |
| Positions | All positions except vertical down |
| Redrying | 250-300°C for minimum 1 hour |
| Packing | 10 kg carton with 5 cartons of 2 kg |
For stick and TIG welding on site, the ESAB Rebel EMP 285ic covers MMA as well as MIG. For carbon steel structural attachments, consider the Lincoln SuperArc L-59 wire, and for heavy shop seams the LongTeng EL8 SAW wire. Browse all welding electrodes we carry.
To receive a quotation for the Ador Betanox 2594, tell us the electrode diameters, number of 10 kg cartons and delivery site in Oman or the GCC. The Ador Betanox 2594 datasheet is available for download on this page, and our Muscat consumables team can support you with procedure questions and matching super duplex fillers for other processes.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.