
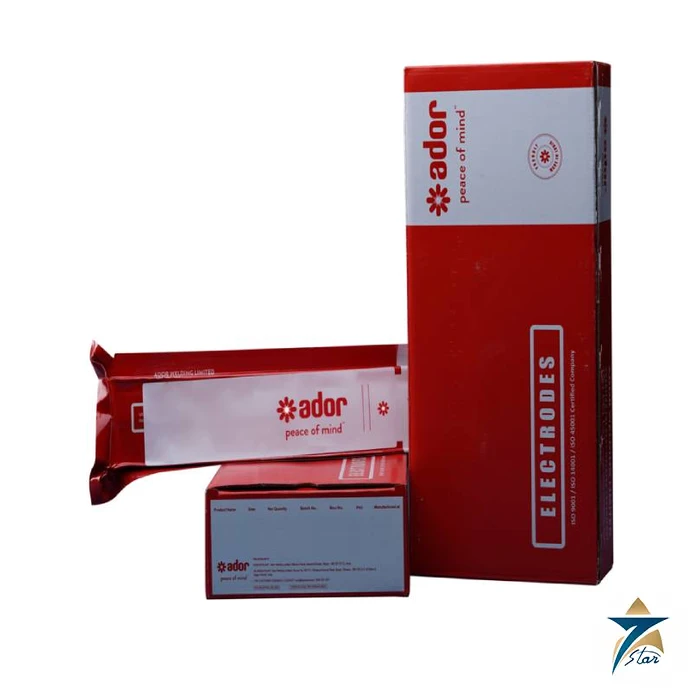
Ador Cromoten 9M-15 is a basic coated, low hydrogen electrode for the modified 9 percent chromium steels that dominate modern high temperature power and process piping. Ador Welding classifies it AWS A/SFA 5.5 E9015-B91 and EN ISO 3580-A E CrMo91 B 42 H5. Its weld deposit is a 9Cr-1Mo alloy modified with niobium and vanadium, matching grade 91 steels such as P91 pipe, T91 tube and F91 forgings. Ador highlights excellent strength and creep resistance at high temperature under prolonged holding, good impact toughness at subzero temperatures, all-positional capability and radiographic quality for the Ador Cromoten 9M-15.
Seven Star LLC supplies Ador Cromoten 9M-15 to power generation, boiler and petrochemical contractors throughout the Sultanate of Oman and the GCC. Grade 91 is common in heat recovery steam generators, main steam and hot reheat piping at combined cycle plants and in high temperature refinery service, and our Muscat team provides the datasheet, background on the welding requirements and lead time coordination.
As general metallurgical background, grade 91 is a creep strength enhanced ferritic steel. Its strength at high temperature does not come only from chromium and molybdenum but from a carefully controlled tempered martensite structure stabilised by fine vanadium and niobium carbonitrides. That structure lets thinner walls carry the same steam pressure and temperature as much heavier 2.25Cr-1Mo components, which is why grade 91 replaced older alloys in many modern boilers.
The same structure makes grade 91 demanding to weld. Weld metal must contain the right amounts of vanadium, niobium and nitrogen, and the joint must be preheated, cooled through the martensite transformation in a controlled way and then tempered by post-weld heat treatment at a high temperature. Errors in chemistry or heat treatment can leave a hard, brittle or creep-weak joint. The Ador Cromoten 9M-15 supplies the alloy side of that equation, and Ador reports its properties after PWHT at 740°C for two hours; preheat, interpass and PWHT details for any job must come from the qualified procedure and code.
The typical undiluted weld chemistry printed by Ador is 0.1 percent carbon, 0.6 percent manganese, 0.15 percent silicon, 8.7 percent chromium, 1.0 percent molybdenum, 0.2 percent vanadium, 0.06 percent niobium and 0.03 percent nitrogen, with copper at 0.01 percent and aluminium at 0.001 percent. After PWHT at 740°C for two hours, the all-weld-metal tensile strength is typically 670 MPa, yield 580 MPa and elongation 22 percent, against specification minimums of 620 MPa, 530 MPa and 17 percent. Diffusible hydrogen is below 5 ml per 100 g.
As a special test, the datasheet lists a creep rupture test at 600°C with 100 MPa stress for a minimum of 1000 hours. The electrode runs on DCEP only and is made in 2.5 × 350, 3.15 × 350, 4.0 × 450 and 5.0 × 450 mm sizes, packed in a 20 kg box of four 5 kg cartons, with vacuum packing available. Ador lists Automig 90S-B9 for GMAW, Tigfil 90S-B9 for GTAW, Automig FC 91T-1 B91 for FCAW and Automelt B20 Plus flux with Automelt B91 wire for SAW as process equivalents.
The Ador Cromoten 9M-15 datasheet lists these key features:
Ador lists welding of similar composition creep resistant steels such as P91, T91 and F91, material 1.4903 and similar grades, and applications in petrochemical plants, power plants, boilers and oil refineries. In Oman the Ador Cromoten 9M-15 is relevant to HRSG harps and headers, main steam and hot reheat lines in gas-fired combined cycle plants, steam turbine bypass piping and high temperature refinery furnace and transfer lines, both for new construction and for repair during outages.
Seven Star LLC supplies the Ador Cromoten 9M-15 together with welding machines and wires used around such projects. A portable inverter like the ESAB Rebel EMP 285ic covers site stick and TIG work, the Lincoln Electric Power Wave S500 suits workshop production, and the Lincoln Electric SuperArc L-59 handles associated carbon steel fabrication. Other stick grades are listed in our welding electrodes category.
Ador recommends DCEP at 50–80 A for 2.5 mm, 90–130 A for 3.15 mm, 130–170 A for 4.0 mm and 180–240 A for 5.0 mm, in all positions except vertical downwards. As general practice for grade 91, thin stringer beads are preferred over wide weaves, the root is commonly TIG welded with matching B9 filler under a back purge, and temperature is controlled continuously from preheat through PWHT.
Redry at 250–300°C for a minimum of one hour, then hold the electrodes in an oven and issue them in heated quivers. Procedure qualification, hardness checks after PWHT and documented heat treatment records are normally required by owners for grade 91 joints.
The table gives the Ador Cromoten 9M-15 data from the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Cromoten 9M-15 |
| Type | Basic coated low hydrogen, Nb-V modified 9Cr-1Mo electrode |
| AWS classification | AWS A/SFA 5.5 E9015-B91 |
| EN ISO classification | EN ISO 3580-A E CrMo91 B 42 H5 |
| Approvals listed | IBR / CE |
| Typical weld metal chemistry | C 0.1, Mn 0.6, Si 0.15, Cr 8.7, Mo 1.0, V 0.2, Nb 0.06, N 0.03, Cu 0.01, Al 0.001 (wt %) |
| Condition tested | PWHT 740°C for 2 hours |
| Tensile strength | Typical 670 MPa; specification 620 MPa min |
| Yield strength | Typical 580 MPa; specification 530 MPa min |
| Elongation | Typical 22%; specification 17% min |
| Diffusible hydrogen | Below 5 ml/100 g |
| Special test | Creep rupture at 600°C, 100 MPa, minimum 1000 hours |
| Base materials listed | P91, T91, F91; material 1.4903 and similar |
| Current | DCEP |
| Sizes and amperage | 2.5 × 350 mm: 50–80 A; 3.15 × 350 mm: 90–130 A; 4.0 × 450 mm: 130–170 A; 5.0 × 450 mm: 180–240 A |
| Positions | All positions except vertical downwards |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg box of 4 cartons of 5 kg; vacuum packing available |
Send Seven Star LLC your grade 91 project details, sizes and quantities to receive a formal quotation for Ador Cromoten 9M-15 in Oman or the GCC. We include the Ador Cromoten 9M-15 datasheet with every offer and can advise on matching B9 TIG and MIG wires, with engineering support and lead time coordination from Muscat.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.