
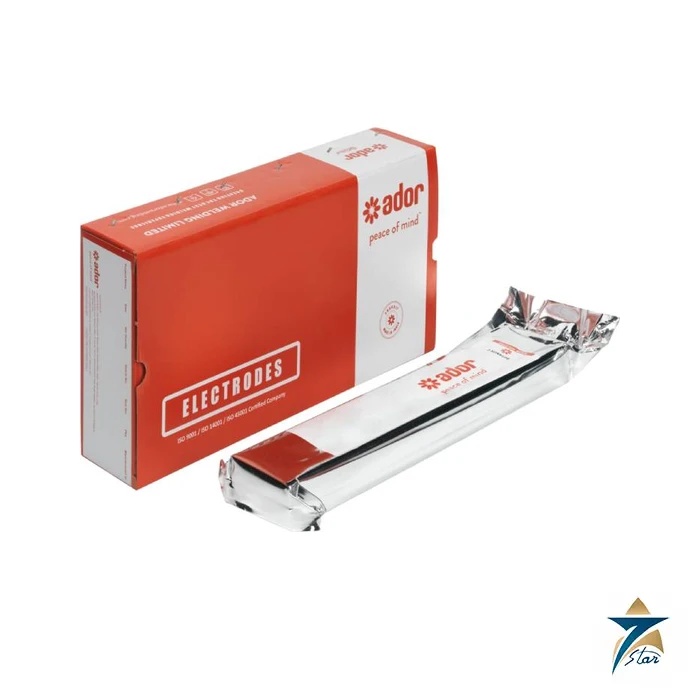
Ador Supabase X Plus is a general fabrication workhorse from Ador Welding: a basic coated, low hydrogen iron powder electrode for carbon-manganese steels, classified AWS A/SFA 5.1 E7018 H4R, ISO 2560-A E 42 3 B 32 H5 and IS 814 EB5426H3JX. The H4R suffix indicates very low diffusible hydrogen with moisture-resistant coating behaviour, and Ador reports diffusible hydrogen below 5 ml per 100 g. The Ador Supabase X Plus offers medium penetration, a high deposition rate thanks to iron powder in the flux, all-position capability apart from vertical down and radiographic weld quality.
Seven Star LLC supplies Ador Supabase X Plus to fabrication shops, shipyards, tank builders and plant maintenance departments across the Sultanate of Oman and the GCC. Pressure equipment in the Sohar and Duqm industrial zones, storage tanks at coastal terminals, structural steel for power and water plants and ship repair in Muscat and Duqm all depend on reliable E7018 electrodes, and our Muscat team supports buyers with datasheets and lead time coordination.
As general welding knowledge, a basic electrode coating is built mainly on calcium carbonate and calcium fluoride rather than cellulose or rutile. When the carbonate decomposes in the arc it releases carbon dioxide that shields the weld, while the fluoride helps form a fluid basic slag that refines the weld metal and lowers oxygen and sulphur. Because the coating contains almost no organic material or chemically bound water, the hydrogen absorbed by the weld is very low, which greatly reduces the risk of cold cracking in thick or restrained joints.
The practical consequence for the Ador Supabase X Plus is tough, crack-resistant weld metal suited to boilers, vessels and dynamically loaded structures. The trade-off is that the coating must stay dry: moisture picked up from humid air reintroduces hydrogen. That is why Ador prints a redrying condition of 250–300°C for at least one hour and offers vacuum packing, and why, in general practice, low hydrogen electrodes are kept in holding ovens or quivers once taken out of their packing on site.
Ador gives the typical undiluted weld chemistry as 0.05 percent carbon, 1.1 percent manganese and 0.5 percent silicon. As welded, the all-weld-metal properties are typically 555 MPa tensile strength, 480 MPa yield and 26 percent elongation, with Charpy V-notch impact energy of 60 J at -30°C. Specification values printed alongside are 490 MPa, 400 MPa, 22 percent and 47 J minimum. Three-layer hardness is limited to 200 BHN, and the datasheet lists a special test for HIC and SSCC to NACE, which is relevant for sour service equipment.
The Ador Supabase X Plus runs on AC with 70 V open-circuit voltage or on DC electrode positive. It is produced in 2.5 × 350, 3.15 × 350, 3.15 × 450, 4.0 × 450 and 5.0 × 450 mm sizes. Standard packing is a 20 kg box of four 5 kg cartons, with vacuum packing also available. For other processes Ador lists equivalents such as Automig I and Automig 70S-3 for GMAW, Tigfil 70S-2, 70S-3 and 70S-6 for GTAW, Automig FC 71T-5 for FCAW, and Automelt B71 with EM12K or B31 with EH14 for SAW.
The datasheet for Ador Supabase X Plus highlights these characteristics:
Ador lists boilers and pressure vessels, heavy structures subject to dynamic loading, ship building, storage tanks, bridges, pipelines and penstocks, and the joining of IS 2002 and IS 2062 steels. In Oman the Ador Supabase X Plus fits refinery and petrochemical maintenance, pressure vessel and heat exchanger shops, crude and product storage tanks at terminals, steel structures for power stations and desalination plants, and hull and deck repairs at shipyards. The marine society approvals printed on the datasheet are useful for yards and offshore fabrication where classification is required.
Seven Star LLC supplies the Ador Supabase X Plus along with the wire and equipment that fabricators use for the same steels. Shops that move fill passes to MIG can use the Lincoln Electric SuperArc L-59 ER70S-6 on a power source such as the Lincoln Electric Power Wave S500, and heavy seams on tanks and vessels are often submerged arc welded with wire like the LongTeng EL8. Further stick electrodes are listed in our welding electrodes category.
Recommended currents for Ador Supabase X Plus are 60–90 A for 2.5 mm, 100–130 A for both 3.15 mm lengths, 140–180 A for 4.0 mm and 180–240 A for 5.0 mm. As general practice with E7018 electrodes, a short arc and a slight drag angle give the best shielding, and restarting on a fresh bead is easier when the electrode tip is clean of slag. Weaving is kept moderate so that heat input stays within the procedure.
In the hot and humid coastal climate of Oman, keeping basic electrodes dry is critical. Unopened vacuum packs or cartons should be stored indoors; opened electrodes should be redried at 250–300°C for at least one hour when required and held in a heated oven or quiver until use, following the project welding procedure.
The table lists the Ador Supabase X Plus values given on the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Supabase X Plus |
| Type | Basic coated, low hydrogen iron powder electrode for C-Mn steel |
| AWS classification | AWS A/SFA 5.1 E7018 H4R |
| ISO / IS classification | ISO 2560-A E 42 3 B 32 H5; IS 814 EB5426H3JX |
| Approvals listed | ABS / BV / DNV / IRS / LRA / NPCIL / BIS / CE |
| Typical weld metal chemistry | C 0.05, Mn 1.1, Si 0.5 (wt %) |
| Tensile strength | Typical 555 MPa; specification 490 MPa min |
| Yield strength | Typical 480 MPa; specification 400 MPa min |
| Elongation | Typical 26%; specification 22% min |
| CVN impact at -30°C | Typical 60 J; specification 47 J min |
| Hardness / hydrogen | 200 BHN max (3 layer); diffusible H2 below 5 ml/100 g |
| Special test | HIC and SSCC (NACE) |
| Current | AC (70 OCV) / DCEP |
| Sizes and amperage | 2.5 × 350 mm: 60–90 A; 3.15 × 350 and 450 mm: 100–130 A; 4.0 × 450 mm: 140–180 A; 5.0 × 450 mm: 180–240 A |
| Positions | All positions except vertical down |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg box of 4 cartons of 5 kg; vacuum packing available |
Seven Star LLC can quote Ador Supabase X Plus in the sizes and packing your fabrication or maintenance job needs. Send us your quantities and delivery point in Oman or the GCC for a formal quotation, request the Ador Supabase X Plus datasheet, and ask our Muscat team about matching MIG, TIG, flux-cored or submerged arc consumables and current availability.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.