
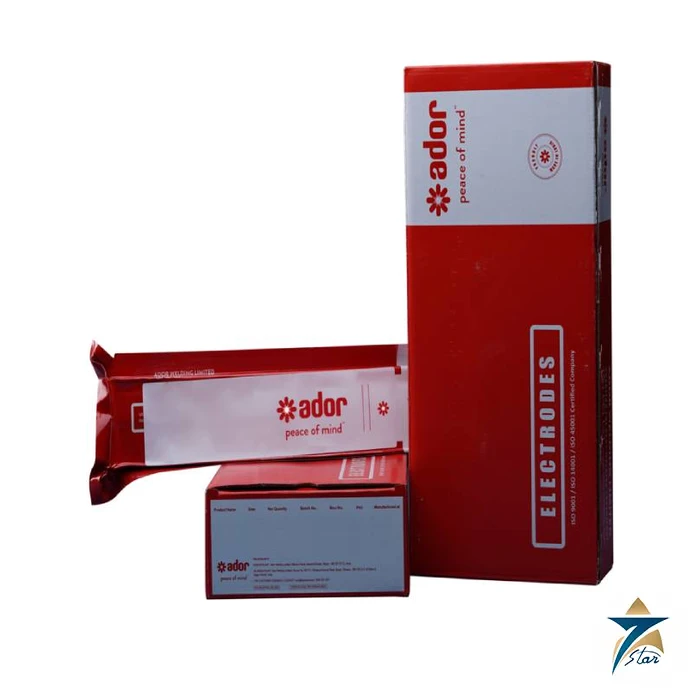
Ador Cromoten is a chrome-moly stick electrode for high temperature service, classified AWS A/SFA 5.5 E8018-B2, EN ISO 3580-A E CrMo1 B 32 H5 and IS 1395 E 55B-B2. It deposits a 1.25Cr-0.5Mo weld metal that matches the P11 and P12 family of steels used for steam piping, boiler tubes, headers and hot process lines. Ador Welding describes the Ador Cromoten as a basic coated iron powder electrode with radiographic quality, positional welding capability and resistance to creep and heat up to 550°C.
Seven Star LLC supplies Ador Cromoten to power plant, refinery and boiler maintenance contractors across the Sultanate of Oman and the GCC. Shutdowns at refineries in Sohar and Muscat, steam systems at independent power and water plants, and fired heater and boiler repair work all depend on correctly matched Cr-Mo consumables, and our Muscat team provides the datasheet, procedure context and lead time coordination.
As general metallurgical knowledge, chromium and molybdenum are added to steel to keep strength at elevated temperature and to resist slow deformation, known as creep, under long-term stress. Chromium also improves oxidation resistance in steam and hot gases. A 1.25Cr-0.5Mo steel such as SA 335 P11 is therefore common for steam lines and hydrocarbon process piping operating at temperatures where plain carbon steel would lose strength over time.
The same alloying that gives these properties also makes the steel and weld hardenable. Welds in Cr-Mo steel need controlled preheat to slow cooling and avoid hard, crack-prone microstructures, and post-weld heat treatment to temper the weld and heat-affected zone and relieve residual stress. The Ador Cromoten datasheet reflects this directly: it specifies preheat and interpass temperature of 150–200°C followed by PWHT, and reports properties after 690°C for one hour.
Typical undiluted weld chemistry for Ador Cromoten is 0.06 percent carbon, 0.7 percent manganese, 0.6 percent silicon, 1.3 percent chromium and 0.5 percent molybdenum. After PWHT at 690°C for one hour, the all-weld-metal tensile strength is typically 615 MPa, yield 525 MPa and elongation 24 percent, with typical Charpy energy of 70 J at 27°C. Specification values printed are 550 MPa tensile, 460 MPa yield and 19 percent elongation minimum. Diffusible hydrogen is below 5 ml per 100 g.
The electrode welds on AC with 70 V open-circuit voltage or on DCEP, in 2.5 × 350, 3.15 × 450, 4.0 × 450 and 5.0 × 450 mm sizes. Standard packing is a 20 kg box of four 5 kg cartons, with vacuum packing available. For other processes Ador lists matching consumables: Automig 80S-B2 for GMAW, Tigfil 80S-B2 for GTAW, Automig FC81T1-B2 for FCAW, and Automelt B20 Plus flux with Automelt EB2 wire for SAW, which lets one alloy system cover TIG roots, stick fill and automatic seams.
Ador lists these features for Ador Cromoten:
The datasheet lists welding of 1.25Cr-0.5Mo and 1Cr-0.5Mo steels in refineries, power plants and chemical plants; pressure vessels and boilers; Cr and Cr-Mo bearing steels at elevated temperature such as steam production plants and steam pipes; and joining of P4 materials including ASTM SA 182 Gr. F2, F11 and F12, SA 213 Gr. T11 and T12, SA 335 Gr. P11 and P12, SA 387 Gr. 2, 11 and 12, plus 13CrMo44, 15CrMo5, 15Cr3, 16MnCr5 and 20MnCr5. In Oman the Ador Cromoten is typically used on steam and condensate systems at combined cycle plants, hydrotreater and reformer piping, and boiler tube replacement during planned turnarounds.
Seven Star LLC supplies Ador Cromoten together with the machines and wires used on the same jobs. A multi-process inverter such as the ESAB Rebel EMP 285ic or a heavy-duty source like the Lincoln Electric Power Wave S500 handles stick welding of Cr-Mo spools, and carbon steel structural work on the same site may use the Lincoln Electric SuperArc L-59 wire. Other stick grades are listed in our welding electrodes category.
Ador recommends 60–90 A for 2.5 mm, 100–140 A for 3.15 mm, 140–180 A for 4.0 mm and 190–250 A for 5.0 mm. As general practice on P11 piping, the root is often TIG welded with matching B2 wire and the joint is filled and capped with the stick electrode, while preheat is maintained throughout and the joint is taken to PWHT without being allowed to cool uncontrolled where the procedure requires.
The electrode should be redried at 250–300°C for a minimum of one hour and kept in a holding oven. Exact preheat, interpass, PWHT temperature and holding time must follow the qualified procedure and the governing code for the project.
The table lists Ador Cromoten data from the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Cromoten |
| Type | Basic coated iron powder, low alloy high temperature electrode |
| AWS classification | AWS A/SFA 5.5 E8018-B2 |
| EN ISO / IS classification | EN ISO 3580-A E CrMo1 B 32 H5; IS 1395 E 55B-B2 |
| Approvals listed | ABS / IBR / NPCIL / BHEL / NTPC / BIS / CE |
| Typical weld metal chemistry | C 0.06, Mn 0.7, Si 0.6, Cr 1.3, Mo 0.5 (wt %) |
| Condition tested | PWHT 690°C for 1 hour |
| Tensile strength | Typical 615 MPa; specification 550 MPa min |
| Yield strength | Typical 525 MPa; specification 460 MPa min |
| Elongation | Typical 24%; specification 19% min |
| CVN impact at 27°C | Typical 70 J |
| Preheat / interpass | 150–200°C, followed by PWHT |
| Current | AC (70 OCV) / DCEP |
| Sizes and amperage | 2.5 × 350 mm: 60–90 A; 3.15 × 450 mm: 100–140 A; 4.0 × 450 mm: 140–180 A; 5.0 × 450 mm: 190–250 A |
| Positions | All positions except vertical down |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg box of 4 cartons of 5 kg; vacuum packing available |
For Ador Cromoten electrodes for a shutdown or new-build project in Oman or the GCC, send Seven Star LLC your sizes and quantities. We will return a formal quotation with the Ador Cromoten datasheet and can propose matching B2 TIG and MIG wires, with engineering support and lead time coordination from Muscat.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.