Rutile 25 9 4 electrode with AC and DC capability
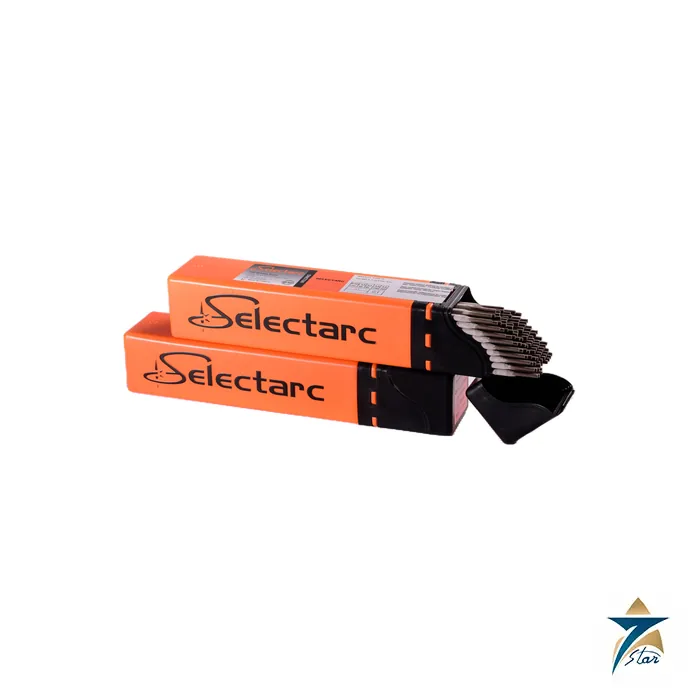
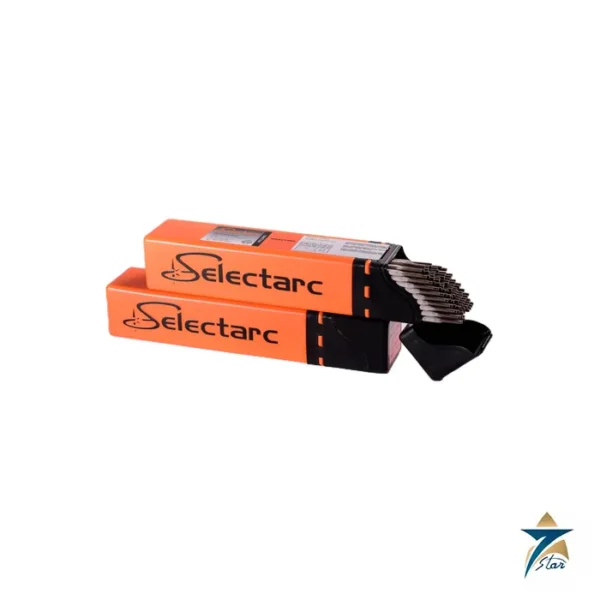
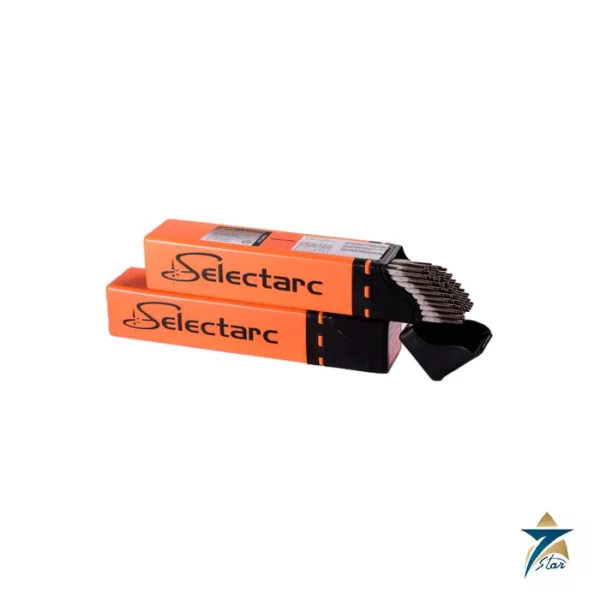
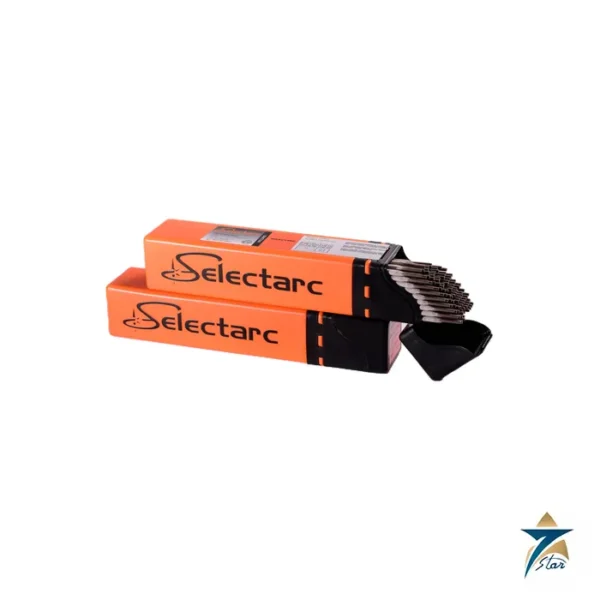
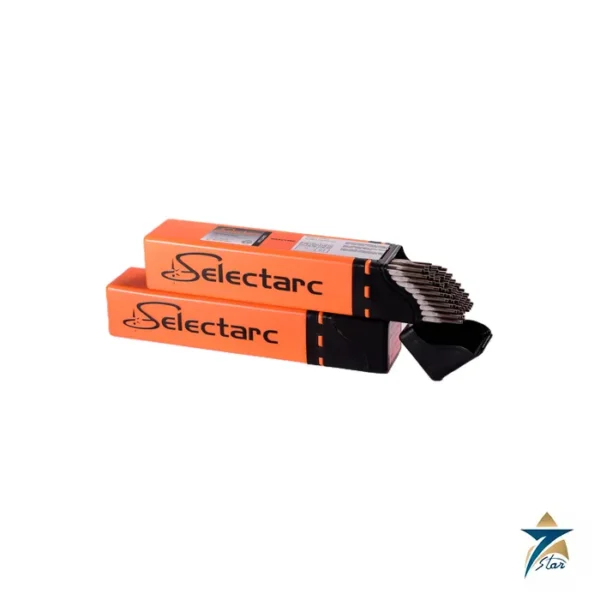
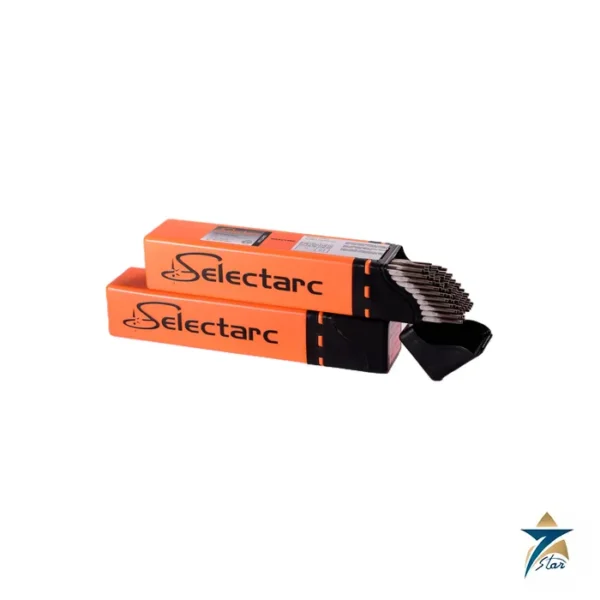
The Selectarc Inox 2509MoR is the rutile coated member of Selectarc super duplex stick electrode range. Its deposit is austenitic-ferritic with a typical ferrite number of about 40 (WRC) and a pitting index above 40, classified AWS A5.4 E2594-16 and ISO 3581-A E 25 9 4 N L R 3 2.
Selectarc rates the weld metal for operation up to 250 °C and for resistance to pitting, crevice and stress corrosion in chloride media. Listed uses are butt welding and cladding of wrought and cast super duplex in pumps, vessels and piping attacked by chloride solutions, and welding of impellers and other high-strength parts exposed to corrosion.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / Inox 2509MoR |
| Process |
SMAW (manual metal arc) |
| AWS classification |
A5.4 E2594-16 |
| ISO classification |
3581-A E 25 9 4 N L R 3 2 |
| Coating |
Rutile |
| Typical weld metal, % |
C under 0.03, Si 0.75, Mn 0.7, Cr 24.8, Ni 9.3, Mo 4.0, Cu 0.1, N 0.25, P under 0.030, S under 0.020, Fe remainder |
| Ferrite number (WRC) |
About 40 |
| Pitting index |
Above 40 |
| Yield strength Rp0.2 |
690 MPa |
| Tensile strength Rm |
890 MPa |
| Elongation A5 |
25% |
| Impact energy KV |
Above 50 J at +20 °C; above 35 J at -40 °C |
| Sizes and current |
2.5 × 300 mm, 55–85 A; 3.2 × 350 mm, 70–110 A; 4.0 × 350 mm, 110–150 A |
| Current type |
DC electrode positive or AC (open circuit voltage above 70 V) |
| Drying |
2–3 h at 250–300 °C |
| Interpass temperature |
Below 150 °C |
Rutile versus basic super duplex electrodes
A rutile coating gives easier arc striking, smooth bead shape and simple slag removal, and the electrode can run from AC transformers as well as DC sources. That makes Inox 2509MoR practical for cladding, repair and general fabrication of super duplex parts, especially in workshops where cosmetic finish matters. The basic version, Inox 2509MoB (E2594-15), runs on DC+ only but its data sheet gives higher impact energy, so it is usually preferred for thick restrained joints and pressure parts with demanding Charpy requirements.
Base materials listed for the rutile grade are identical: UNS S32750 (2507, 1.4410), S32760 (1.4501), S32550 (1.4517), 52N+ (1.4507), S31803 (1.4462), S32304 (1.4362) and S32900 (1.4460).
Handling and technique
Dry the electrodes for 2 to 3 hours at 250–300 °C before use. Hold them with a slight inclination, keep a short arc, and limit the interpass temperature to 150 °C. These measures keep the cooling rate in the range that gives a balanced austenite-ferrite structure and prevents intermetallic precipitation.
On pipe, a GTAW root followed by electrode fill and cap passes is common practice. On overlays applied to carbon steel, the first layer is diluted and can fall below the super duplex corrosion requirement, so plan at least two layers and confirm the surface chemistry. Qualification for super duplex typically adds ferrite measurement, impact tests and an ASTM G48 corrosion test to the usual mechanical tests.
Rutile coatings absorb moisture more readily than one might expect from their easy handling, and hydrogen is not the main concern in super duplex, but wet coatings still cause porosity and erratic arc behaviour. Keep opened packets in a holding oven and redry any electrodes left out overnight.
Documents and quotation
The Selectarc Inox 2509MoR data sheet is attached. More grades are listed in our Welding Electrodes category.
For a quotation, send diameters, quantities and certificate requirements.

Reviews
There are no reviews yet.