
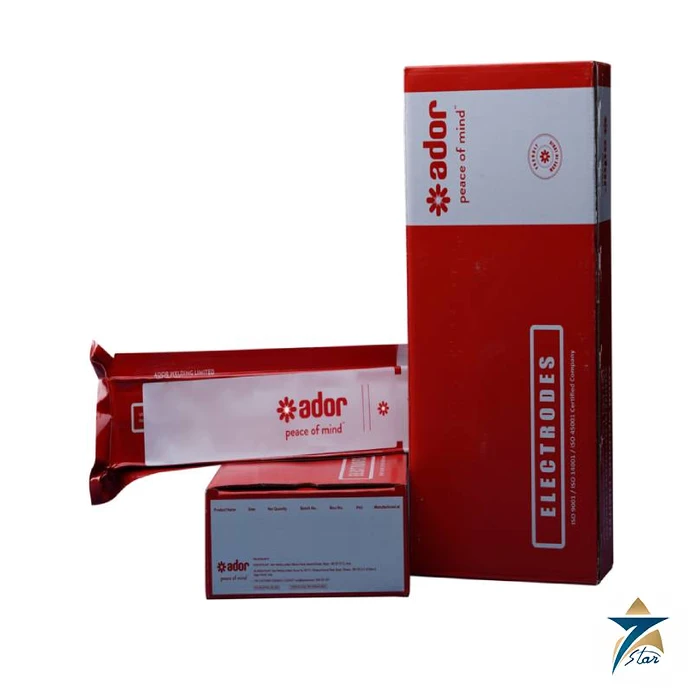
Ador Ultracorten I is a low alloy stick electrode for weathering steel, classified AWS A/SFA 5.5 E7018-W1. It is a basic type iron powder electrode that deposits chromium-nickel-copper low alloy weld metal, so the finished joint shares the atmospheric corrosion resistance of the parent plate instead of becoming a rust-prone line along a weathering steel structure. Ador Welding lists excellent atmospheric corrosion resistance, high crack resistance under restraint, radiographic quality and all-position capability as the key strengths of the Ador Ultracorten I.
Seven Star LLC supplies Ador Ultracorten I to structural steel fabricators, chimney and stack builders, heat recovery and power plant contractors across the Sultanate of Oman and the GCC. Exhaust stacks at gas turbine power stations and desalination plants, architectural facades and bridges built from CORTEN-type steel all need a matching electrode, and our Muscat office supports specifiers with the datasheet and lead time coordination.
Weathering steel, described here as general metallurgical knowledge, is a low alloy structural steel containing small amounts of copper, chromium, nickel and sometimes phosphorus. Exposed to cycles of wetting and drying, it develops a dense, adherent oxide layer, often called a patina, that slows further corrosion. That is why weathering steel is often left unpainted on bridges and building facades, and why it is used in flue gas ducts and stacks where the inside surface sees corrosive condensate.
If such a structure is welded with an ordinary carbon steel electrode, the weld metal lacks those alloying elements and can corrode faster and look different from the surrounding plate. The Ador Ultracorten I avoids this by adding chromium, nickel and copper to the deposit. For single-pass fillet welds, dilution from the base plate also contributes alloy, but for multi-pass and exposed cap passes a matching weathering electrode is the usual specification.
Ador gives the typical undiluted weld chemistry of the Ador Ultracorten I as 0.035 percent carbon, 0.65 percent manganese, 0.6 percent silicon, 0.25 percent chromium, 0.3 percent nickel and 0.5 percent copper. As welded, the all-weld-metal tensile strength is typically 540 MPa, yield 450 MPa and elongation 25 percent, with Charpy V-notch energy of 80 J at -20°C. The specification column requires 490 MPa, 415 MPa, 22 percent and 47 J minimum, and diffusible hydrogen is below 5 ml per 100 g.
The electrode is supplied in three diameters, 3.15, 4.0 and 5.0 mm, each 450 mm long, and is welded on DC electrode positive. Ador packs it in a 20 kg box containing four 5 kg cartons, and vacuum packing is available. The low carbon content of the deposit, combined with the basic coating, is part of what gives the high crack resistance under restraint that Ador highlights for thick or rigid structural joints.
The Ador Ultracorten I datasheet lists the following features, explained in practical terms:
Ador names welding of weathering steels such as CORTEN-A and CORTEN-B and their equivalents, steels to ASTM A242 and A588, and applications in bridges, architectural structures, exhaust gas flues and chimneys. In Oman the most frequent use of the Ador Ultracorten I is on exhaust stacks, bypass stacks and flue ducts of gas turbine and heat recovery steam generator installations at power and water plants, where weathering steel resists the corrosive condensate. Architectural steel in public buildings, pedestrian bridges and landscape structures in Muscat and other cities also use CORTEN-type plate.
Seven Star LLC supplies the Ador Ultracorten I alongside welding equipment and wires for the same projects. Structural shops can pair it with a multi-process machine such as the ESAB Rebel EMP 285ic or a production MIG source like the Lincoln Electric Power Wave S500, and carbon steel seams elsewhere in a project can use submerged arc wire like the LongTeng EL8. Other stick electrodes are listed in our welding electrodes category.
For the Ador Ultracorten I the datasheet specifies DCEP at 100–140 A for 3.15 mm, 140–180 A for 4.0 mm and 190–250 A for 5.0 mm. As general practice, structural welders keep a short arc with low hydrogen electrodes, use stringer or moderate weave beads, and clean slag fully between passes. Where the weld will remain exposed and unpainted, the final cap should be deposited with the weathering electrode so that the visible surface weathers like the plate.
Redrying is specified at 250–300°C for a minimum of one hour. Opened electrodes should be stored in a holding oven and issued in heated quivers, especially in humid coastal locations such as Sohar, Sur and Salalah.
The specification values for the Ador Ultracorten I below come from the manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Ultracorten I |
| Type | Basic iron powder, Cr-Ni-Cu low alloy weathering steel electrode |
| AWS classification | AWS A/SFA 5.5 E7018-W1 |
| Typical weld metal chemistry | C 0.035, Mn 0.65, Si 0.6, Cr 0.25, Ni 0.3, Cu 0.5 (wt %) |
| Tensile strength | Typical 540 MPa; specification 490 MPa min |
| Yield strength | Typical 450 MPa; specification 415 MPa min |
| Elongation | Typical 25%; specification 22% min |
| CVN impact at -20°C | Typical 80 J; specification 47 J min |
| Diffusible hydrogen | Below 5 ml/100 g |
| Base steels listed | CORTEN-A, CORTEN-B and equivalents; ASTM A242, A588 |
| Current | DCEP |
| Sizes and amperage | 3.15 × 450 mm: 100–140 A; 4.0 × 450 mm: 140–180 A; 5.0 × 450 mm: 190–250 A |
| Positions | All positions except vertical down |
| Redrying | 250–300°C for minimum 1 hour |
| Packing | 20 kg box of 4 cartons of 5 kg; vacuum packing available |
Seven Star LLC can quote Ador Ultracorten I for stacks, flues, bridges and architectural steel in Oman and the GCC. Send the diameters and quantity, and we will respond with a formal quotation and the Ador Ultracorten I datasheet, along with engineering support and lead time coordination from Muscat.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.