
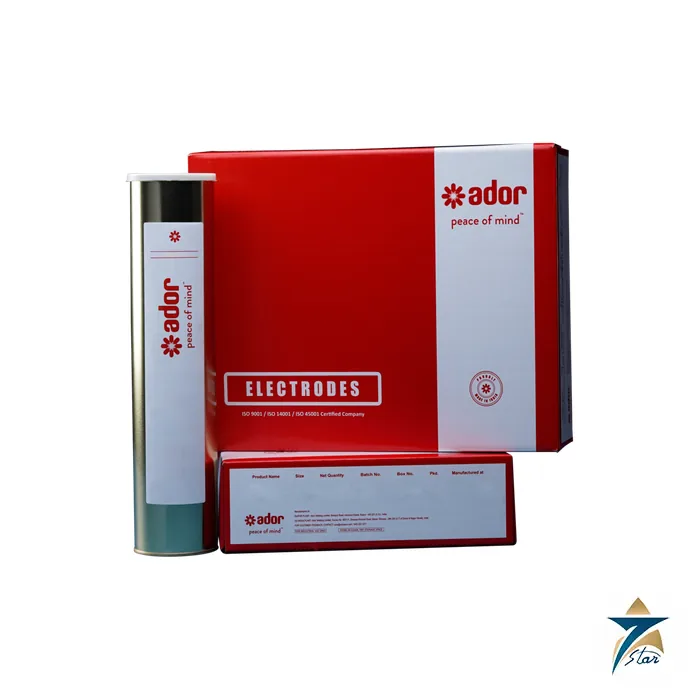
Ador Celwel 80P is the high-strength member of the Ador Welding cellulosic pipeline range. It is classified AWS A/SFA 5.5 E8010-P1 and EN ISO 2560-A E 46 3 1Ni C 21, and its weld deposit contains a deliberate nickel addition to reach the strength and low-temperature toughness demanded by modern high tensile line pipe. Ador recommends the Ador Celwel 80P for vertical-down welding of high strength, medium and large diameter pipelines, for root and capping runs, and particularly for hot passes, where a strong, crack-resistant layer has to be laid quickly over a fresh root.
Seven Star LLC supplies the Ador Celwel 80P to pipeline builders and EPC contractors in the Sultanate of Oman and across the GCC. Long-distance gas transmission, export lines to coastal terminals and high-pressure injection systems increasingly use X65 and X70 pipe, and our Muscat team supports buyers with the manufacturer datasheet, consumable selection for each pass and lead time coordination.
In general terms, line pipe strength has risen over the decades from X42 and X52 to X65, X70 and above, so that thinner walls can carry the same pressure. A weld must normally match or exceed the strength of the pipe it joins. A standard E6010 deposit does not reach the yield needed for X70, which is why E8010-P1 electrodes were developed: they keep the cellulosic arc and vertical-down capability but add alloying elements to lift strength. Nickel is used because it raises strength while improving toughness at low temperature.
The hot pass is the second layer in a pipeline weld. Its job, described here as general practice, is to burn out the slag lines left along the toes of the root, to add thickness quickly so the joint can be lowered or moved, and to temper the root. Because it is laid soon after the root on a pipe that may be under restraint, the hot-pass material benefits from good strength and toughness, which is the role Ador assigns to the Ador Celwel 80P.
The typical undiluted weld metal of the Ador Celwel 80P contains 0.1 percent carbon, 1.0 percent manganese, 0.2 percent silicon and 0.6 percent nickel. In the as-welded condition the all-weld-metal tests give typically 555 MPa tensile strength, 470 MPa yield strength and 24 percent elongation, with Charpy V-notch energy of 60 J at -30°C. Ador prints specification values of 550 MPa minimum tensile, 460 MPa minimum yield, 19 percent minimum elongation and 47 J minimum impact energy.
The product is made in 2.5, 3.15, 4.0 and 5.0 mm diameters, all 350 mm long, and welded on DC electrode positive. It ships in an 18 kg box or tin holding three 6 kg cartons. As general advice for any cellulosic electrode, the coating relies on retained moisture for its arc characteristics, so the rods are used from their packing without the high-temperature redrying that basic electrodes need, and opened cartons should be protected from wetting and from long exposure to hot sun.
Ador lists the following features for the Ador Celwel 80P on its datasheet, expanded here with practical context:
The manufacturer lists the Ador Celwel 80P for vertical down welding of high strength, medium and large diameter pipelines, for high tensile pipe steels such as API 5L X60, X65 and X70, and for welding thin API 5L X80 pipes. In Oman these grades appear on gas transmission lines feeding power and desalination plants, on export pipelines to Sohar and Duqm, and on high-pressure lines in the oil and gas concession areas. Elsewhere in the GCC, the same pipe grades are used on cross-border gas networks and new industrial gas corridors.
Seven Star LLC supplies the Ador Celwel 80P together with the wider welding package that pipeline and station contractors need. Fabrication shops producing station piping and spools often weld with MIG equipment such as the ESAB Rebel EMP 285ic or the Lincoln Electric Power Wave S500, and submerged arc double-jointing uses wire like the LongTeng EL8. Root and hot pass electrodes from other grades are listed in our cellulosic pipeline electrodes category.
The Ador Celwel 80P runs on DCEP at 60–90 A for 2.5 mm, 80–140 A for 3.15 mm, 120–180 A for 4.0 mm and 160–200 A for 5.0 mm. As general guidance, hot passes are usually run with a slightly higher current and faster travel than the root so that the slag lines are washed out without burning through. The best settings for a particular joint come from procedure qualification and welder practice coupons.
Pipeline codes and company specifications set the preheat, the maximum interval between root and hot pass and other controls for cellulosic welding on high-strength pipe, because hydrogen cracking risk rises with pipe strength. Those controls should be taken from the qualified welding procedure specification. Keep cartons sealed until use and rotate stock so older material is used first.
All values are from the Ador Celwel 80P manufacturer datasheet.
| Parameter | Specification |
|---|---|
| Model | Ador Celwel 80P |
| Coating type | Cellulose type, cellulosic pipeline electrode |
| AWS classification | AWS A/SFA 5.5 E8010-P1 |
| EN ISO classification | EN ISO 2560-A E 46 3 1Ni C 21 |
| Approvals listed | CE |
| Typical weld metal chemistry | C 0.1, Mn 1.0, Si 0.2, Ni 0.6 (wt %) |
| Tensile strength | Typical 555 MPa; specification 550 MPa min |
| Yield strength | Typical 470 MPa; specification 460 MPa min |
| Elongation | Typical 24%; specification 19% min |
| CVN impact at -30°C | Typical 60 J; specification 47 J min |
| Pipe steels listed | API 5L X60, X65, X70; thin X80 pipe |
| Current | DCEP |
| Sizes and amperage | 2.5 × 350 mm: 60–90 A; 3.15 × 350 mm: 80–140 A; 4.0 × 350 mm: 120–180 A; 5.0 × 350 mm: 160–200 A |
| Positions | All positions, specifically vertical down |
| Packing | 18 kg box / tin containing 3 cartons of 6 kg |
For a quotation on Ador Celwel 80P, send Seven Star LLC the pipe grade, wall thickness, diameters and required quantity. We will reply with a formal offer and the Ador Celwel 80P datasheet, and our Muscat team can advise on the root, fill and cap consumables and coordinate availability and engineering support for projects in Oman and the GCC.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.