Rutile flux-cored wire for all-position carbon steel welding
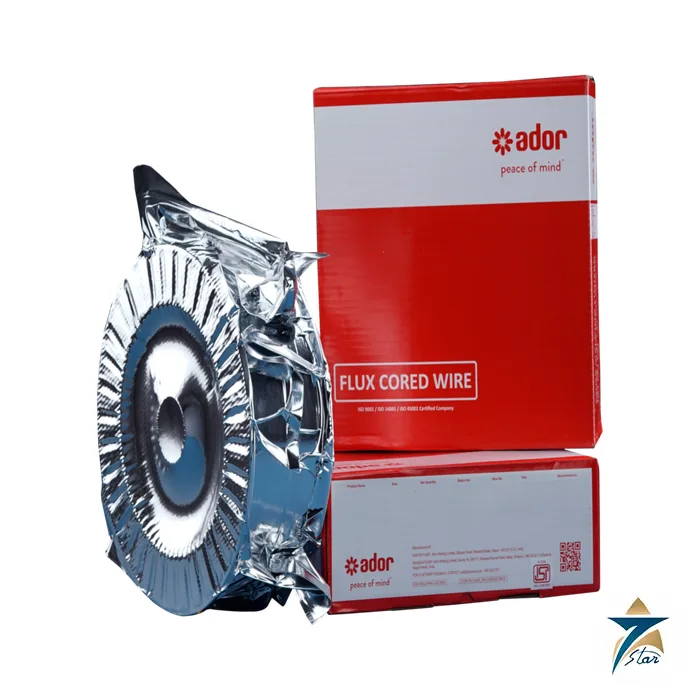
The Ador Automig FC 71T-1 is a rutile-type, gas-shielded flux-cored wire classified AWS A5.20 E71T-1C and EN ISO 17632-A T 42 2 P C1 2. Ador lists low fumes and minimal spatter, easy slag removal, a smooth weld bead, a high deposition rate and radiographic-quality welds, with all-position capability on DCEP using CO2 shielding.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Ador Welding / Automig FC 71T-1 |
| Process |
FCAW C-Mn steel, gas-shielded, rutile |
| AWS classification |
A5.20 E71T-1C |
| EN ISO classification |
17632-A T 42 2 P C1 2 |
| Approvals listed |
ABS, BV, DNV, LRA, IRS, IBR, CE |
| Undiluted weld metal, typical % |
C 0.06, Mn 1.4, Si 0.4 |
| Tensile strength, as welded (typical) |
600 MPa |
| Yield strength at 0.2% offset |
490 MPa |
| Elongation |
25% |
| Charpy V impact at -20 °C |
35 J |
| Hardness, 3 layers |
200 BHN max |
| Diameters |
1.2 and 1.6 mm |
| Net weight |
15 kg |
| Polarity / positions |
DCEP; all positions except vertical down |
| Shielding gas |
CO2 at 15-20 l/min |
Typical applications
Ador points to C-Mn steel with tensile strength up to 500 MPa, in bridges, shipbuilding, towers and cranes, chemical plant machinery and hulls, storage tanks and structural steel, construction equipment, farm machinery and rolling stock. In short, it is a general-purpose rutile wire for carbon steel fabrication where a steady arc and little cleanup matter.
Reading the classification
In E71T-1C, the 7 stands for a minimum tensile strength of 70 ksi, the 1 for all-position welding, T for a tubular wire, the 1 for the usage group, and the C for CO2 shielding. The EN designation T 42 2 P C1 2 reads as a 420 MPa class with 47 J at -20 °C, a rutile slag type, CO2 gas and positional capability. The typical impact result on the Ador sheet is 35 J at -20 °C; where the specification calls for 47 J at that temperature, confirm the batch certificate rather than relying on the typical value.
The 15 kg net weight is convenient for wire feeders in structural shops. Use CO2 at 15 to 20 litres a minute with the contact tip set back according to the torch maker. Because rutile cored wires deposit quickly, procedure heat-input limits become important on thick plate. When joint fit-up is poor the high deposition tempts overheating, so use stringer beads in the vertical-up position to keep the pool small.
For a chrome-moly cored wire in the same range, see Ador Automig FC 91T1-B3.
Documents and quotation
The Ador Automig FC 71T-1 data sheet is attached to this page for download. Related consumables are listed in our Flux-Cored Welding Wire category.
For a quotation, send the diameter or size, pack type, quantity and any certificate or approval requirement.


Reviews
There are no reviews yet.