
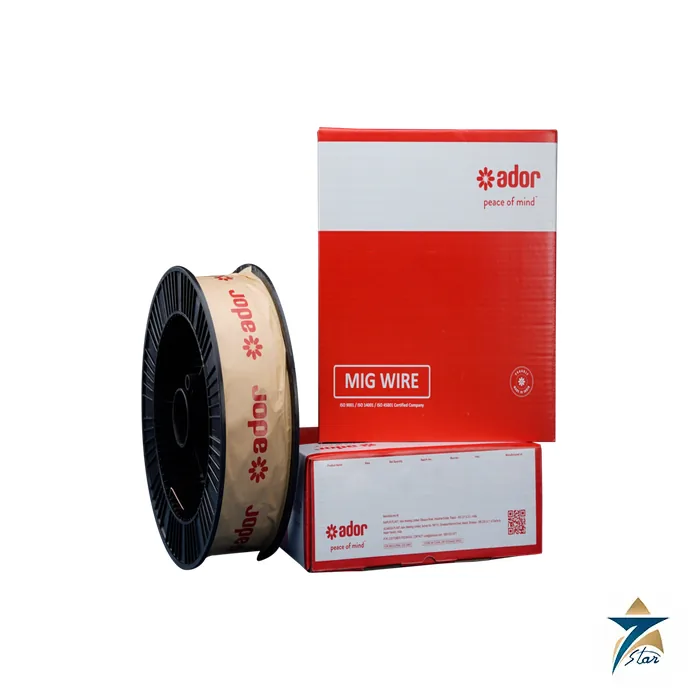
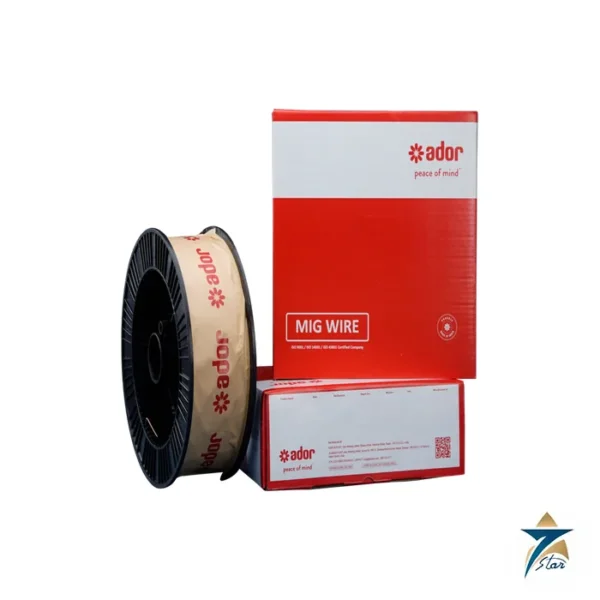
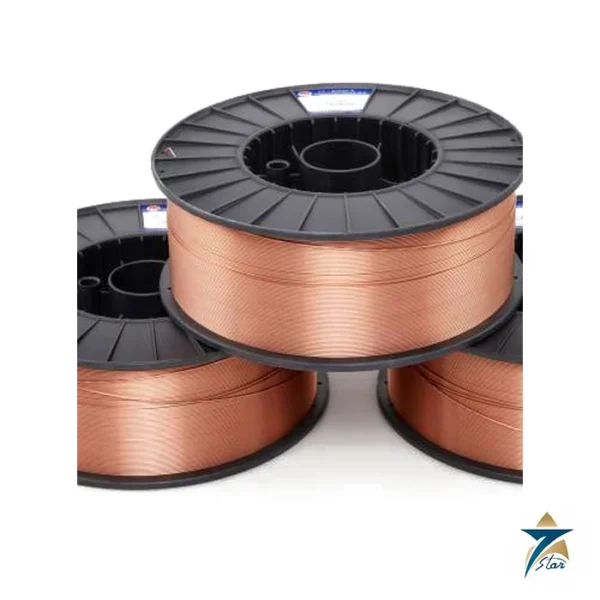
Ador Automig 90S-B3 is a copper-coated low alloy solid wire for gas metal arc welding, classified to AWS A/SFA 5.28 ER90S-B3 and EN ISO 21952-B G 62 M13 2C1M. It deposits a typical 2.25Cr-1Mo weld metal, which places it in the chrome-moly family used for creep resistant steels that stay in service at elevated temperature for many years. Ador Welding Limited describes the wire as giving notch-free welds of radiographic quality, with superior strength and toughness after post weld heat treatment. For fabricators who already qualify their root and fill passes with semi-automatic MIG, the Ador Automig 90S-B3 is the solid-wire option for P22-type piping and plate where productivity matters more than the slower deposition of TIG or stick.
Seven Star LLC supplies the Ador Automig 90S-B3 to refinery, petrochemical, fertilizer and power contractors in Muscat, Sohar, Duqm and the wider GCC. Our Muscat team works from the official Ador technical data sheet, which is attached to this page, so welding engineers can check the chemistry, the PWHT mechanical values and the creep data against their procedure qualification records before ordering.
As general welding background, chromium and molybdenum are added to ferritic steels to hold strength and resist creep and oxidation at temperatures where plain carbon steel would slowly deform. Grades such as ASTM A335 P22 pipe and A387 Grade 22 plate rely on roughly 2.25 percent chromium and 1 percent molybdenum, and a matching filler is normally required so that the weld does not become the weak link of a hot pressure system. The typical bare wire analysis printed for the Ador Automig 90S-B3 is 0.09 C, 0.6 Mn, 0.5 Si, 2.45 Cr and 0.95 Mo, which lines up with that base-metal family.
Chrome-moly weld metal is hardenable, so industry practice is to control preheat and interpass temperature and to apply post weld heat treatment. Ador reports its all weld metal properties after a PWHT of 690°C for one hour, and that is the condition in which the mechanical figures below should be read. Always follow the qualified WPS and the governing code for actual preheat and soak times.
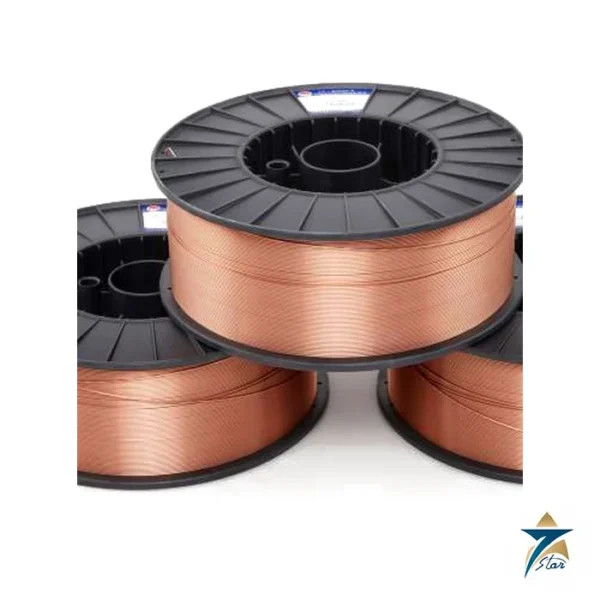
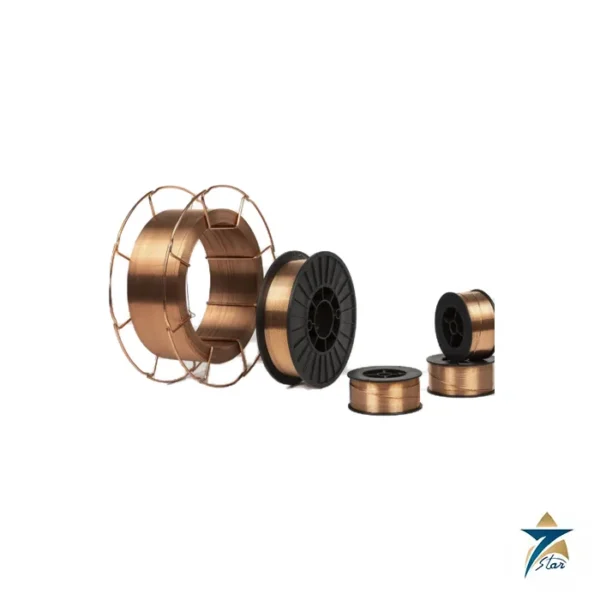
The wire carries a uniform copper coating. In general terms, copper coating protects the wire surface during storage and improves current pick-up at the contact tip, which supports a steadier arc during long runs on a pipe positioner or a plate seam. The datasheet lists two diameters, 1.2 mm and 1.6 mm, both on 15 kg spools, and states all-position use on DCEP (electrode positive). Recommended shielding is argon with 1 to 5 percent oxygen at 15 to 20 litres per minute.
Ador also publishes creep test data for this product, which is less common on a one-page sheet. After PWHT at 690°C for one hour, the deposit recorded 0.92 percent strain after 1000 hours at 550°C under 140 MPa, and 1.28 percent strain after 1000 hours at 600°C under 80 MPa. These values give designers a reference point for the high-temperature behaviour of Ador Automig 90S-B3 weld metal, alongside the room temperature tensile properties.
The points below summarise what the manufacturer data sheet states for the Ador Automig 90S-B3.
Ador lists the welding of 2.25Cr-0.5Mo and 2.25Cr-1Mo creep resistant steels, joining of ASTM A335 Gr. P22 and A387 Gr. 22 materials, joining of P5A materials, Cr-Mo and Cr-Mo-V bearing steels for high temperature service, and German grades such as 12CrMo9-10 and 10CrSiMoV7. In practice that means hot process lines in refineries, petrochemical units and fertilizer plants. Around Oman this covers hydrotreater and reformer piping at the Sohar and Duqm refineries, steam and condensate systems in ammonia and urea complexes, and heater coil connections in gas processing trains. The Ador Automig 90S-B3 is a natural fit where a contractor wants to raise deposition rate on fill passes after a TIG root.
Power and utility work is the other major user. Independent water and power projects in the Sultanate run steam headers, desuperheater lines and boiler pressure parts in chrome-moly steels, and shutdown repairs on that pipework are usually time-critical. Seven Star LLC supplies the Ador Automig 90S-B3 for those planned outages and new-build packages, together with matching consumables from the same chemistry family, so a contractor can source the MIG wire, the TIG rod and the flux-cored wire for one P22 job from a single supplier in Muscat.
The table below reproduces the values from the official Ador Automig 90S-B3 data sheet. Chemistry is for bare solid wire; mechanical values are typical all weld metal results.
| Parameter | Specification |
|---|---|
| Model | Ador Automig 90S-B3 |
| Process | GMAW (MIG/MAG), low alloy steel, high temperature |
| AWS classification | A/SFA 5.28 ER90S-B3 |
| EN ISO classification | EN ISO 21952-B G 62 M13 2C1M |
| IS classification | IS 6419 SLA-4-M-561 |
| Approvals | CE |
| Typical wire chemistry, wt % | C 0.09, Mn 0.6, Si 0.5, Cr 2.45, Mo 0.95 |
| UTS (PWHT 690°C, 1 h) | 680 MPa |
| Yield strength 0.2% offset | 600 MPa |
| Elongation | 20 % |
| Creep, 550°C / 140 MPa / 1000 h | 0.92 % strain |
| Creep, 600°C / 80 MPa / 1000 h | 1.28 % strain |
| Diameters | 1.2 mm and 1.6 mm |
| Packing | 15 kg spool |
| Polarity and positions | DCEP, all positions |
| Shielding gas | Ar + 1-5 % O2, 15-20 L/min |
| Storage | Keep dry; follow handling instructions on the box |
For carbon steel MIG work on the same project, see the Lincoln Electric SuperArc L-59 ER70S-6 wire. A suitable pulsed MIG power source is the Lincoln Electric Power Wave S500, and for submerged arc seams there is the LongTeng EL8 SAW wire. You can browse all solid welding wire in our catalogue.
To order the Ador Automig 90S-B3, send Seven Star LLC your required diameter, quantity and delivery point in Oman or the GCC, along with the WPS or code reference if you need us to confirm suitability. Download the Ador Automig 90S-B3 datasheet from this page for your procedure file, and contact our welding consumables team in Muscat for a formal quotation and technical support.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.
Reviews
There are no reviews yet.