Overview
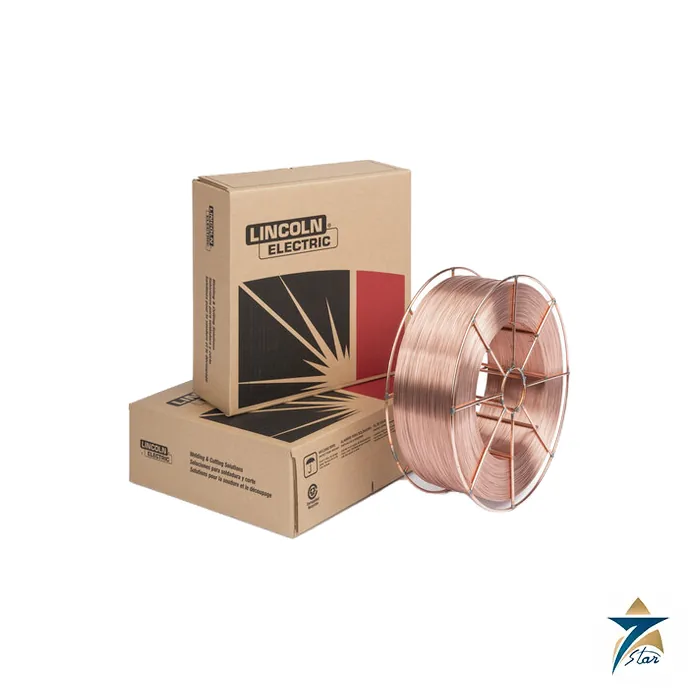
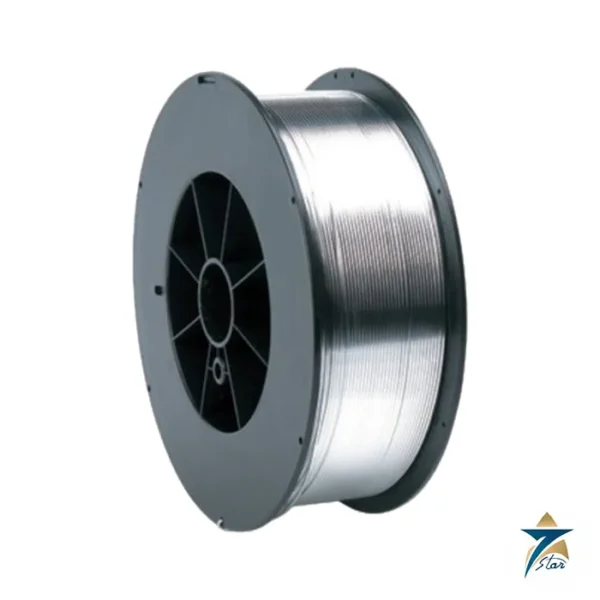
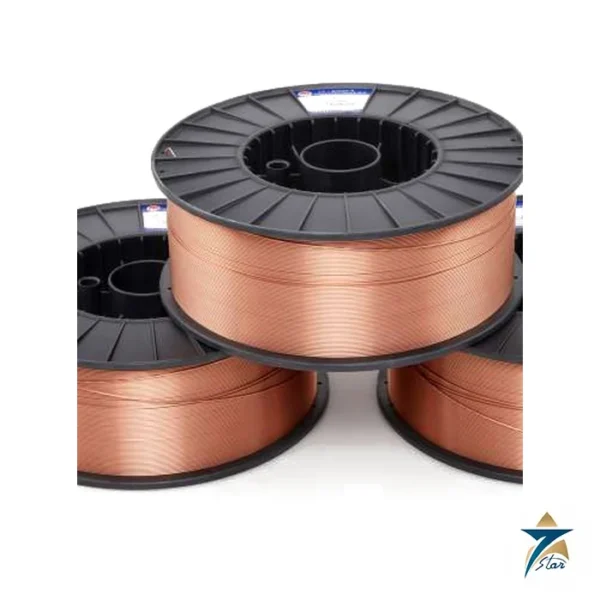
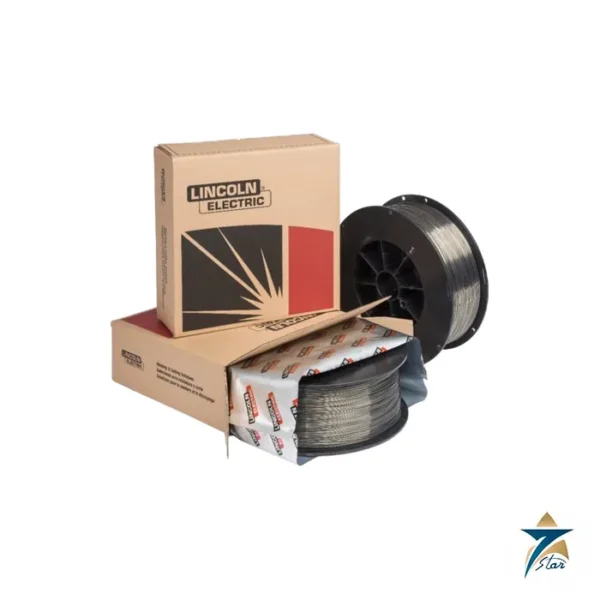
Lincoln Electric SuperArc L-59 is a copper coated mild steel solid wire classified as AWS ER70S-6 and intended for gas metal arc welding, commonly called MIG or GMAW. It belongs to the SuperArc family of solid wires from Lincoln Electric and is one of the most widely specified general purpose carbon steel wires in structural, pressure and automated fabrication. The manufacturer datasheet lists an engineered alloy system that improves silicon island management, minimal spatter, a copper coating for long contact tip life, fast travel speeds and a MicroGuard Ultra surface treatment for superior feeding and arc stability.
Seven Star LLC supplies Lincoln Electric SuperArc L-59 to fabricators, EPC contractors and maintenance workshops in the Sultanate of Oman and the wider GCC, with engineering support from Muscat. Buyers who need a deoxidised ER70S-6 wire that tolerates mill scale, handles both short circuit and spray transfer, and runs on robotic cells as well as semi-automatic guns can request this product together with the datasheet and the matching shielding gas recommendation.
How a Solid ER70S-6 Wire Works in the Arc
In the GMAW process a continuously fed solid wire carries welding current, melts in the arc and transfers into the joint while a flow of shielding gas displaces air from the molten pool. The ER70S-6 designation means a solid electrode (the letter S) with a minimum tensile strength of 70 ksi (the digits 70) and a chemistry tagged 6, which carries the highest silicon and manganese levels of the common mild steel wires. Those deoxidisers combine with oxygen in the weld pool, forming small silicate islands on the bead surface while leaving a sound, pore free deposit. This is why Lincoln Electric SuperArc L-59 tolerates light rust and mill scale better than low silicon wires such as ER70S-3.
The same deoxidiser content in Lincoln Electric SuperArc L-59 allows wider choices of shielding gas. According to the datasheet, Lincoln Electric SuperArc L-59 is used with 100 percent CO2, with argon and CO2 mixtures in the range 75 to 95 percent argon, and with 95 to 98 percent argon and balance oxygen, at a flow rate of 30 to 50 CFH. With Lincoln Electric SuperArc L-59, pure CO2 gives deeper penetration and lower gas cost, argon rich mixtures give a smoother spray arc with less spatter, and the choice moves the typical mechanical results shown in the table below.
Engineering Design of the Lincoln Electric SuperArc L-59 Wire
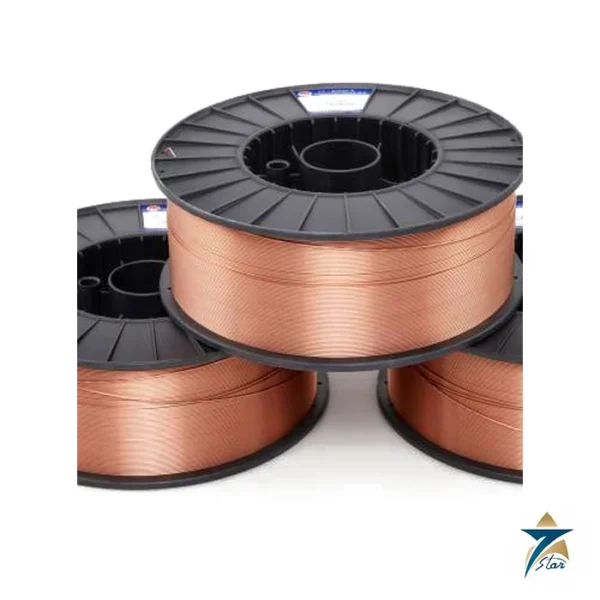
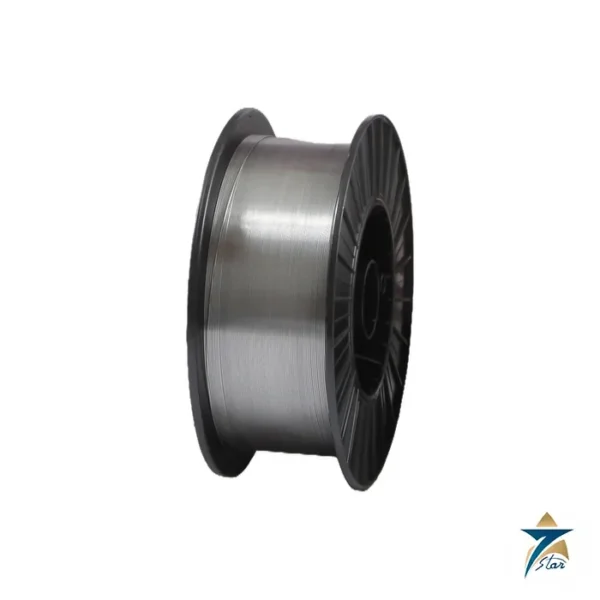
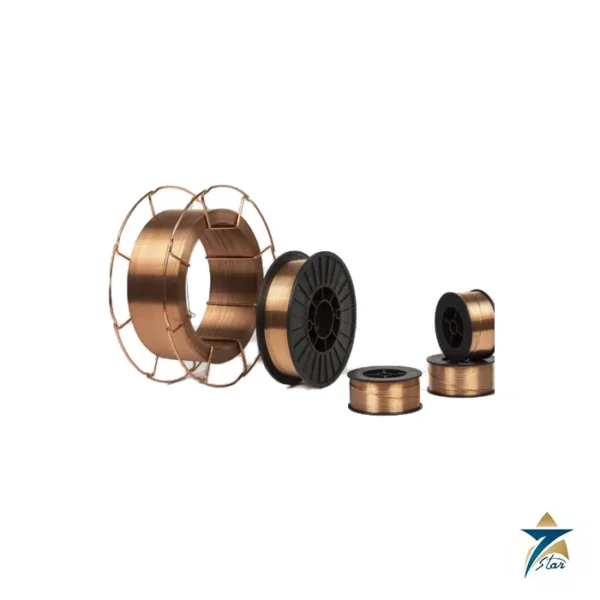
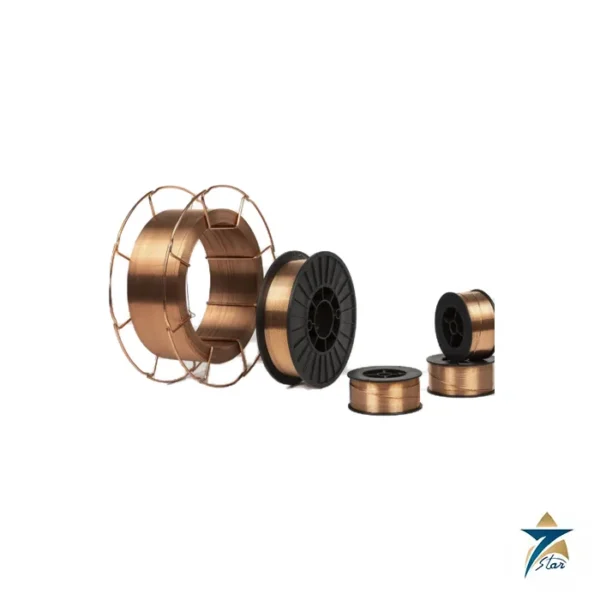
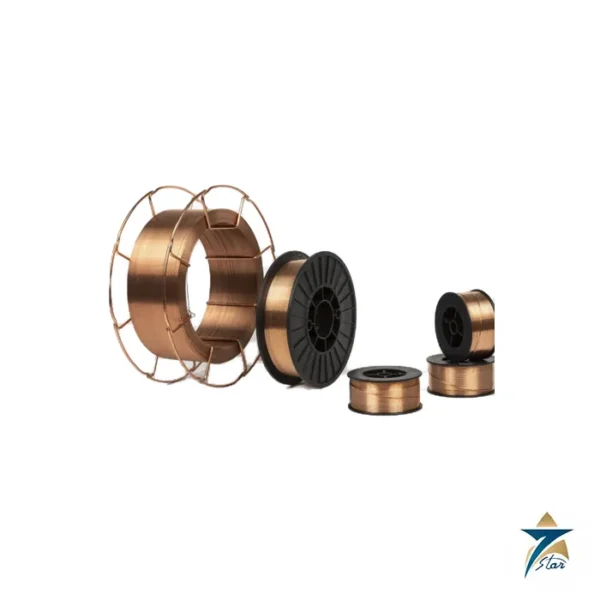
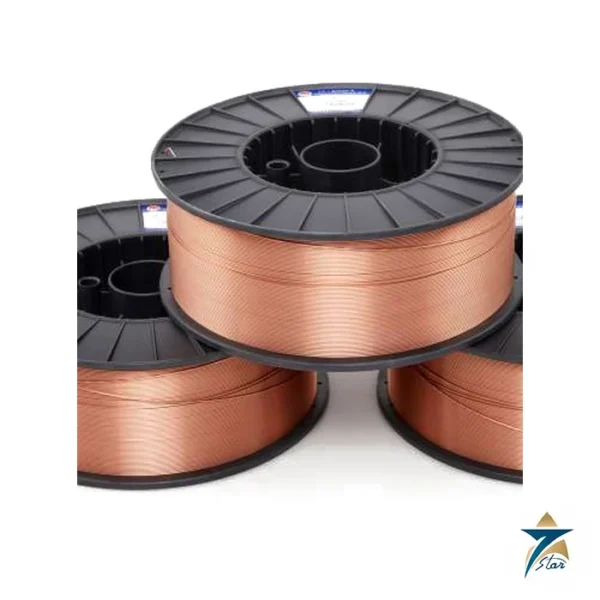
Lincoln Electric SuperArc L-59 is drawn from a controlled alloy rod and given a thin copper coating. The coating protects the surface during storage, lowers friction in the liner and conduit, and improves electrical contact in the tip, which the manufacturer links directly to long contact tip life. MicroGuard Ultra is the surface finish named in the datasheet for consistent feeding and arc stability, which matters most on long conduit runs and robotic torches where a small increase in friction becomes a feeding fault.
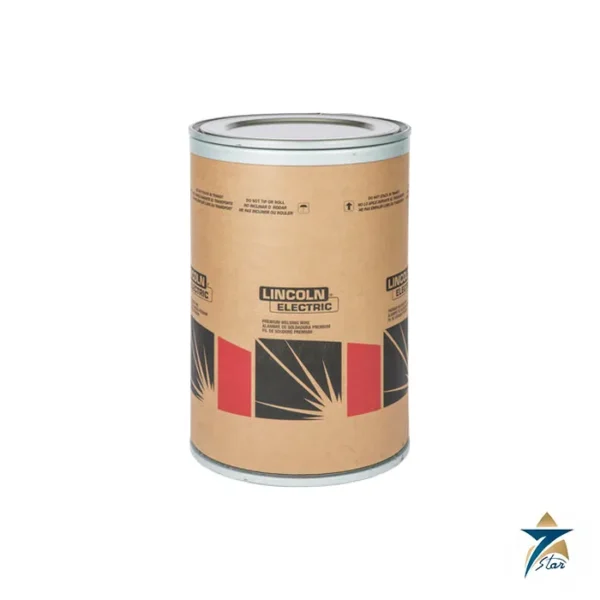
Lincoln Electric lists diameters of 0.035, 0.040, 0.045, 0.052 and 1/16 inch (0.9, 1.0, 1.1, 1.3 and 1.6 mm). The reference packages in the datasheet include 33 lb plastic spools, 44 lb fiber or steel spools, 60 lb fiber spools, 500 lb and 900 lb Accu-Pak boxes, Infinity-Pak containers, a 1000 lb Accu-Pak box and a 1000 lb Precise-Trak reel for high volume cells. These are the manufacturer reference packages, not a statement of Seven Star stock; please ask for current availability.
Key Features of Lincoln Electric SuperArc L-59
The following points are taken from the manufacturer datasheet and describe what Lincoln Electric SuperArc L-59 offers a welding shop:
- An engineered alloy system that enhances silicon island management on the finished bead, reducing the cleaning needed before painting or a following pass.
- Minimal spatter, which cuts grinding time and nozzle cleaning in production welding.
- A copper coating that supports long contact tip life and consistent current transfer.
- Fast travel speeds that suit thin to medium plate and high duty cycle automation.
- MicroGuard Ultra treatment that gives superior feeding and arc stability through long conduit.
- Suitability for all welding positions, with 100 percent CO2, argon and CO2 blends or argon and oxygen blends.
- Conformance to AWS A5.18 ER70S-6 and ASME SFA-A5.18, together with the classifications listed in the specification table.
- A wide range of reference packaging from 33 lb spools to 1000 lb bulk packs for different production volumes.
Industrial Applications in Oman and the GCC
For Lincoln Electric SuperArc L-59 the datasheet lists robotic or hard automation, automotive, pipeline and offshore work, pressure vessels, heavy fabrication and use as an alternative to metal cored wire. In Oman these map onto structural steel shops in Sohar and Rusayl, skid and piping fabrication yards supporting oil and gas projects, pressure vessel and tank workshops, and general engineering shops in Muscat and Salalah. The high deoxidiser content makes Lincoln Electric SuperArc L-59 a practical choice where plate arrives with light surface scale and where welders switch between short circuit transfer on thin sections and spray transfer on thicker joints.
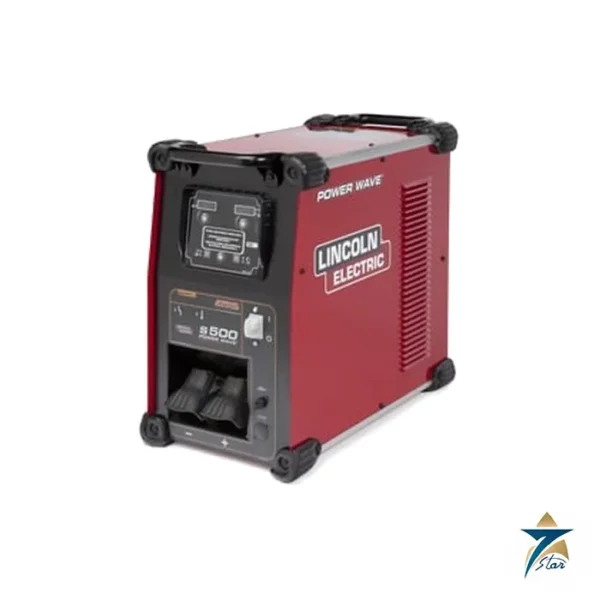
Seven Star LLC supplies Lincoln Electric SuperArc L-59 alongside other consumables and welding power sources, so a project team can align wire diameter, gas and machine settings in one enquiry. A multi-process inverter such as the Lincoln Electric Power Wave S500 can run solid wire in pulsed and synergic modes, while a compact unit such as the ESAB Rebel EMP 285ic suits site and maintenance work. For a mixed equipment order the Kobelco Lubricator Assembly page shows how Seven Star also supports industrial machinery spares.
Typical Settings Printed by the Manufacturer
The datasheet publishes operating procedures for each diameter with direct current electrode positive polarity. For 0.035 inch (0.9 mm) wire the listed settings run from 2.5 m/min wire feed speed at 17 V and about 80 A up to 15.2 m/min at 30 V and about 275 A, with a contact tip to work distance of 12 mm for short circuit procedures and 19 mm for spray procedures. Larger Lincoln Electric SuperArc L-59 diameters carry higher current for the same feed speed, and the sheet notes that for 100 percent CO2 short circuit procedures 1 to 2 volts should be added to the 75 percent argon values. Use these Lincoln Electric SuperArc L-59 figures as a starting point only and qualify the final procedure on your own material.
Technical Specifications of Lincoln Electric SuperArc L-59
The table below reproduces the key values printed in the Lincoln Electric SuperArc L-59 datasheet. Typical results are all weld metal values reported by the manufacturer and are not a guarantee for a particular application.
| Parameter |
Specification |
| Model |
Lincoln Electric SuperArc L-59 |
| Wire type |
Mild steel solid MIG wire, copper coated |
| AWS classification |
AWS A5.18/A5.18M ER70S-6; ASME SFA-A5.18 ER70S-6 |
| Other conformances listed |
ABS 3YSA (100 percent CO2 and mixed gas); DNV III YMS H5 (mixed gas); BV SA3YHHH (mixed gas); CWB/CSA W48-06 ER49S-6; EN ISO 14341-B G 49A 3 C S6 |
| Welding positions |
All |
| Shielding gas |
100 percent CO2; 75-95 percent Ar / balance CO2; 95-98 percent Ar / balance O2; flow 30-50 CFH |
| Diameters |
0.035, 0.040, 0.045, 0.052, 1/16 in (0.9, 1.0, 1.1, 1.3, 1.6 mm) |
| AWS requirement, 100 percent CO2 |
Yield 400 MPa (58 ksi) min; tensile 485 MPa (70 ksi) min; elongation 22 percent min; 27 J (20 ft-lbf) min at -29 C |
| Typical, 100 percent CO2 |
Yield 455 MPa (66 ksi); tensile 565 MPa (82 ksi); elongation 28 percent; 71 J (52 ft-lbf) at -29 C; 53 J (39 ft-lbf) at -40 C |
| Typical, 75 percent Ar / 25 percent CO2 |
Yield 485 MPa (70 ksi); tensile 595 MPa (86 ksi); elongation 25 percent; 56 J (41 ft-lbf) at -29 C; 53 J (39 ft-lbf) at -40 C |
| Typical, 90 percent Ar / 10 percent CO2 |
Yield 460 MPa (67 ksi); tensile 570 MPa (83 ksi); elongation 25 percent; 75 J (55 ft-lbf) at -29 C; 65 J (48 ft-lbf) at -40 C |
| Wire composition (AWS requirement) |
C 0.06-0.15; Mn 1.40-1.85; Si 0.80-1.15; S 0.035 max; P 0.025 max; Cu 0.50 max; Ni 0.15 max; Cr 0.15 max; Mo 0.15 max; V 0.03 max (percent) |
| Polarity |
DC electrode positive |
Handling and Storage Notes
Lincoln Electric SuperArc L-59 as a solid wire is far less moisture sensitive than a flux cored wire, but good practice still applies. Keep spools in their sealed packaging until needed, store them in a dry area away from direct contact with floors and wall condensation, and cover a spool on the feeder during long shutdowns to keep out dust and humidity. This is general welding practice, not a Lincoln Electric statement. In the coastal climate of Muscat and Sohar, wrapped spools returned to the store after a shift stay cleaner and feed more reliably.
How to Order
To order Lincoln Electric SuperArc L-59, send Seven Star LLC your diameter, package size, quantity and shielding gas, and our team in Muscat will prepare a formal quotation and confirm availability for delivery across Oman and the GCC. The manufacturer datasheet is attached to this page for download, and our engineers can help match the wire to your power source and procedure. Seven Star LLC supplies Lincoln Electric products as a trusted supplier with engineering support in Muscat, so contact the instrumentation and industrial supply division with your request today.
See also: Lincoln Electric Jet-LH 78 MR E7018 H4R Low Hydrogen Stick Electrode; Lincoln Electric Lincolnweld L-61 EM12K Submerged Arc Welding Wire.

 Automation & Control
 Electrical & Power
 Fittings & Valves
 Sensors & Transmitters
 Emergency Power
 Analyzer Systems
 Metering Systems
 Welding
 Fire & Gas Systems
 Motors, Pumps & Turbines
 Portable Test & Measurement
 Compressor & Cooling
 Bearings & Power Transmission
 Filtration
 Safety & PPE
 Material Handling & Lifting Equipment
 Non-Destructive Testing (NDT)
Reviews
There are no reviews yet.