
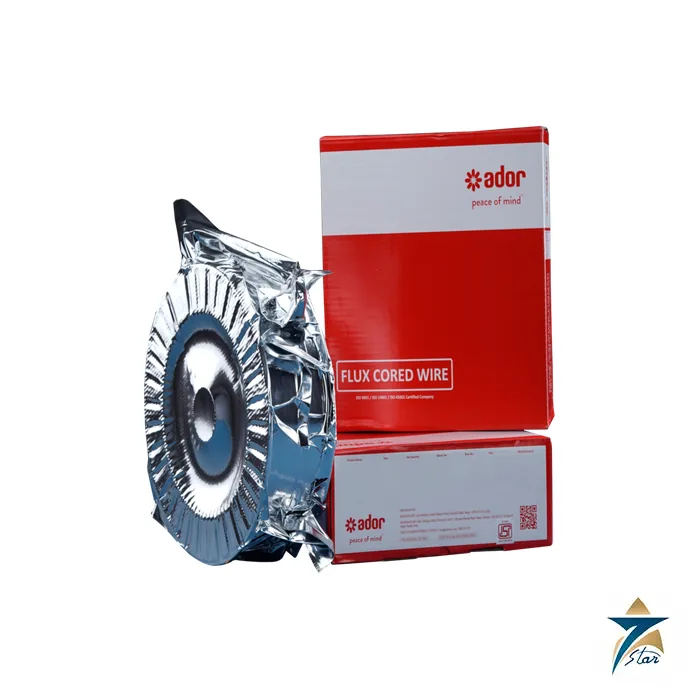
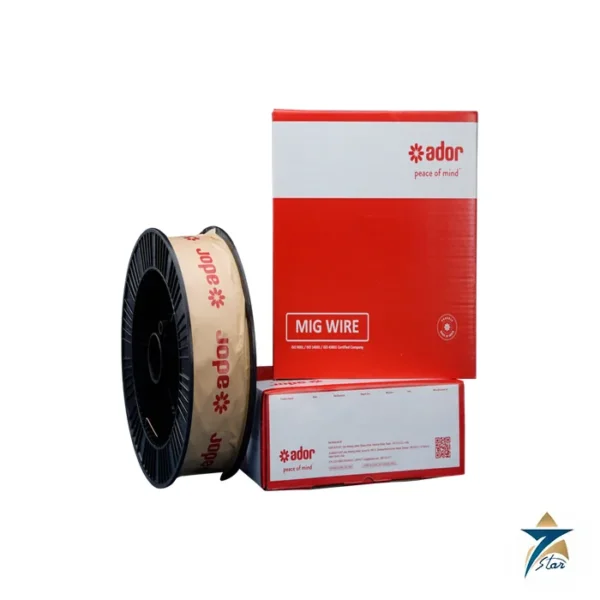
Ador Automig FC 91T1-B3 is a rutile type, gas shielded flux-cored wire from Ador Welding Limited that deposits chromium-molybdenum weld metal for creep resistant steels. It is classified to AWS A/SFA 5.29 E91T1-B3C and EN ISO 17634-A T CrMo2 P C1 2, and the official data sheet carries a CE approval. Ador states that the deposit resists creep and heat up to 600°C. The Ador Automig FC 91T1-B3 is aimed at contractors who need higher deposition and easier out-of-position fill on 2.25Cr-1Mo pipe and plate than solid wire or stick electrodes normally allow.
Seven Star LLC supplies the Ador Automig FC 91T1-B3 to boiler makers, refinery maintenance teams and pressure vessel fabricators in Oman and across the GCC. The manufacturer datasheet is attached for download, giving welding engineers the undiluted weld metal analysis, post weld heat treated tensile data and recommended operating conditions in one document.
In general terms, a flux-cored wire is a tube of metal filled with powdered flux and alloying elements. With rutile (titanium dioxide based) cores, the slag freezes quickly and supports the weld pool, which is why these wires are popular for positional welding. Shielding gas protects the arc while the slag system shapes the bead and carries away impurities. For a chrome-moly product the alloy additions in the core bring the deposit to the target composition; the Ador Automig FC 91T1-B3 has a typical undiluted weld metal analysis of 0.06 C, 1.0 Mn, 0.5 Si, 2.3 Cr and 1.0 Mo.
Ador highlights a stable and smooth arc, low fumes, minimal spatter, easy slag removal and a smooth weld bead. On site, those characteristics translate into less grinding between passes and fewer interruptions, which matters on large-diameter steam lines where fill time dominates the schedule. As with any 2.25Cr-1Mo filler, preheat, interpass temperature and PWHT should be set by the qualified procedure.
One general consideration with gas shielded flux-cored wires is the choice of gas. The 91T1-B3C designation indicates CO2 shielding, and Ador specifies CO2 for this wire. Using a different gas mixture than the one used in qualification can change arc behaviour, bead shape and weld metal chemistry, so the shielding gas should be treated as an essential element of the procedure and kept consistent between the test coupon and production welding.
The data sheet lists two wire diameters, 1.2 mm and 1.6 mm, each supplied as 15 kg net. Operation is on DCEP using CO2 shielding gas at 15 to 20 litres per minute. The wire is rated for all positions except vertical down, so vertical-up, horizontal and overhead fill and cap passes on fixed pipe joints are within its stated capability.
After post weld heat treatment at 690°C for one hour, Ador reports typical all weld metal values of 710 MPa ultimate tensile strength, 600 MPa yield at 0.2 percent offset and 19 percent elongation. These figures give the Ador Automig FC 91T1-B3 a tensile margin comparable to matching solid wire, while the rutile slag system adds the positional handling that solid wire lacks.
The features of the Ador Automig FC 91T1-B3 listed by Ador are summarised below.
Ador names main steam pipes of boilers in electric power plants and boiler super heaters, along with refineries, power plants, pressure vessels and boilers generally. The wire is intended for 2.25Cr-0.5Mo and 2.25Cr-1Mo creep resistant steels, Cr-Mo and Cr-Mo-V steels for high temperature applications, P5A materials, and ASTM A335 P22 and A387 Grade 22. In Oman this maps directly onto combined-cycle and steam plants serving the national grid and integrated water and power projects along the Batinah coast, where steam headers and superheater connections are fabricated in P22.
Refinery and petrochemical owners are the second group. Reactor effluent lines, heater outlet piping and pressure vessel nozzles in chrome-moly steels are common in Sohar and Duqm, and turnaround windows reward a filler that fills joints quickly in position. Seven Star LLC supplies the Ador Automig FC 91T1-B3 for these projects and can supply matching TIG and solid MIG consumables from the same Ador chemistry range for root passes and attachments.
Values are taken from the official Ador Automig FC 91T1-B3 data sheet; chemistry is typical undiluted weld metal.
| Parameter | Specification |
|---|---|
| Model | Ador Automig FC 91T1-B3 |
| Process | FCAW, gas shielded, low alloy steel for high temperature |
| AWS classification | A/SFA 5.29 E91T1-B3C |
| EN ISO classification | EN ISO 17634-A T CrMo2 P C1 2 |
| Approvals | CE |
| Flux type | Rutile |
| Typical weld metal chemistry, wt % | C 0.06, Mn 1.0, Si 0.5, Cr 2.3, Mo 1.0 |
| UTS (PWHT 690°C, 1 h) | 710 MPa |
| Yield strength 0.2% offset | 600 MPa |
| Elongation | 19 % |
| Diameters | 1.2 mm, 1.6 mm |
| Net weight | 15 kg |
| Polarity | DCEP |
| Positions | All positions except vertical down |
| Shielding gas | CO2, 15-20 L/min |
| Storage | Keep dry; follow box handling instructions |
A capable wire feeder and power source for flux-cored work is the Power Wave S500 from Lincoln Electric, or the portable Rebel EMP 285ic multi-process welder. For carbon steel shop seams by submerged arc, see the LongTeng EL8 wire. Our full range of flux-cored welding wire is also available.
For a quotation on the Ador Automig FC 91T1-B3, send Seven Star LLC the diameter, quantity of 15 kg units and delivery location in Oman or elsewhere in the GCC. Download the Ador Automig FC 91T1-B3 datasheet from this page for your welding procedure file, and contact our Muscat office if you want help comparing it with your existing chrome-moly consumables.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.







Reviews
There are no reviews yet.