
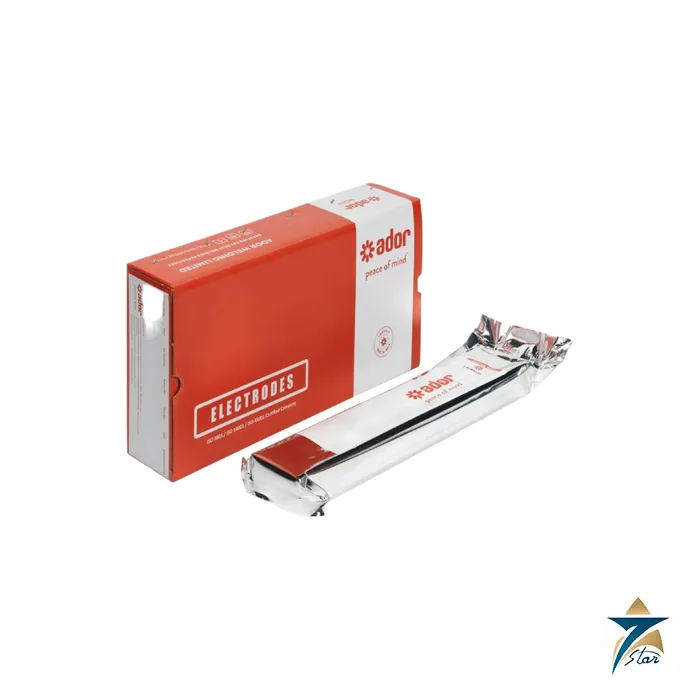
Ador Betanox 4462 is a duplex stainless steel stick electrode from Ador Welding Limited classified as AWS A/SFA 5.4 E2209-16, ISO 3581-A E 22 9 3 N L R 22 and IS 5206 E 22.9.3 LR23. It produces an austenitic-ferritic 22Cr-9Ni-3Mo-N weld deposit that Ador says offers an excellent combination of high strength and resistance to chloride-induced stress corrosion cracking and pitting. The official sheet prints IBR and CE approvals for this electrode, states a minimum PREN of 35 and gives a ferrite number specification of 30 to 55. The name reflects the 1.4462 material number used in Europe for standard 2205 duplex.
Seven Star LLC supplies the Ador Betanox 4462 to piping, structural and equipment fabricators in Oman and across the GCC. We provide the manufacturer datasheet as a download on this page, so procurement and QA teams can confirm classification, mechanical properties and redrying requirements against the job specification.
As general background, 2205 duplex stainless steel sits between austenitic 316L and super duplex in both cost and corrosion resistance. It offers higher strength than 316L and much better resistance to chloride stress corrosion cracking, which makes it attractive for pipelines, tanks and pressure vessels handling salty or sour process fluids. The weld needs a filler that restores the ferrite-austenite balance after the rapid cooling of an arc weld, and E2209 type consumables are enriched in nickel for that purpose.
The typical undiluted weld metal of the Ador Betanox 4462 contains 0.03 C, 0.9 Mn, 0.5 Si, 22.5 Cr, 8.9 Ni, 3.2 Mo and 0.15 N. Ador publishes a typical ferrite number of 32 within its 30 to 55 specification band. Controlled heat input, limited interpass temperature and clean joint preparation are the usual general precautions; the qualified WPS defines the real limits.
Another general point concerns dissimilar joints. Duplex filler of the 2209 type is frequently chosen when duplex stainless steel must be joined to carbon steel or to austenitic stainless, because its composition tolerates dilution from either side without forming a crack-sensitive structure. Where the Ador Betanox 4462 is used for such dissimilar welds, the procedure should still be qualified on the actual material combination, and the designer should consider the different thermal expansion of the two base metals.
The electrode has a rutile type, non-synthetic coating and is suitable for all positions, with Ador listing all positions except vertical down in the parameter table. It operates on DCEP. Three sizes are offered, each 350 mm long: 2.5 mm at 50 to 75 A, 3.15 mm at 80 to 100 A and 4.0 mm at 110 to 140 A. The deposit gives uniform and fine ripples and radiographic quality welds, and Ador states the product can be applied for operating temperatures up to 200°C.
Typical as-welded all weld metal values are 735 MPa ultimate tensile strength, 25 percent elongation and 50 J Charpy impact at minus 40°C, against specification minimums of 690 MPa, 20 percent and 47 J. Redrying is specified at 250 to 300°C for at least one hour, and standard packing is a 10 kg box with five 2 kg cartons.
The small 2 kg inner cartons are practical in the humid coastal conditions found in much of Oman, since only the electrodes needed for a shift have to be opened and redried. Keeping unopened Ador Betanox 4462 cartons in a dry store and returning unused electrodes to a holding oven are good general practices that help avoid moisture-related porosity in duplex welds.
Features of the Ador Betanox 4462 as listed by the manufacturer are given below.
Ador lists welding of 2205 and 2209 type duplex stainless steels and similar compositions, pipelines carrying chloride-bearing products and sour gases, cladding on carbon and low alloy steels, cast pumps, valve bodies and sea water handling equipment, chemical equipment, heat exchangers and offshore platforms, as well as materials 1.4417, 1.4460, 1.4462, 1.4362 and 1.4162. In Oman, 2205 duplex is common in gas gathering and sour service flowlines in the interior, in chemical storage and process tanks at Sohar, and in cooling water and brine handling systems at coastal utilities. Repair crews working on these assets value an electrode that can be carried to the joint and run without wire feeders or gas cylinders.
The ability to clad carbon steel is also useful, for example when buttering a carbon steel nozzle before welding it to a duplex line. Seven Star LLC supplies the Ador Betanox 4462 for these projects; Ador lists Miginox 2209, Tiginox 2209, Miginox FC 2209 and Subinox 2209 with Automelt S33 flux as the matching consumables for MIG, TIG, flux-cored and submerged arc welding respectively.
All values for the Ador Betanox 4462 below are from the official manufacturer data sheet.
| Parameter | Specification |
|---|---|
| Model | Ador Betanox 4462 |
| Process | SMAW (MMA), duplex stainless steel |
| AWS classification | A/SFA 5.4 E2209-16 |
| ISO classification | ISO 3581-A E 22 9 3 N L R 22 |
| IS classification | IS 5206 E 22.9.3 LR23 |
| Approvals | IBR, CE |
| Typical weld metal, wt % | C 0.03, Mn 0.9, Si 0.5, Cr 22.5, Ni 8.9, Mo 3.2, N 0.15 |
| UTS, as welded | 735 MPa typical (690 min) |
| Elongation | 25 % typical (20 min) |
| CVN impact at -40°C | 50 J typical (47 min) |
| Ferrite number | 32 typical (30-55) |
| PREN | 35 min |
| Sizes and current | 2.5 x 350 mm 50-75 A; 3.15 x 350 mm 80-100 A; 4.0 x 350 mm 110-140 A |
| Polarity | DCEP |
| Redrying | 250-300°C, minimum 1 hour |
| Packing | 10 kg box of 5 cartons x 2 kg |
Stick welding in the field can be done with the Rebel EMP 285ic from ESAB. For carbon steel MIG fabrication we list Lincoln Electric L-59 wire, and for tank and vessel seams the EL8 submerged arc wire from LongTeng. All our welding electrodes are listed in one category.
Send Seven Star LLC your required Ador Betanox 4462 diameters, quantity in 10 kg boxes and delivery point in Oman or the GCC for a formal quotation. The Ador Betanox 4462 datasheet can be downloaded here for your procedure file, and our team in Muscat is available to discuss duplex procedures and matching wires for other welding processes.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.