
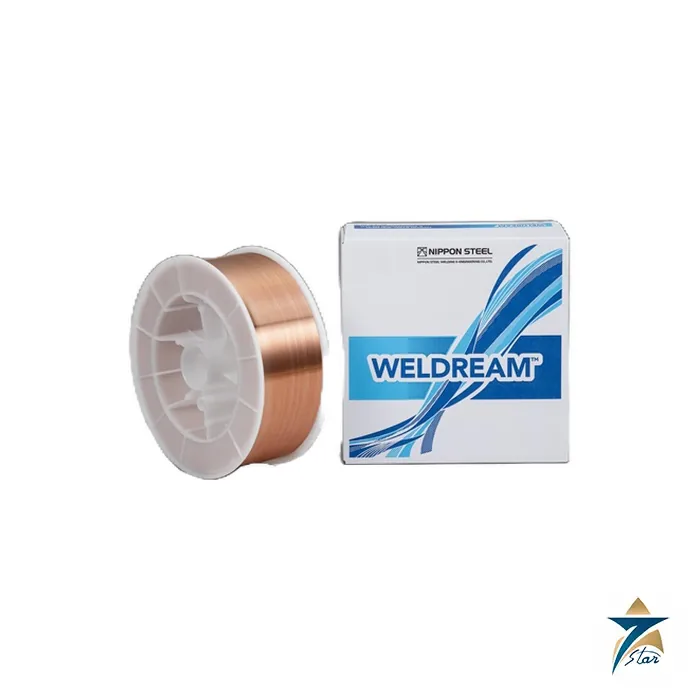
The Nippon Steel SF-1 is a rutile-type seamless flux-cored wire for gas-shielded arc welding with CO2. It is classified AWS A5.20 E71T-1C-H4 and JIS Z 3313 T49J0T1-1CA-UH5, and is intended for mild steel and 490 MPa high tensile strength steel.
Because the tube has no seam, Nippon Steel Welding & Engineering states that the diffusible hydrogen content is as low as that of solid wire, which gives the weld metal excellent crack resistance. The manufacturer describes a stable arc, little spatter, a smooth bead covered evenly by easily removable slag, low fume, a high deposition rate and all-position welding at almost the same current. Listed applications include machinery, structures, steel frames, ships, bridges, towers, chemical apparatus and rolling stock.
| Parameter | Specification |
|---|---|
| Manufacturer / product | Nippon Steel Welding & Engineering / SF-1 |
| Process | FCAW, gas-shielded, seamless rutile flux-cored wire |
| AWS classification | A5.20 E71T-1C-H4 |
| JIS classification | Z 3313 T49J0T1-1CA-UH5 |
| Shielding gas | CO2, 20–25 L/min |
| Polarity | DC (+) |
| Typical weld metal, % | C 0.06, Si 0.50, Mn 1.40, P 0.015, S 0.010 |
| Typical mechanical properties | YS 520 MPa, TS 580 MPa, El. 28%, Charpy 91 J at 0 °C |
| Current, 1.0 mm | Flat 150–260 A; V-up 150–200 A; V-down 160–220 A; overhead 150–240 A |
| Current, 1.2 mm | Flat 180–320 A; V-up 180–260 A; V-down 200–280 A; overhead 180–260 A |
| Current, 1.4 mm | Flat 200–410 A; V-up 180–260 A; V-down 220–300 A; overhead 180–260 A |
| Current, 1.6 mm | Flat 220–450 A; horizontal 220–400 A; V-up 200–280 A |
| Contact tip to work distance | 20–30 mm |
The handbook gives practical usage guidelines. Any welding machine for solid wire can be used, but the pressure of the wire feed rolls should be set a little looser. The arc voltage should be 1 or 2 volts lower than for conventional flux-cored wires and 4 or 5 volts lower than for solid wire. Keep the distance between the base metal and the contact tip within 20–30 mm, and use a gas flow of 20–25 L/min.
For one-side welding, the manufacturer recommends the SB-41 backing material. The 1.6 mm size is not listed for vertical-down or overhead welding, so choose 1.2 mm or 1.4 mm when the work includes those positions.
SF-1 is published for CO2 shielding. If your procedure uses an argon-CO2 mixture, confirm the classification and properties with the manufacturer before qualifying it. The product page lists classification society certificates from NK, ABS, LR, DNV and BV; not all sizes are certified, so ask for the certificate covering your diameter.
A note on the classification marks: the manufacturer flags the AWS A5.20 E71T-1C-H4 designation with a symbol meaning that the product meets the classification requirements, but that the classification has not been certified by a third party under the JIS Mark system or by AWS. Where a project specification requires third-party certification, use the classification society approvals instead. In the current table, the horizontal fillet range is the same as the flat range for every diameter from 1.0 to 1.6 mm, which keeps set-up simple when a joint moves between flat and fillet work.
The Nippon Steel SF-1 handbook page is attached to this page. Browse our Flux-Cored Welding Wire category for other cored wires.
For a quotation, send the diameter, spool type and weight, quantity and any approval or mill certificate requirement.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.











Reviews
There are no reviews yet.