- Automation & ControlView all 1,924 products
- AC Drives
- PLC & I/O Cards
- Industrial Communications
- Vibration Monitoring
- Automation Accessories
- Controllers & Data Acquisition
- Isolator & Barrier
- CCTV & Security
- Safety Switches & Guard Locking
- Encoders
- HMI Displays
- Industrial Computers
- Motor Soft Starters
- Servo Drives
- Pneumatic Cylinders
- Machine Vision
- Automation Software
- Robotics
Brand: Böhler Welding
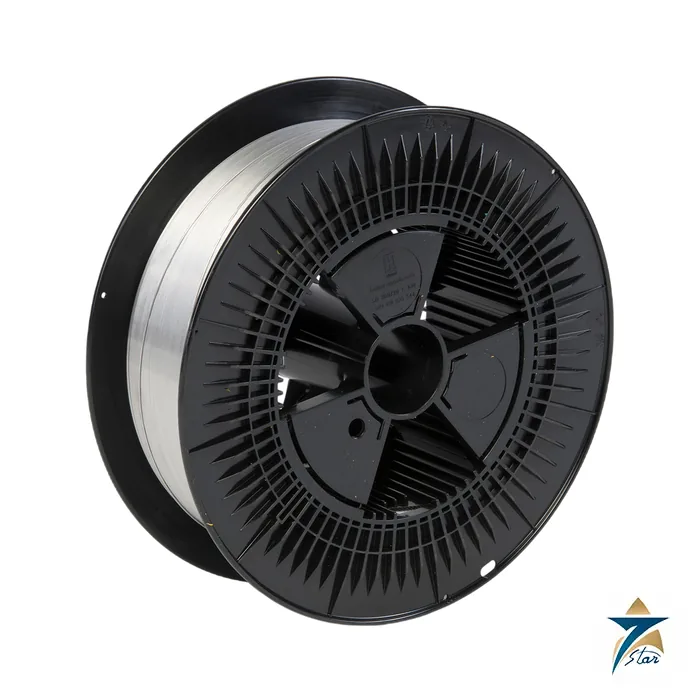
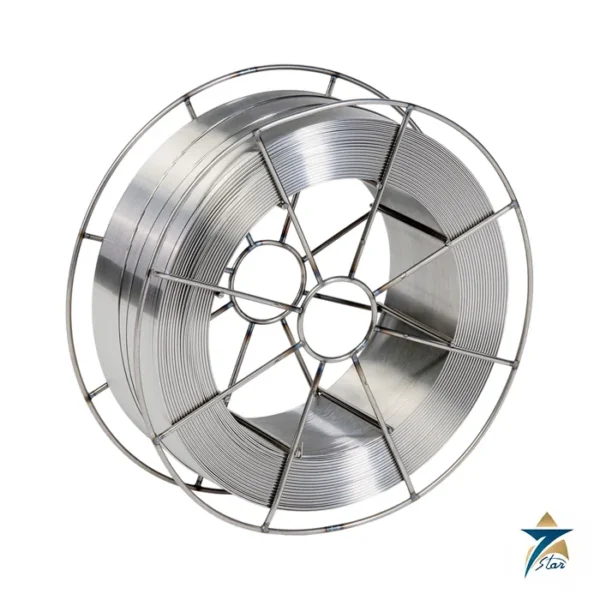
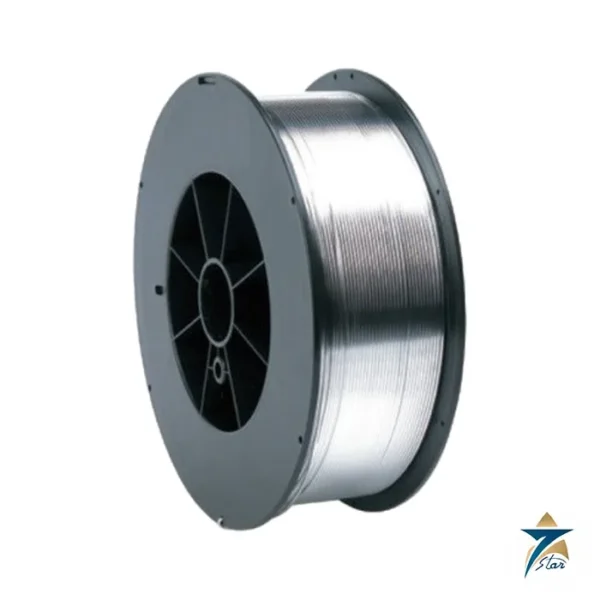
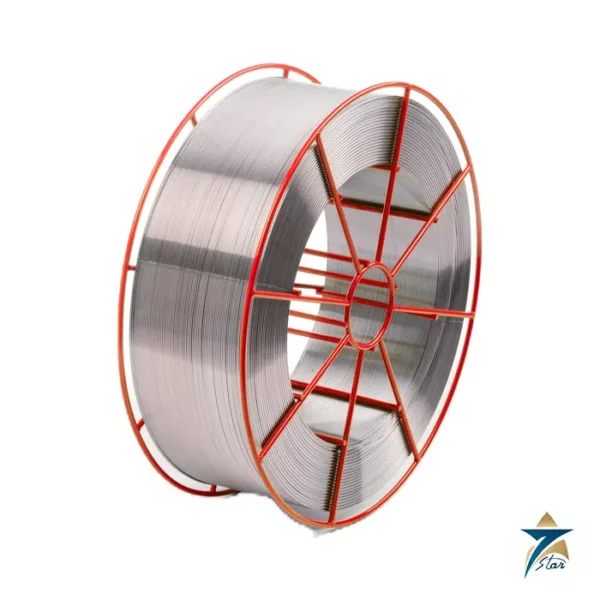
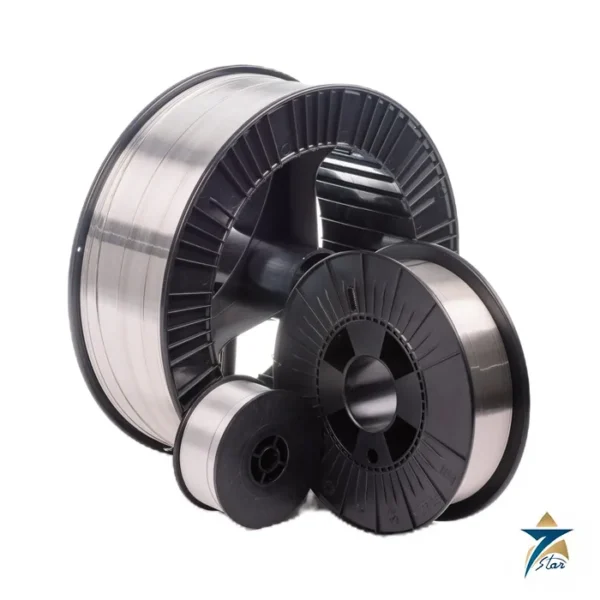
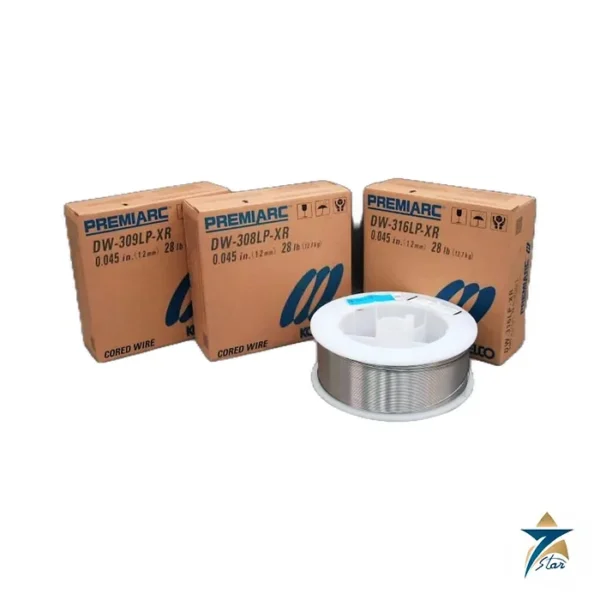
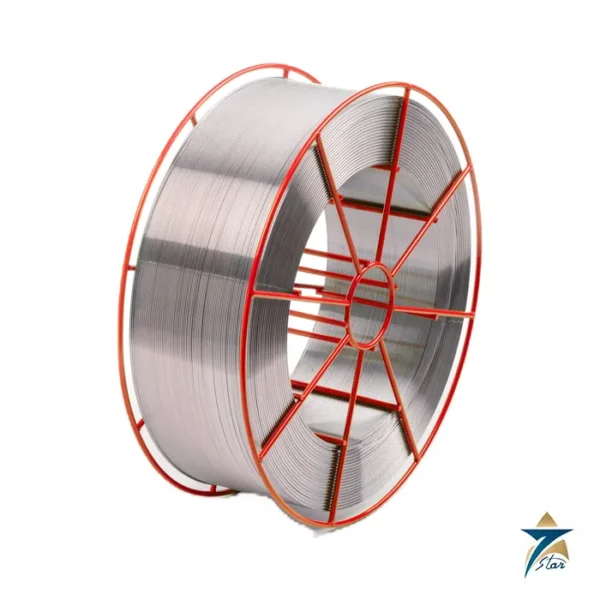
Böhler FOXcore 309L-T1 E309LT1-4 Dissimilar Flux-Cored Wire
Description
Rutile 309L flux-cored wire for buffer layers and dissimilar joints
The Böhler FOXcore 309L-T1 is a rutile flux-cored wire of type E309LT1 / T 23 12 L P, classified AWS A5.22 E309LT1-4(1). Böhler Welding states that it is primarily intended for surfacing low-alloyed steels and for dissimilar welds between mild steel and CrNi stainless steels. Ferrite measured with a FeritScope is 14 to 22 FN. Corrosion resistance is superior to E308L / T 19 9 L fillers, and when used for overlay welding on mild steel a corrosion resistance equivalent to that of 1.4301 / 304 is obtained in the first layer. The wire can be used in all positions without changing parameters, with a fast-freezing rutile slag, excellent vertical-up and overhead weldability, very good slag detachability and almost no spatter.
Technical specifications
| Parameter | Specification |
|---|---|
| AWS classification | A5.22 / SFA-5.22 E309LT1-4(1) |
| EN ISO 17633-A / -B | T 23 12 L P M21 (C1) 1 / TS 309L-F M21 (C1) 1 |
| Deposit analysis, wt % | C 0.03; Si 0.7; Mn 1.4; Cr 23.0; Ni 12.5; ferrite 12 to 23 FN |
| Yield (Rp0.2), as welded | 61 ksi typical (minimum 46) |
| Tensile (Rm), as welded | 78 ksi typical (minimum 75) |
| Elongation (L0=5d0) | 36 % typical (minimum 30) |
| Impact energy | 44 ft-lbf at 68 °F; 41 at 0 °F; 37 at -70 °F (minimum 24) |
| Hardness | 210 HB |
| Service temperature | -75 °F to 570 °F; scaling temperature about 1830 °F in air |
| Diameters | 0.035 in; 0.045 in; 1/16 in |
| Gas and polarity | Ar plus 15 to 25 % CO2; 100 % CO2 with about 2 V more; outdoor gas flow 30 to 50 scfh; DC+ |
| Heat input and stick-out | Maximum 50 kJ/in; stick-out 5/8 to 3/4 in |
| Approvals | TÜV (09115), DB (43.014.22), DNV GL, LR, RINA (M21), BV |
Dissimilar welds and buffer layers
The data sheet describes use for surfacing (buffer layers) on unalloyed or low-alloyed steels and for joining non-molybdenum-alloyed stainless steels to carbon steels, as well as joints between austenitic steels, austenitic and ferritic heat-resistant steels with ferritic steels, pressure boiler steels, fine-grained structural steels and shipbuilding steels. Slight weaving is recommended for dissimilar welding in all positions. For constructions that include low-alloyed steels, a stress-relieving annealing stage may be advisable, and Böhler advises always consulting the parent material supplier on heat treatment. The TIG equivalent is the
rod; for 316L top layers see the .| Related Böhler Welding cored wire | Classification | Typical use |
|---|---|---|
| FOXcore 71 RC | AWS A5.20 E71T-1 family | All-position rutile wire for mild steel, 0.045 to 1/16 in. |
| FOXcore 316L-T1 | AWS A5.22 E316LT1-4(1) | 316L stainless, all positions |
| FOXcore 2209-T1 | AWS A5.22 E2209T1-4(1) | 2205 duplex, all positions |
Ordering notes for dissimilar work
State in the enquiry whether the wire will be used for a buffer layer or a dissimilar joint, the base materials on both sides, the ferrite range required by the specification, the shielding gas and the spool format. Preheat and interpass temperatures follow the base metal, and the certificate type should be named with the order.
Documents and quotation
You can download the FOXcore 309L-T1 data sheet from this page to check each value against your procedure. Browse flux-cored welding wire for neighbouring items. To request a price, tell us the diameter, how it should be packed, how much you need, the parent metal and any certificate wording.
Datasheets & Documents
- Datasheet Böhler Welding FOXcore 309L-T1 product data sheet (US edition) Download
Reviews (0)
How would you rate this product? Cancel reply
About brand
Böhler Welding is the welding consumables and equipment brand of voestalpine Böhler Welding, part of the Austrian steel and technology group voestalpine. Its roots go back to 1870, when the brothers Albert and Emil Böhler founded the Böhler company in Vienna; in 1894 they bought the steel works in Kapfenberg, Styria, which became the home of Böhler special steels and, later, Böhler welding filler metals. Welding became a separate division of the newly formed Böhler-Uddeholm group in 1991. voestalpine took over Böhler-Uddeholm in 2007, and the welding business, headquartered in Düsseldorf, Germany, has been part of voestalpine's Metal Engineering Division since 2013.
Böhler Welding company profile
| Origins | 1870, Vienna, Austria: Albert and Emil Böhler found the Böhler company; Kapfenberg steel works acquired in 1894 |
|---|---|
| Welding business | Separate division of Böhler-Uddeholm from 1991 (the same year it acquired UTP) |
| Ownership | voestalpine AG (Linz, Austria), which took over Böhler-Uddeholm in 2007; welding integrated into the Metal Engineering Division in 2013 |
| Headquarters | Düsseldorf, Germany (voestalpine Böhler Welding); Austrian company seated in Kapfenberg |
| Brands in the group | Böhler Welding (joining consumables and welding machines), UTP Maintenance (repair and hardfacing), Fontargen Brazing; product lines such as FOX, Thermanit, Union, diamondspark, FOXcore, Marathon and UV fluxes |
| Product families | Stick electrodes, TIG rods, MIG/MAG solid wires, flux-cored and metal-cored wires, submerged arc wires and fluxes, welding machines and plasma cutters |
Milestones
- 1870: Albert and Emil Böhler found the company in Vienna.
- 1894: The Kapfenberg cast steel works is purchased.
- 1991: Böhler Welding becomes a separate division of Böhler-Uddeholm and acquires UTP.
- 2007: voestalpine makes its takeover offer for Böhler-Uddeholm.
- 2013: The welding business is integrated into voestalpine's Metal Engineering Division as voestalpine Böhler Welding.
Choosing Böhler welding consumables
The filler metal must match the base metal and the service. Carbon steel pipe is often welded with a cellulosic root (FOX CEL+, AWS E6010) because it penetrates well in vertical-down welding, followed by low-hydrogen fill and cap passes (FOX EV 50, E7018-1, or FOX BVD vertical-down electrodes). Creep-resistant chromium-molybdenum steels need matching consumables and controlled preheat and post-weld heat treatment: for example FOX DCMS Kb (E8018-B2) for 1.25Cr-0.5Mo, FOX CM 2 Kb (E9018-B3) for 2.25Cr-1Mo and Thermanit Chromo 9 V Mod for P91. Duplex stainless steel uses an over-alloyed 2209 filler (FOX CN 22/9 N-B, Thermanit 22/09) to keep the ferrite-austenite balance. Low-hydrogen electrodes must be stored dry and re-baked according to the data sheet.
Where Böhler Welding products are used
In Oman and the GCC, Böhler consumables are used on cross-country pipelines, oil and gas facilities, refineries and petrochemical plants, power and desalination plants with P91 and Cr-Mo piping, pressure vessel and tank fabrication, and structural steel work.
Böhler Welding products we list
| Family | Examples |
|---|---|
| Stick electrodes | FOX CEL+ E6010, FOX EV 50, FOX EV PIPE, FOX BVD 85, FOX DCMS Kb, FOX CM 2 Kb, FOX CN 22/9 N-B, Thermanit Chromo 9 V Mod |
| TIG rods | EMK 6, Union ER 80S-B2, Union ER 90S-B3, Thermanit GE-316L, Thermanit 22/09, Thermanit 309L |
| Flux-cored and metal-cored wires | FOXcore 71 RC, diamondspark 52 RC, diamondspark X70 RC-Pipe, FOXcore 316L-T1, FOXcore 2209-T1 |
| Submerged arc wires and fluxes | Union S 2 Si, Union S 3 Si, Union S 1 CrMo 2, Thermanit MTS 3 LNi, UV 418 TT, Marathon 543 |
| Welding and cutting machines | TERRA 500 RC, TERRA NX 400 TLH, TERRA NX 500 PME, SABER 70 CHP |
Ordering Böhler Welding products: what we need
Send the product name and AWS or EN classification (for example FOX EV 50, AWS A5.1 E7018-1), the diameter and the quantity in kg. For project work, tell us the base material, welding process and any certificate needed, such as an EN 10204 3.1 inspection certificate.
Facts checked against voestalpine's published company histories, October 2026.
Browse Böhler Welding products by category: Welding Electrodes, TIG Welding Wire, Flux-Cored Welding Wire, Submerged Arc Welding Wire, Submerged Arc Fluxes, Cellulosic Pipeline Electrodes.
FAQ
Questions about the Böhler FOXcore 309L-T1 E309LT1-4 Dissimilar
Answers from our engineering team on installation, compatibility and integration.
01What is the classification of FOXcore 309L-T1?
AWS A5.22 E309LT1-4(1) and EN ISO 17633-A T 23 12 L P M21 (C1) 1.
02What is it mainly used for?
Surfacing low-alloyed steels and dissimilar welds between mild steel and CrNi stainless steels.
03What ferrite level is given?
14 to 22 FN measured with a FeritScope MP30; typical analysis lists 12 to 23 FN.
04Which diameters are listed?
0.035, 0.045 and 1/16 inch.
05Which approvals are printed?
TÜV (09115), DB (43.014.22), DNV GL, LR, RINA (M21) and BV.


Reviews
There are no reviews yet.