
Kobelco DW-50 Rutile Flux-Cored Welding Wire for Carbon Steel
Overview
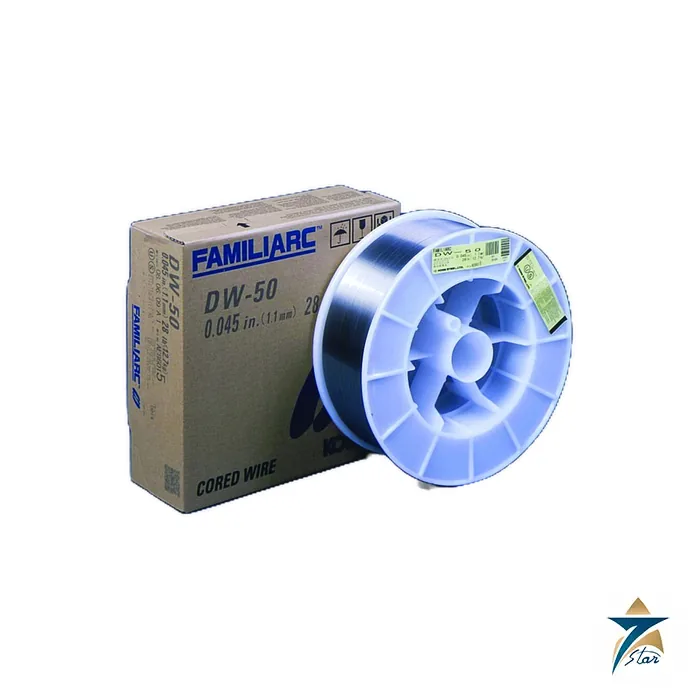
Kobelco DW-50 is a rutile flux-cored wire for gas-shielded welding of carbon steel, sold in the FAMILIARC range of Kobelco. The manufacturer brochure describes it as a general use wire that also suits seismic applications, classified AWS A5.20 E71T-1C/M H8 and E71T-9C/M H8, with the Canadian equivalent CWB W48-18 E491T-9C/9M-H8 and the European designation EN ISO 17632-A T42 2 P C/M 1 H5. The slag of Kobelco DW-50 freezes fast and gives excellent weldability in horizontal, vertical and overhead positions, and the brochure notes a low fume emission formula that helps keep the welding environment cleaner.
Seven Star LLC supplies Kobelco DW-50 to fabricators, shipyards and structural steel contractors in the Sultanate of Oman and the GCC. Our Muscat team can send the manufacturer datasheet, help select diameters and shielding gas, and review the machine settings needed to run this wire productively.
How a Rutile Flux-Cored Wire Behaves
A rutile flux-cored wire has a tubular steel sheath filled with titanium dioxide based flux and alloying powders. In the arc, the flux creates a fast freezing slag that supports the weld pool in vertical and overhead positions, produces a smooth bead surface and lets welders run higher currents out of position than a solid wire permits. The gas shield, either 100 percent CO2 or a 75 percent argon and 25 percent CO2 mixture, provides most of the protection against air. The two gases give slightly different results: pure CO2 gives deeper penetration and a hotter arc, and the argon mixture yields a softer arc with less spatter and higher strength in the all weld metal.
The manufacturer states that Kobelco DW-50 can be used with either gas and has a wide welding parameter range, which makes it versatile. The brochure shows a bead appearance example of 0.045 inch wire welded vertical upward at 64 kJ per inch heat input with mixed gas, which demonstrates the slag control on a demanding joint.
Engineering Design of the Kobelco DW-50 Wire
Kobelco DW-50 is supplied in diameters of 0.045 inch (1.1 mm), 0.052 inch (1.3 mm) and 1/16 inch (1.6 mm), with a listed wire stick-out of 3/4 inch at lower settings and 1 inch at the highest settings on the 0.052 inch and 1/16 inch sizes. The brochure includes a table of wire feed speed, current, arc voltage for both gases and deposition rate for each size, which welding engineers can use to set up a procedure quickly.
Of particular interest to structural fabricators, Kobelco DW-50 now carries AWS D1.8 approval, making it a strong choice for seismic applications in the structural steel industry. The approvals listed on the brochure are ABS, CWB, LR, DNV-GL and AWS D1.8.
Key Features of Kobelco DW-50
These points come from the manufacturer brochure for Kobelco DW-50:
- A fast freezing slag formula that gives excellent weldability in horizontal, vertical and overhead positions.
- Use with 100 percent CO2 or 75 percent argon and 25 percent CO2 shielding gas.
- A wide welding parameter range that makes the wire versatile for different thicknesses.
- A low fume emission formula that creates a cleaner welding environment.
- AWS D1.8 approval for seismic applications in structural steel.
- Classification AWS A5.20 E71T-1C/M H8 and E71T-9C/M H8, CWB W48-18 E491T-9C/9M-H8 and EN ISO 17632-A T42 2 P C/M 1 H5.
- Typical diffusible hydrogen content of 4.7 mL per 100 g according to AWS A4.3.
- Typical all weld metal tensile strength of 84 ksi with 100 percent CO2 and 95 ksi with the argon mixture.
Industrial Applications in Oman and the GCC
A general use rutile wire with seismic approval such as Kobelco DW-50 suits a broad range of work: structural steel for industrial buildings, platforms and pipe racks, plate fabrication for storage tanks and process skids, shipbuilding and ship repair, and heavy equipment frames. In Oman these include fabrication shops at Sohar, Rusayl and Duqm, as well as project yards supporting gas, power and water developments, where a productive flux-cored wire shortens fabrication schedules compared with stick welding.
Seven Star LLC supplies Kobelco DW-50 together with welding machines and spares. The Lincoln Electric Power Wave S500 and the ESAB Rebel EMP 285ic are examples of power sources in our catalogue that can run flux-cored wire, and our team also lists items such as the Kobelco Lubricator Assembly for plant owners who deal with Kobelco equipment.
Technical Specifications of Kobelco DW-50
The tables below reproduce values printed in the Kobelco DW-50 brochure. They are typical values and are not guarantees for a specific application.
| Parameter | Specification |
|---|---|
| Model | Kobelco DW-50 (FAMILIARC) |
| Wire type | Rutile flux-cored wire for carbon steel, general use including seismic application |
| Classification | AWS A5.20 E71T-1C/M H8, 9C/M H8; CWB W48-18 E491T-9C/9M-H8; EN ISO 17632-A T42 2 P C/M 1 H5 |
| Shielding gas | 100 percent CO2 or 75 percent Ar / 25 percent CO2 |
| Approvals listed | ABS, CWB, LR, DNV-GL, AWS D1.8 |
| Diffusible hydrogen | 4.7 mL/100 g (AWS A4.3) |
| Typical, AWS A5.20, 100 percent CO2 | 0.2 percent proof stress 74 ksi; tensile 84 ksi; elongation 31 percent; 58 ft-lbs at -20 F; 79 ft-lbs at 0 F |
| Typical, AWS A5.20, 75 percent Ar / 25 percent CO2 | 0.2 percent proof stress 81 ksi; tensile 95 ksi; elongation 27 percent; 50 ft-lbs at -40 F; 76 ft-lbs at -4 F |
| AWS D1.8 results listed | Low heat input 30 kJ/in: 83 ksi proof stress, 91 ksi tensile, 27 percent elongation, 103 ft-lbs at +70 F; high heat input 74 kJ/in: 66 ksi, 79 ksi, 26 percent, 94 ft-lbs at +70 F |
| Deposit chemistry, 100 percent CO2 | C 0.04; Si 0.67; Mn 1.29; P 0.011; S 0.008 (percent) |
| Deposit chemistry, 75/25 Ar/CO2 | C 0.05; Si 0.81; Mn 1.54; P 0.011; S 0.008 (percent) |
| Sizes | 0.045, 0.052, 1/16 in (1.1, 1.3, 1.6 mm) |
Recommended Conditions Listed in the Brochure
The brochure gives recommended wire feed speed, current, voltage and deposition rate. For 0.045 inch wire, a feed speed of 140 in/min corresponds to 120 A, 23 to 26 V with CO2 or 21 to 24 V with the argon mixture and a deposition rate of 4.0 lb/hr, rising to 400 in/min, 250 A and 10.5 lb/hr at 28 to 30 V with CO2. For 0.052 inch wire the listed range runs from 120 in/min at 140 A and 3.5 lb/hr to 395 in/min at 300 A and 11.5 lb/hr. For 1/16 inch wire it runs from 100 in/min at 180 A and 4.5 lb/hr up to 250 in/min at 300 A and 10.0 lb/hr. Use these figures only as a starting point and qualify the procedure on your own material.
Handling and Storage
As with all flux-cored wires, keep Kobelco DW-50 in its sealed packaging until needed, store it in a dry room and cover partly used spools on the feeder when work stops. Moisture in the core raises hydrogen and porosity risk, and the humid coastal climate in Muscat makes good storage discipline important. This is general welding guidance, not a Kobelco warranty statement.
Call To Action
To request Kobelco DW-50, send Seven Star LLC the diameter, spool size, quantity and delivery location, and our Muscat team will prepare a formal quotation and confirm availability across Oman and the GCC. The manufacturer brochure is attached to this page as a datasheet. Seven Star LLC supplies Kobelco products on request with engineering support in Muscat, so contact us with your enquiry today.
- Datasheet Kobelco DW-50 datasheet (manufacturer brochure) Download
Browse Kobelco products by category: Compressor.
Related products


Reviews
There are no reviews yet.