All-position rutile cored wire for CO2 welding of 490 MPa steel
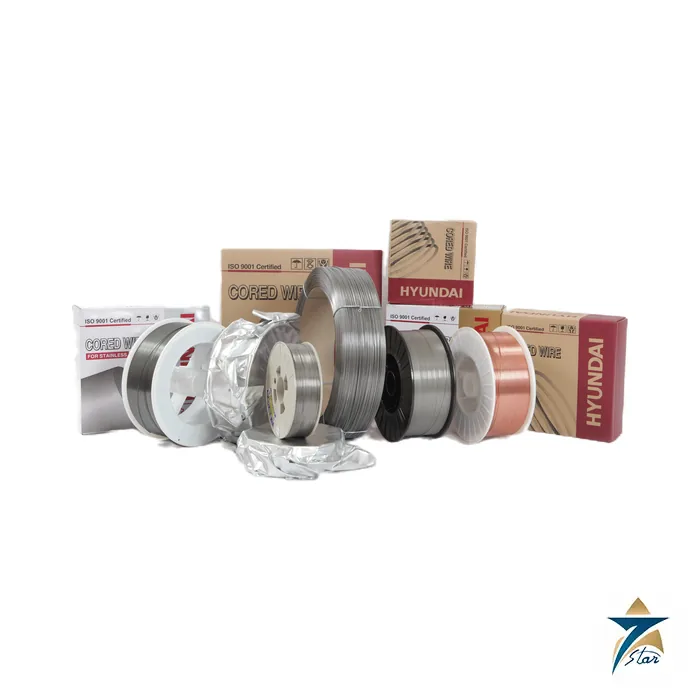
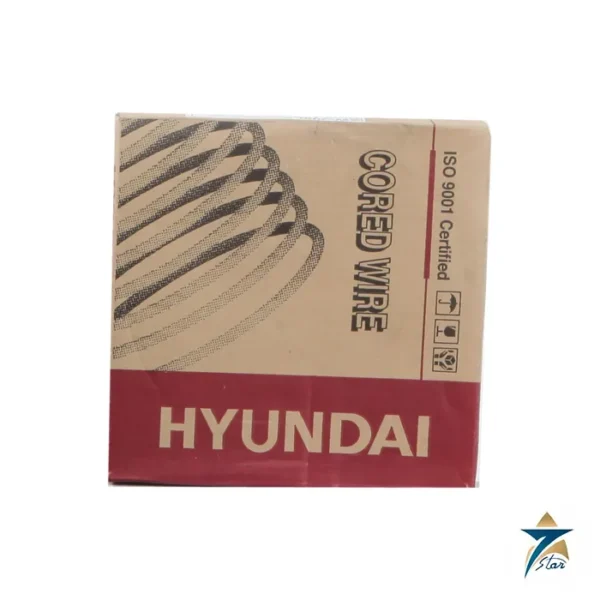
The Hyundai Welding SF-71 is a flux-cored wire classified AWS A5.20 / ASME SFA-5.20 E71T-1C, EN ISO 17632-A T 42 0 P C1 1, JIS Z 3313 T49J 0 T1-1 C A-U and KS D7104 YFW-C50DR. It is designed for welding with 100% CO2 shielding gas, on DC positive polarity, and the manufacturer lists the 1G, 2F, 3G and 4G positions, which covers flat, horizontal fillet, vertical and overhead work.
Hyundai Welding describes good performance and low spatter, with a smooth and stable arc and a fast-freezing slag. The application areas given are shipbuilding, general fabrication and structural fabrication.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Hyundai Welding / SF-71 |
| Process |
FCAW, gas-shielded, rutile |
| AWS classification |
A5.20 / SFA-5.20 E71T-1C |
| EN ISO classification |
17632-A T 42 0 P C1 1 |
| JIS classification |
Z 3313 T49J 0 T1-1 C A-U |
| Shielding gas / polarity |
100% CO2 / DC + |
| Welding positions |
1G, 2F, 3G, 4G |
| Weld metal, typical % (100% CO2) |
C 0.04, Si 0.49, Mn 1.29, P 0.013, S 0.011 |
| Yield strength |
548 MPa (79 ksi) |
| Tensile strength |
582 MPa (84 ksi) |
| Elongation |
28% |
| Impact toughness |
75 J at 0 °C; 40 J at -20 °C |
| Current, 1.2 mm |
110-280 A |
| Current, 1.4 mm |
110-280 A |
| Current, 1.6 mm |
120-300 A |
| Packaging |
Spool 5, 12.5, 15 and 20 kg; drum 100, 200 and 250 kg |
| Approvals listed |
ABS, BV, CCS, CR, DNV, KR, LR, NK, RINA, RS, CWB, CE, TUV |
Where E71T-1C is the right classification
In AWS A5.20, E71T-1C is the general-purpose rutile flux-cored wire used with 100% CO2: the 7 denotes a 70 ksi minimum tensile strength, the 1 means all-position capability, the T that it is a tubular wire, and the 1C the usage group with CO2 gas. Its slag system is fast-freezing, so the pool is supported in the vertical and overhead positions, while the wire is also efficient on flat and horizontal work.
The impact figures on the Hyundai Welding sheet, 75 J at 0 °C and 40 J at -20 °C, are typical for this class and suit ordinary structural service. Where a project specifies a lower test temperature, a nickel-bearing or low-temperature cored wire from the same manufacturer is the better choice, so check the project specification before choosing.
Setting up the wire
Use a gas flow suited to the nozzle and keep shielding free of draughts, since porosity is the first sign of lost gas cover with CO2. Select the 1.2 mm size for thin plate and position welding, and 1.4 or 1.6 mm for thicker flat and horizontal joints. If heat input is raised too far the weld metal toughness falls, so keep to the preheat and interpass limits of the procedure you are qualifying.
Documents and quotation
The Hyundai Welding SF-71 catalog sheet is attached to this page for download. Related consumables are listed in our Flux-Cored Welding Wire category. A published stick-electrode page from the same manufacturer is Hyundai Welding S-7018.1.
For a quotation, send the diameter or size, pack type, quantity and any certificate or approval requirement.


Reviews
There are no reviews yet.