Alloy 182 type cored wire for dissimilar welds and buttering
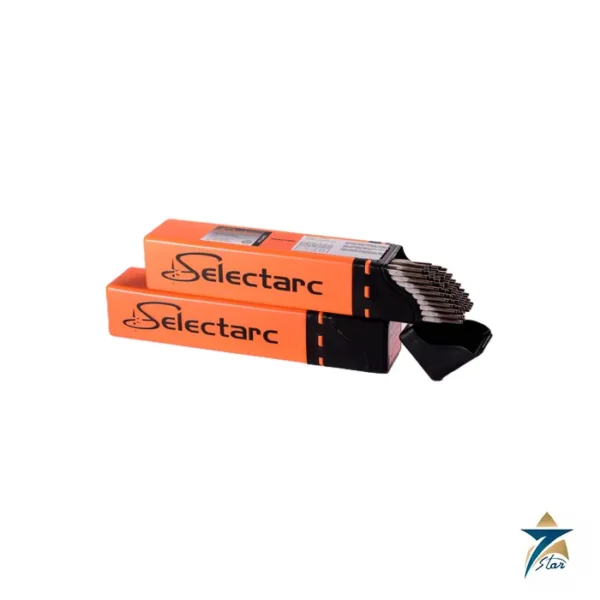
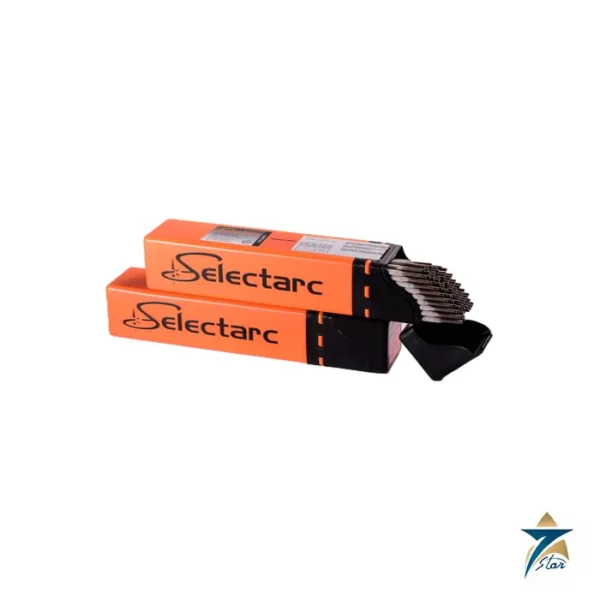
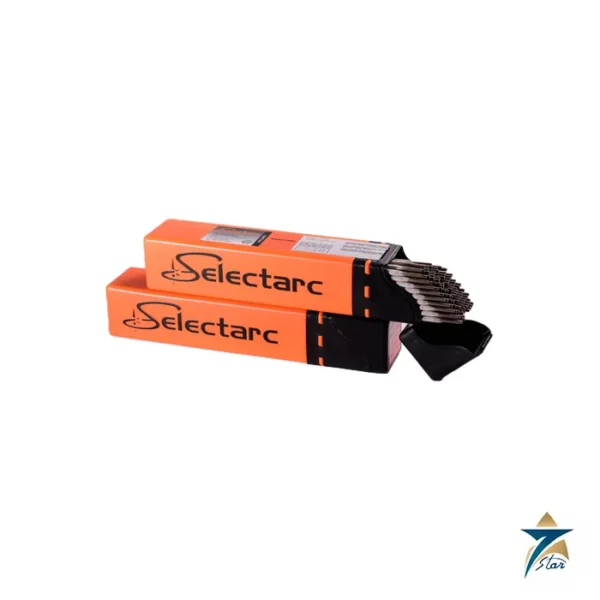
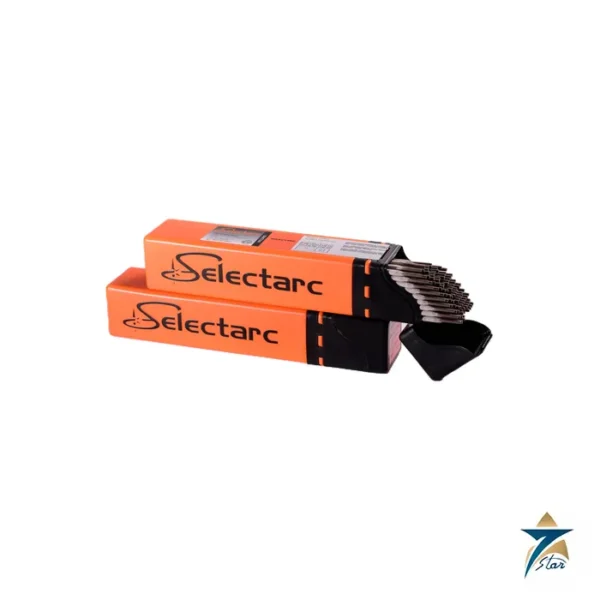
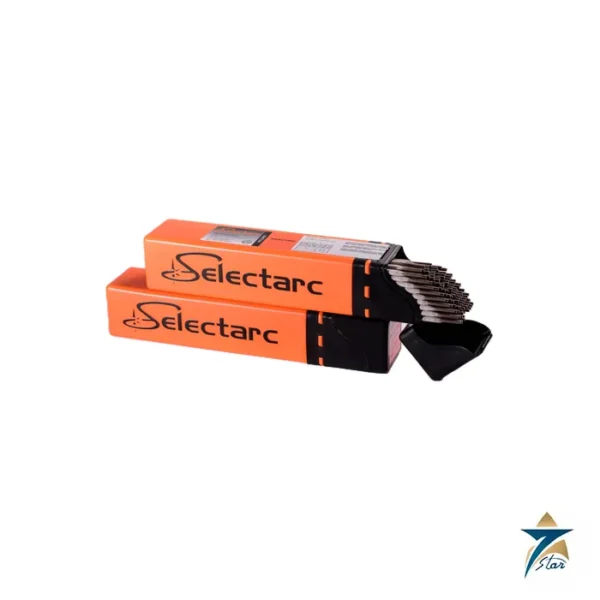
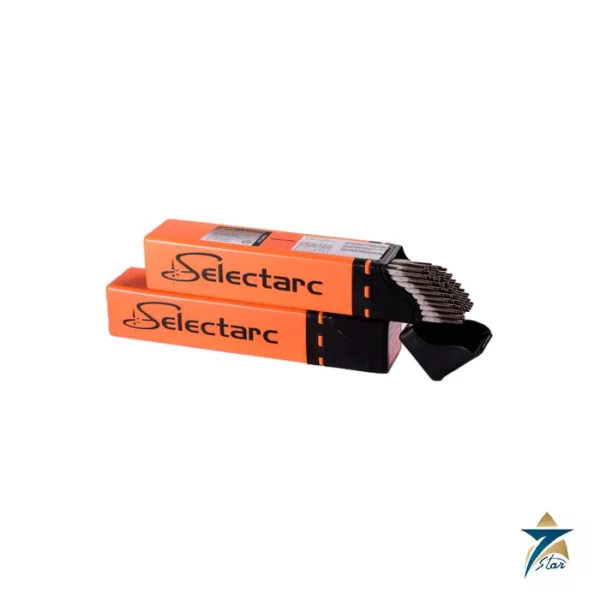
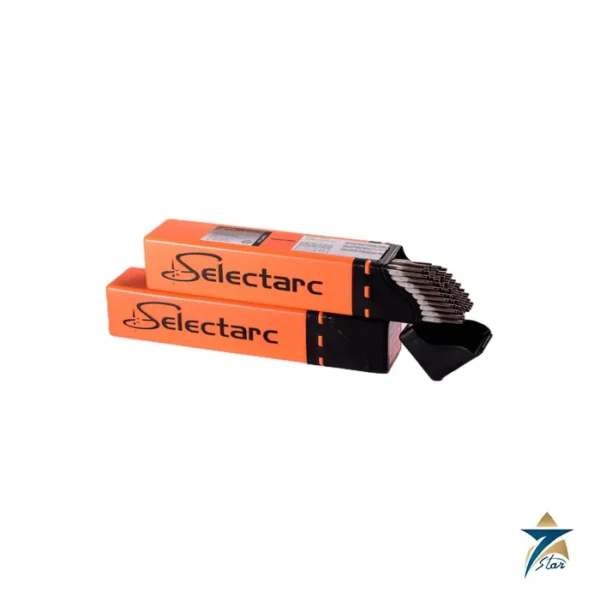
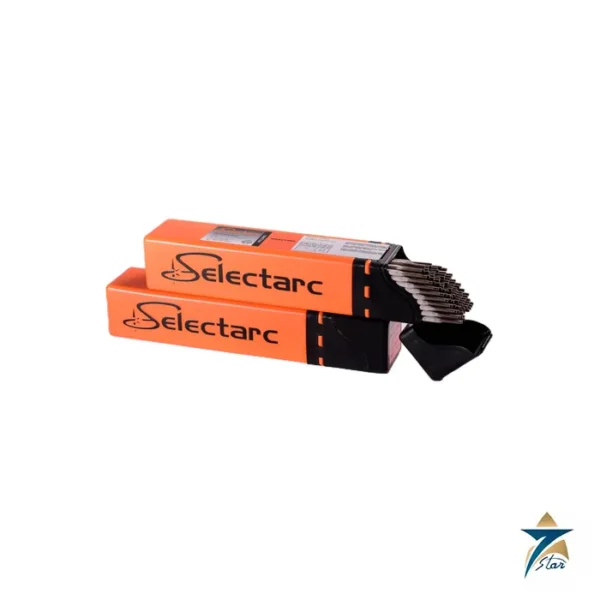
The Selectarc FCW NI182 is a rutile-basic, nickel-base flux-cored wire for gas-shielded welding in the flat position. Its deposit is of the alloy 600 / 182 family, classified AWS A5.34 ENiCrFe3T0-4 and ISO 12153 T Ni 6182 (NiCr15Fe6Mn) B M21 3, with a typical 16.8% chromium, 6% manganese, 6% iron and 1.7% niobium in a nickel matrix of more than 59%.
Selectarc names high-nickel alloys such as alloy 600 and alloy 800 types as matching materials, together with special austenitic stainless steels and dissimilar joints between low-alloy steel, stainless steel and nickel-base alloys. The deposit has good resistance to various forms of corrosion and keeps high mechanical properties at low temperature.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / FCW NI182 |
| Process |
FCAW, gas shielded |
| AWS classification |
A5.34 ENiCrFe3T0-4 |
| ISO classification |
12153 T Ni 6182 (NiCr15Fe6Mn) B M21 3 |
| Welding position |
Flat |
| Weld metal composition, min–max % |
C max 0.10, Si max 1.0, Mn 5.0–9.5, Cr 13.0–17.0, Fe max 10.0, Cu max 0.50, Nb+Ta 1.0–2.5, Ti max 1.0, P max 0.030, S max 0.015, Ni min 59.0, others max 0.50 |
| Typical composition, % |
C 0.01, Si 0.20, Mn 6.0, Cr 16.8, Fe 6.0, Nb+Ta 1.7, Ti 0.15, Ni above 59.0 |
| Rp0.2 (min / typical) |
360 / 380 MPa |
| Rm (min / typical) |
550 / 610 MPa |
| Elongation A5 (min / typical) |
25 / 40% |
| Impact energy KV (typical) |
70 J at -196 °C |
| Parameters |
1.2 mm: 130–250 A; 1.6 mm: 150–300 A; 24–32 V; stick-out 12–25 mm |
| Current type |
DC, electrode positive |
| Shielding gas |
ISO 14175 M21 (Ar/CO2), 10–20 l/min |
Typical jobs for ENiCrFe-3 filler
The data sheet lists cladding of 5% and 9% nickel steels, equipment exposed to acids at very high temperature, repair of difficult-to-weld steels and buffer layers as main applications. In refinery and power work, ENiCrFe-3 is a standard choice for joints between ferritic Cr-Mo steel and austenitic stainless steel. Its thermal expansion lies between the two parent materials, and the nickel matrix limits carbon migration across the fusion line during long service at temperature, which reduces the risk of creep-related failure at dissimilar welds.
The high manganese and niobium contents make the deposit tolerant of dilution and resistant to hot cracking, which is why it is often used to butter weld preparations before final joining, or as an intermediate layer under hardfacing and corrosion-resistant overlays.
Using the wire
Run 1.2 mm wire at 130 to 250 A and 1.6 mm wire at 150 to 300 A, both at 24 to 32 V on DC positive, with M21 shielding gas at 10 to 20 l/min and 12 to 25 mm stick-out. Weld in the flat position, using a positioner for pipe or nozzles.
When buttering carbon or Cr-Mo steel, apply preheat according to the steel side, and if the steel component needs PWHT, carry it out after buttering and before the final joint to the stainless or nickel member where the design allows. Remove slag between passes, keep spools dry, and control dilution on the first layer so that the deposit chemistry stays within the qualified range.
Documents and quotation
The Selectarc FCW NI182 data sheet is attached for download. Browse more products in our Flux-Cored Wire category.
For a quotation, send diameter, spool type, quantity and certificate requirements.


Reviews
There are no reviews yet.