E9018-B3 electrode for 2.25Cr-1Mo steel in refineries and power plants
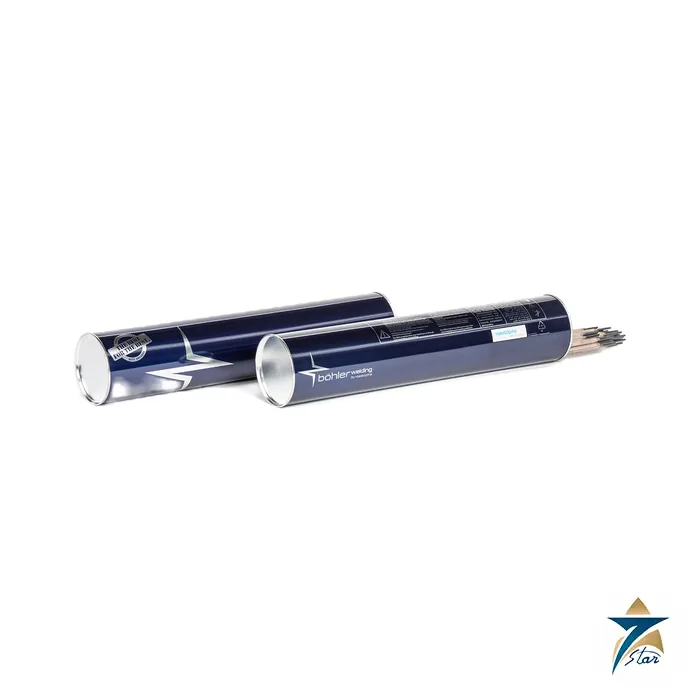
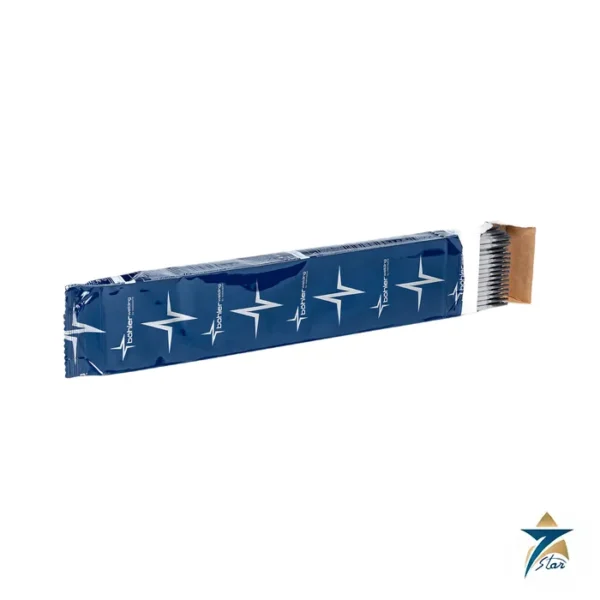
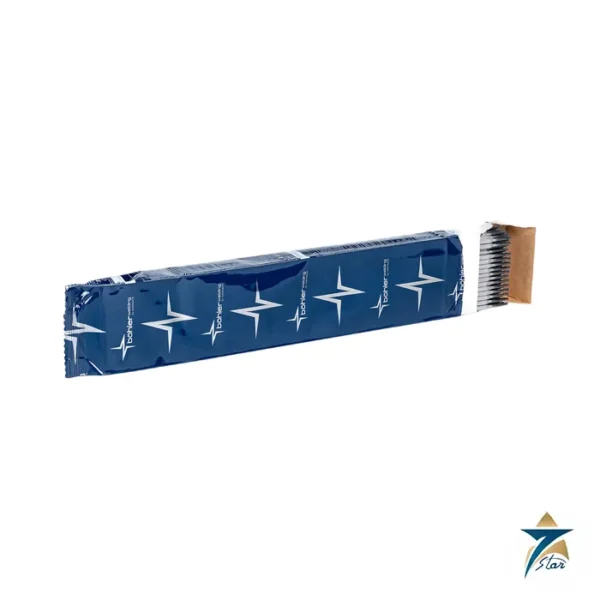
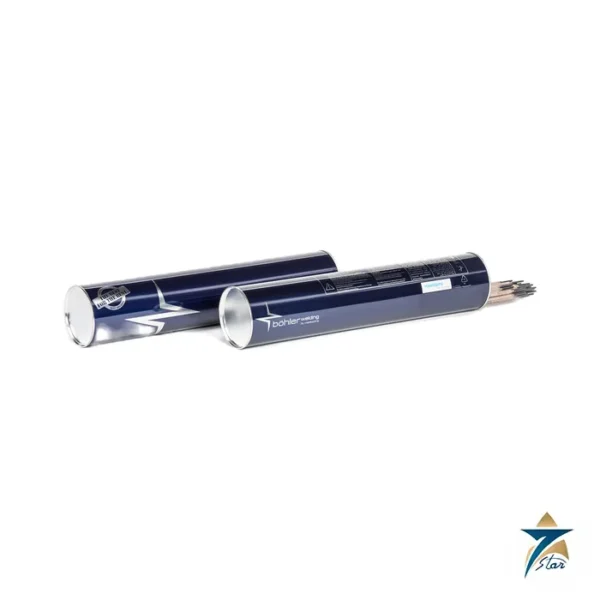
The Böhler FOX CM 2 Kb is a basic-covered, core-wire-alloyed stick electrode for 2.25 % Cr, 1 % Mo steels, classified AWS A5.5 E9018-B3 H4R and EN ISO 3580-A E CrMo2 B 4 2 H5. Böhler Welding lists it as approved for long-term exposure up to 1112 °F service temperature and applicable to welds in refineries, boiler construction and thermal power plants. The deposit is described as crack resistant and ductile with high creep rupture strength and low hydrogen (HD below 4 ml per 100 g), good weldability in all positions except vertical-down, and metal recovery of about 110 %. The deposit is nitridable and heat treatable.
Technical specifications
| Parameter |
Specification |
| AWS classification |
A5.5 / SFA-5.5 E9018-B3 H4R; A5.5M E6218-B3 H4 |
| EN ISO classification |
3580-A E CrMo2 B 4 2 H5; 3580-B E6218-2C1M H5 |
| Typical analysis, wt % |
C 0.08; Si 0.3; Mn 0.7; Cr 2.2; Mo 1.0; P up to 0.010; Sb up to 0.005; Sn up to 0.006; As up to 0.005 |
| Tempered at 1274 °F for 1 h (T1) |
Yield 87 ksi (minimum 77); tensile 102 ksi (minimum 90); elongation 22 % (minimum 18); 125 ft-lbs at 68 °F (minimum 35) |
| Tempered 1346 °F / 2 h (T2) |
Yield 81 ksi (minimum 58); tensile 96 ksi (minimum 73); elongation 21 % (minimum 18) |
| Quenched and tempered (QT) |
Yield 70 ksi (minimum 58); tensile 87 ksi (minimum 73); elongation 21 %; 133 ft-lbs at 68 °F |
| Polarity |
DC+ |
| Sizes and current |
3/32 in x 10 in: 80 to 110 A; 1/8 in x 14 in: 100 to 140 A; 5/32 in x 14 and 18 in: 130 to 180 A; about 3/16 in x 18 in: 180 to 230 A |
| Redrying |
525 to 625 °F, 2 h |
| Preheat and interpass |
390 to 660 °F; post-weld annealing 1290 to 1380 °F for at least 1 h, furnace cool to 572 °F, then still air |
| Approvals |
TÜV (00722), DB (10.014.81), ABS, DNV, CE |
Parent steels and where it fits
The data sheet lists high-temperature steels and similarly alloyed cast steels, quenched and tempered steels of similar alloy up to 140 ksi tensile strength, case-hardening and nitriding steels, among them 10CrMo9-10, 10CrMo11, 16CrMo9-3, 11CrMo9-10, G17CrMo9-10 and G19CrMo9-10, and ASTM A 182 F22, A 213 T22, A 234 WP22, A 335 P22, A 336 F22 and A 426 CP22. Choose it for P22 piping, superheater and header joints and hydroprocessing equipment where the code asks for matching chemistry. For the lighter 1.25Cr-0.5Mo grades use the
FOX DCMS Kb.
, and for P91 the
Thermanit Chromo 9 V mod.
. Alloy electrodes must be kept separate from carbon steel consumables, because mix-ups are hard to detect after welding.
| Related Böhler Welding electrode |
Classification (AWS A5.1 / A5.5 / A5.4) |
Typical use |
| FOX EV 50 |
E7018-1 H4R |
Mild and fine-grain steel, boiler, tank and offshore work |
| FOX DCMS Kb |
E8018-B2 H4 |
1 % Cr, 0.5 % Mo boiler, plate and tube steel |
| Thermanit Chromo 9 V mod |
E9015-B91 H4 |
Grade 91 (9Cr-1Mo-V-Nb) creep-strength steel |
| FOX NiMo |
E10018-D2 |
Cast steel, valves and oil tools |
Heat treatment and what to confirm
The preheat range, interpass limits and annealing cycle quoted above are the data sheet guidance; the procedure qualification for the actual wall thickness decides the final values. The low limits on phosphorus, antimony, tin and arsenic in the analysis are relevant if step-cooling or temper-embrittlement tests are in the specification, so state this in the enquiry together with the diameter, pack type, quantity and certificate level.
Documents and quotation
Attached: the manufacturer data sheet for FOX CM 2 Kb, which is the source of every figure on this page. More products of this kind are collected in welding electrodes. Send us the size, packaging, quantity, the steel you are welding and the certificate you expect, and we will prepare the offer.

Reviews
There are no reviews yet.