
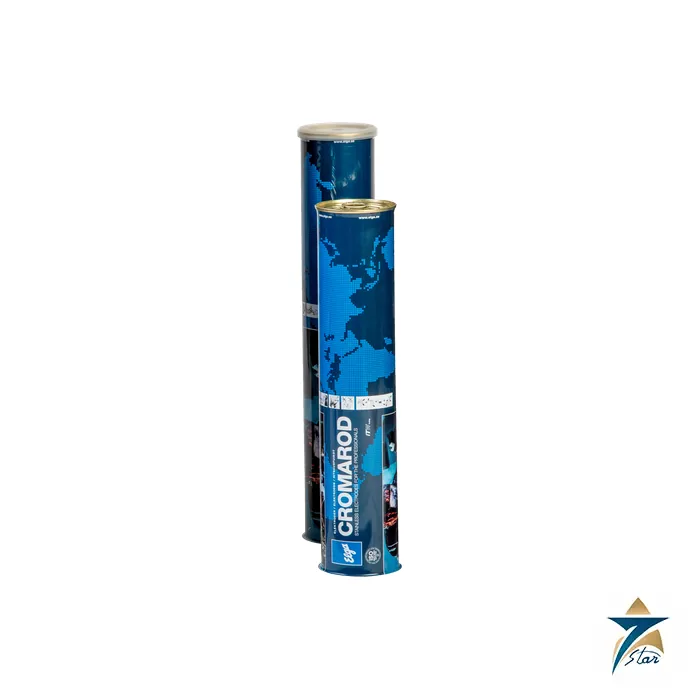
The Elga Cromarod Duplex is a rutile-coated stick electrode that deposits a 24% Cr, 10% Ni, 3% Mo and 0.15% N austenitic-ferritic weld metal with a ferrite content of about FN 35. It is designed for welding duplex stainless steels of similar composition, which combine high strength with very good resistance to chloride pitting and stress corrosion cracking.
Elga lists offshore platform pipework, pipelines carrying chloride-bearing products or sour gas, and process vessels for chloride service as typical applications. The electrode is described as easy to use, with a smooth bead finish and good slag detachability.
| Parameter | Specification |
|---|---|
| Manufacturer / product | Elga (ITW Welding AB) / Cromarod Duplex |
| Process | SMAW (stick, MMA) |
| AWS classification | A5.4 ~E2209-17 (slight difference in Cr) |
| EN ISO 3581-A | E 22 9 3 N L R 12 |
| Coating type | Rutile |
| Welding current | DC+ or AC, OCV above 39 V |
| Ferrite content | FN 35 (WRC-92) |
| Corrosion data | PRE = 36; CPT = 30 °C (ASTM G48) |
| Typical weld metal, % | C 0.02, Si 0.9, Mn 0.7, Cr 23.2, Ni 9.5, Mo 3.0, N 0.16 |
| Yield strength Rp0.2 | Specified at least 450 MPa; typical 670 MPa |
| Tensile strength Rm | Specified at least 690 MPa; typical 840 MPa |
| Elongation A5 | Specified at least 20%; typical 25% |
| Impact energy | Specified at least 27 J at -46 °C; typical 34 J |
| Sizes and current | 2.5 × 300 mm, 60–90 A; 3.2 × 350 mm, 80–120 A; 4.0 × 350 mm, 130–170 A |
| Redrying | 350 °C, 2 h |
| Approvals listed | TÜV, DNV, BV, CE, CWB |
Duplex steels depend on a balanced ferrite-austenite structure. Elga recommends a heat input range of 0.5–2.5 kJ/mm to keep a favourable phase balance, so the welding procedure should control both the current and the travel speed rather than the current alone. Electrodes that have picked up moisture can be redried at 350 °C for 2 hours.
Where the project requires higher fracture toughness at -46 °C, Elga points to Cromarod Duplex B instead. Super duplex base metals with higher alloy content are outside the scope of this grade. The AWS designation is given as approximate because the chromium content differs slightly from the E2209 range, which matters if a specification calls for a strict AWS A5.4 match.
The data sheet also gives the deposition data per size: about 1.1 kg of weld metal per arc hour for 2.5 mm, rising to about 2.0 kg per arc hour for 4.0 mm.
Further data from the sheet: the core wire is limited to P 0.020% max and S 0.010% max, with nitrogen held between 0.14% and 0.17%, and the scaling temperature of the weld metal is about 850 °C in air. Per kilogram of weld metal, about 92 electrodes are needed in 2.5 mm, 45 in 3.2 mm and 30 in 4.0 mm. The burn-off time per electrode is about 33 s, 50 s and 54 s respectively, figures that help when estimating electrode consumption and welder time for a pipe spool or vessel nozzle.
The Elga Cromarod Duplex product data sheet is attached to this page. Browse our Welding Electrodes category for other stick electrodes.
For a quotation, send the diameter, quantity, base material grade and any certificate or approval required by your welding procedure specification.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.



























Reviews
There are no reviews yet.