Metal-cored wire for automated carbon steel welding with Ar-CO2
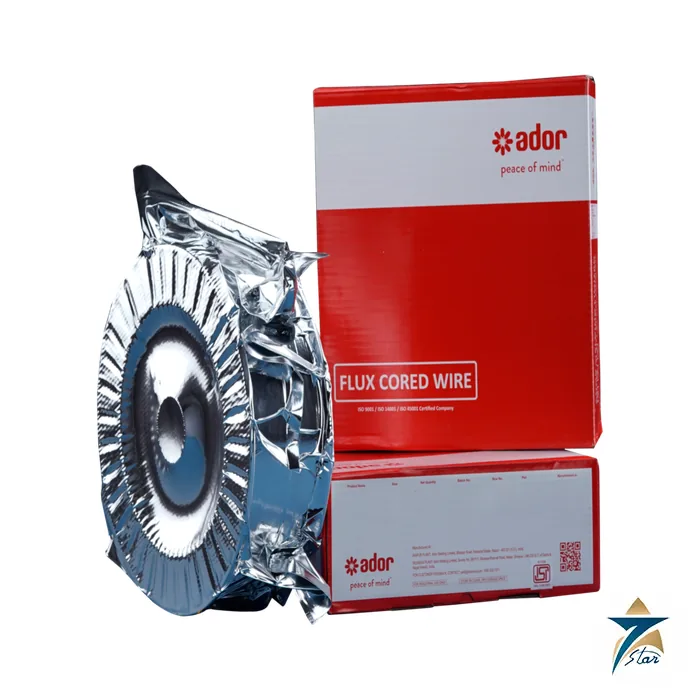
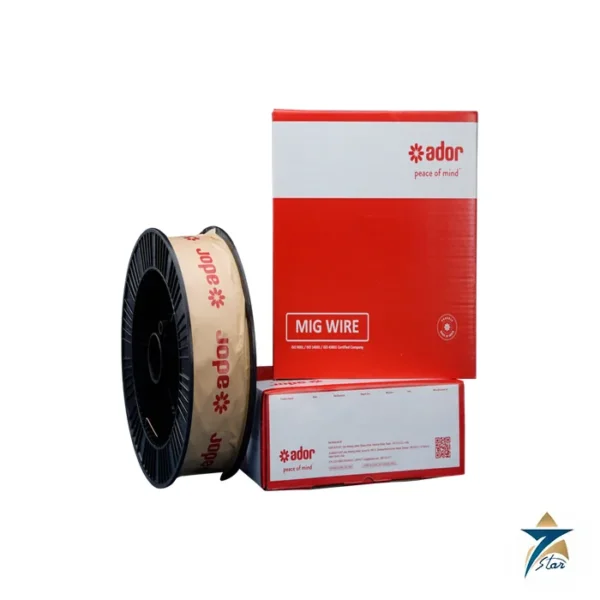
The Ador Automig MC 70C-6M is a metal-cored wire classified AWS A5.18 E70C-6M H4 and EN ISO 17632-A T 46 4 M M21 3 H5. Ador lists good weldability with minimal or no slag, excellent bead appearance, a high deposition rate, suitability for single and multi-pass welding, exceptional mechanical properties at low temperatures, and a best fit for automated and robotised applications.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Ador Welding / Automig MC 70C-6M |
| Process |
MCAW C-Mn steel, gas-shielded |
| AWS classification |
A5.18 E70C-6M H4 |
| EN ISO classification |
17632-A T 46 4 M M21 3 H5 |
| Approvals listed |
CE |
| Undiluted weld metal, typical % |
C 0.06, Mn 1.45, Si 0.4 |
| Tensile strength, as welded (typical) |
585 MPa |
| Yield strength at 0.2% offset |
490 MPa |
| Elongation |
28% |
| Charpy V impact at -40 °C |
60 J |
| Diffusible hydrogen |
Under 4 ml/100 g |
| Diameters |
1.2 and 1.6 mm |
| Net weight |
15 kg |
| Polarity / positions |
DCEP; flat butt and fillet welds only |
| Shielding gas |
80Ar+20CO2 at 15-20 l/min |
Typical applications
The data sheet lists welding of carbon and C-Mn steels including fine-grained steels, shipbuilding, boilers, pressure vessels and pipe steels. It also names suitability for joining SA 36/36M (P No. 1) and SA 285/285M Grades A, B and C (P No. 1).
How a metal-cored wire differs from a rutile cored wire
The core is mostly metal powder with little slag former, so the bead is nearly slag-free and multi-pass welds can be laid without chipping between passes. Deposition efficiency is higher than a solid wire because the arc spreads over a wider area of the tubular sheath, giving a broader penetration profile and good sidewall fusion. The compromise is positional limitation: Ador lists flat butt and fillet welds only, so the wire is not intended for vertical or overhead use.
With a low diffusible hydrogen figure under 4 ml per 100 g, the wire helps limit cold-cracking risk on thicker sections, though preheat rules from your procedure still apply. Keep a steady contact-tip-to-work distance and set voltage to hold spray transfer in the 80/20 argon-CO2 mixture. On mechanised carriages, constant travel speed makes the most of the nearly slag-free bead.
For a solid wire in the same C-Mn class, see KISWEL KC-28 ER70S-6; this metal-cored grade is the one to consider when deposition rate and automation are priorities.
Documents and quotation
The Ador Automig MC 70C-6M data sheet is attached to this page for download. Related consumables are listed in our Flux-Cored Welding Wire category.
For a quotation, send the diameter or size, pack type, quantity and any certificate or approval requirement.


Reviews
There are no reviews yet.