Seamless rutile wire for shipbuilding and structural steel
The Böhler diamondspark 52 RC is a seamless rutile flux-cored wire for single- or multilayer welding of carbon and carbon-manganese steels, including fine-grain steels, with Ar-CO2 or pure CO2 shielding. Böhler Welding lists excellent all-position weldability at high welding speed, very low spatter, good bead appearance, fast-freezing and easy-to-remove slag. The wire is described as especially suitable for shipbuilding, structural steelwork and wherever good bead appearance is required. It is approved to the AWS D1.8 seismic supplement and can be used in sour gas applications (HIC tested to NACE TM-0284, SSC values on request). The typical hydrogen level is 2.5 to 3.5 ml per 100 g weld metal. The data sheet lists the AWS classes E71T1M / T-9M / T-12M JDH4 and E71T1C / T-9C / T-12C DH4.
Technical specifications
| Parameter |
Specification |
| AWS A5.20 classification |
E71T1M/T-9M/T-12M JDH4 (M21); E71T1C/T-9C/T-12C DH4 (C1) |
| EN ISO 17632-A |
T 46 4 P M21 1 H5; T 46 2 P C1 1 H5 |
| EN ISO 17632-B |
T 49 5 T1-1M21A-H5; T 49 3 T1-1C1A-H5 |
| Deposit analysis M21 / C1, wt % |
C 0.06 / 0.04; Si 0.40 / 0.35; Mn 1.45 / 1.25 |
| Yield strength, as welded, M21 |
73 ksi typical (minimum 67) |
| Tensile strength, as welded, M21 |
86 ksi typical (77 to 90) |
| Elongation, as welded, M21 |
26 % typical (minimum 22) |
| Impact energy ISO-V, as welded, M21 |
74 J at -4 °F (minimum 35); 52 at -40 °F (minimum 35); 37 at -50 °F (minimum 20); 33 at -58 °F (minimum 20) |
| As welded, C1 |
Yield 68 ksi (minimum 67); tensile 81 ksi; elongation 28 %; 59 J at -4 °F; 35 at -40 °F |
| Stress relieved 620 °C / 1 h, M21 |
Yield 74 ksi; tensile 86 ksi; elongation 26 %; 59 J at -40 °F; 30 at -50 °F |
| Diameters |
0.045 in; 0.052 in; 1/16 in |
| Hydrogen, typical |
2.5 to 3.5 ml per 100 g weld metal |
| Approvals |
ABS, CWB, AWS D1.8 seismic supplement |
Base materials and selection
The base-material list covers S235JR to S355J2, S275N to S460N, P235GH to P355GH, L245NB to L415NB, shipbuilding grades AH32 to FH40 and ASTM A 106 Gr. A to C, A 516 Gr. 55 to 70, A 573, A 588 and API 5L Gr. B to X65. The data sheet states that standard GMAW equipment can be used. Compared with the
FOXcore 71 RC.
, this is a seamless, copper-coated design and carries the D1.8 seismic supplement; for root passes on pipe and for automation the seamless metal-cored
diamondspark 54 MC.
is the usual alternative.
| Related Böhler Welding cored wire |
Classification |
Typical use |
| FOXcore 71 RC |
AWS A5.20 E71T-1 family |
All-position rutile wire for mild steel, 0.045 to 1/16 in. |
| diamondspark 54 MC |
AWS A5.18 E70C-6M H4 |
Seamless metal-cored wire, root passes and automation |
| diamondspark X70 RC-Pipe |
AWS A5.29 E91T1-K2M |
Rutile NiMn wire for X70 and X80 pipeline welding |
Storage and ordering notes
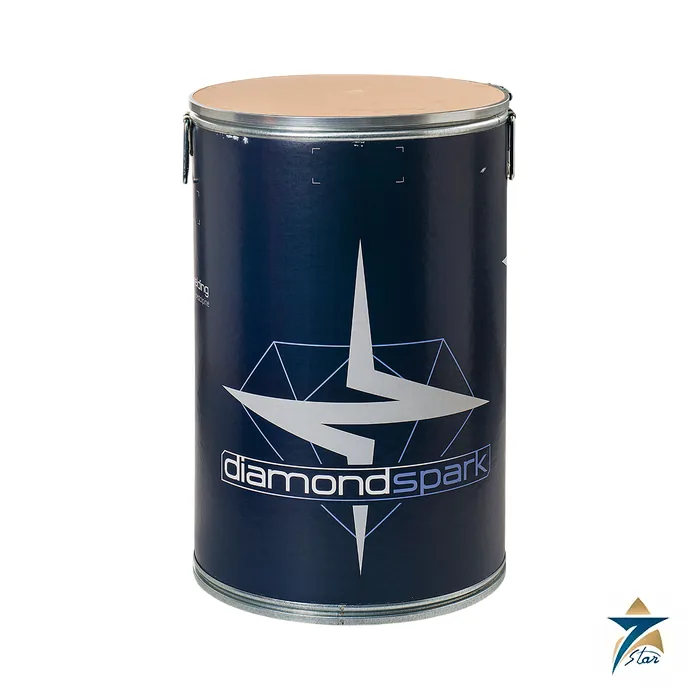
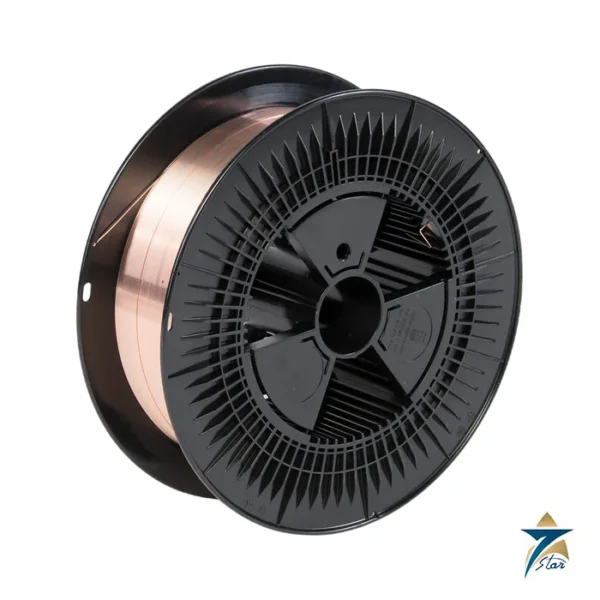
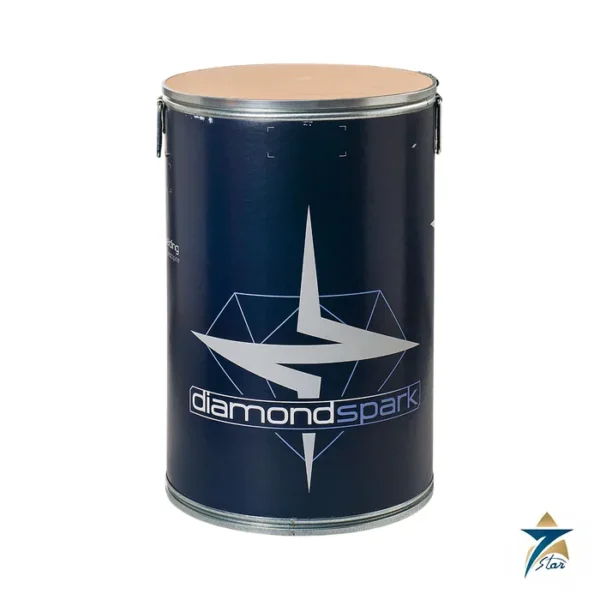
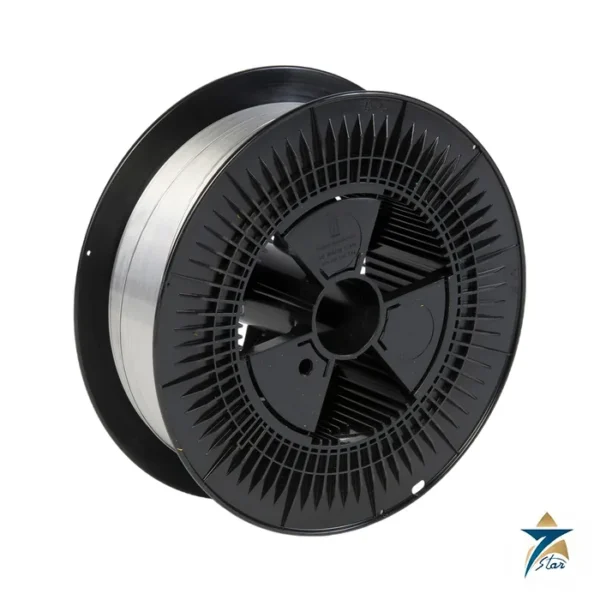
Seamless wires pick up moisture less readily than folded-seam types, but spools should still be stored dry and in the original packaging. In your enquiry state the shielding gas, diameter, packaging (spool or drum), required toughness temperature, and any class or seismic approval, because the data sheet lists ABS and CWB approvals and D1.8 only.
Key features of diamondspark 52 RC
- Seamless tube construction, which limits moisture pick-up compared with folded wires.
- Rutile slag system for all-position welding at high travel speed.
- Fast-freezing, easy-to-remove slag and low spatter, reducing post-weld cleaning.
- Usable with M21 (Ar-CO2) or C1 (100 % CO2) shielding gas.
- Low diffusible hydrogen, typically 2.5–3.5 ml/100 g weld metal.
- AWS D1.8 seismic supplement approval and HIC testing to NACE TM-0284.
Choosing the shielding gas
The data sheet gives different classifications and mechanical values for the two gases. With M21 mixed gas, the classification is T 46 4 P M21 1 H5 under EN ISO 17632-A, with impact values specified down to −40 °C; with pure CO2 the classification is T 46 2 P C1 1 H5. In general, mixed gas gives a smoother arc and less spatter, while CO2 is cheaper and gives deeper penetration. Where the welding procedure requires low-temperature toughness, the M21 data is the relevant reference, and the procedure qualification should be carried out with the gas that will be used in production.
Welding parameters and technique
As a rutile flux-cored wire, diamondspark 52 RC is normally welded with DC electrode positive. Use the parameter ranges in the Böhler data sheet for each diameter as the starting point and fine-tune for position and joint type. For vertical-up welding, a slight weave and lower current help the fast-freezing slag support the pool. Keep a consistent stick-out and travel angle, and remove the slag between passes in multilayer welds.
Use in Oman and GCC fabrication
Typical applications in the region include steel structures, ship repair and offshore support work, tanks, and general fabrication for oil and gas projects. The sour service capability (HIC tested) is relevant for some hydrocarbon applications, but confirm with the project specification whether additional SSC data is needed; Böhler provides SSC values on request. In hot and humid coastal sites, keep wire spools in their original packaging until use, return partly used spools to a dry storage cabinet, and protect the wire feeder from dust.
Quality documentation
Fabricators working to ASME, AWS D1.1 or classification society rules usually need the material test certificate for each batch. Approvals listed by Böhler include ABS and CWB; confirm with us which certificate type (for example EN 10204 3.1) you require when ordering.
What to include in your RFQ
State the product name diamondspark 52 RC, the diameter (0.045 in, 0.052 in or 1/16 in), the spool type and weight, the quantity, the required certificate, and the delivery location.
Documents and quotation
You can download the diamondspark 52 RC data sheet from this page to check each value against your procedure. Browse flux-cored welding wire for neighbouring items. To request a price, tell us the diameter, how it should be packed, how much you need, the parent metal and any certificate wording.


















Reviews
There are no reviews yet.