
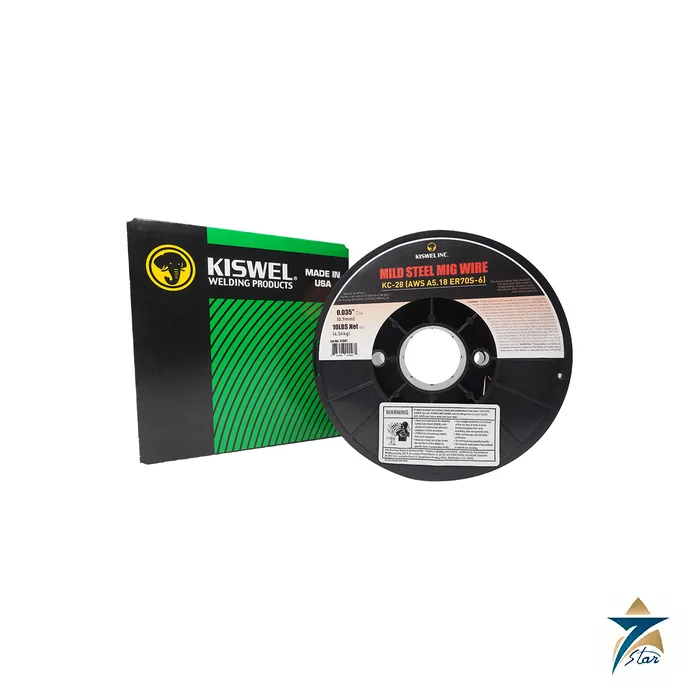
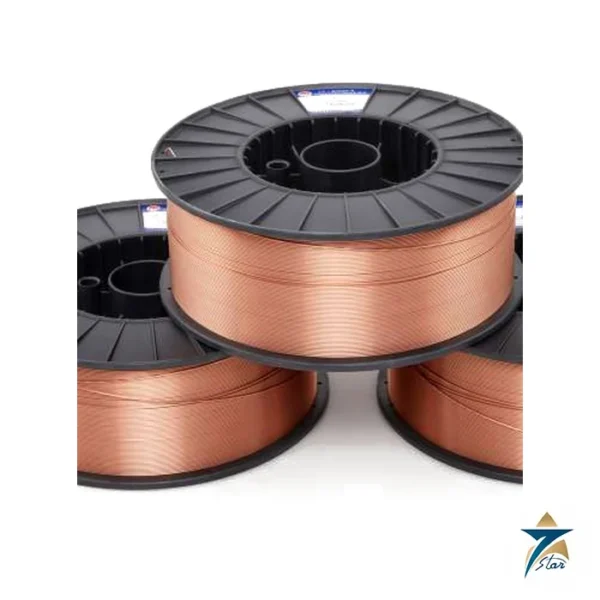
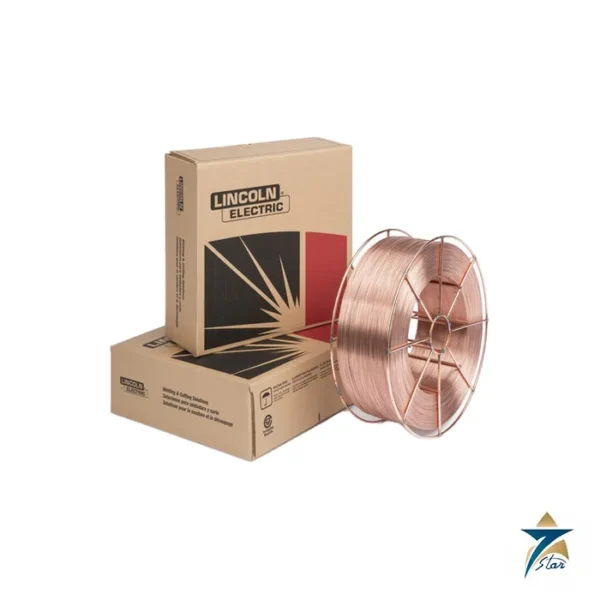
The KISWEL KC-28 is a solid MIG/MAG welding wire for mild steel and 490 MPa tensile strength steel. It is classified AWS A5.18 ER70S-6 and carries the EN ISO 14341 designations G 42 2 C G3Si1 and G 42 3 M G3Si1, so one wire covers both a pure CO2 procedure and an argon-CO2 mixed-gas procedure.
KISWEL lists KC-28 for butt and fillet welds in shipbuilding, bridges, structural steel, steel buildings, machinery and vehicles. The manufacturer describes a stable arc over almost the whole current range, low spatter, use in all welding positions, and the ability to weld sheet metal at a high current without burning through.
| Parameter | Specification |
|---|---|
| Manufacturer / product | KISWEL / KC-28 |
| Process | Gas metal arc welding (MIG/MAG), solid wire |
| AWS classification | A5.18 ER70S-6 |
| EN ISO 14341-A | G 42 2 C G3Si1 |
| EN ISO 14341-B | G 49A 3 C G6; G 49A 3 M G6 |
| KS / JIS | KS D 7025 YGW12; JIS Z 3312 YGW12 |
| Typical wire chemistry, % | C 0.07, Si 0.86, Mn 1.53, P 0.012, S 0.007 |
| Typical all-weld metal, CO2 | YS 450 MPa, TS 550 MPa, El. 30%, 70 J at -30 °C |
| Typical all-weld metal, Ar+20% CO2 | YS 480 MPa, TS 580 MPa, El. 28%, 80 J at -30 °C |
| Polarity | DCEP (DC+) |
| Shielding gas | 100% CO2 or Ar+20% CO2, 15–25 L/min |
| Current, 1.2 mm | Flat 100–350 A; vertical 50–180 A; overhead 50–180 A |
| Current, 1.4 mm | Flat 140–400 A; vertical 100–250 A; overhead 100–250 A |
ER70S-6 is the higher-silicon, higher-manganese grade in the AWS A5.18 family. The extra deoxidisers help when the plate surface is not perfectly clean, which is why it is the usual choice for general structural work. The weld metal values in the datasheet differ with the gas: the typical yield and tensile strengths are higher with the Ar+20% CO2 mixture than with 100% CO2, so qualify the procedure with the gas you will actually use on site.
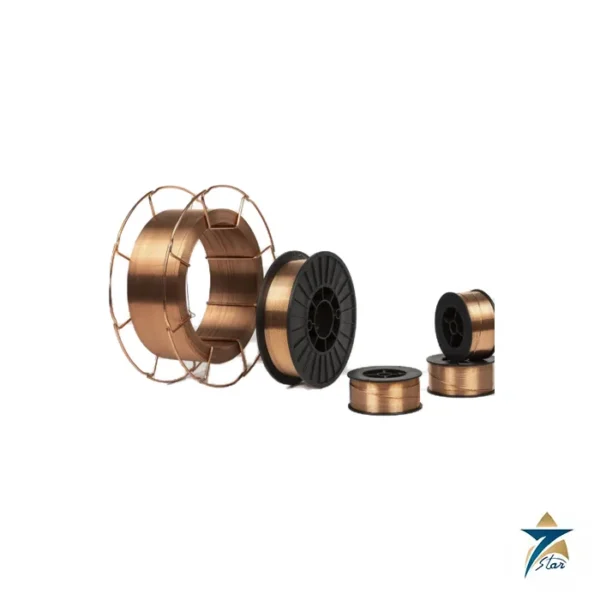
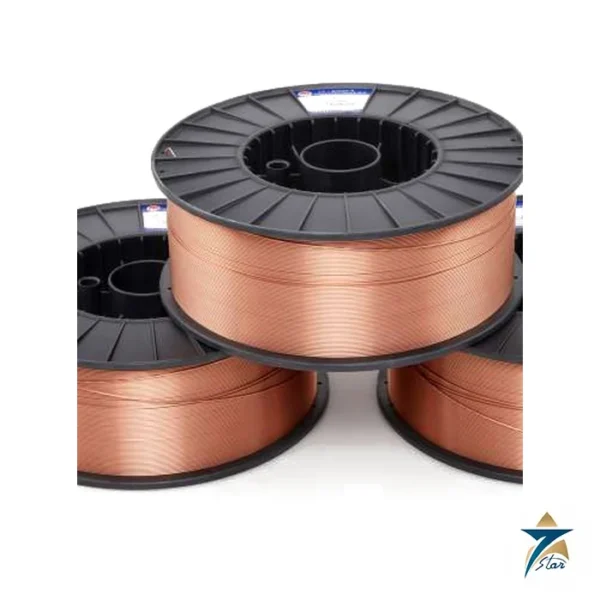
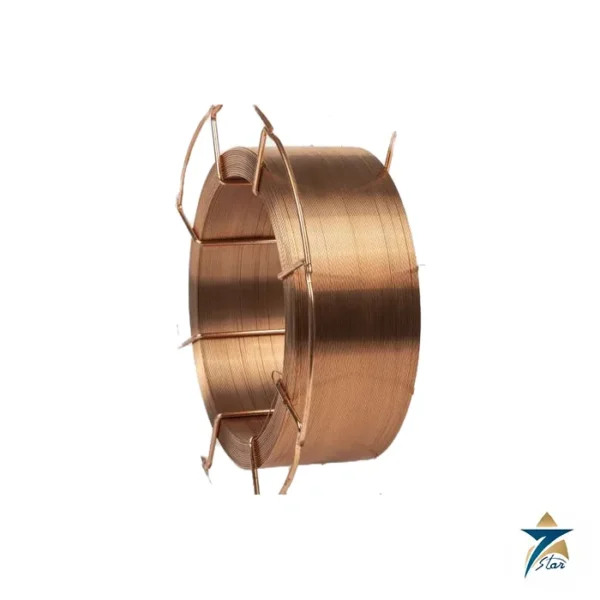
The datasheet gives separate current windows for flat, vertical and overhead welding. Vertical and overhead work runs at much lower current than flat work, so the 1.2 mm size is the more flexible choice for positional welding, while 1.4 mm suits high-current flat and horizontal fillet work. Spool size and wire diameter must match the drive rolls and the contact tips of the wire feeder.
The datasheet also lists approvals from classification societies including ABS, BV, DNV, LR, KR and NK. Approval scope depends on the gas and the grade, so ask for the certificate that covers your shielding gas if your project requires it.
It helps to separate the specified minimums from the typical results. Under AWS A5.18 the datasheet lists a minimum yield strength of 400 MPa, tensile strength of 480 MPa, elongation of 22% and at least 27 J at -30 °C with CO2. Under EN ISO 14341-A the minimums are 420 MPa yield, 500–640 MPa tensile, 20% elongation and at least 47 J at -20 °C with CO2 (G 42 2 C) or -30 °C with mixed gas (G 42 3 M). The typical values quoted above are example test results, not guaranteed figures, so design calculations and procedure qualification records should refer to the classification minimums.
The KISWEL KC-28 datasheet is attached to this page. Browse our Solid Welding Wire category for other MIG/MAG wires.
For a quotation, send the wire diameter, spool type and weight, quantity, shielding gas and any certificate requirement, such as an EN 10204 3.1 mill certificate or a classification society approval.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.













Reviews
There are no reviews yet.