High-ferrite flux-cored wire for stainless-to-carbon steel joints
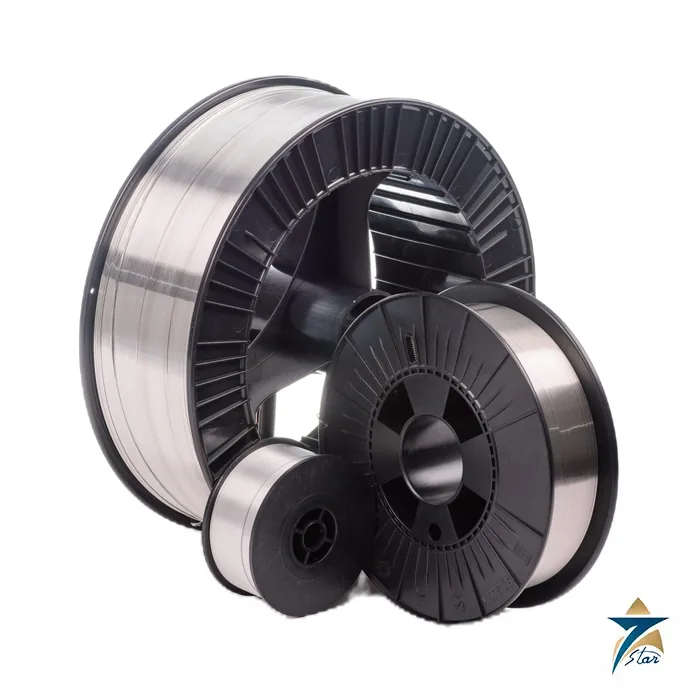
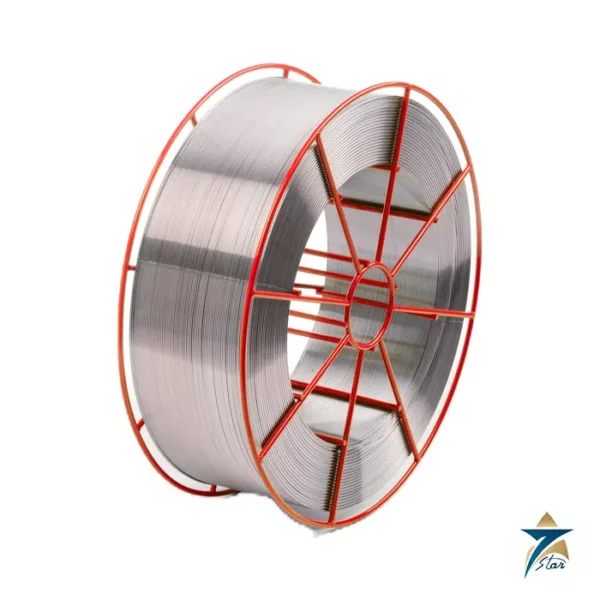
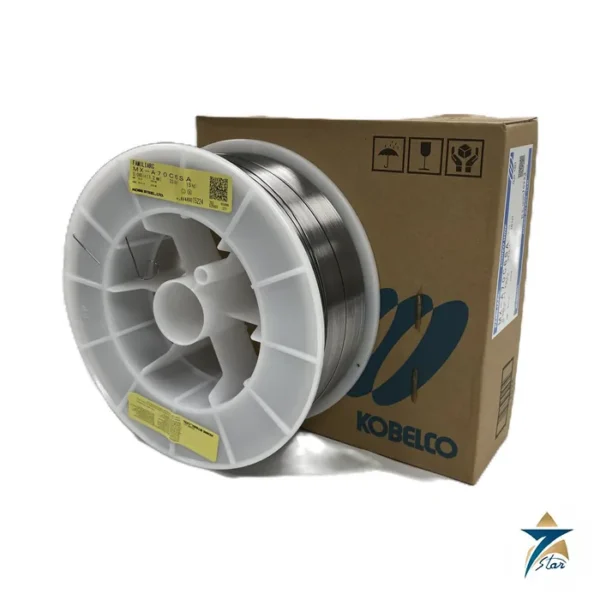
The Selectarc FCW 309LP is a gas-shielded rutile flux-cored wire of the 309L type, classified AWS A5.22 E309LT1-1/-4 and ISO 17633-A T 23 12 L P M21 (C1) 1. Selectarc describes it for welding 309L stainless steel and for dissimilar joints of 304 or 316 stainless to low-alloy steels, where the high ferrite content allows a large amount of dilution without cracking. The rutile flux freezes quickly and the wire can be used in all positions.
Listed main applications are pressure vessels, maintenance and repair, and buttering before low-carbon cladding or final hardfacing.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / FCW 309LP |
| Process |
FCAW, gas-shielded flux-cored wire |
| AWS classification |
A5.22 E309LT1-1/-4 |
| ISO classification |
17633-A T 23 12 L P M21 (C1) 1 |
| Chemical composition limits, % |
C max 0.04, Si max 1.0, Mn 0.5-2.5, Cr 22.0-25.0, Ni 12.0-14.0, Mo max 0.3, Cu max 0.5, P max 0.030, S max 0.025 |
| Typical composition, % |
C 0.03, Si 0.80, Mn 1.4, Cr 23.5, Ni 12.5, Mo 0.08, Cu 0.08, P 0.020, S 0.008; ferrite FN 23 |
| Yield strength Rp0.2 |
Minimum 320 MPa; typical 460 MPa |
| Tensile strength Rm |
Minimum 520 MPa; typical 580 MPa |
| Elongation A5 |
Minimum 30%; typical 35% |
| Impact energy KV |
Typical 45 J at -60 C |
| Wire diameter and parameters |
1.2 mm; 130-270 A; 22-35 V; stick-out 12-25 mm |
| Shielding gas |
ISO 14175 M21 (Ar/CO2), 10-20 l/min |
Why a 309L consumable for dissimilar joints
When stainless steel is welded to carbon or low-alloy steel, the carbon steel dilutes the weld metal and lowers its chromium and nickel. A 309L-type filler starts with about 23.5% chromium and 12.5% nickel, so the diluted deposit stays austenitic with some ferrite and resists hot cracking. The typical ferrite number of FN 23 on the data sheet is higher than for a 316L-type wire, which is the reason it is also used for buffer layers under 308L or 316L cladding passes.
Where the final surface must be 316L, a buffer layer of 309L is normally followed by a 316L-type consumable such as the Selectarc FCW 316LP, and the layers are chosen to match the corrosion requirement in the specification.
Welding practice
The wire runs with Ar/CO2 gas (M21) at 10 to 20 l/min on DC electrode positive. The data sheet lists 130 to 270 A, 22 to 35 V and a stick-out of 12 to 25 mm for the 1.2 mm size. Remove slag between passes. Preheat and interpass limits for the carbon steel side come from the procedure and base material thickness, not from the wire. Other cored wires are listed in the flux-cored welding wire category.
For pressure vessel repair, the weld procedure should record the base metal grades on both sides of the joint, the wire batch and the gas mixture, since these determine the final dilution and ferrite level. Selectarc quotes the limits and typical values separately, which lets a welding engineer compare the purchased wire with the procedure requirement and with the mechanical properties needed at the design temperature.
Documents and quotation
The Selectarc FCW 309LP technical data sheet is attached to this page. For a quotation, send the diameter, spool size and quantity, the shielding gas you use and any certificate requirement, such as an EN 10204 3.1 inspection certificate.


Reviews
There are no reviews yet.