Basic electrode for 13Cr-4Ni martensitic stainless castings and plate
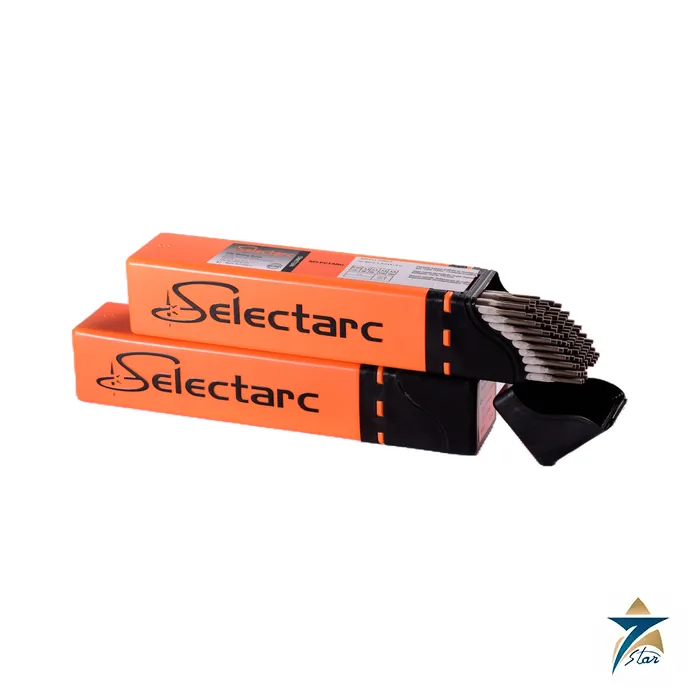
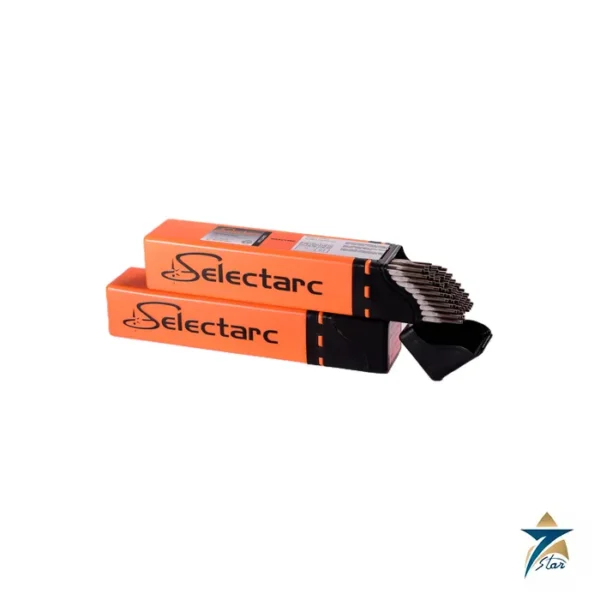
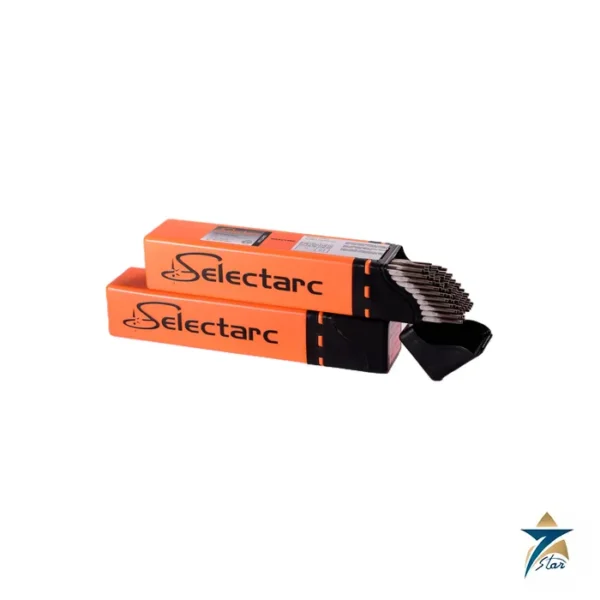
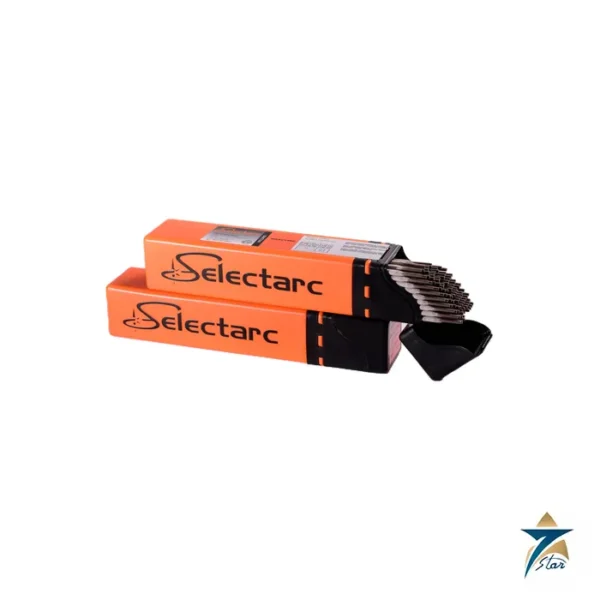
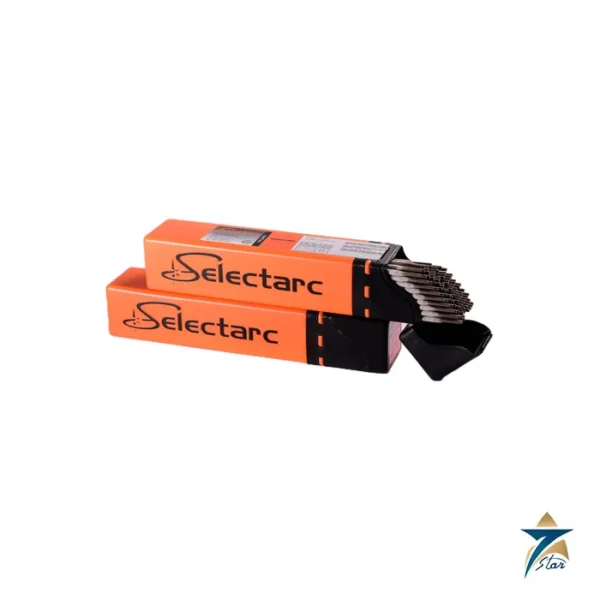
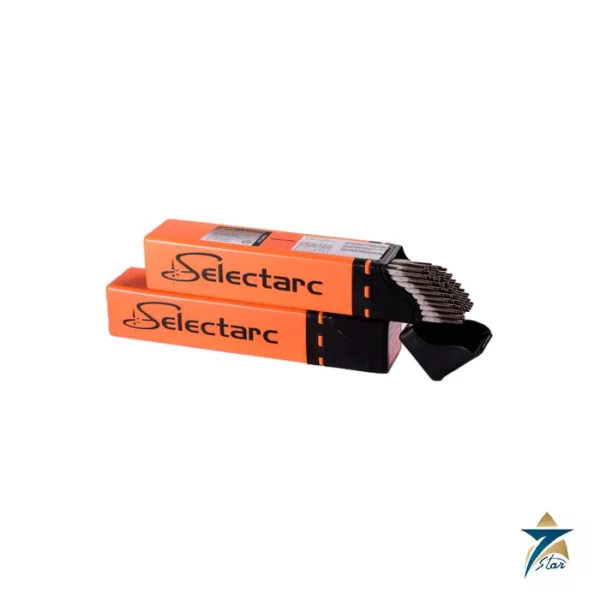
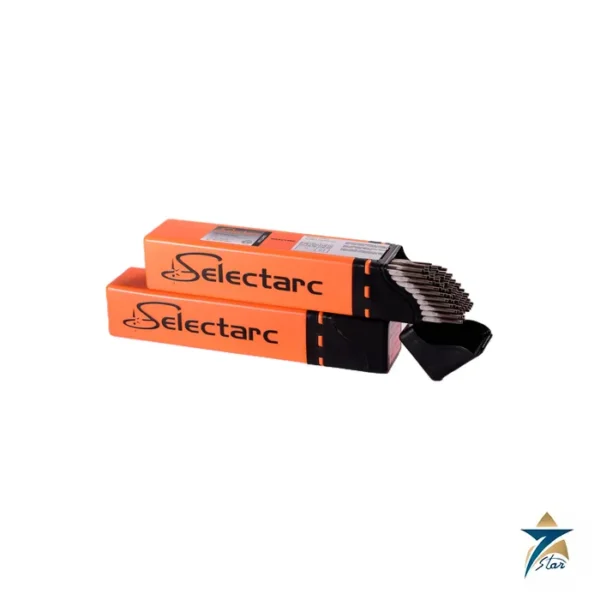
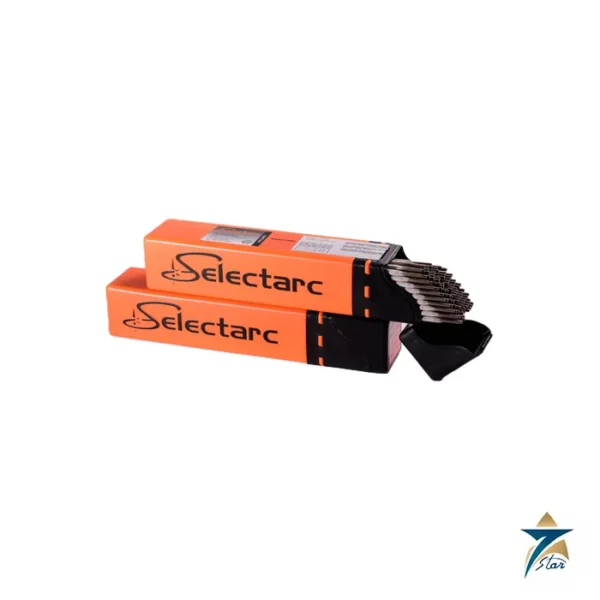
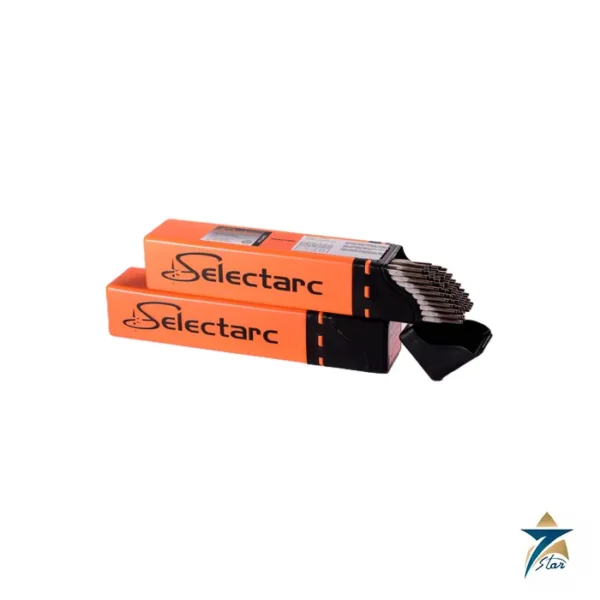
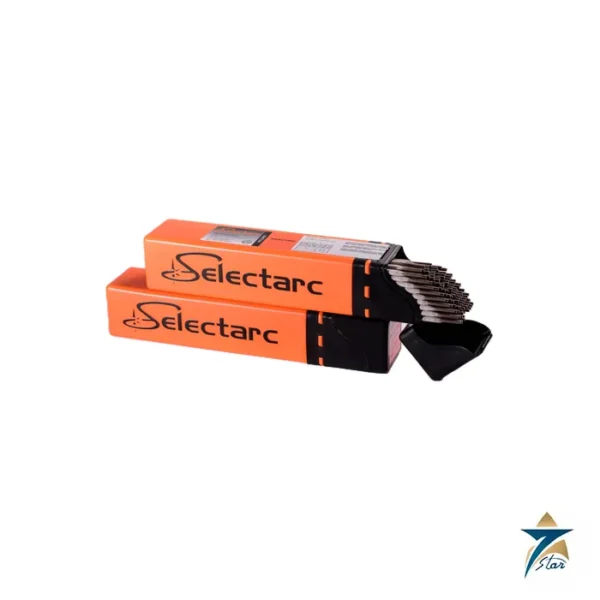
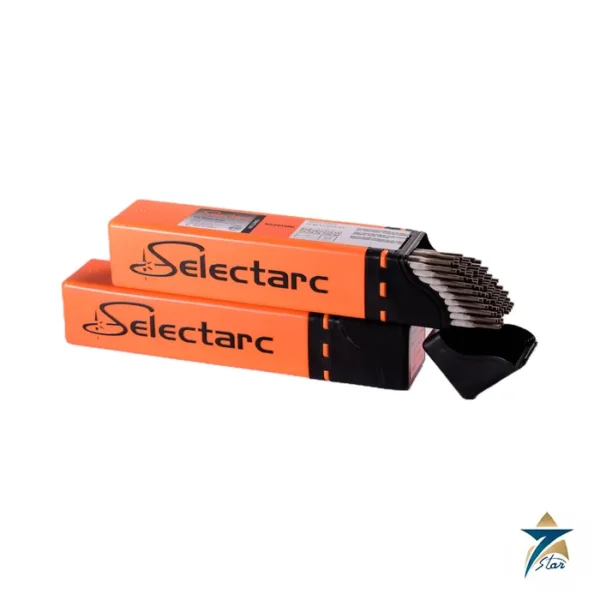
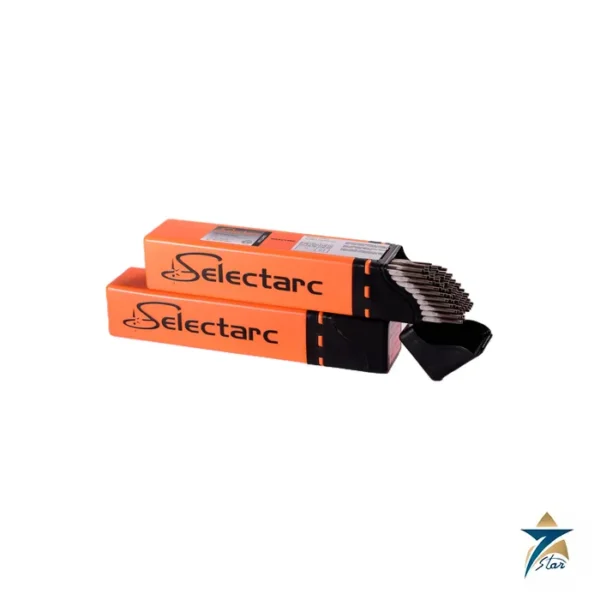
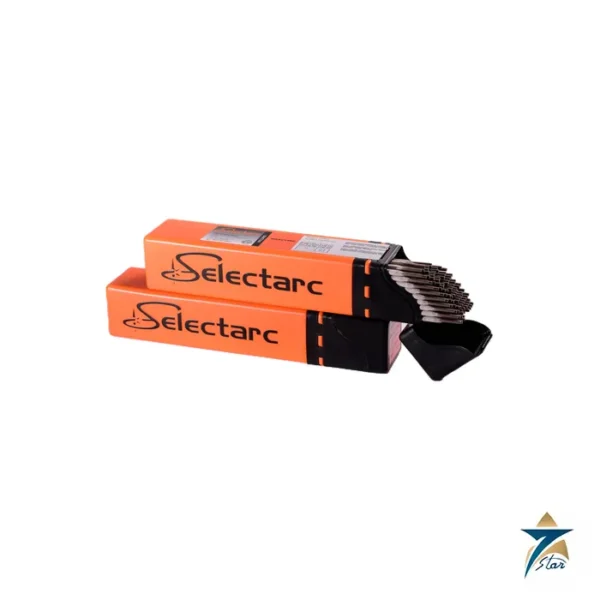
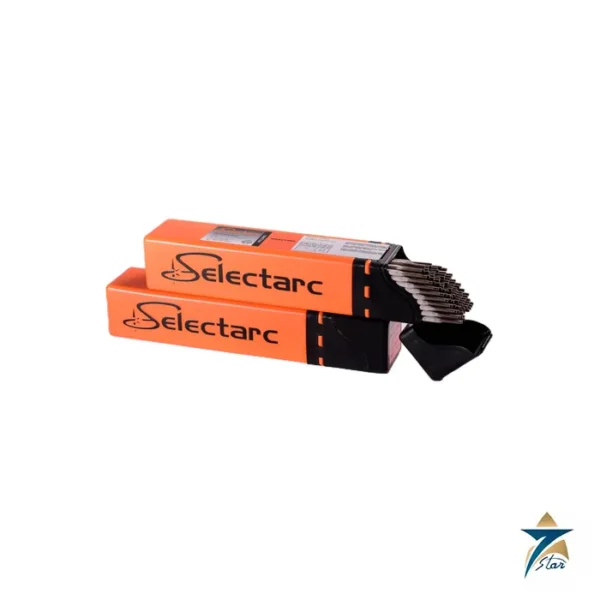
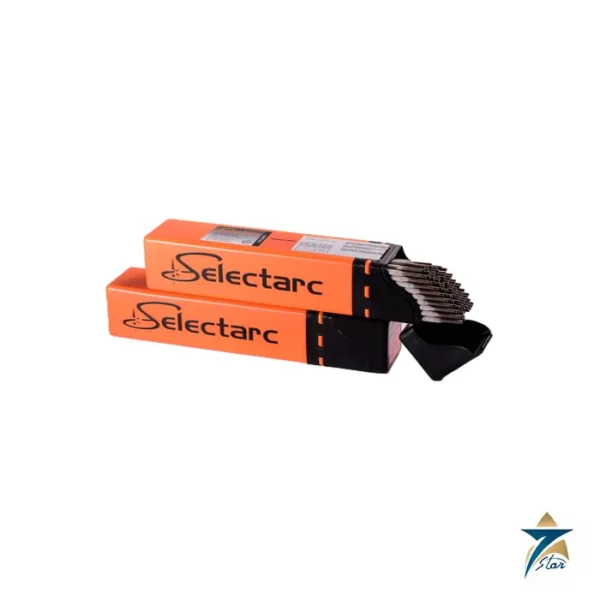
The Selectarc Inox 410NiMoB is a basic-coated stainless electrode with an alloyed core wire, classified AWS A5.4 E410NiMo-15 and ISO 3581-A E 13 4 B 4 2. Selectarc describes it for repair and construction welding of martensitic Cr-Ni steels of similar composition, with a stable arc, easy slag removal and regular beads. The weld metal contains about 12.2% chromium, 4.4% nickel and 0.5% molybdenum.
The steels and castings it is intended for are those used in hydraulic turbines, pumps, valve bodies and compressor parts, where cavitation and erosion resistance matter along with strength.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / Inox 410NiMoB |
| Process |
SMAW (stick, MMA) |
| AWS classification |
A5.4 E410NiMo-15 |
| ISO classification |
3581-A E 13 4 B 4 2 |
| Coating |
Basic, alloyed core wire |
| Typical weld metal, % |
C 0.04, Si 0.3, Mn 0.6, Cr 12.2, Ni 4.4, Mo 0.5, Cu 0.1, Fe balance |
| Yield strength Rp0.2 |
Over 630 MPa (after PWHT 600 C / 4 h) |
| Tensile strength Rm |
Over 830 MPa |
| Elongation A5 |
Over 15% |
| Impact energy KV |
Over 60 J at +20 C |
| Hardness |
About 300 HB |
| Sizes (diameter x length) and current |
2.5 x 350 mm, 80 A; 3.2 x 350 mm, 110 A; 4.0 x 450 mm, 150 A; 5.0 x 450 mm, 180 A |
| Redrying |
2 h at 300 C |
Base materials covered
The data sheet lists martensitic stainless steels and castings: CA6-NM (J91540, G-X5CrNi13-4, 1.4313), S41500 (X3CrNiMo13-4, 1.4313), G-X4CrNi13-4 (1.4317), G-X5CrNiMo13-4 (1.4407), X3CrNiMo13-4 (1.4413) and G-X4CrNiMo13-4 (1.4414). Typical jobs are the repair of eroded or cracked runner blades, pump casings and valve bodies, as well as fabrication welding of new castings and plate of the same family.
A matching 13Cr-4Ni deposit reaches its properties only after a post-weld heat treatment. The values on the data sheet apply after PWHT at 600 C for 4 hours, so a procedure qualification should be run with the same cycle that the finished component will receive.
Preheat, redrying and welding practice
Selectarc advises redrying for 2 hours at 300 C, guiding the electrode with a slight inclination and welding with a short arc. The base material is preheated to 200-300 C and kept at that temperature during welding; after welding, the part is cooled to room temperature before the PWHT is performed, which allows the martensitic structure to form fully and then be tempered. Use 2.5 mm at 80 A for thin sections or roots, 3.2 mm at 110 A for general work, and 4.0 or 5.0 mm at 150 to 180 A on heavy sections and large repairs.
Martensitic 13Cr-4Ni steels are chosen over plain 12% chromium grades because the nickel keeps carbon low and the structure tough, so castings can be welded with manageable preheat and still reach good impact toughness. For an exact match to a particular casting grade, compare the typical weld metal analysis on the data sheet with the parent metal specification and your qualified procedure, and agree any additional testing, such as hardness limits after PWHT, before ordering.
Documents and quotation
The Selectarc Inox 410NiMoB technical data sheet is attached to this page. Browse our Welding Electrodes category for other stick electrodes. For a quotation, send the diameter and length, quantity, packaging preference and any certificate requirement, such as an EN 10204 3.1 inspection certificate.

Reviews
There are no reviews yet.