
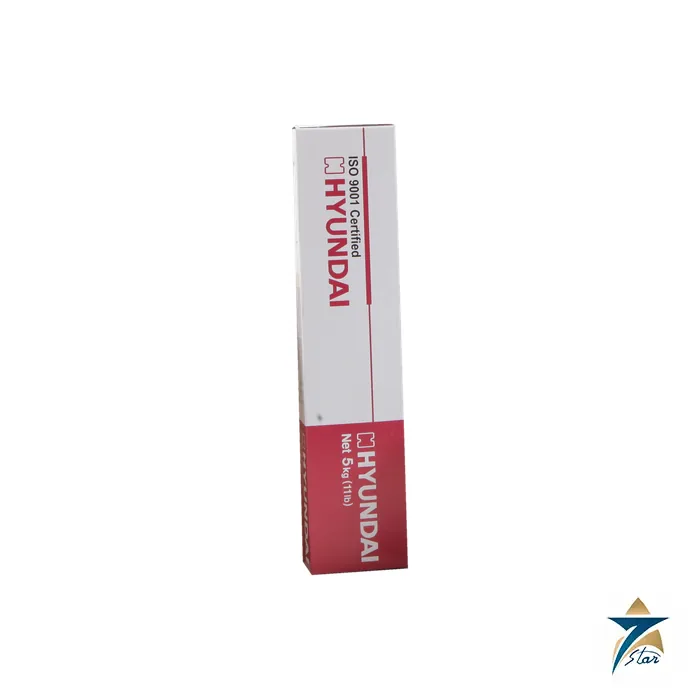
The Hyundai Welding S-9018.B3 is an iron powder, low hydrogen electrode for 2.25 % chromium – 1 % molybdenum steel. It is classified to AWS A5.5 / ASME SFA-5.5 E9018-B3, JIS Z 3223 E6218-2C1M and EN ISO 3580-A E CrMo2 B 3 2. Hyundai Welding gives a maximum service temperature of 600 °C (1112 °F), good mechanical properties and good creep resistance.
This grade is the step above B2 for higher temperature and higher pressure duty. Seven Star LLC supplies the Hyundai Welding S-9018.B3 from Muscat to power generation, refining and pressure vessel customers throughout Oman and the GCC. The manufacturer datasheet is attached to this page.
In general terms, 2.25Cr-1Mo steel is chosen when service temperature, pressure or hydrogen partial pressure exceed what 1.25Cr-0.5Mo steel can handle economically. It offers higher creep strength and better resistance to high-temperature hydrogen attack, so it is common in steam lines, superheater and reheater piping, and in heavy-wall reactors for hydrotreating and hydrocracking.
Welding it calls for matching filler, careful control of hydrogen, controlled preheat and interpass temperature, and post-weld heat treatment. The Hyundai Welding S-9018.B3 datasheet reports its properties after PWHT at 690 °C for one hour. The actual thermal cycle for a job is set by the design code and the qualified procedure, not by the electrode data alone.
Typical all-weld-metal composition is 0.08 % C, 0.21 % Si, 0.58 % Mn, 0.015 % P, 0.011 % S, 2.13 % Cr and 1.10 % Mo. After PWHT at 690 °C x 1 hour, typical mechanical properties are 564 MPa (82 ksi) yield, 674 MPa (98 ksi) tensile and 24 % elongation. Positions are 1G, 2F, 3G and 4G, the polarity field reads AC, DC±, and the approvals line shows ABS, DNV, KR and LR.
Diameters for the Hyundai Welding S-9018.B3 are 2.6 and 3.2 mm (350 mm long), 4.0 and 5.0 mm (400 mm) and 6.0 mm (450 mm). The 5.0 and 6.0 mm sizes are listed only for flat and horizontal-fillet welding, where the 5.0 mm runs at 190 to 250 A. Packing is a 5 kg (11 lbs) packet, standard or vacuum, inside a 20 kg (44 lbs) carton, with redrying at 300 to 350 °C for 0.5 to 1 hour.
Hyundai Welding lists these characteristics for the Hyundai Welding S-9018.B3:
The Hyundai Welding S-9018.B3 is used for main steam and hot reheat piping, boiler and HRSG components, refinery heater tubes and transfer lines, and heavy-wall pressure vessels in 2.25Cr-1Mo steel. Combined-cycle plants and the large refinery and petrochemical sites in Oman rely on this alloy class, and repair welding during planned outages is a frequent requirement.
Alongside the electrode, Seven Star LLC can supply power sources such as the ESAB Rebel EMP 285ic and Lincoln Electric Power Wave S500, and filler wires such as the Lincoln Electric SuperArc L-59 for carbon steel work. Other stick electrodes are listed in the welding electrodes category.
Hyundai Welding publishes both grades, which makes a direct comparison possible. The Hyundai Welding S-9018.B3 deposit contains about 2.13 % Cr and 1.10 % Mo, against 1.21 % Cr and 0.53 % Mo for the S-8018.B2. After the same 690 °C x 1 hour PWHT, the B3 shows typical 674 MPa tensile and 24 % elongation, while the B2 shows 681 MPa and 27 %. The decisive difference is therefore not room-temperature strength but the alloy content that governs creep behaviour and resistance to hydrogen attack at service temperature, which is why the B3 carries a stated maximum service temperature of 600 °C.
As general guidance, the filler should match the base metal: B3 for 2.25Cr-1Mo, B2 for 1.25Cr-0.5Mo. When joining the two grades together, codes usually allow the lower-alloy filler, but this must be confirmed by the design engineer and the procedure. Never mix boxes on site; separate, clearly labelled holding ovens prevent costly weld-metal mix-ups that are only found by later PMI testing.
The table summarises Hyundai Welding S-9018.B3 manufacturer data; chemistry and strength figures are typical, not guaranteed minimums.
| Parameter | Specification |
|---|---|
| Model | S-9018.B3 |
| Type | Heat-resistant and low-alloy steel, iron powder low hydrogen (SMAW) |
| AWS / ASME | A5.5 / SFA-5.5 E9018-B3 |
| JIS | Z 3223 E6218-2C1M |
| EN ISO | 3580-A E CrMo2 B 3 2 |
| Polarity (datasheet) | AC, DC± |
| Positions | 1G, 2F, 3G, 4G |
| Maximum service temperature | 600 °C (1112 °F) |
| Approvals shown | ABS, DNV, KR, LR |
| Redrying | 300 to 350 °C (572 to 662 °F), 0.5 to 1 hour |
| Chemistry (wt %) | C 0.08, Si 0.21, Mn 0.58, P 0.015, S 0.011, Cr 2.13, Mo 1.10 |
| PWHT for test | 690 °C x 1 hour |
| Yield / tensile after PWHT | 564 MPa (82 ksi) / 674 MPa (98 ksi) |
| Elongation | 24 % |
| Packaging | 5 kg (11 lbs) packet, standard or vacuum; 20 kg (44 lbs) carton |
| Diameter mm (in) | Length mm (in) | F and HF (A) | V-up, OH (A) |
|---|---|---|---|
| 2.6 (3/32) | 350 (14) | 50-90 | 50-80 |
| 3.2 (1/8) | 350 (14) | 90-130 | 80-120 |
| 4.0 (5/32) | 400 (16) | 130-190 | 120-170 |
| 5.0 (3/16) | 400 (16) | 190-250 | not listed |
| 6.0 (15/64) | 450 (18) | 250-300 | not listed |
General guidance for chrome-moly consumables is strict moisture control: open only what can be used, redry exposed electrodes, and keep them in heated holding ovens. For the Hyundai Welding S-9018.B3 the manufacturer redrying condition is 300 to 350 °C for 0.5 to 1 hour. Exposure time limits and any further hydrogen requirements should follow the project code.
For outage work, plan oven capacity in advance: heavy-wall 2.25Cr-1Mo joints can consume many packets per shift, and every electrode issued should come from a redried, temperature-controlled source so that the low hydrogen character of the coating is preserved right up to the arc.
The official Hyundai Welding S-9018.B3 datasheet is attached to this page for download.
Send Seven Star LLC the diameters, quantities and test certificates you need to receive a quotation for the Hyundai Welding S-9018.B3. Our Muscat team supports power, refinery and fabrication customers across Oman and the GCC with engineering support.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.

























Reviews
There are no reviews yet.