Nickel-chromium-molybdenum electrode for severe corrosion
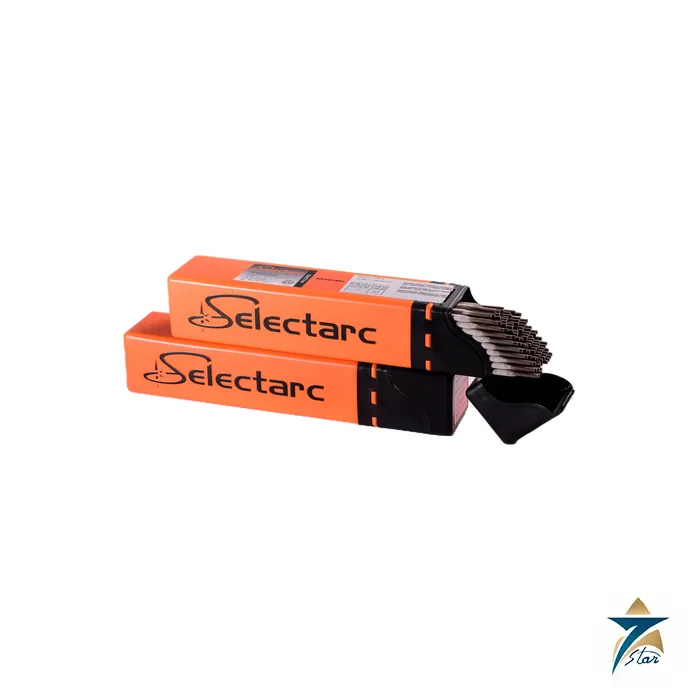
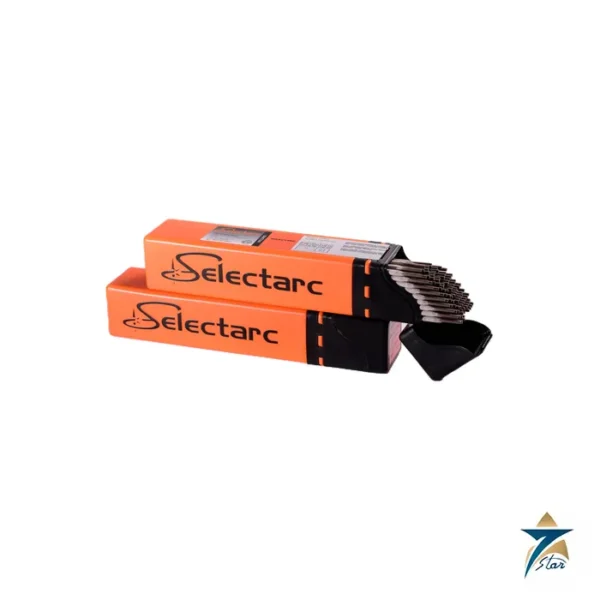
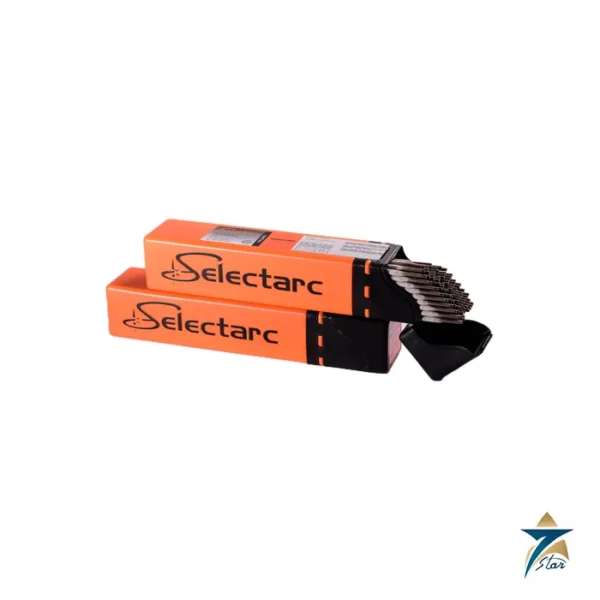
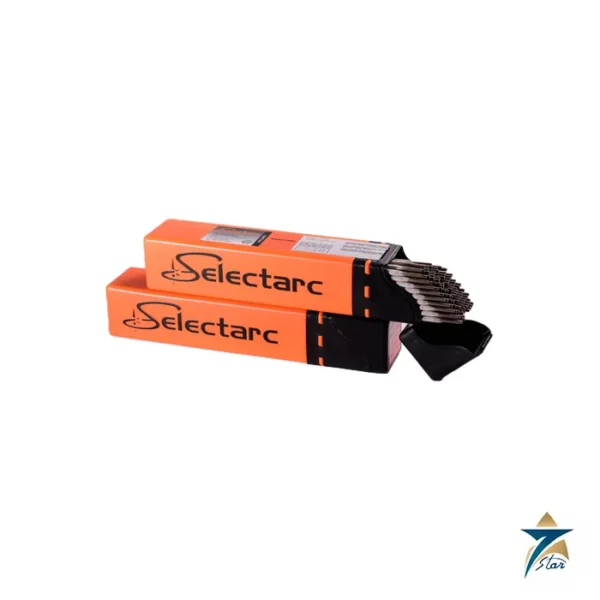
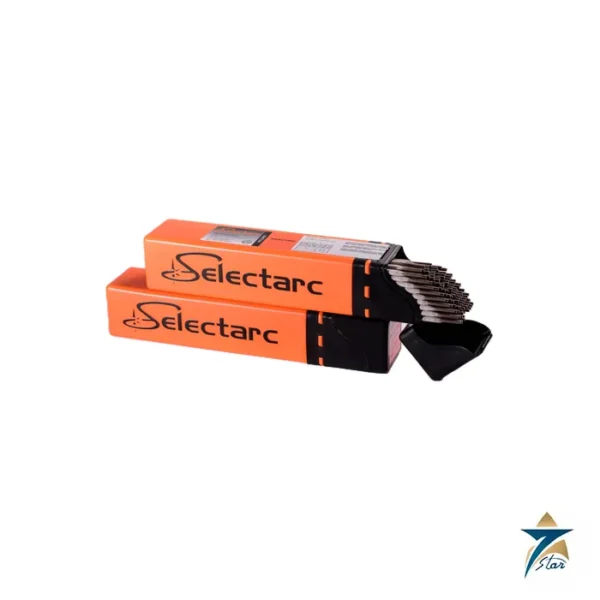
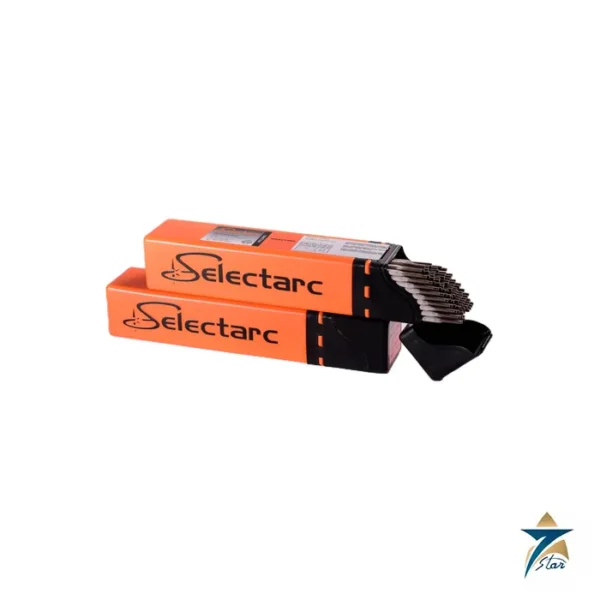
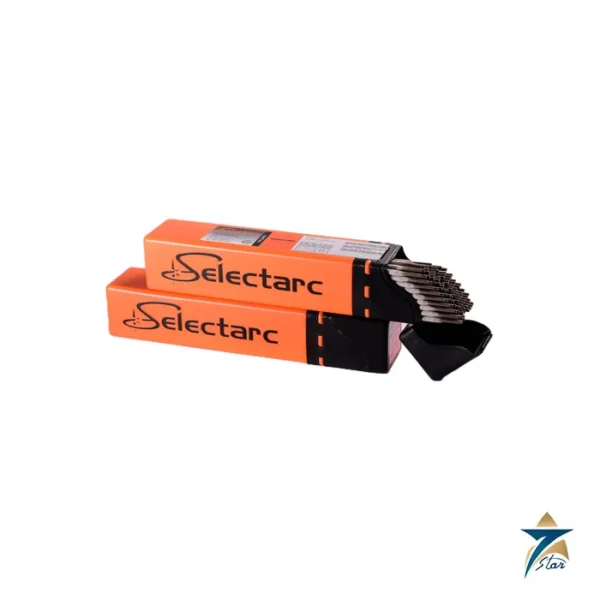
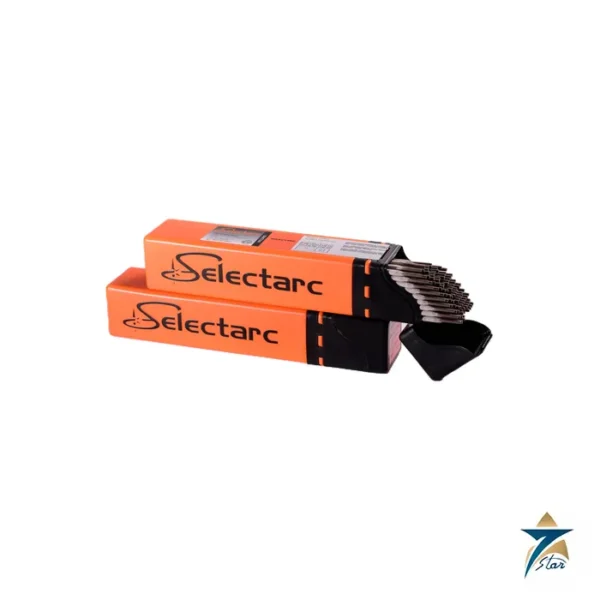
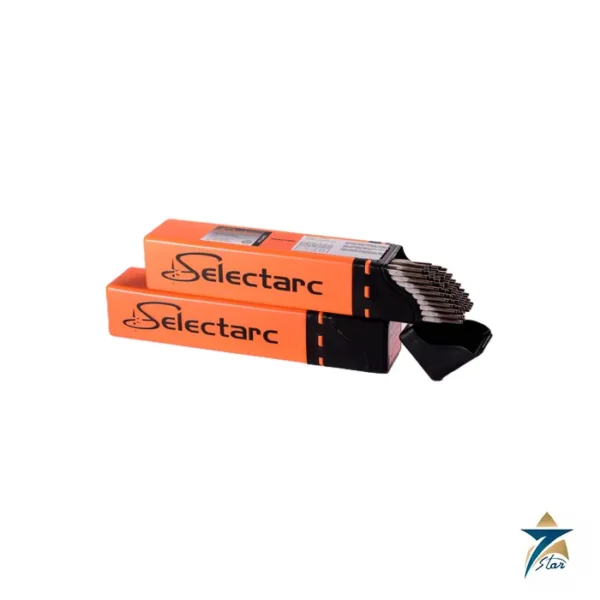
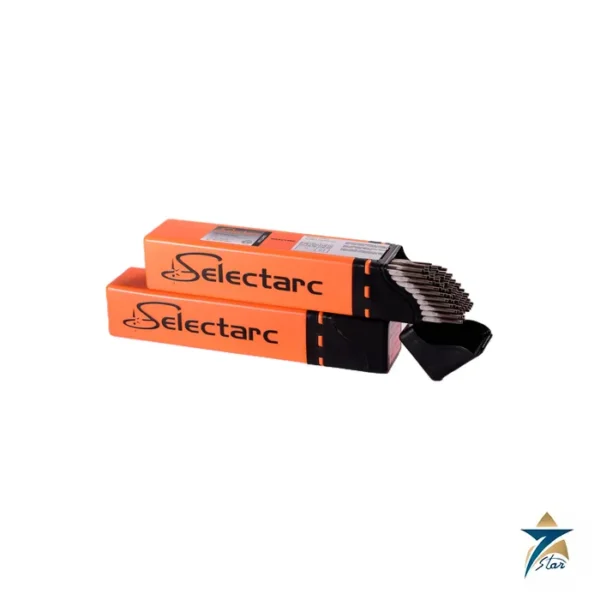
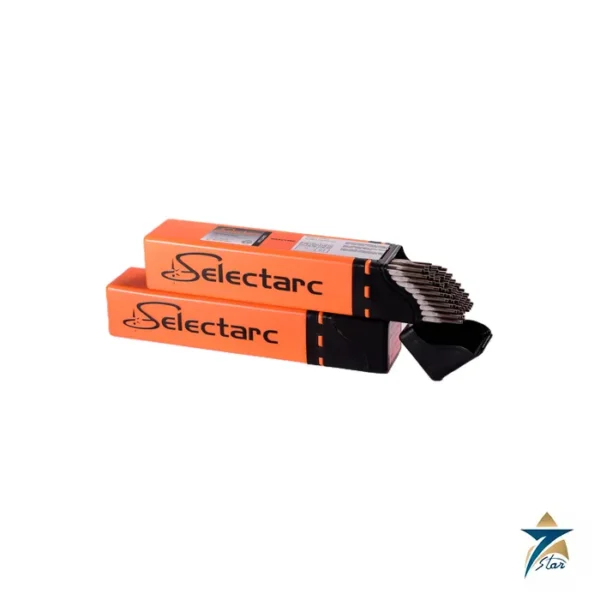
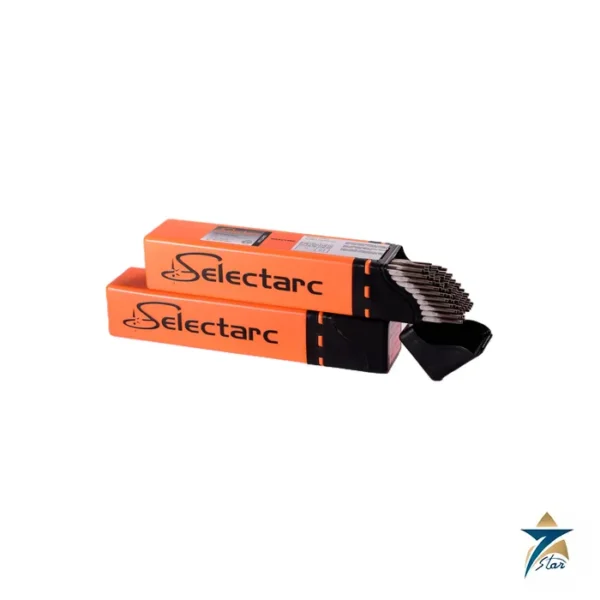
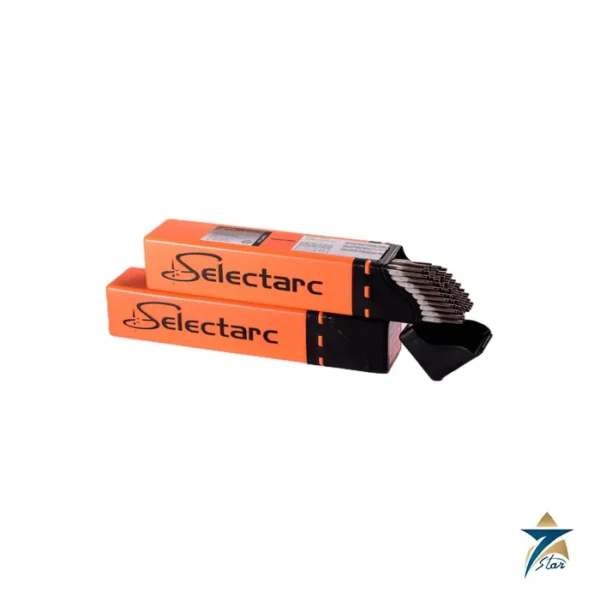
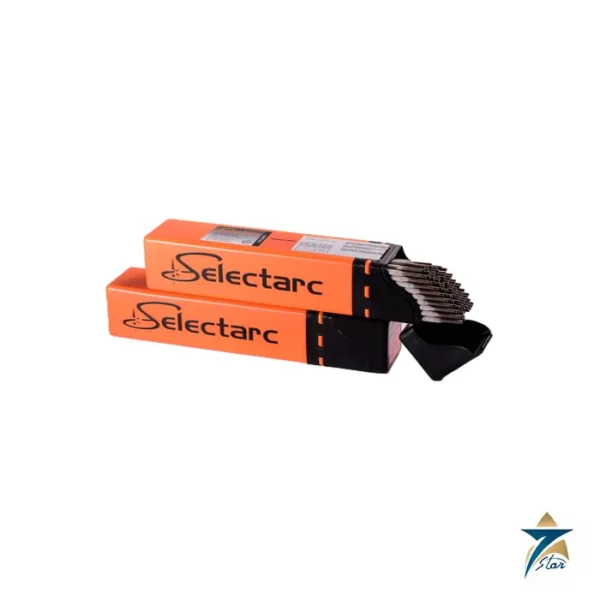
The Selectarc Ni276 is a basic coated electrode with an alloyed core wire that deposits alloy C-276 type weld metal. It is classified AWS A5.11 ENiCrMo-4, ISO 14172 E-Ni 6276 (NiCr15Mo15Fe6W4), UNS W80276, material number 2.4887. With about 16% chromium, 16% molybdenum and 4% tungsten, the deposit is among the most corrosion-resistant nickel alloys available for stick welding.
Selectarc describes high resistance in sulphurous acid environments, in highly concentrated chloride media and in the presence of oxidising salts such as ferric and cupric chlorides. The electrode offers a stable arc, regular droplet transfer, an easily watched weld pool and a neat bead appearance.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / Ni276 |
| Process |
SMAW (manual metal arc) |
| AWS classification |
A5.11 ENiCrMo-4 |
| ISO classification |
14172 E-Ni 6276 (NiCr15Mo15Fe6W4) |
| UNS / material number |
W80276 / 2.4887 |
| Coating |
Basic, alloyed core wire |
| Typical weld metal, % |
C under 0.02, Si 0.2, Mn 0.6, Cr 16.2, Mo 16.0, W 4.0, Fe 5.0, V 0.15, Ni remainder |
| Yield strength Rp0.2 |
Above 450 MPa |
| Tensile strength Rm |
Above 720 MPa |
| Elongation A5 |
Above 30% |
| Impact energy KV |
Above 70 J at +20 °C |
| Sizes and current |
2.5 × 300 mm, 50–70 A; 3.2 × 350 mm, 70–100 A; 4.0 × 350 mm, 90–120 A |
| Current type |
DC, electrode positive |
| Redrying |
2 h at 250–300 °C |
Applications in process plant and offshore
Selectarc lists offshore components, boilers, containers and piping systems in chemical and petrochemical plants, together with flue gas desulphurisation units, as the main fields of use. Base metals named on the data sheet are alloy C-276 (N10276, 2.4819), C-4 (N06455, 2.4610), alloy 625 (N06625, 2.4856), alloy 825 (N08825, 2.4858) and the 6Mo superaustenitic steel 254SMo (N08926, 1.4529).
Because the deposit is more highly alloyed in molybdenum than alloy 625 weld metal, ENiCrMo-4 is often chosen when joining superaustenitic or 625 components that will see hot, acidic chloride service. It is also a common option for overlays and repairs on equipment already built from C-276. For general alloy 625 fabrication, see the related Selectarc Ni625 ENiCrMo-3 electrode.
Welding technique for Ni-Cr-Mo alloys
Nickel alloy weld pools are sluggish and do not wet out like steel, so joint preparation and technique matter. Selectarc asks for clean joints free of grease and cracks, a slight electrode inclination and a short arc. Heat input should be kept low by stringer beads, with weaving limited to twice the core wire diameter. Redry the electrodes for 2 hours at 250–300 °C.
Wider bevel angles than those used for carbon steel help the filler reach the sidewalls, and grinding between passes removes oxide and slag that could cause lack of fusion. Keep the interpass temperature low; preheating is not normally applied to nickel-base alloys.
When C-276 type filler is used on dissimilar joints, for example a superaustenitic pipe to a carbon steel flange, the dilution from the steel side lowers the alloy content of the first layers. Buttering the steel face and keeping penetration controlled are common ways to protect corrosion performance at the fusion line, and the procedure should be qualified on the real material pairing.
Documents and quotation
Download the Selectarc Ni276 data sheet below. Other grades are listed in our Welding Electrodes category.
Send the diameter, quantity and certificate requirements to receive a quotation.

Reviews
There are no reviews yet.