Matching SAW wire for grade 91 creep-resisting steel
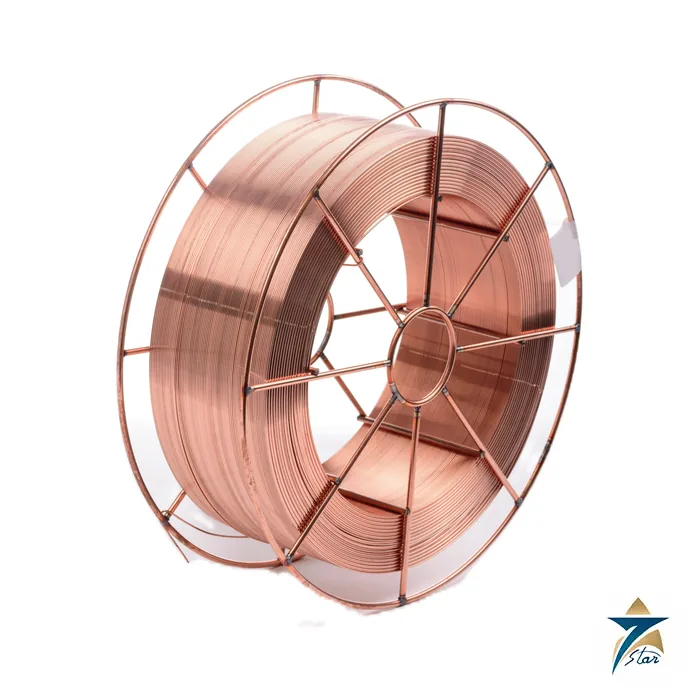
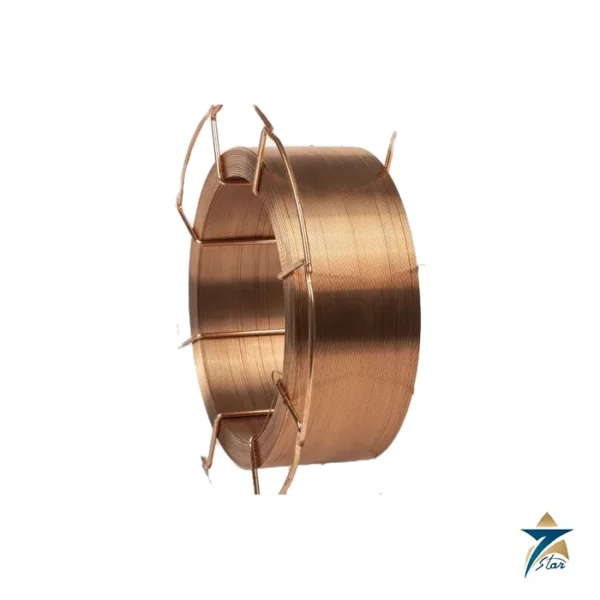
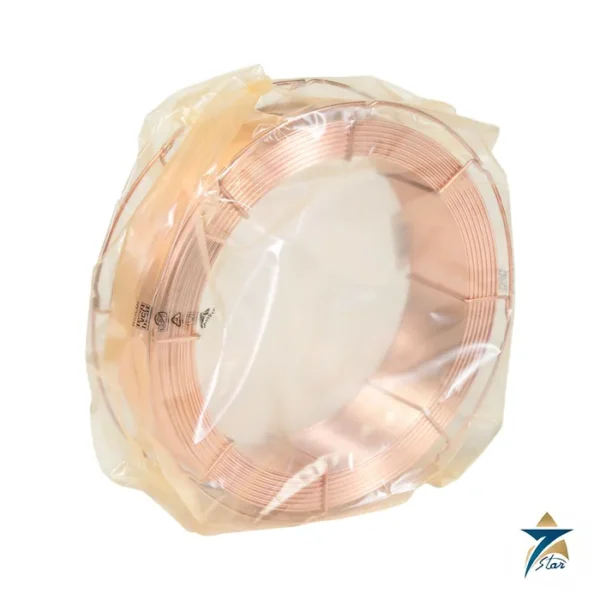
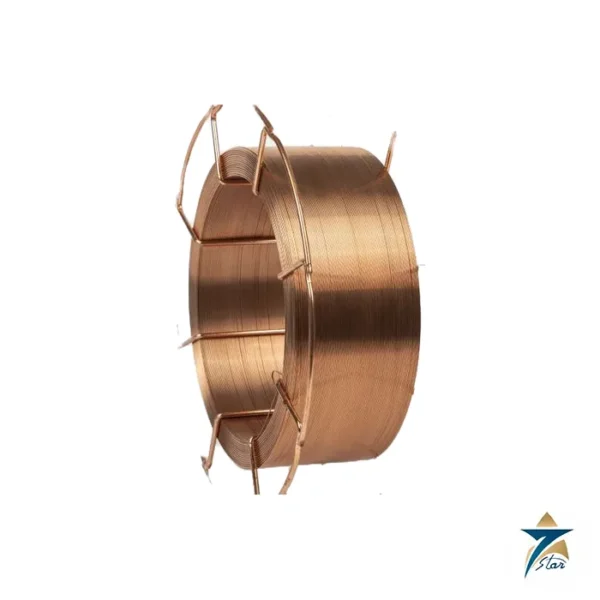
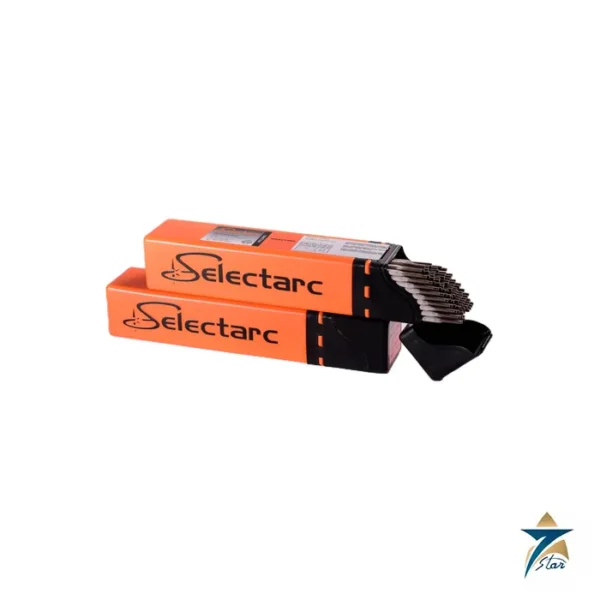
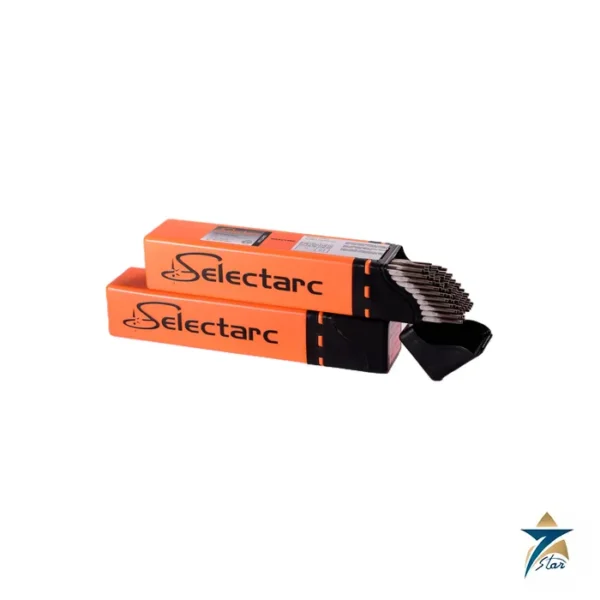
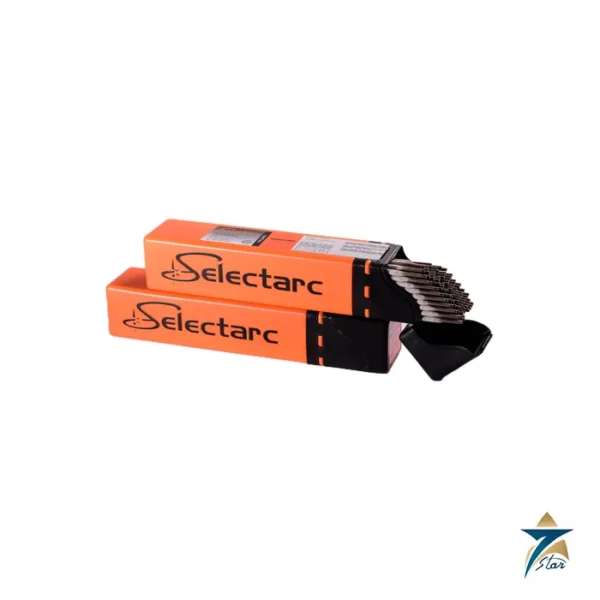
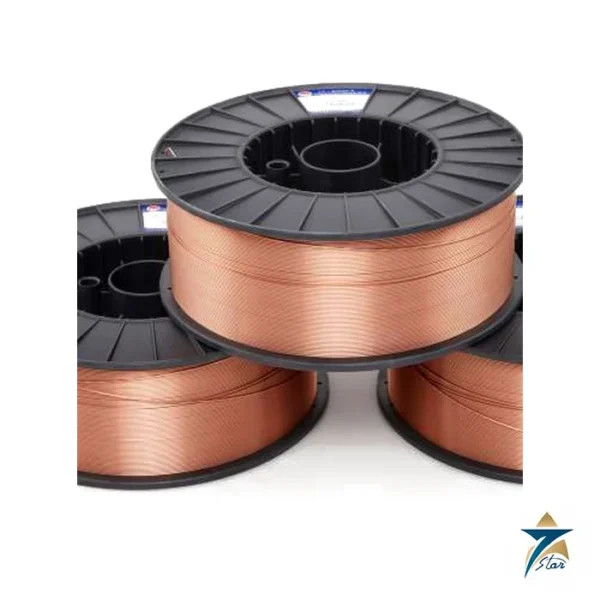
The Selectarc UP P91 is a solid wire for submerged arc welding of 9% chromium – 1% molybdenum creep-resisting steels such as P91, for service temperatures up to 650 °C. It is classified AWS A5.23 EB91 and ISO 24598-A S S CrMo91. Microalloying with niobium, vanadium and nitrogen improves creep resistance, matching the modified 9Cr-1Mo design of the base metal.
Selectarc names the chemical and petrochemical industries as main users. Grade 91 is also standard in power plant steam piping and headers, and in refinery heater and hydroprocessing equipment where its strength at temperature allows thinner walls than older 2.25Cr-1Mo designs.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / UP P91 |
| Process |
SAW (submerged arc) |
| AWS classification |
A5.23 EB91 |
| ISO classification |
24598-A S S CrMo91 |
| Wire composition, min–max % |
C 0.07–0.13, Si max 0.50, Mn 0.40–1.25, Cr 8.50–10.50, Ni 0.40–1.00, Mo 0.85–1.15, Cu max 0.10, Nb 0.03–0.10, V 0.15–0.25, N 0.03–0.07, Al max 0.04, P max 0.010, S max 0.010 |
| Typical wire composition, % |
C 0.10, Si 0.32, Mn 0.50, Cr 8.7, Ni 0.60, Mo 1.0, Nb 0.04, V 0.20, N 0.04 |
| Parameters, 2.4 mm |
200–400 A, 25–30 V, stick-out 18 mm, 40–60 cm/min |
| Parameters, 3.2 mm |
300–500 A, 28–32 V, stick-out 20 mm, 40–60 cm/min |
| Parameters, 4.0 mm |
500–700 A, 30–35 V, stick-out 22 mm, 50–60 cm/min |
| Current type |
AC or DC electrode positive |
| Recommended flux |
UP WP380 |
| Maximum service temperature |
650 °C |
Base materials
Listed parent metals are EN X10CrMoVNb9-1 and the ASTM grades A182 / A336 F91 forgings, A213 T91 tube, A217 C12A castings, A234 WP91 fittings, A335 P91 pipe and A387 Gr 91 plate. The wire is therefore suitable for longitudinal and circumferential seams in thick-walled P91 pipe, headers and pressure vessels.
The data sheet gives a combined Mn + Ni limit, shown as A/T, of 0.50 max, and nickel itself is kept low. This matters because manganese and nickel lower the Ac1 transformation temperature; if Ac1 drops too far, the post-weld heat treatment can partly re-austenitise the weld and leave untempered martensite.
Preheat, interpass and PWHT for grade 91
Grade 91 welds are martensitic and need strict thermal control. General practice is a preheat in the region of 200 to 250 °C, an interpass maximum agreed in the WPS, cooling below the martensite finish temperature before PWHT, and tempering typically around 740 to 770 °C. These values come from codes and the qualified procedure, not from this wire data sheet, so always follow the approved WPS.
Hardness checks after PWHT confirm adequate tempering. Weld metal toughness of 9Cr-1Mo SAW deposits is sensitive to flux basicity and oxygen pick-up; Selectarc names UP WP380 as the partner flux. Keep flux dry, use clean wire, and avoid excessive heat input, which coarsens the structure and can lower impact energy.
Dissimilar joints between grade 91 and lower-alloy Cr-Mo or stainless components need special attention to carbon migration and to PWHT temperatures that suit both sides. Where such joints are unavoidable, the filler choice and heat treatment should be set by the welding engineer for that specific combination.
Documents and quotation
The Selectarc UP P91 data sheet is attached for download. Browse more wires in our SAW Wire category.
For a quotation, send wire diameter, packaging, quantity and certificate requirements.

Reviews
There are no reviews yet.