25 9 4 wire for super duplex seams and cladding
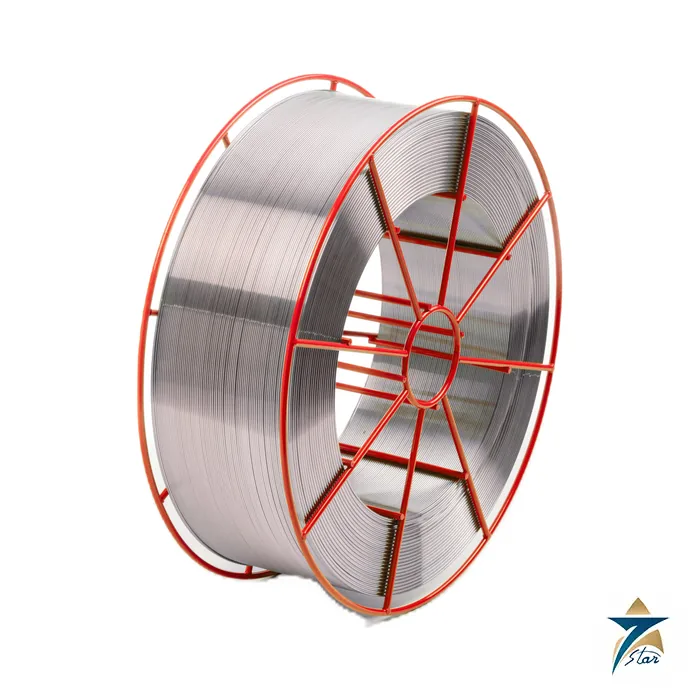
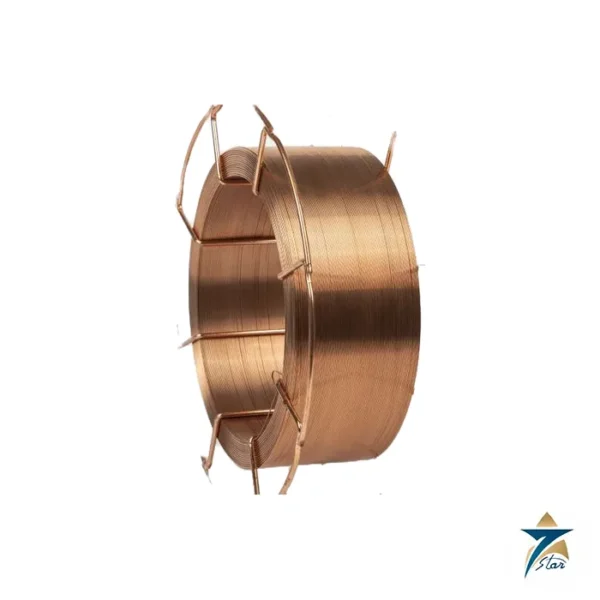
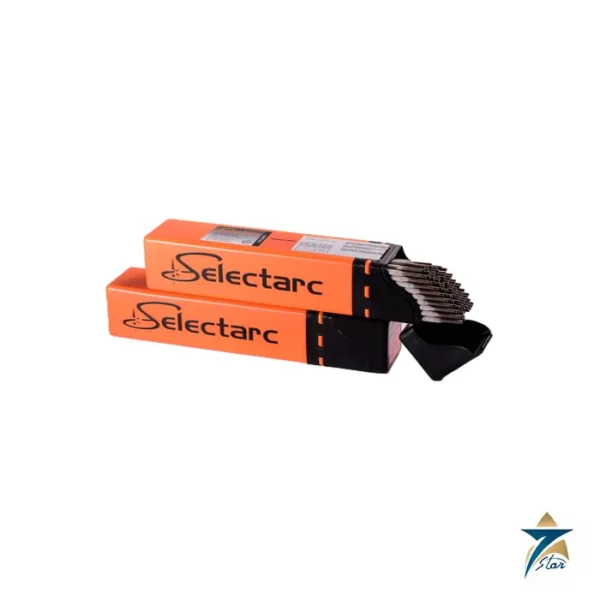
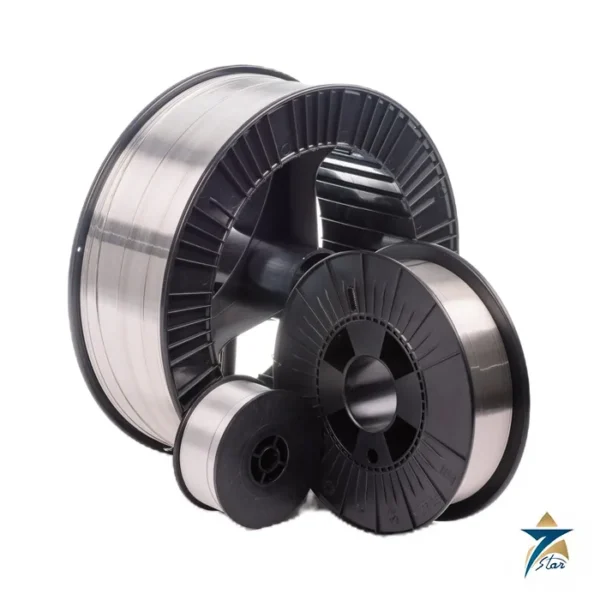
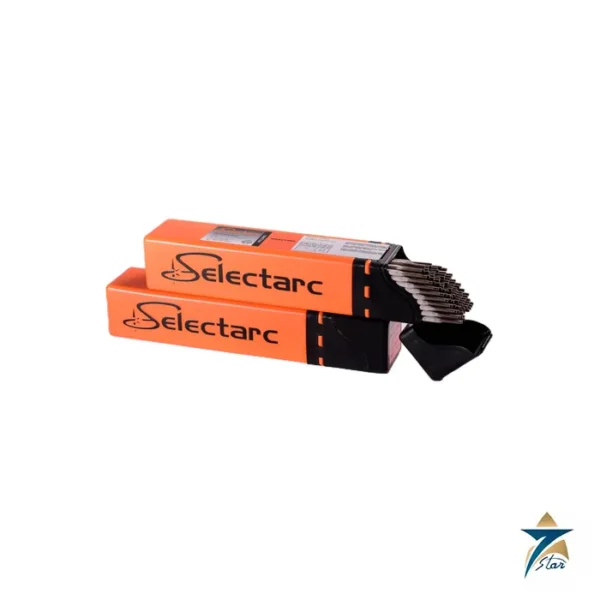
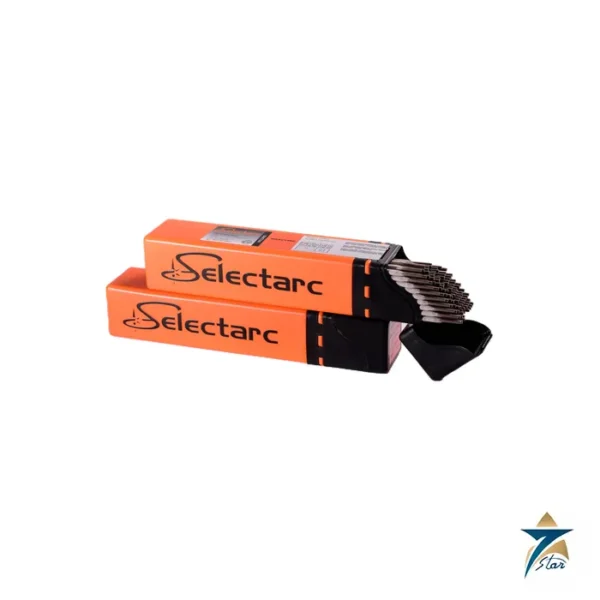
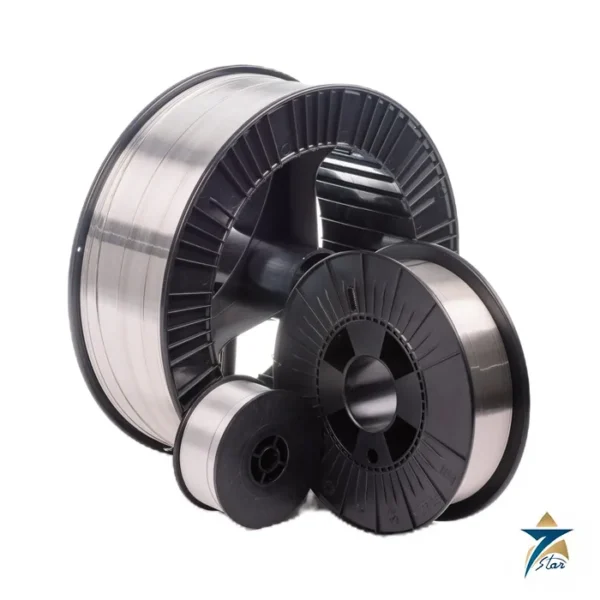
The Selectarc UP 2509 is a low-carbon solid wire for submerged arc welding of duplex and super duplex stainless steels. Classified AWS A5.9 ER2594 and ISO 14343-A S 25 9 4 N L, it has a typical analysis of 25.5% chromium, 9.2% nickel, 4.0% molybdenum and 0.25% nitrogen, the composition used to give super duplex weld metal its high resistance to localised corrosion.
Selectarc states resistance in chloride-bearing media against pitting, crevice and stress corrosion, use at service temperatures up to +250 °C, and main applications in pumps, vessels and piping. The wire suits long seams in thick plate and pipe, where SAW productivity offsets the extra set-up compared with manual welding.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / UP 2509 |
| Process |
SAW (submerged arc) |
| AWS classification |
A5.9 ER2594 |
| ISO classification |
14343-A S 25 9 4 N L |
| Wire composition, min–max % |
C max 0.03, Si max 1.0, Mn max 2.5, Cr 24.0–27.0, Ni 8.0–10.5, Mo max 4.5, Cu max 1.5, W max 1.0, N 0.20–0.30, P max 0.03, S max 0.02 |
| Typical wire composition, % |
C 0.012, Si 0.50, Mn 0.60, Cr 25.5, Ni 9.2, Mo 4.0, Cu 0.10, N 0.25, Fe remainder |
| Parameters, 2.4 mm |
340–380 A, 28–29 V, stick-out 18 mm, 48–60 cm/min |
| Parameters, 3.2 mm |
360–430 A, 28–29 V, stick-out 20 mm, 48–60 cm/min |
| Parameters, 4.0 mm |
450–550 A, 28–30 V, stick-out 22 mm, 50–60 cm/min |
| Current type |
DC, electrode positive |
| Recommended flux |
UP WP380M |
| Maximum service temperature |
+250 °C |
Listed parent metals
The data sheet names the super duplex grades UNS S32750 (2507, X2CrNiMoN25-7-4, 1.4410), S32760 (X2CrNiMoCuWN25-7-4, 1.4501), S32550 (G-X2CrNiMoCuN26-6-3, 1.4517) and the 52N+ grade 1.4507, together with standard duplex S31803 (1.4462), lean duplex S32304 (1.4362) and S32900 (1.4460).
Super duplex is widely specified for seawater injection, firewater and cooling water systems, subsea manifolds and process vessels handling chloride-rich produced water. The 25 9 4 filler keeps the weld PREN at the level of the parent metal, which a 22 9 3 wire cannot do. On standard 2205 the higher-alloyed wire may also be chosen where the client asks for extra corrosion margin in the weld.
Heat input and quality control
The heat input of SAW is high, and super duplex is sensitive to sigma and chi phase formation when the weld region spends too long between about 700 and 1000 °C. Practical controls are moderate current within the published windows, limited bead size, a firm interpass temperature limit agreed in the WPS, and avoiding very slow travel speeds. Selectarc gives travel speeds of 48 to 60 cm/min for all diameters.
Weld metal properties in SAW depend on the wire-flux pairing, so mechanical and corrosion results must come from the qualified combination with UP WP380M or another approved flux. Super duplex procedure tests typically include ferrite measurement, low-temperature Charpy tests, microstructural examination for intermetallics and an ASTM G48 pitting test. Keep the flux dry and recycle it only after removing fines and slag.
Documents and quotation
The Selectarc UP 2509 data sheet is attached for download. See more wires in our SAW Wire category.
Send the wire diameter, packaging, quantity and certificate requirements for a quotation.

Reviews
There are no reviews yet.