Duplex solid wire for high-deposition submerged arc welding
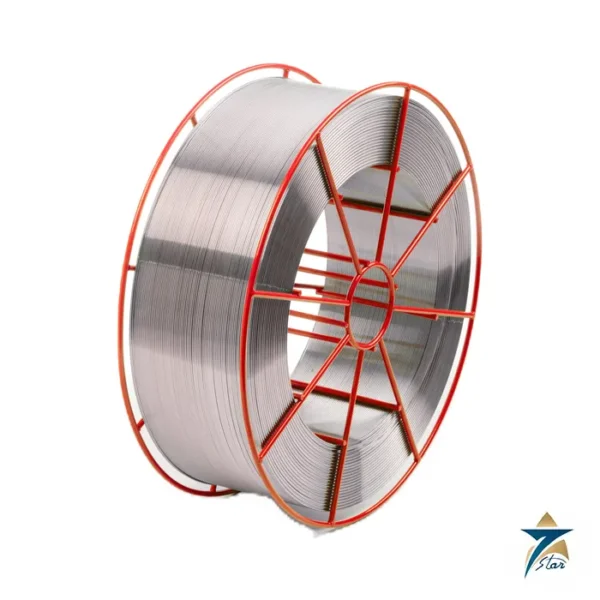
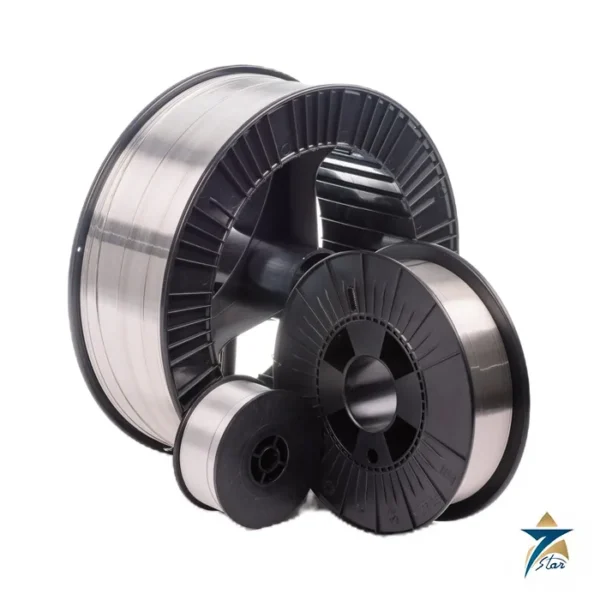
The Selectarc UP 2209 is a low-carbon solid wire for submerged arc welding of austenitic-ferritic (duplex) stainless steels such as 2205 and 2304. It is classified AWS A5.9 ER2209 and ISO 14343-A S 22 9 3 N L, and the data sheet gives a pitting resistance equivalent number above 35.
The weld deposit resists pitting, crevice corrosion and stress corrosion cracking in chloride-containing media and can be used at service temperatures up to +250 °C. Selectarc names pumps, vessels and piping systems as the main applications, together with other components that need high strength combined with corrosion resistance. Submerged arc welding brings the duplex chemistry to thick longitudinal and circumferential seams at far higher deposition rates than manual processes.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / UP 2209 |
| Process |
SAW (submerged arc) |
| AWS classification |
A5.9 ER2209 |
| ISO classification |
14343-A S 22 9 3 N L |
| Wire composition, min–max % |
C max 0.03, Si 0.50–0.90, Mn max 2.00, Cr 21.5–23.5, Ni 7.5–9.5, Mo 2.5–3.5, Cu max 0.5, N 0.10–0.20, P max 0.03, S max 0.02 |
| Typical wire composition, % |
C 0.012, Si 0.40, Mn 1.5, Cr 23.1, Ni 8.7, Mo 3.2, N 0.14 |
| PREN |
Above 35 |
| Parameters, 2.4 mm |
340–380 A, 28–29 V, stick-out 18 mm, 48–60 cm/min |
| Parameters, 3.2 mm |
360–430 A, 28–29 V, stick-out 20 mm, 48–60 cm/min |
| Parameters, 4.0 mm |
450–550 A, 28–30 V, stick-out 22 mm, 50–60 cm/min |
| Current type |
DC, electrode positive |
| Recommended fluxes |
UP WP380M, UP INOX L, UP INOX 620 |
| Maximum service temperature |
+250 °C |
Base metals and flux pairing
Listed base metals are UNS S31803 (X2CrNiMoN22-5-3, 1.4462), S32304 (X2CrNi23-4, 1.4362) and S32900 (329, 1.4460). The Selectarc sheet pairs the wire with its UP WP380M, UP INOX L and UP INOX 620 fluxes. Because the final weld metal chemistry and mechanical properties in SAW depend on the wire-flux combination, they should be confirmed from the flux data or from procedure qualification, rather than from wire analysis alone.
For duplex, a neutral or slightly basic stainless steel flux that does not burn off nitrogen or add excessive oxygen is preferred, since both affect phase balance and toughness. Clad plate and super duplex parts call for different combinations; Selectarc also offers the 25 9 4 type UP 2509 wire for super duplex.
Getting the phase balance right in SAW
Submerged arc welding uses high heat input, so the main risk on duplex is slow cooling that encourages intermetallic phases, especially in thick multi-pass joints. Keep interpass temperature modest, avoid very large beads and use the smaller wire diameters for root-side and thinner work. Dilution from the base metal is higher than in manual processes, which helps ferrite control but also means the weld chemistry follows the plate more closely.
Procedure qualification for duplex vessels and piping commonly includes ferrite measurement, impact testing at low temperature and a corrosion test such as ASTM G48. Store flux in dry conditions and rebake it according to the flux manufacturer before use.
Documents and quotation
Download the Selectarc UP 2209 data sheet attached to this page. Further wires are listed in our SAW Wire category.
For a quotation, send wire diameter, spool or coil type, quantity and certificate requirements.

Reviews
There are no reviews yet.