High-recovery electrode for fast fillet welding of heavy steel
The Hyundai Welding S-7024.F is a high-recovery stick electrode classified AWS A5.1 / ASME SFA-5.1 E7024, EN ISO 2560-A E42 0 RR 7 4, JIS Z 3211 E4924 and KS D7004 E4324. The manufacturer lists highly efficient fillet welding, high welding speed, good bead appearance and easy slag removal, with heavy steel fabrication and shipbuilding as the application areas.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Hyundai Welding / S-7024.F |
| Process |
SMAW, high recovery |
| AWS classification |
A5.1 / SFA-5.1 E7024 |
| EN ISO classification |
2560-A E42 0 RR 7 4 |
| JIS / KS |
Z 3211 E4924 / D7004 E4324 |
| Polarity |
AC or DC +/- |
| Welding positions |
1G, 2F |
| Redrying |
70-100 °C (158-212 °F) for 0.5-1 h |
| Weld metal, typical % |
C 0.06, Si 0.37, Mn 0.69, P 0.021, S 0.009 |
| Yield strength |
477 MPa (69 ksi) |
| Tensile strength |
556 MPa (81 ksi) |
| Elongation |
24% |
| Impact toughness |
61 J (45 ft-lbs) at 0 °C |
| 3.2 x 400 mm |
100-150 A, flat and horizontal fillet |
| 4.0 x 450 mm |
140-200 A |
| 4.5 x 450 / 700 mm |
180-230 A |
| 5.0 x 450 / 700 mm |
200-250 A |
| 6.0 x 450 / 700 mm |
260-300 A |
| Packaging |
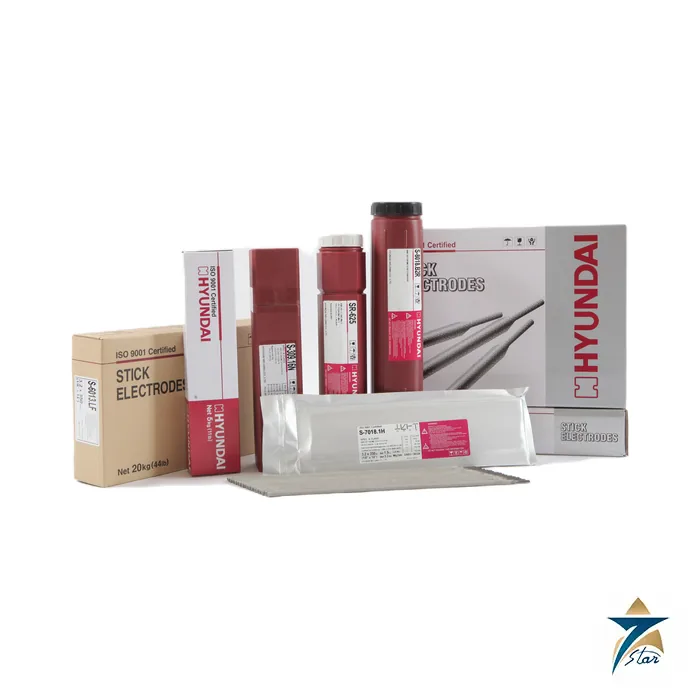
Standard or vacuum packet 5 kg; carton 20 kg |
| Approvals listed |
ABS, DNV, LR, NK, CWB |
What the E7024 class is meant for
E7024 electrodes carry a thick iron-powder coating that lets the welder drag the electrode lightly along the joint in contact with the work. The extra metal in the coating raises deposition, so one electrode lays more weld than a conventional type of the same diameter. The class is restricted to flat and horizontal fillet positions, which is why the Hyundai Welding sheet shows only 1G and 2F.
For vertical-up, overhead or root work you need another class entirely, such as an E6010 or E7018 type. Within its scope the S-7024.F is an economical choice for long fillet seams on heavy plate in a shop or yard.
Using it well
Pick the diameter from leg length and plate thickness: the 3.2 mm electrode suits small fillets at 100 to 150 A, while 6.0 mm at 260 to 300 A deposits heavy fillets in few passes. The 700 mm lengths reduce the number of electrode changes on long joints. Keep the arc short with the coating resting on the work, and keep the packs dry; the redrying window of 70 to 100 °C for up to an hour is modest because the coating is not highly hygroscopic.
The manufacturer gives no low-temperature requirement beyond the 0 °C result of 61 J, so for service colder than that choose an electrode with a specified colder impact test.
Documents and quotation
The Hyundai Welding S-7024.F catalog sheet is attached to this page for download. Related consumables are listed in our Welding Electrodes category. A related published low-hydrogen page is Hyundai Welding S-7018.1.
For a quotation, send the diameter or size, pack type, quantity and any certificate or approval requirement.

Reviews
There are no reviews yet.