Promass G 100: compact Coriolis flowmeter for high-pressure liquids and gases
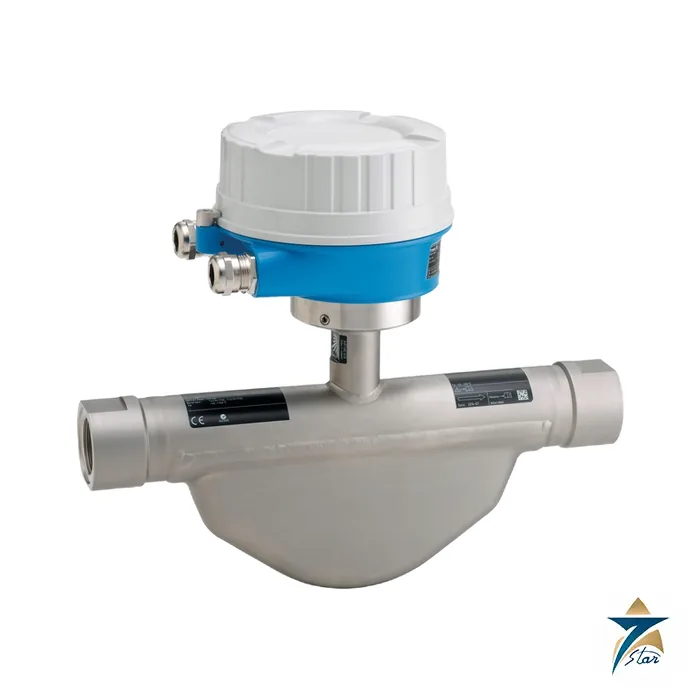
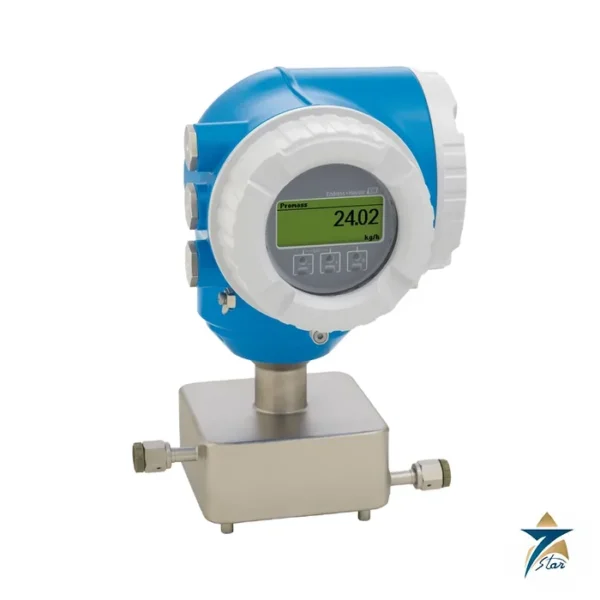
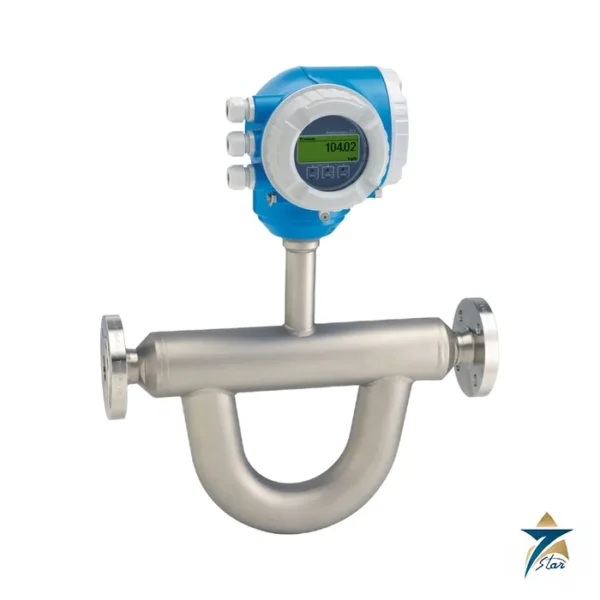
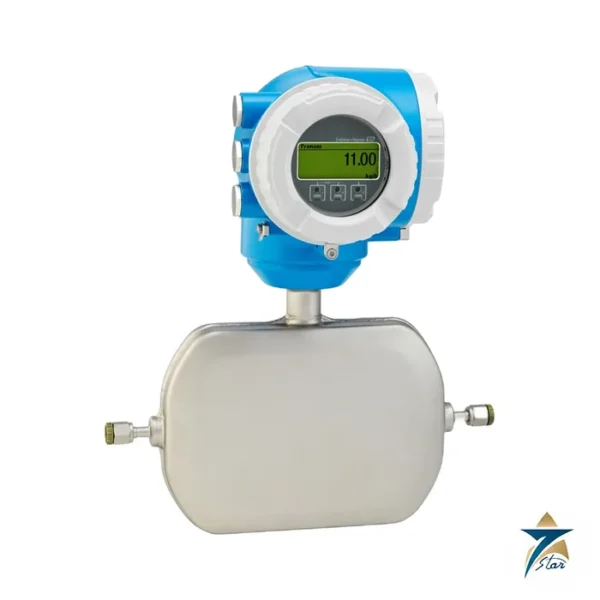
The Endress+Hauser Promass G 100 is a Coriolis mass flowmeter built for small-bore, high-pressure lines. It combines a curved 316L measuring tube with an ultra-compact Proline 100 transmitter, so mass flow, density, temperature and derived volume flow come from one device. The Promass G 100 is rated for process pressure up to 350 bar and sits in the 8G1B product root with cylindrical internal BSPP threads, which makes it a practical choice for skids, injection packages and test rigs where space is short.
Because the measuring principle responds to mass rather than to velocity, the Promass G 100 does not depend on viscosity or density of the medium, and it needs no straight inlet or outlet runs. Seven Star LLC supplies Endress+Hauser instrumentation in Oman and the GCC as an independent supplier based in Muscat, and can help check a Promass G 100 selection against your process data.
Promass G 100 technical specifications
| Parameter |
Specification |
| Manufacturer / part number |
Endress+Hauser Promass G 100 (product root 8G1B, internal-thread version) |
| Measuring principle |
Coriolis |
| Measured variables |
Mass flow, density, temperature, volume flow, corrected volume flow, reference density |
| Nominal diameter |
DN 8 to 25 (3/8 to 1 in.) |
| Measuring range (full scale) |
0 to 18 000 kg/h (0 to 662 lb/min) at DN 25 |
| Max. measured error, liquids |
Mass flow and volume flow ±0.15 % of reading |
| Max. measured error, gases |
Mass flow ±0.75 % of reading |
| Density, liquids |
±0.0005 g/cm³ at reference conditions (±0.02 g/cm³ with standard density calibration) |
| Repeatability |
±0.075 % (liquid mass flow), ±0.35 % (gas mass flow), ±0.00025 g/cm³ (liquid density) |
| Medium temperature |
–50 to +150 °C (–58 to +302 °F) |
| Max. process pressure |
350 bar (5080 psi) |
| Wetted materials |
Measuring tube 1.4435 (316L); process connection 1.4404 (316/316L) |
| Sensor housing |
1.4301 (304), corrosion resistant |
| Ambient temperature |
–40 to +60 °C non-Ex; option –50 to +60 °C |
| Degree of protection |
IP66/67, type 4X enclosure |
| Outputs |
4–20 mA HART (active); pulse/frequency/switch (passive) |
| Digital communication |
HART, Modbus RS485, EtherNet/IP, PROFIBUS DP, PROFINET |
| Power supply |
DC 20 to 30 V |
| Process connection |
Cylindrical internal thread BSPP (G) to ISO 228-1; seal not included |
How the Promass G 100 measures mass flow and density
Inside the sensor the measuring tubes are driven to oscillate at their natural frequency. When fluid flows through the oscillating tubes, Coriolis forces twist them slightly and the phase shift between two sensing points is proportional to mass flow. The oscillation frequency itself gives density, and an integrated temperature sensor compensates the tube. The transmitter then derives volume flow, corrected volume flow and reference density from these three primary values.
The high oscillation frequency of the tubes makes the Promass G 100 largely insensitive to pipe vibration in normal plant conditions. A zero point is set at the factory under reference conditions, so a field zero adjustment is normally unnecessary and is mostly useful when you need best accuracy at very low flow.
Promass G 100 nominal sizes and flow ranges
Three sensor sizes are offered. The full-scale values below are the 1:1 flow figures from the manufacturer technical information, together with the zero point stability and compact-version weight for each size.
| Size |
Full scale (1:1) |
Zero point stability |
Weight, compact |
| DN 8 (3/8 in.) |
2 000 kg/h |
0.20 kg/h |
3.8 kg |
| DN 15 (1/2 in.) |
6 500 kg/h |
0.65 kg/h |
4.4 kg |
| DN 25 (1 in.) |
18 000 kg/h |
1.80 kg/h |
5.1 kg |
For sizing, the manufacturer suggests 20 to 50 % of maximum full scale as ideal, with about one twentieth as the lowest recommended value. For abrasive liquids with entrained solids, choose a lower full scale so that velocity stays under 1 m/s. For gases, velocity in the tubes should not exceed half the speed of sound, so maximum mass flow depends on gas density.
Promass G 100 transmitter, communication and system fit
The Promass G 100 uses an ultra-compact transmitter housing with a pre-configured plug connector and an optional four-line backlit display. The display is for reading only, and configuration is done through the integrated web server in a browser or with operating tools. Digital communication options are HART, Modbus RS485, EtherNet/IP, PROFIBUS DP and PROFINET, depending on the order code. Power is DC 20 to 30 V.
Heartbeat Technology is available for in-situ verification of the device and its traceability. The manufacturer states calibration is carried out on accredited rigs to ISO/IEC 17025, and 3.1 material certificates can be ordered. Hazardous-area approvals listed for the family include ATEX, IECEx and cCSAus; confirm the exact approval against the order code before purchase, since they depend on the selected output and housing.
The Promass G 100 is the compact high-pressure member of the Proline Promass 100 range. For skid builders the key advantage is that a single Promass G 100 replaces a flowmeter, a density meter and a temperature point.
A separate Safety Barrier Promass 100 is used for intrinsically safe connection of the measuring device in hazardous areas, with a shielded twisted-pair connecting cable and a maximum cable resistance of 2.5 Ω on one side. Tell us if the plant needs the hazardous-area version so the correct barrier and cable are quoted together.
Selecting a Promass G 100: ordering checklist
- Fluid: liquid or gas, density, viscosity, and any entrained solids or gas bubbles.
- Flow range: minimum, normal and maximum mass flow so the right DN 8, 15 or 25 is chosen.
- Process pressure and temperature, including pressure peaks, against the 350 bar and –50 to +150 °C limits.
- Thread type needed on the pipe side; the sensor has internal BSPP threads and the profile or copper seal is not in the scope of delivery.
- Rupture disc: required or not for the pressure case, noting the label that must stay visible.
- Output and fieldbus: HART with pulse output, Modbus, EtherNet/IP, PROFIBUS DP or PROFINET.
- Display, cable entry thread (M20, G 1/2 or NPT 1/2), and any hazardous-area approval.
Installing and commissioning the Promass G 100
Install the sensor so the arrow on the nameplate matches flow direction. Avoid the highest point of the pipeline and a position directly upstream of a free outlet in a down pipe, because gas bubbles collecting in the tube cause errors. With the curved tube, the manufacturer advises against the orientation that traps solids for dirty liquids and against the orientation that traps gas for outgassing liquids.
If a rupture disc is fitted, make sure nothing obstructs its operation; its position is marked by a sticker that is destroyed if the disc triggers, so it can be inspected visually. The disc triggering pressure in the housing is 10 to 15 bar. Use shielded cable for HART and ground the shield per the plant concept. Valves, elbows and tees nearby do not require special straight runs unless cavitation can occur.
Typical Promass G 100 applications in Oman and the GCC
In oil and gas, the Promass G 100 suits chemical injection skids, methanol and glycol dosing, gas lift and well-test packages where pressure is high and lines are small. Desalination and power plants use compact Coriolis meters for antiscalant, hypochlorite and fuel additive dosing, where mass-based measurement avoids density corrections. Petrochemical sites use them for catalyst, inhibitor and sample-loop duties.
The stainless steel sensor housing and IP66/67 transmitter cope with Gulf heat, dust and humidity when the unit is shaded and cable glands are sealed.
Information to send with a Promass G 100 RFQ
- Fluid name, composition, density range and viscosity.
- Mass flow minimum, normal, maximum; operating pressure and temperature.
- Line size and thread standard on both ends, plus orientation and available space.
- Output type, fieldbus, power supply and display requirement.
- Hazardous-area classification and approval needed.
- Whether a rupture disc, Heartbeat verification or 3.1 certificates are wanted.
- Quantity, delivery site and any existing order code to match.
Documents and quotation
A manufacturer technical information document for the Promass G 100 is attached on this page. It covers the measuring principle, dimensions, specifications and ordering structure, and it should be read together with the safety instructions that ship with the instrument.
To request a quotation, send the full order code from the nameplate or your datasheet, or describe the process data above. Seven Star LLC will confirm the specification and respond with availability for Oman and the GCC.
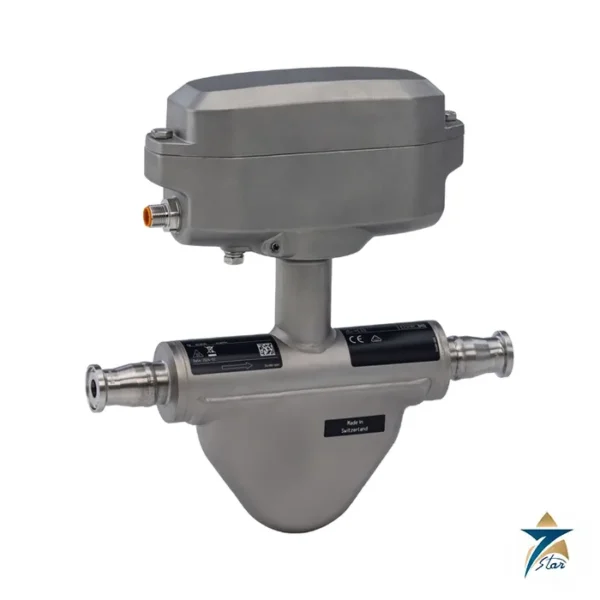
Other Models in the Promass Coriolis Range
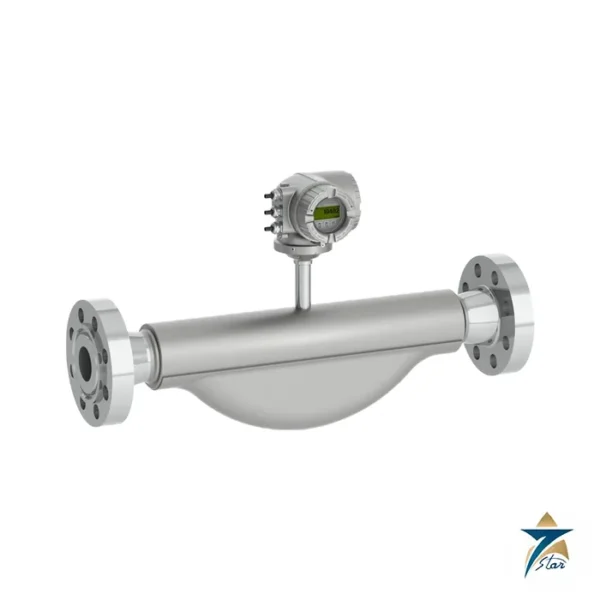
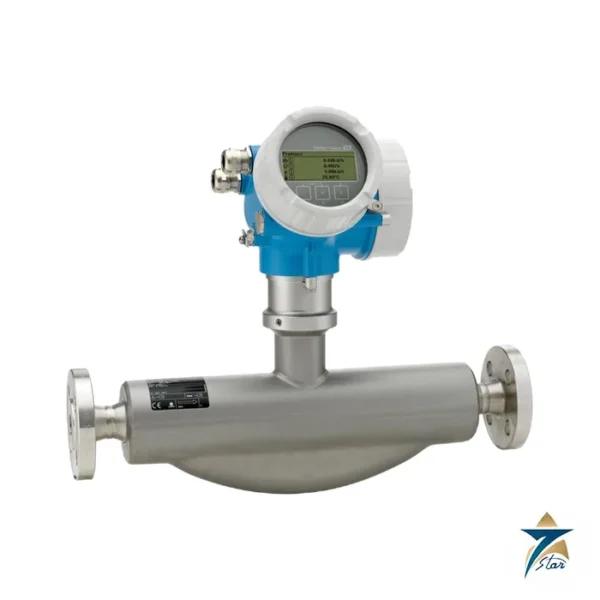
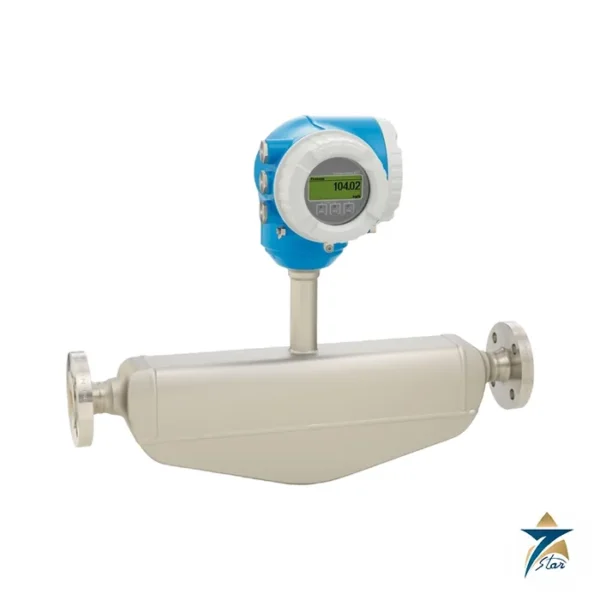
Seven Star LLC supplies models from the Promass Coriolis range in Oman and the GCC. Compare the related models below and request a quote for the one that matches your application.



















Reviews
There are no reviews yet.