High-current CO2 wire for deep penetration and fast deposition
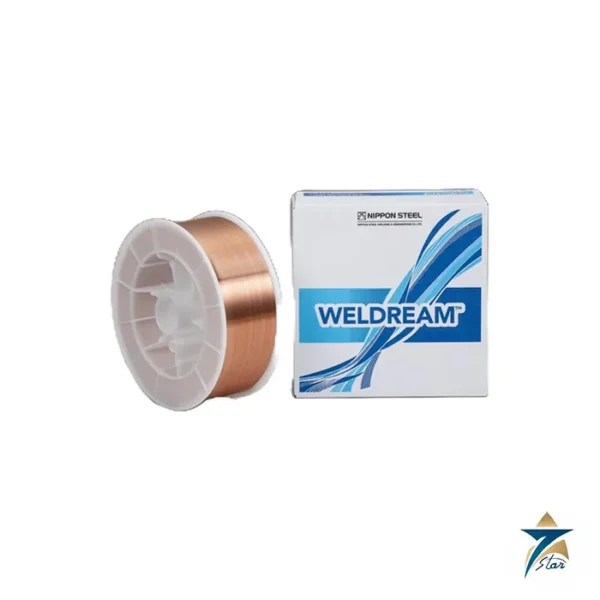
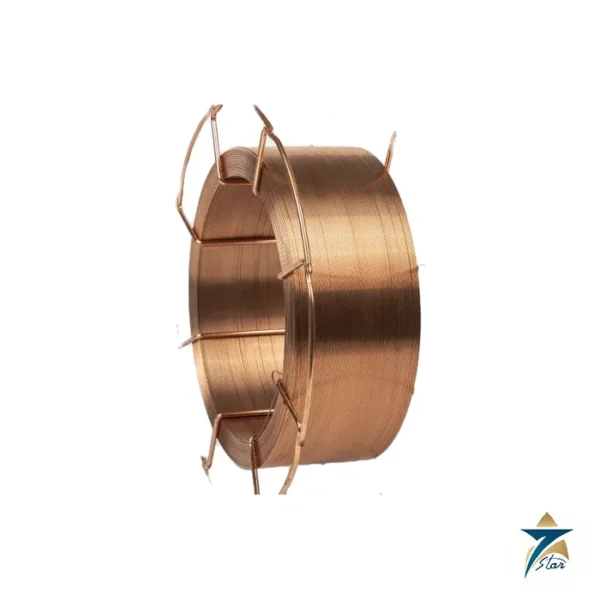
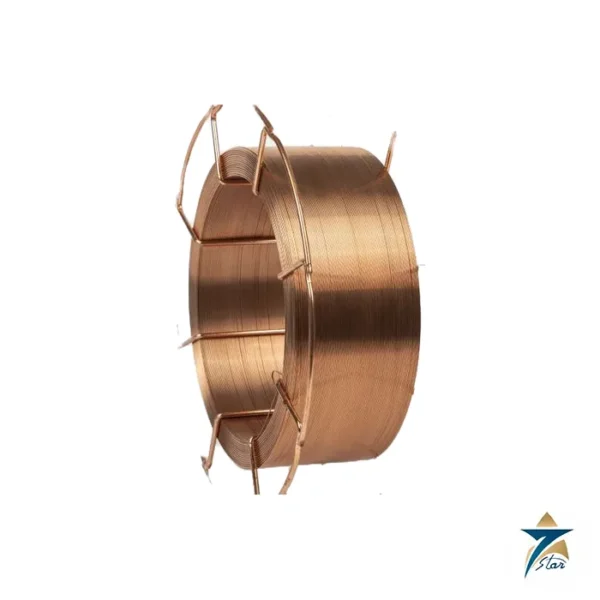
The Nippon Steel YM-26 is a solid wire for gas metal arc welding with CO2 shielding, classified JIS Z 3312 YGW11 and AWS A5.18 ER70S-G. Nippon Steel Welding & Engineering describes a stable arc and low spatter with excellent weldability even in the high current range, plus a high deposition rate and deep penetration.
It is used on mild steel and 490 MPa high tensile steel for automobiles, rolling stock, machinery, air conditioners, tools, light gauge steel, steel frames, bridges and ships.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Nippon Steel Welding & Engineering / YM-26 |
| Process |
GMAW, solid wire |
| AWS classification |
A5.18 ER70S-G |
| JIS classification |
Z 3312 YGW11 |
| Shielding gas |
CO2 |
| Polarity |
DC (+) |
| Typical weld metal, % |
C 0.07, Si 0.52, Mn 1.11, P 0.017, S 0.011, Ti 0.04 |
| As-welded properties |
YS 460 MPa, TS 560 MPa, El. 28%, Charpy 130 J at 0 °C |
| After PWHT 625 °C × 3 h |
YS 400 MPa, TS 510 MPa, El. 31%, Charpy 180 J at 0 °C |
| Current, flat |
1.0 mm 70–250 A; 1.2 mm 100–350 A; 1.4 mm 150–470 A; 1.6 mm 200–550 A; 2.0 mm 250–650 A |
| Current, horizontal / horizontal fillet |
1.0 mm 70–250 A; 1.2 mm 100–350 / 130–300 A; 1.4 mm 150–450 / 150–400 A; 1.6 mm 200–450 A |
| Positions |
Flat, horizontal fillet and horizontal |
| Wire extension |
20–30 mm |
When to pick YM-26
YGW11 wires in the JIS system are the high-current, titanium-bearing CO2 wires used for heavy fillet and butt welds in flat and horizontal positions. The listed range runs up to 650 A on 2.0 mm wire, which suits robotic and mechanised welding of thick sections. For thin plate and vertical-down work at low current, the sister wire YM-28 (ER70S-6, YGW12) is the better match.
The handbook includes post-weld heat treated properties at 625 °C for 3 hours, useful when a fabrication is stress relieved.
Heat input and interpass limits
For 490 MPa steel, the manufacturer limits heat input to a maximum of 30 kJ/cm and interpass temperature to 250 °C. Exceeding these on high tensile steel can reduce strength and toughness of the weld metal. Keep the wire extension between contact tip and base metal at 20–30 mm.
A high-current CO2 wire places demands on the equipment too. Check that the welding power source, torch and liners are rated for the current and duty cycle, and that the contact tip is changed before wear causes an unstable arc. On thick plate, multi-pass welds run at high current should still respect the interpass limit, so plan the pass sequence and cooling time accordingly.
Documents and quotation
The official product page link is given below. Browse our Solid Welding Wire category for related consumables.
For a quotation, send the diameter, package type (spool or pail) and weight, quantity and certificate requirements.
Nippon Steel YM-26 classification and typical properties
| Item |
Manufacturer data |
| JIS |
Z 3312 YGW11 |
| AWS |
A5.18 ER70S-G |
| Shielding gas |
CO2 |
| Positions |
Flat, horizontal fillet and horizontal |
| Weld metal chemistry (%) |
C 0.07, Si 0.52, Mn 1.11, Ti 0.04 |
| As welded |
YS 460 MPa, TS 560 MPa, El 28%, CVN 130 J at 0 °C |
| After PWHT 625 °C × 3 h |
YS 400 MPa, TS 510 MPa, El 31%, CVN 180 J at 0 °C |
Flat-position current ranges
| Diameter (mm) |
Current (A) |
| 1.0 |
70–250 |
| 1.2 |
100–350 |
| 1.4 |
150–470 |
| 1.6 |
200–550 |
| 2.0 |
250–650 |
How YM-26 works
YM-26 is a solid wire designed for high-current CO2 welding. The silicon and manganese deoxidise the weld pool, and the titanium addition helps refine the weld metal and stabilise the arc at high current. The result is high deposition and deep penetration, which suits heavy fillet and butt welds in the flat and horizontal positions. Because CO2 is low-cost and widely available, this combination is a productive choice for structural steel fabrication.
Selection and procedure guide for YM-26
- Choose YM-26 for high-current, high-deposition welding of mild steel and 490 MPa class steel in flat and horizontal positions.
- For 490 MPa class steel, Nippon Steel limits heat input to 30 kJ/cm and interpass temperature to 250 °C.
- Keep the wire stickout at 20–30 mm.
- For all-position work or thin sheet at low current, a wire such as YM-28 is often a better fit.
- The PWHT values above help when the structure will be stress relieved after welding.
Storage and maintenance
- Store spools and drums dry, away from condensation and corrosive fumes, to avoid rust on the wire surface.
- Inspect the contact tip, liner and drive rolls regularly; high-current work wears the tip faster.
- Clean mill scale, rust and paint from the joint to reduce porosity.
- Protect the gas shield from wind on outdoor jobs.
Typical YM-26 applications in Oman and the GCC
Steel structure fabricators, bridge and building contractors, tank builders and heavy equipment workshops in Oman and the GCC use high-current CO2 wires for columns, beams, box sections and base frames. YM-26 is well suited to robotic and mechanised welding lines as well as manual welding of thick plate where deposition rate matters.
Why source from Seven Star LLC
Seven Star LLC supplies MIG and MAG welding wire to fabricators and contractors across Oman and the GCC. Tell us the diameter, package type and quantity to request a quote; our team can help confirm the correct ordering code.
Practical tips for productive welding with YM-26
To get the most from the high deposition rate of YM-26, match the wire diameter to the joint and the power source. A 1.2 mm wire covers most manual fillet work, while 1.4 and 1.6 mm wires suit heavy plate and mechanised carriages that can sustain high currents. Increase the voltage with the current so the arc stays stable and spatter remains low. When welding 490 MPa class steel, watch the heat input on large multi-pass joints, because very wide weave beads at high current can exceed the 30 kJ/cm limit and reduce toughness. Check the interpass temperature with a contact thermometer or temperature crayon, and allow the joint to cool when it goes above 250 °C. Keep a written record of the parameters used on qualified procedures.

Reviews
There are no reviews yet.