
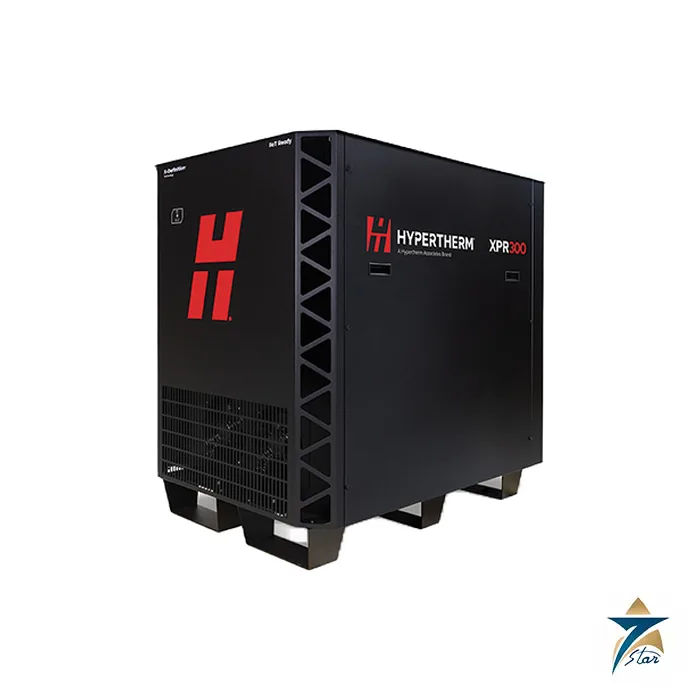
Hypertherm XPR300 X-Definition Mechanized Plasma Cutting System
Overview
The Hypertherm XPR300 is a 300 A X-Definition plasma system built for mechanized cutting on CNC tables, bevel heads and robotic cells. It is intended for steel service centres, heavy fabricators and plate processing lines that need consistent high-definition edge quality on mild steel together with capable stainless steel and aluminium cutting, all from one plasma source. The power supply delivers up to 66.5 kW, is rated at 100% duty cycle at that output, and is controlled entirely from the CNC, so cut parameters, gas selection and diagnostics are handled by the machine rather than by manual settings.
Seven Star LLC supplies the Hypertherm XPR300 to plate cutting and fabrication businesses in Oman and the GCC, with engineering support in Muscat. Because a mechanized plasma system must be matched to a cutting table, torch height control and gas supply, our engineers work through the console choice, torch lead lengths and integration questions with each customer before a quotation is finalised.
Operating Principle
Mechanized high-definition plasma works on the same basic physics as handheld air plasma but with far tighter control. A constricted arc is formed between the electrode and a precision nozzle, plasma gas is swirled through the nozzle to stabilise the arc, and a separate shield gas protects the cut and shapes the kerf. On the Hypertherm XPR300 the CNC selects oxygen, nitrogen, air, argon, F5 or hydrogen mixtures through the gas console according to material and thickness, and the power supply regulates current from low settings for thin sheet up to 300 A for heavy plate.
Hypertherm explains that advanced power-supply technology provides rapid feedback and automatically intervenes to eliminate events that reduce efficiency and consumable life. Its Arc response technology provides automatic torch and ramp-down error protection, which the manufacturer states increases consumable life three times that of competitor systems and reduces catastrophic electrode blowouts at high current. The practical result is a more consistent edge quality over the life of each set of consumables.
Hypertherm describes the cut quality of the Hypertherm XPR300 as X-Definition, a refinement of its earlier HyDefinition process. The manufacturer cites consistent ISO range 2 results on thin mild steel, extended ISO range 3 results compared with earlier plasma technology, improved stainless steel quality across all thicknesses and better aluminium edges with Vented Water Injection. For fabricators this means fewer parts sent for grinding or re-machining before welding, and a cleaner edge on bevels prepared directly on the Hypertherm XPR300 table.
Engineering Design of the Hypertherm XPR300
The power supply has a maximum open-circuit voltage of 360 VDC, an output voltage range of 50 to 210 VDC and a power factor of 0.98 at 66.5 kW. It is forced-air cooled with Class H insulation, operates from minus 10 to 40 °C ambient, and has a top lift eye rated to 680 kg. Diagnostic sensors in the power supply generate refined fault codes, and a web interface reachable through Wi-Fi or Ethernet LAN supports monitoring and service. Built-in IIoT connectivity through Ethernet and MTConnect allows remote data access.
Four gas console options set the process capability of the Hypertherm XPR300. Core and CorePlus consoles provide excellent mild steel performance, Vented Water Injection (VWI) adds water-injection cutting for stainless steel and aluminium, and OptiMix adds hydrogen, nitrogen and argon mixing for the widest stainless and aluminium range. The EasyConnect torch lead and one-hand torch-to-receptacle connection speed up change-outs, and the QuickLock electrode simplifies consumable replacement.
Key Features
Production managers evaluating the Hypertherm XPR300 typically focus on the following capabilities.
- A 66.5 kW output at 100% duty cycle supports continuous production cutting of heavy plate.
- Mild steel production pierce reaches 50 mm with argon assist and 45 mm with standard oxygen, with severance up to 80 mm.
- Stainless steel can be pierced to 38 mm and severed to 75 mm, while aluminium can be pierced to 38 mm and severed to 50 mm.
- Arc response technology protects against ramp-down errors and electrode blowouts, extending consumable life.
- Full CNC control of every function, plus a Manual Set-Mode for simpler jobs such as gouging and off-table bevelling.
- Automated gouging produces cleaner, weld-ready profiles than carbon-arc gouging and reduces grinding.
- Extended Pilot Arc removes manual edge-finding and shortens setup.
- Hypertherm reports 64% less consumable copper per foot of cut and a 99.5% recyclable system.
Industrial Applications
The Hypertherm XPR300 is aimed at operations where plasma cutting is a production process rather than a repair tool. In Oman that includes steel service centres that cut plate to order, fabricators producing structural members for petrochemical and power projects in Sohar and Duqm, pressure vessel and tank manufacturers that need bevelled edges for weld preparation, and contractors cutting stainless and aluminium parts for desalination and marine work. With a bevel head the system can prepare weld bevels directly, reducing secondary machining.
Parts cut on the table then move to welding stations, and Seven Star LLC supplies that equipment too, for example the Lincoln Electric Power Wave S500 for robotic and semi-automatic MIG, the ESAB Rebel EMP 285ic for site work, and LongTeng EL8 submerged arc wire for heavy longitudinal seams. Customers who do not need a mechanized system can review the handheld Powermax units in our plasma cutting systems category alongside the Hypertherm XPR300.
Technical Specifications
The Hypertherm XPR300 values below are taken from the manufacturer product page. Process capability depends on the gas console selected.
| Parameter | Specification |
|---|---|
| Model | Hypertherm XPR300 |
| Maximum output current | 300 A |
| Maximum output power | 66.5 kW |
| Output voltage | 50–210 VDC (100% duty arc voltage 210 V) |
| Maximum open-circuit voltage | 360 VDC |
| Duty cycle | 100% at 66.5 kW, 40 °C |
| Power factor | 0.98 at 66.5 kW |
| Ambient operating range | -10 °C to 40 °C |
| Cooling / insulation | Forced air (Class F) / Class H |
| Pierce capacity | Mild steel 50 mm (argon assist), 45 mm (standard O2); stainless 38 mm; aluminium 38 mm |
| Severance capacity | Mild steel 80 mm; stainless 75 mm; aluminium 50 mm |
| Gas consoles | Core, CorePlus, Vented Water Injection (VWI), OptiMix |
| Connectivity | CNC control, Wi-Fi and Ethernet web interface, MTConnect |
| Top lift eye rating | 680 kg |
Documentation
No single-model manufacturer datasheet for the Hypertherm XPR300 was available to attach here, so the specifications come from the manufacturer product page. Detailed cut charts, console part numbers and torch lead options are confirmed during the engineering review that precedes each quotation.
Call To Action
To request a quotation for the Hypertherm XPR300, send Seven Star LLC the materials and thickness range you cut, your table or robot details, the required console and lead lengths, and your local supply voltage. Our team in Muscat will help define a complete configuration and a consumables plan for production in Oman and the GCC.
Reviews
There are no reviews yet.