- Automation & ControlView all 2,897 products
- Automation Accessories
- AC Drives
- PLC & I/O Cards
- Industrial Communications
- Vibration Monitoring
- Controllers & Data Acquisition
- Isolator & Barrier
- Safety Switches & Guard Locking
- Motor Soft Starters
- CCTV & Security
- Encoders
- Pneumatic Cylinders
- HMI Displays
- Servo Drives
- Industrial Computers
- Machine Vision
- Automation Software
- Robotics
Brand: Miller
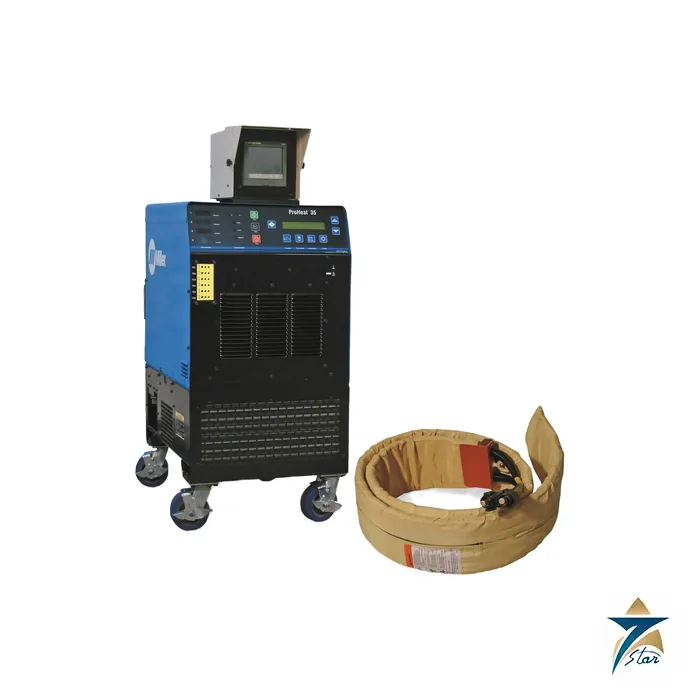
Miller ProHeat 35 Induction Heating System
Description
Overview
The Miller ProHeat 35 is an air-cooled induction heating system designed specifically for weld preheating up to 400 °F (204 °C). Its 35 kW power source runs at 100 percent duty cycle and drives flexible induction blankets or air-cooled heating cables that wrap around pipe and plate. Miller lists process piping, refinery, petrochemical, cross-country pipeline, power piping, pressure vessels, structural work and shipbuilding as core applications. The Miller ProHeat 35 replaces open-flame and resistance heating with a cleaner, faster and more uniform method of bringing joints to temperature before welding.
Seven Star LLC supplies the Miller ProHeat 35 and its blankets and accessories to pipeline contractors, refinery maintenance teams and power-plant fabricators across Oman and the GCC. Preheat is a mandatory step in many welding procedures for thick carbon steel and chrome-moly piping, and our Muscat team helps customers specify a complete induction package for projects from Fahud and Qarn Alam to Sohar and Duqm.
Operating Principle
As general background, induction heating passes an alternating current through a coil placed close to a conductive workpiece. The changing magnetic field induces eddy currents inside the metal itself, and the resistance of the metal to those currents generates heat within the part rather than on its surface. Because heat is created in the material and not conducted inward from a hot element, the temperature rises quickly and evenly through the thickness of the heat zone.
Miller describes the practical results for the Miller ProHeat 35: uniform heating is maintained along and through the heat zone, the surface is not marred by localised conducted heat above the specified temperature, and time-to-temperature is faster than with conventional processes, which reduces cycle time. The working environment also improves, because welders are not exposed to open flame, explosive gases or the hot elements associated with fuel-gas and resistance heating. At more than 90 percent efficiency, the power source transfers more energy into the part and reduces operating costs compared with other heating methods.
Engineering Design of the Miller ProHeat 35
The Miller ProHeat 35 power source has a built-in temperature controller for manual or temperature-based programming using up to four control thermocouples. It has two outputs and can run one blanket, two blankets in parallel, or four blankets in a series/parallel arrangement using series cable adapters and output extension cables. Each power source connection identifies the type of heating device to the controller, and this cable identification system prevents over-duty-cycling of the heating tool. The unit measures about 699 mm high, 552 mm wide and 933 mm deep and weighs 103 kg; optional running gear adds four 5-inch swivel casters with brakes.
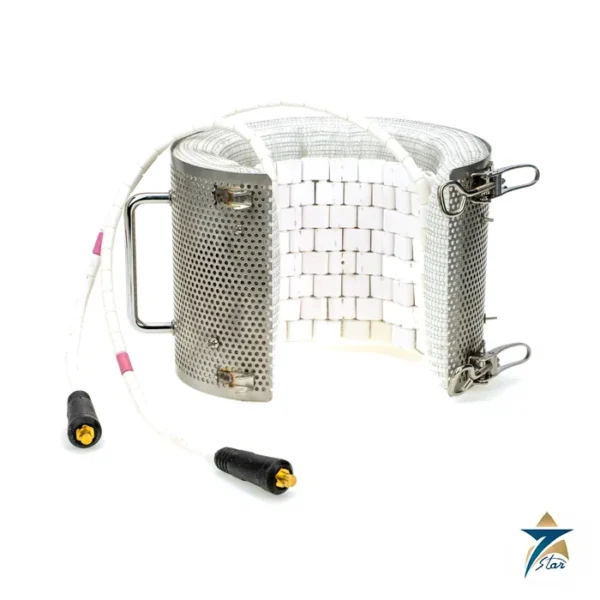
Flexible induction blankets are made from durable high-temperature materials, conform to circular and flat parts, and install in a matter of seconds. Each blanket is supplied with a replaceable Kevlar sleeve that protects against abrasion, cuts and tears. Air-cooled cables in 30, 50 and 80 ft lengths offer the same flexibility as liquid-cooled cables for preheat, and can be wrapped into coils of different shapes without a cooler or coolant. Preheat insulation, 1/2 inch thick, holds coils at the correct coupling distance and can be cut to length.
Temperature feedback on the Miller ProHeat 35 comes from a contact thermocouple sensor placed between the blanket and the part, rated for preheat use up to 500 °F (260 °C). An armoured 25 ft thermocouple extension connects the sensor to the power source, and a thermocouple extension cable with a terminal connection allows six thermocouples to be used, avoiding a clutter of individual wires across the work area. Preheat cable covers protect heating cables from slag and molten metal during welding.
Key Features
The main features of the Miller ProHeat 35 air-cooled system are:
- The power source delivers 35 kW at 100 percent duty cycle for continuous preheat on long welding shifts.
- A built-in temperature controller supports manual or programmed heating with up to four control thermocouples.
- Efficiency above 90 percent transfers more energy into the part than other heating methods.
- Two outputs can drive one, two or four blankets or air-cooled cables at a time.
- Air-cooled blankets fit pipe from 8 to 60 inches and plate lengths from 1 to 5 m.
- Air-cooled cables in 30, 50 and 80 ft lengths heat irregular shapes without coolant.
- Cable identification prevents over-duty-cycling of the connected heating device.
- Remote contactor and RHC-14 hand controls allow heat to be started, stopped or adjusted remotely.
Industrial Applications
In Oman and the wider GCC, the Miller ProHeat 35 is suited to preheating girth welds on cross-country oil, gas and water pipelines, tie-ins at gathering stations, and thick-wall process piping in refineries and petrochemical plants. Power and desalination plants use induction preheat on steam, feedwater and header piping where chrome-moly and thick carbon steels require controlled minimum preheat and interpass temperatures. Because the heat is generated inside the pipe, the blanket can stay in place while the welder works, maintaining temperature throughout the pass sequence.
Fabrication yards using the Miller ProHeat 35 on pressure vessels, structural nodes and ship sections can apply air-cooled cables and preheat insulation on plate and non-standard shapes. Seven Star LLC supplies the ProHeat 35 together with the welding equipment and consumables used on the same joints, such as the LongTeng EL8 submerged arc welding wire and the Lincoln Electric Power Wave S500 MIG system. You can see related equipment in our induction heating and preheating category.
Technical Specifications
The Miller ProHeat 35 specifications below are taken from Miller spec sheet IN/14.0 for the air-cooled system (subject to change without notice).
| Parameter | Specification |
|---|---|
| Model | Miller ProHeat 35 power source (907689 CSA; 907690 CE) |
| Input power | 460–575 V, 3-phase, 60 Hz (CSA); 400–460 V, 3-phase, 50/60 Hz (CE) |
| Rated output | 35 kW at 100% duty cycle |
| Input amps at rated output | 60 A at 400 V; 50 A at 460 V; 40 A at 575 V |
| KVA / KW at rated output | 39 / 37 |
| Max. preheat temperature (air-cooled) | 204 °C (400 °F); air-cooled cables 200 °C (392 °F) |
| Temperature control | Built-in controller, up to 4 control thermocouples |
| Outputs | 2 (one, two parallel or four series/parallel blankets) |
| Blanket sizes | Pipe 8–60 in. (20–152 cm); plate 1–5 m |
| Air-cooled cable lengths | 9.1 m, 15.2 m, 24.4 m (30, 50, 80 ft) |
| Ambient temperature, operating | -15 to 55 °C |
| Dimensions (H × W × D) | 699 × 552 × 933 mm |
| Weight | Net 103 kg; ship 120 kg |
| Standards | CSA certified; manufactured and certified in accordance with IEC 60974-1 and -10 |
How to Order
Send Seven Star LLC an RFQ for the Miller ProHeat 35 listing your site voltage, pipe diameters, wall thickness and required preheat temperature, and we will propose the power source, blankets or cables, extension leads and thermocouple accessories. Download the Miller ProHeat 35 spec sheet from this page and contact our team in Muscat for current availability and engineering support in Oman and the GCC.
Ordering Notes for the Miller ProHeat 35
Pricing for the ProHeat 35 depends on the exact order code, quantity and delivery point in Oman or the GCC, so it is given in a written quotation rather than as a list price.
Datasheets & Documents
- Datasheet Miller ProHeat 35 Air-Cooled Induction System Spec Sheet (IN/14.0) Download
Reviews (0)
How would you rate this product? Cancel reply
About brand
Miller Electric is the American maker of arc welding and cutting equipment: TIG, stick and multiprocess power sources, engine-driven welders, plasma cutters, induction heating systems, guns and welding helmets. Niels Miller built his first arc welder in his home in Appleton, Wisconsin, in 1929. The company, still headquartered in Appleton, has been part of Illinois Tool Works (ITW) since 1993 and sits in ITW's welding segment.
Seven Star LLC sources and supplies Miller welding power sources, engine-driven welders, induction heating systems, MIG guns and auto-darkening helmets for fabricators and contractors in Oman, and checks each model and its input power configuration against the manufacturer's documentation before quoting.
Miller company profile
| Founded | 1929, Appleton, Wisconsin, USA, by Niels Miller |
|---|---|
| Incorporated | 1935, as Miller Electric Mfg. Co. |
| Ownership | Illinois Tool Works (NYSE: ITW) since 1993; part of ITW's welding segment |
| Headquarters | Appleton, Wisconsin, USA |
| Product families | Dynasty and Maxstar TIG inverters, XMT and PipeWorx multiprocess systems, Millermatic MIG welders, Trailblazer and Big Blue engine drives, Spectrum plasma cutters, ProHeat induction heating, MIG guns and Digital Infinity helmets |
Milestones
- 1929: Niels Miller starts building arc welders at his home in Appleton.
- 1935: The business is incorporated as Miller Electric Mfg. Co.
- 1971: The Millermatic combines power source and wire feeder in one unit, bringing MIG welding to a wider market.
- 1993: Illinois Tool Works acquires Miller Electric.
Miller product families listed here
Miller welding machines on this page cover most processes used in plant construction and maintenance:
- TIG and stick: Dynasty 400 AC/DC and Maxstar 210 STR
- Multiprocess: XMT 400 ArcReach, XMT 650 and the PipeWorx 400 pipe welding system
- Engine-driven welders: Trailblazer 330 and Big Blue 800 Duo Pro
- Induction heating: ProHeat 35
- Guns and helmets: XR-Aluma-Pro push-pull gun; T94, Classic, Digital Performance, Digital Elite and Digital Infinity helmets
Where Miller equipment is used
An XMT or PipeWorx set suits pipe spools and structural work where one power source must run stick, TIG, MIG and flux-cored procedures. Dynasty machines handle aluminum and stainless TIG. Trailblazer and Big Blue engine drives go where no mains supply exists, such as pipelines, tank erection and remote maintenance in the GCC. The ProHeat 35 is used for preheat and post-weld heat treatment of pipe joints.
Miller products we list
Ordering Miller machines and parts: what we need
State the model and the Miller part number of the exact package, because the same machine is sold in several configurations. Give the supply at your site (voltage, phase and 50 Hz), the process and maximum current, and the accessories needed: wire feeder, remote control, cable length, torch or gun, cooler, running gear. For spare parts, the serial number from the rating label is essential, since Miller parts lists are issued by serial number range. For helmets, name the series and lens type.
Facts checked against published histories of Miller Electric and ITW, October 2026.
FAQ
Questions about the Miller ProHeat 35 Induction Heating System
Answers from our engineering team on installation, compatibility and integration.
01What temperatures can the Miller ProHeat 35 air-cooled system reach?
The air-cooled Miller ProHeat 35 system described in the spec sheet is designed for preheating applications up to 400 °F (204 °C). Induction blankets are rated for preheat up to 400 °F, and air-cooled cables are listed for temperatures up to 392 °F (200 °C). It is therefore intended for weld preheat and interpass control rather than high-temperature post-weld heat treatment.
02What pipe sizes do ProHeat 35 induction blankets fit?
Air-cooled induction blankets are available for pipe diameters from 8 to 60 inches (20–152 cm), and for plate in lengths from 40 to 197 inches (1–5 m). Blankets are made to order for each pipe diameter and come with a replaceable Kevlar sleeve. For irregular shapes, air-cooled cables of 30, 50 or 80 ft can be wrapped into coils.
03How is temperature controlled on the ProHeat 35?
The power source has a built-in temperature controller that allows manual operation or temperature-based programming using up to four control thermocouples. A contact thermocouple sensor placed between the blanket and the part provides feedback, and a thermocouple extension cable allows up to six thermocouples to be connected.
04What input power does the ProHeat 35 need?
Two versions are listed: stock 907689 for 460–575 V, three-phase, 60 Hz (CSA) and stock 907690 for 400–460 V, three-phase, 50/60 Hz (CE). At rated output the input current is 60 A at 400 V, 50 A at 460 V and 40 A at 575 V. For Oman and the GCC the 400–460 V CE version is normally specified. The primary input cable is not included.
05Does Seven Star LLC supply the ProHeat 35 and induction blankets in Oman?
Seven Star LLC supplies the Miller ProHeat 35 power source, induction blankets, air-cooled cables, thermocouple accessories and running gear to pipeline, power and refinery contractors in Oman and the GCC. Our Muscat team provides quotations, package selection and regional engineering support.


Reviews
There are no reviews yet.