
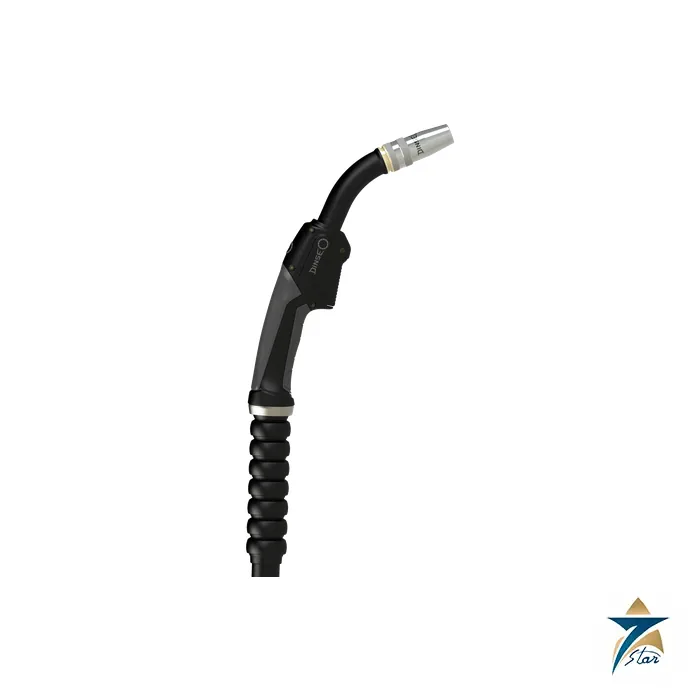
The DINSE MZ 304.PLUS is a manual MIG/MAG welding torch for heavy-duty work. It is a liquid-cooled member of the DINSE PlusLine, which combines the torch technology of the DINSE 304 series with a newly designed handle and ball joint. DINSE rates it at 500 A with CO2 and 450 A with mixed gas at 60% duty cycle according to DIN EN 60974-7, for wire diameters from 0.8 mm to 1.6 mm.
Because the inner workings come from the 304 series, the PlusLine torch takes the same wear parts and the same expansion and conversion options as the established 304 torches. A workshop already using DINSE 304 consumables can keep its stock of contact tips, gas nozzles and diffusers.
| Parameter | Specification |
|---|---|
| Manufacturer / model | DINSE / DIX MZ 304.PLUS |
| Process | Manual MIG/MAG welding |
| Cooling | Liquid-cooled |
| Rating, CO2 | 500 A at 60% duty cycle |
| Rating, mixed gas | 450 A at 60% duty cycle |
| Wire diameter | 0.8–1.6 mm |
| Standard | DIN EN 60974-7 |
| Machine connection | DINSE connector or Euro connector |
| Wear parts | Compatible with the DINSE 304 series |
| Handle options | Standard, 2 buttons, 4 buttons or main key on top; optional integrated LED light |
DINSE developed the PlusLine handle together with ergonomics specialists and welders from the field. The aim was to reduce strain on the forearm, hand and fingers. The grip is rubberized, the button has extra ripples for grip, and the torch is balanced so that it does not tip forward. The slim handle area can be guided precisely even with thick leather gloves.
The ball joint moves in all directions and has integrated kink protection. A limit on its range of motion protects the kink protector from overbending. If the ball chain wears, it can be reordered as a spare part. The torch has a separate shielding gas guide, and the gas nozzles use a trapezoid thread for heat transfer. DINSE states that the gas diffuser geometry gives a laminar gas flow.
Push-button variants can be retrofitted. With the multi-button handles the welder can start the process from the upper button, adjust the welding current at the torch or switch between welding programs during work. On request, the cap and the metal ring of the handle can be marked, for example to identify sets within a team.
The torch must run with a cooling unit that supplies coolant flow and return, either built into the power source or added as a separate unit. Do not weld with a liquid-cooled torch without coolant flow. Check that the cooling unit and the wire feeder suit a 500 A class torch.
Choose the connector to match the socket on the wire feeder. Then select the liner, contact tip and gas nozzle for the wire diameter, the wire material and the gas. According to the DINSE catalogue, the 304 series is used on unalloyed, low-alloy and high-alloy steels, copper alloys for MIG brazing, and aluminium, magnesium and nickel alloys. The cable assembly length and the article number for each version are listed in the DINSE product catalogue MANUAL.
The DINSE PlusLine flyer with the technical data is available under Datasheets & Documents. Browse our TIG Torches & MIG Guns for related welding torches.
For a quotation, send the torch designation, cable length, connector type, button variant, wire diameter and material, and quantity. If you are replacing a torch, a photo of the connector and the old handle helps us check the version.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.



Reviews
There are no reviews yet.