Highly basic flux for P91 and P92 creep-resistant 9Cr steels
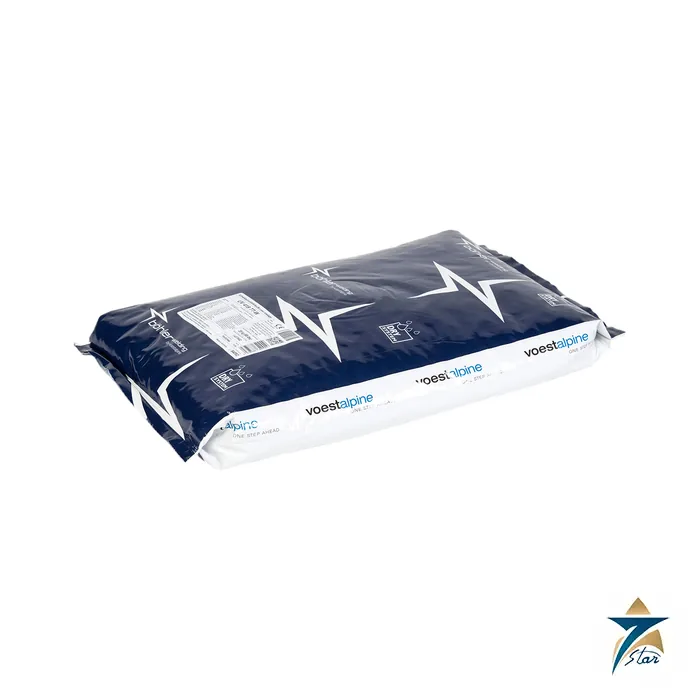
Böhler Marathon 543 is a special agglomerated fluoride-basic welding flux of high basicity for multi-run welding of high creep-resistant 9 % Cr steels. The data sheet names grade P91/T91 (1.4903, X10CrMoVNb9-1), grade P92/T92, NF616 and 1.4905 (X11CrMoWVNb9-1-1). Its metallurgical behaviour regarding silicon and manganese is neutral. The flux produces well-contoured, smooth beads with good slag release, together with appropriate weld metal ductility and impact behaviour after tempering. It is hydrogen-controlled, with low diffusible hydrogen.
Technical specifications
| Parameter |
Specification |
| Flux type |
Agglomerated, fluoride-basic, high basicity |
| Classification EN ISO 14174 |
S A FB 1 55 DC H5 |
| Polarity |
DC+ |
| Basicity index (Boniszewski) |
3.0 (wt %); 4.5 (mol) |
| Grain size (EN ISO 14174) |
3 to 20 (0.3 to 2.0 mm) |
| Apparent density |
1.0 kg/dm³ |
| Redrying |
570 to 750 °F (about 300 to 400 °C) for at least 2 hours |
| Diffusible hydrogen (ISO 3690) |
Max 5 ml per 100 g to EN ISO 14174; max 4 ml per 100 g to AWS A5.23 |
| Composition, wt % |
CaF2 21; SiO2 8; CaF2 + CaO + MgO 62 |
Wire combination for P91
Böhler’s global wire data sheet for Thermanit MTS 3 (EB91, S S CrMo91) names Marathon 543 as the recommended SAW flux, and the Böhler combination list pairs it with the Thermanit MTS family for P91/P92 work. The Böhler wire
Thermanit MTS 3 LNi.
is the low-Mn+Ni version of the P91 SAW wire. P91 and P92 are used in main steam and hot reheat piping and headers in power plants, where welds must keep creep strength for decades, so flux choice, preheat, interpass temperature and post-weld tempering must follow the qualified procedure and the applicable code.
| Related Böhler flux |
EN ISO 14174 class |
Intended for |
| UV 420 TTR-W |
S A FB 1 65 AC H5 |
1.25Cr and 2.25Cr wires on AC |
| UV 418 TT |
S A FB 1 55 AC H5 |
Structural fine-grained steels |
| Marathon 104 |
S A FB 2 AC |
Stainless and Ni-base alloys |
Procedure and handling notes
Welding of P91 and P92 is a controlled process: preheat and interpass temperatures, heat input, the time at temperature between passes, and the tempering heat treatment all influence creep strength and toughness. These parameters come from the qualified WPS and the governing code, not from the flux data sheet. Keep the flux dry, redry it at the stated temperature, and control recycled flux carefully, since contamination can raise hydrogen or alter the weld metal chemistry in a steel as sensitive as 9 % Cr.
Documents and quotation
The Böhler Welding product data sheet for Marathon 543 (US edition, 03/2021) is attached. Confirm wire, supply of certificates (including chemistry and hydrogen test) and packaging before ordering. See more in Submerged Arc Fluxes. For a quotation, send quantity and certificate requirements.

Reviews
There are no reviews yet.