Copper-coated C-Mn TIG rod for root passes and thin steel
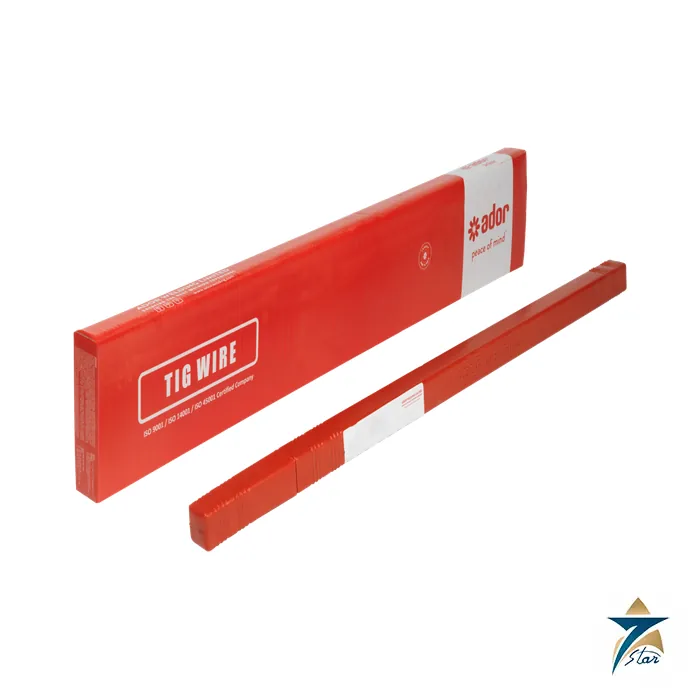
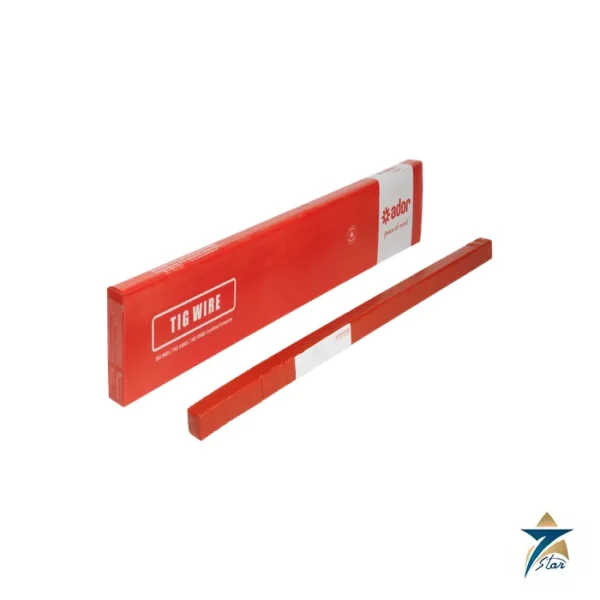
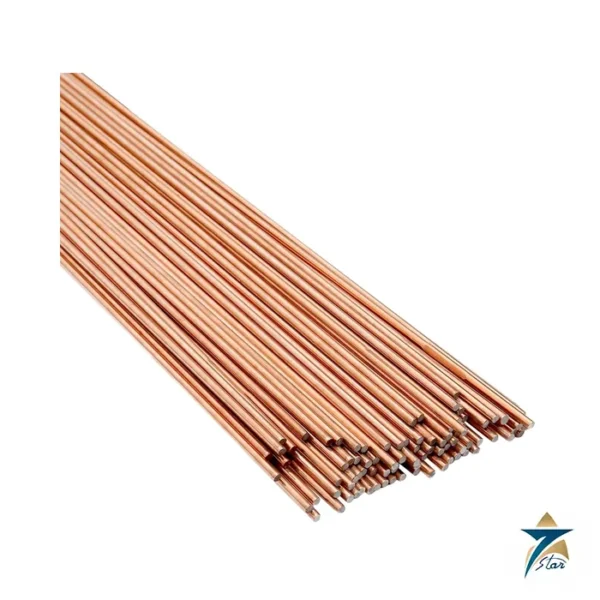
The Ador Tigfil 70S-6 is a C-Mn steel TIG filler rod classified AWS A5.18 ER70S-6 and EN ISO 636-A W 46 5 3Si1. Ador describes a uniform copper coating, a controllable weld pool and radiographic-quality welds. The rod is used with argon shielding on DCEN in all positions.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Ador Welding / Tigfil 70S-6 |
| Process |
GTAW (TIG) C-Mn steel filler rod |
| AWS classification |
A5.18 ER70S-6 |
| EN ISO classification |
636-A W 46 5 3Si1 |
| Approvals listed |
CE |
| Bare wire, typical % |
C 0.075, Mn 1.45 (silicon value not legible in the source sheet) |
| Tensile strength, as welded (typical) |
560 MPa |
| Yield strength at 0.2% offset |
485 MPa |
| Elongation |
27% |
| Charpy V impact at -50 °C |
50 J |
| Diameters |
1.6, 2.0 and 2.4 mm, 1000 mm length |
| Net weight |
20 kg per box |
| Polarity / positions |
DCEN; all positions |
| Shielding gas |
Argon at 10-15 l/min |
Typical applications
The data sheet lists root-pass pipe welding, thin sheet metal and auto body work, farm implements, steel casings, collision repair, pressure vessels, and high-pressure piping for shipbuilding, petrochemical and nuclear power plant service.
Why ER70S-6 is a favoured TIG filler
The S-6 composition carries extra manganese and silicon, which act as deoxidisers. That makes the wire tolerant of light mill scale and surface contamination on carbon steel, and it wets well at the toe of the weld. Under pure argon the pool is fluid and quiet, which is why it is widely chosen for a pipe root before filling with another process. The stated -50 °C impact value of 50 J is a typical figure and shows good low-temperature behaviour for a carbon steel filler.
Keep the rod ends clean and the copper coating intact; wipe off dust and grease before use, because contamination carries into the pool. Store the box dry. Torch angle and arc length should be steady, and the rod fed into the leading edge of the pool without pulling it out of the argon cover.
A solid MIG wire in the same carbon-steel class is available as KISWEL KC-28 ER70S-6, which suits semi-automatic work. Choose the TIG rod where heat control and a slag-free root matter more than speed.
Selecting Tigfil 70S-6 for a job
Before choosing this rod, check the welding procedure specification or the fabrication code that governs the work. ER70S-6 is a carbon-manganese filler, so it is matched to plain carbon and carbon-manganese steels rather than to stainless, low-alloy creep-resisting or high-strength steels. Compare the typical mechanical properties in the table with the minimum values required by the design, and confirm whether the job calls for the AWS or the EN ISO classification on the certificate, or both.
Diameter selection follows the material thickness, joint type and welding current. As a general guide, smaller diameters are easier to control on thin sheet and in tight root gaps, while larger diameters deposit metal faster on thicker sections and fill passes. Where an approved procedure already exists, the diameter it names should be used.
Matching gas and equipment
The data sheet calls for argon shielding and DCEN polarity. Check that the TIG power source, torch and gas regulator are in good order, that the gas hose has no leaks, and that the flow is set within the range given in the table. Draughts from fans, open doors or wind can disturb the gas shield and cause porosity even when the flow is correct, so screen the work area where necessary.
Joint preparation and welding practice
Although the S-6 composition tolerates light mill scale, good preparation still pays off. Clean the joint faces and the area on each side down to bright metal, remove oil, paint and moisture, and check fit-up and root gap against the procedure. For pipe roots, consistent bevel angles and land thickness make the root pass far easier to control.
Tack the joint securely, then weld with a steady travel speed and consistent rod feed. Allow the hot rod end to remain under the gas cover between dips. Between passes, clean the weld surface and inspect it for defects before continuing. Any preheat or interpass temperature limits should come from the welding procedure and the base material, not from general experience.
Storage and handling in Oman and GCC conditions
Fabrication yards and site workshops in Oman often combine high temperatures, fine dust and, near the coast, humid salty air. Copper-coated rods that are left in open boxes in these conditions can pick up dust and surface contamination, which then carries into the weld. Keep the boxes closed and stored indoors off the floor, take out only the rods needed for the shift, and return unused rods to a clean, dry container at the end of the day.
Do not leave rods in hot vehicles or in direct sun on site, and avoid handling them with greasy gloves. Rods that show rust, heavy discolouration or damaged coating should be set aside rather than used on critical joints.
Quality checks and documentation
For pressure vessels, piping and other coded work, record the rod classification, diameter and batch or heat information against each weld or weld map, as the quality plan requires. Visual inspection of every pass, followed by any radiographic or other testing specified for the job, confirms that the filler and technique are delivering the expected result. Keep a copy of the data sheet and any certificates supplied with the order in the welding records.
When a welder or procedure changes, a short trial joint with Tigfil 70S-6 on offcuts of the same base material helps confirm current settings, gas coverage and rod handling before work starts on production joints, and it gives the inspector a reference for the expected bead appearance.
Documents and quotation
The Ador Tigfil 70S-6 data sheet is attached to this page for download. Related consumables are listed in our TIG Welding Wire category.
For a quotation, send the diameter or size, pack type, quantity and any certificate or approval requirement.


















Reviews
There are no reviews yet.