LongTeng ER70S-6 TIG Welding Rod for Pipe Root Passes and Carbon Steel
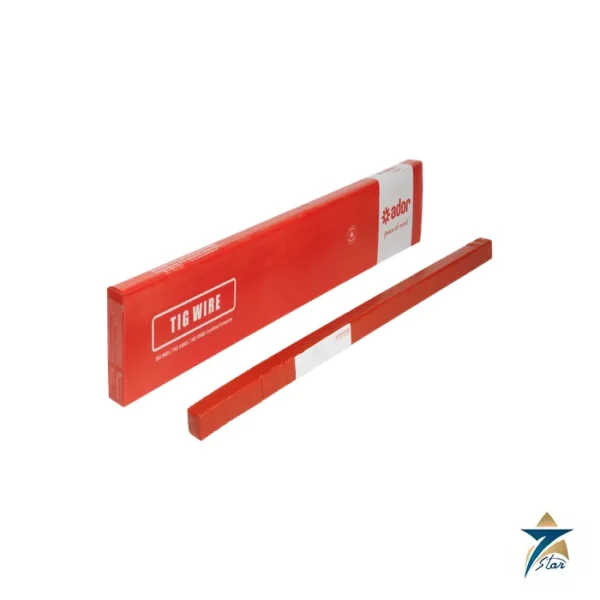
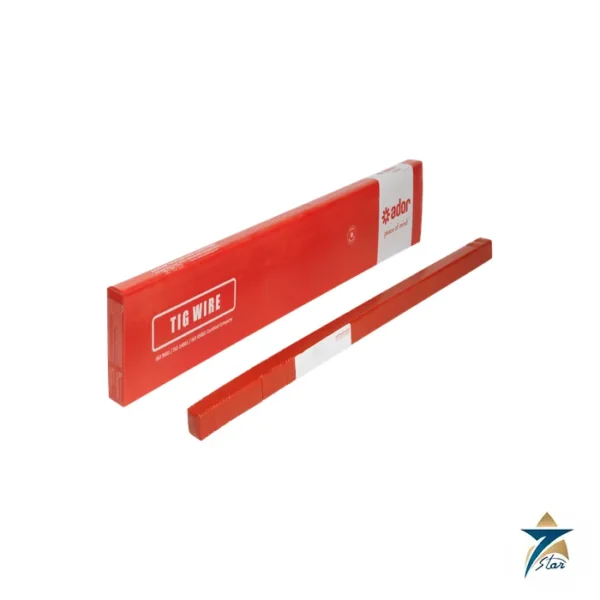
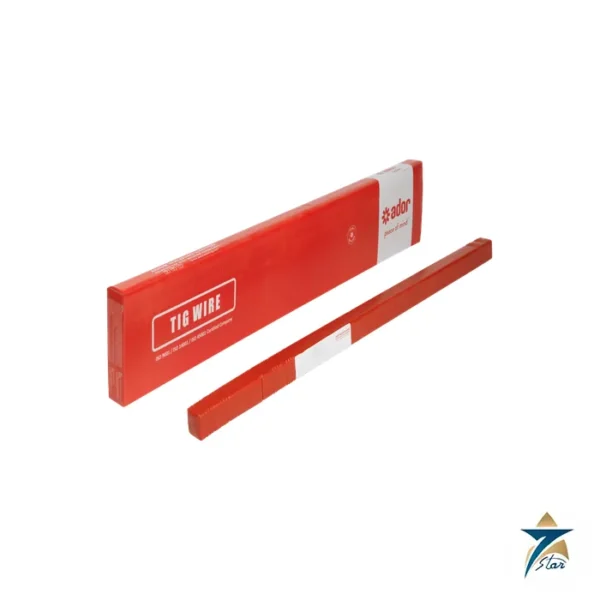
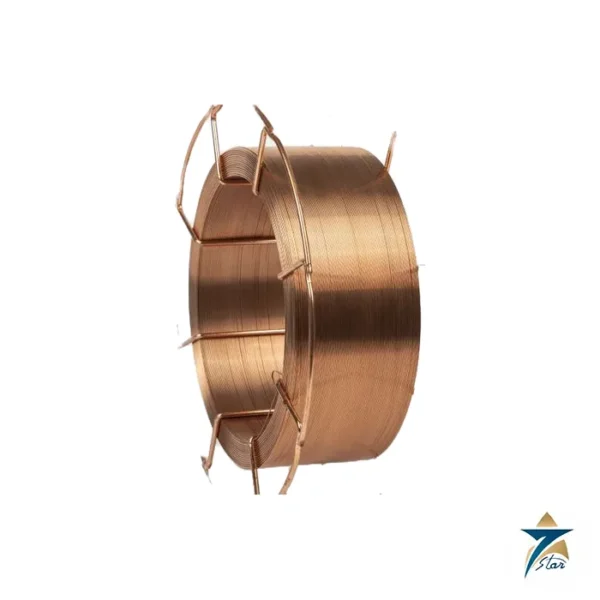
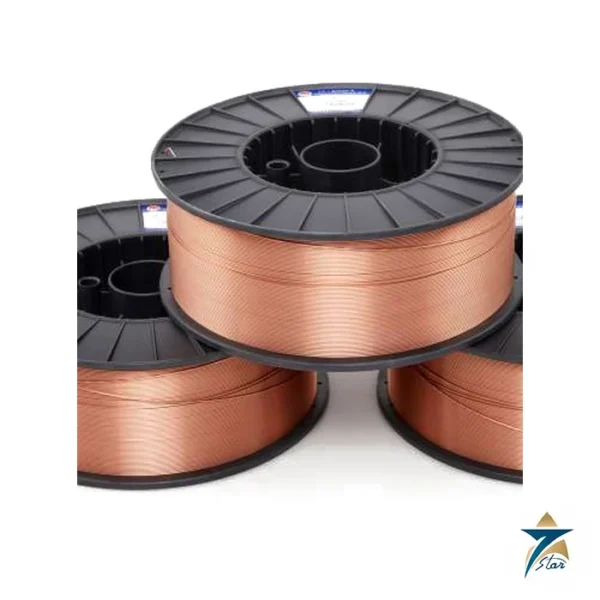
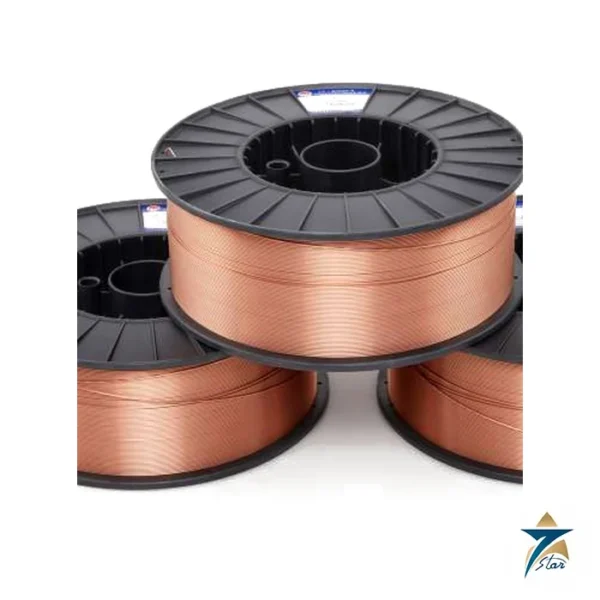
LongTeng ER70S-6 TIG is a high-deoxidiser carbon steel TIG filler wire, listed in the Longteng catalogue to AWS A5.18 ER70S-6. The manufacturer describes it for all-position manual tungsten argon arc welding, both as a backing or root weld and as an arc weld on pipelines, and states that it can weld carbon steel and some low-alloy steels. Of the two carbon steel TIG grades in the catalogue, this is the one aimed at pipe and at material that is not perfectly clean, thanks to a richer deoxidiser package.
Seven Star LLC, from its base in Muscat, supplies LongTeng welding consumables across Oman and the GCC. This LongTeng ER70S-6 TIG page is written for pipe fabricators, maintenance welders and procurement engineers who need to match filler metal to a job. It reproduces the typical values printed in the catalogue, flags the one entry we are leaving out, and explains how to read the rest. All figures are typical values listed by the manufacturer and not a guarantee from Seven Star LLC.
How the S-6 Chemistry Differs
The class name gives the clue. ER70S-6 is the version of the 70 ksi solid wire with a higher level of manganese and silicon, which helps it tolerate light mill scale, rust films and the variable surface condition found on pipe and structural plate. In the catalogue for LongTeng ER70S-6 TIG, manganese is shown at 1.49 percent and silicon at 0.84 percent, both above the values printed for the ER70S-3 TIG grade. Carbon is listed at 0.08 percent, phosphorus at 0.018 percent and copper at 0.08 percent, with nickel 0.019, chromium 0.032, molybdenum 0.004 and vanadium 0.007 percent as residuals.
The sulphur entry on the catalogue page repeats the silicon figure of 0.84 percent, which cannot be right for a filler wire, so we do not show it. The verified sulphur level for any batch is found in the test certificate. Everything else in the chemistry row appears consistent with the class.
Mechanical Values from the Catalogue
The LongTeng ER70S-6 TIG datasheet gives a typical tensile strength of 550 MPa, a yield strength of 450 MPa and elongation of 29 percent. Impact energy is listed as 160 J at minus 30 degrees Celsius. Compared with the other TIG grade in the catalogue, which is tested at minus 20 degrees Celsius, this reference shows toughness at a lower temperature, which is welcome for pipe that sees cold service or outdoor erection. For project acceptance, use the certificate delivered with the consignment of LongTeng ER70S-6 TIG rather than a typical figure.
Argon Flow and Current Guidance
Shielding gas for LongTeng ER70S-6 TIG is pure argon. The catalogue pairs a flow of 9 to 14 L/min with a current of 100 to 200 A, and a flow of 14 to 18 L/min with a current of 200 to 300 A. These flows are slightly higher than those listed for the ER70S-3 TIG grade, which is useful when welding in a pipe bore where gas coverage may be disturbed. Rod diameters are not itemised on the TIG page, so state the diameter you require when you enquire. General practice is to choose a thin rod for root passes on thin wall pipe and a thicker rod for fill and cap passes.
Strengths of LongTeng ER70S-6 TIG
The list below summarises what the catalogue supports for LongTeng ER70S-6 TIG.
- It is cited to AWS A5.18 ER70S-6, the all-round carbon steel solid wire class with enhanced deoxidisers.
- The manufacturer lists use for all-position manual TIG root welding and arc welding on pipelines.
- It is stated to be suitable for carbon steel and some low-alloy steel.
- Typical strength is listed at 550 MPa tensile and 450 MPa yield.
- Elongation is listed at 29 percent, a ductile result for a TIG deposit.
- Impact energy of 160 J at minus 30 degrees Celsius is shown.
- Manganese of 1.49 percent and silicon of 0.84 percent give strong deoxidation.
- Reference operation is in pure argon from 100 to 300 A.
Where It Is Used in Oman and the Gulf
Pipelines, process piping and skid-mounted equipment make up much of the industrial steel work in the region. A TIG root pass followed by stick or MIG fill is a common approach for carbon steel pipe in oil, gas and water services, and LongTeng ER70S-6 TIG is aimed squarely at that sequence. Fabrication yards in Sohar and Duqm, maintenance contractors serving plants around Muscat, and workshops that build pressure skids and support steel all make use of this filler class.
Good root welding with LongTeng ER70S-6 TIG depends on fit-up, argon back-purge where required, and a clean joint. For the welding machines, multi-process units like the ESAB Rebel EMP 285ic and the Lincoln Electric Power Wave S500 can run TIG. After welding, a spot check of weld and heat-affected zone hardness with an instrument such as the Phase II PHT-3500 portable hardness tester can support the quality record.
Technical Specifications
The table reproduces the values printed for LongTeng ER70S-6 TIG. Sulphur is omitted because the printed entry is inconsistent. The datasheet extract is attached to the page.
| Parameter |
Specification |
| Model |
LongTeng ER70S-6 TIG |
| Conformance |
AWS A5.18 ER70S-6 |
| Tensile strength |
550 MPa (typical) |
| Yield strength |
450 MPa (typical) |
| Elongation |
29 % |
| Impact energy |
160 J at -30 °C |
| Carbon (C) |
0.08 |
| Manganese (Mn) / Silicon (Si) |
1.49 / 0.84 |
| Phosphorus (P) |
0.018 |
| Nickel (Ni) / Chromium (Cr) |
0.019 / 0.032 |
| Molybdenum (Mo) / Copper (Cu) / Vanadium (V) |
0.004 / 0.08 / 0.007 |
| Shielding gas |
Ar (argon) |
| Gas flow and current |
9 to 14 L/min at 100 to 200 A; 14 to 18 L/min at 200 to 300 A |
Welding Practice Notes
When welding with LongTeng ER70S-6 TIG, choose the tungsten type and diameter for the current, grind it to a clean point, and keep the gas cup size in proportion to the joint. For pipe root passes, fit-up gaps should be uniform and the arc should be started without contaminating the rod end. Store filler in its sealed packing, away from moisture and oil, and handle it with clean gloves. Preheat and interpass limits come from the steel specification, and a procedure qualification on the actual pipe grade is the proper way to prove the combination.
How to Order
To request a quotation for LongTeng ER70S-6 TIG, send Seven Star LLC your rod diameter, quantity and delivery point in Oman or the GCC. Our Muscat team will confirm available packing, supply the datasheet extract and recommend that you request the batch test certificate for verified chemistry and mechanical results.


Reviews
There are no reviews yet.