
Lincoln Electric UltraCore 71A85 Gas-Shielded Flux-Cored Welding Wire
Overview
Lincoln Electric UltraCore 71A85 is a gas-shielded flux-cored arc welding wire (FCAW-G) for mild steel, classified by the manufacturer as AWS E71T-1M-H8 and E71T-9M-H8. It is designed for use with a 75 to 85 percent argon, balance CO2 shielding gas, and its fast freezing slag lets welders run vertical and overhead joints with high deposition rates. Lincoln Electric lists shipbuilding, seismic structural fabrication, general fabrication and nuclear power plant construction and maintenance among its typical applications, which places it firmly in demanding structural and marine work.
Seven Star LLC supplies Lincoln Electric UltraCore 71A85 to steel fabricators, shipyards, EPC contractors and maintenance teams in the Sultanate of Oman and the GCC. Our Muscat team can send the manufacturer datasheet, help you select spool size and diameter, and review the shielding gas and power source needed to run the wire at its published parameters.
Working Principle of a Gas-Shielded Flux-Cored Wire
A flux-cored wire is a tubular steel sheath filled with powdered flux and alloying ingredients. When the arc melts the sheath, the core produces a slag that floats over the weld pool, shapes the bead, supports the molten metal in vertical and overhead positions and refines the deposit chemistry. In a gas-shielded type such as Lincoln Electric UltraCore 71A85, an external gas supplies most of the protection against nitrogen and oxygen, while the core fine tunes arc stability and slag behaviour. The T-1 type of rutile flux used in this class is known for a smooth, spatter-light arc and a bead that wets cleanly into the toe.
The suffix M in E71T-1M means the wire was tested with a mixed argon and CO2 gas, which is exactly what the datasheet recommends for Lincoln Electric UltraCore 71A85 at a flow rate of 40 to 50 CFH. H8 indicates a diffusible hydrogen level not exceeding 8 mL per 100 g of deposited weld metal, and the typical result printed for this wire is 6 to 8 mL per 100 g. Premium arc performance and bead appearance are the headline benefits quoted by Lincoln Electric for Lincoln Electric UltraCore 71A85.
Engineering Design and Packaging
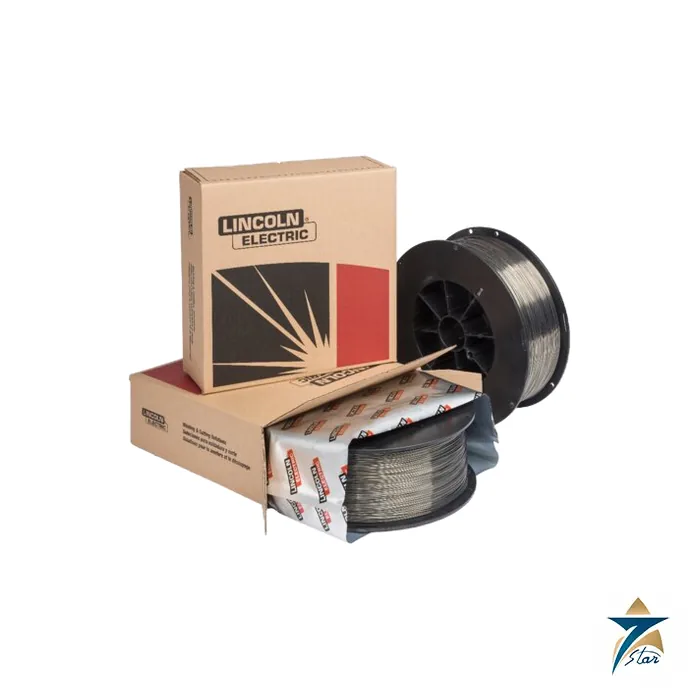
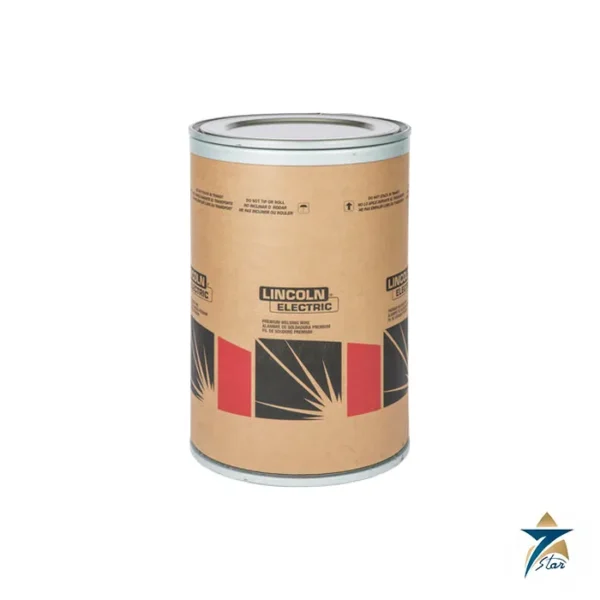
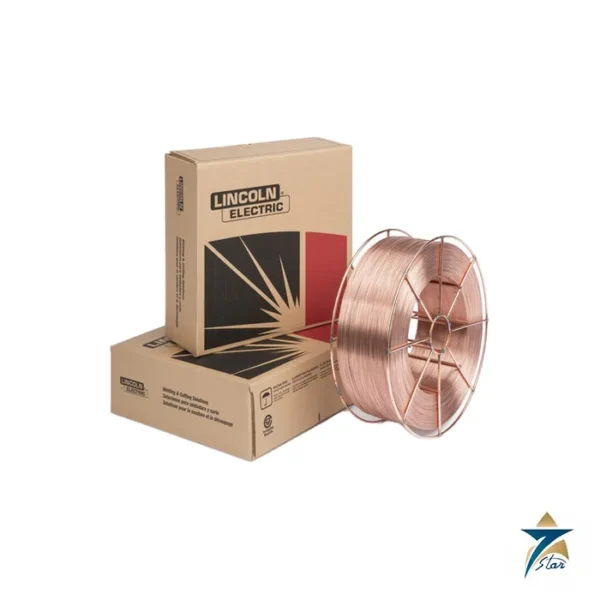
Lincoln Electric UltraCore 71A85 is supplied in diameters of 0.045 inch (1.1 mm), 0.052 inch (1.3 mm) and 1/16 inch (1.6 mm). The datasheet lists reference packages of 15 lb plastic spools in a 60 lb master carton, 33 lb spools, 50 lb fiber spools and a 500 lb Accu-Trak drum for high volume production, and notes that some part numbers are Buy America or Q2 tested products. These are the manufacturer reference packages, not a statement of Seven Star stock, so please request the current availability for the pack you need.
Lincoln Electric UltraCore 71A85 carries a set of approvals listed by the manufacturer: ABS 3YSA H10, Lloyd’s Register 3YS H10, DNV III YMS H10, CWB/CSA W48-06 E491T-9M H8, EN ISO 17632-B T493T1-1MA-H10, FEMA 353 and AWS D1.8. The datasheet also states that Lincoln Electric UltraCore 71A85 meets the AWS D1.8 seismic lot waiver requirements, which is important to structural fabricators working to seismic supplements.
Key Features of Lincoln Electric UltraCore 71A85
These features come from the manufacturer datasheet for Lincoln Electric UltraCore 71A85:
- Fast freezing slag that supports out of position welding, including vertical up and overhead joints.
- Design for 75 to 85 percent argon with balance CO2 shielding gas at 40 to 50 CFH.
- Premium arc performance and bead appearance, giving a flat, well wetted bead that needs little cleanup.
- Compliance with AWS D1.8 seismic lot waiver requirements for structural work.
- Conformance to AWS A5.20 E71T-1M-H8 and E71T-9M-H8 and to ASME SFA-A5.20.
- Marine and international approvals listed in the specification table, including ABS, Lloyd’s Register and DNV.
- Suitability for all welding positions on mild steel.
- Typical all weld metal yield strength of 550 to 600 MPa and tensile strength of 600 to 650 MPa with the recommended gas.
Industrial Applications in Oman and the GCC
Shipbuilding and ship repair are the first applications named by Lincoln Electric for Lincoln Electric UltraCore 71A85, and Oman’s yards and drydock facilities at Duqm and Sohar rely on productive flux-cored wires for hull plate, decks and internal structure. Seismic structural fabrication, general fabrication and nuclear power plant construction and maintenance are the other listed uses, and the same strengths of low hydrogen, controlled chemistry and traceable classification make the wire attractive for pressure part supports, offshore skids and heavy structural steel for industrial plants in the Gulf.
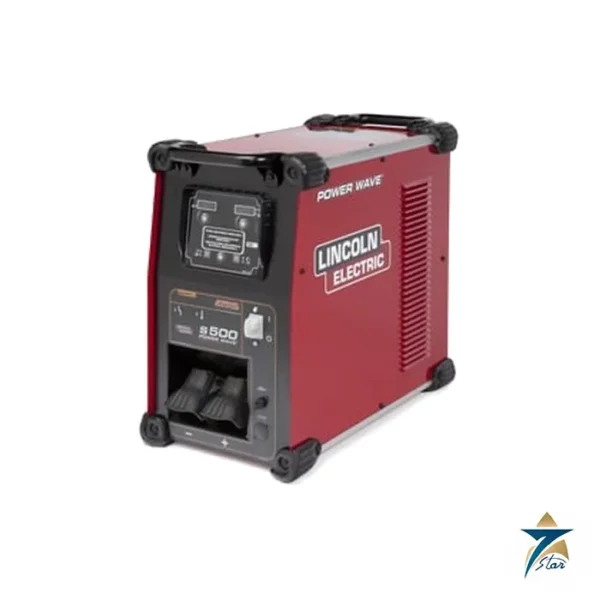
Seven Star LLC supplies Lincoln Electric UltraCore 71A85 together with welding power sources, so the consumable and the machine can be reviewed in a single order. The Lincoln Electric Power Wave S500 gives a multi-process platform for flux-cored welding, and the ESAB Rebel EMP 285ic serves lighter site work. For regional plant maintenance, our team also lists items such as the Kobelco Lubricator Assembly.
Welding Parameters Printed by the Manufacturer
The datasheet publishes procedures with direct current electrode positive polarity, a contact tip to work distance of 25 mm (1 inch) and 75 to 85 percent argon with balance CO2. For 0.045 inch wire, a wire feed speed of 4.4 m/min (175 in/min) corresponds to 21 to 26 V, about 125 A and a melt-off rate of 1.8 kg/hr, while 1/16 inch wire at 3.2 m/min (125 in/min) is listed at 20 to 25 V and about 185 A. Higher Lincoln Electric UltraCore 71A85 feed speeds raise the current, voltage window and deposition rate, and the sheet shows both all position and flat and horizontal procedures. Treat these numbers as starting points and qualify the final procedure on your own material and joint.
Technical Specifications of Lincoln Electric UltraCore 71A85
The values below come from the Lincoln Electric UltraCore 71A85 datasheet and are typical or required values published by the manufacturer, not a guarantee for a specific application.
| Parameter | Specification |
|---|---|
| Model | Lincoln Electric UltraCore 71A85 |
| Wire type | Gas-shielded flux-cored wire (FCAW-G), mild steel, all position |
| AWS classification | AWS A5.20/A5.20M E71T-1M-H8, E71T-9M-H8; ASME SFA-A5.20 same |
| Other conformances listed | ABS 3YSA H10; Lloyd’s Register 3YS H10; DNV III YMS H10; CWB/CSA W48-06 E491T-9M H8; EN ISO 17632-B T493T1-1MA-H10; FEMA 353; AWS D1.8 |
| Shielding gas | 75-85 percent Ar / balance CO2; flow 40-50 CFH |
| Diameters | 0.045, 0.052, 1/16 in (1.1, 1.3, 1.6 mm) |
| AWS requirement | Yield 400 MPa (58 ksi) min; tensile 480-655 MPa (70-95 ksi); elongation 22 percent min; 27 J (20 ft-lbf) min at -18 C (E71T-1M) or -29 C (E71T-9M) |
| Typical, 75-85 percent Ar / balance CO2 | Yield 550-600 MPa (80-88 ksi); tensile 600-650 MPa (87-94 ksi); elongation 24-26 percent; 64-115 J (47-85 ft-lbf) at -18 C |
| Deposit composition requirement | C 0.12 max; Mn 1.75 max; Si 0.90 max; S 0.03 max; P 0.03 max (percent); diffusible hydrogen 8.0 mL/100 g max |
| Typical deposit composition | C 0.03-0.04; Mn 1.43-1.56; Si 0.52-0.59; S below 0.01; P 0.01 (percent); diffusible hydrogen 6-8 mL/100 g |
| Polarity | DC electrode positive; CTWD 25 mm (1 in) |
Handling and Storage
Flux-cored wires are more sensitive to moisture than solid wires, and moisture shows up as porosity or a higher hydrogen level. As general practice, keep Lincoln Electric UltraCore 71A85 in its sealed spool packaging until it goes on the feeder, store it in a dry, temperature stable room, and return partly used spools to a bag or cover them overnight. Humid coastal conditions in Muscat and Sohar make this habit worth enforcing. This is general welding guidance, not a Lincoln Electric warranty statement.
Call To Action
To request Lincoln Electric UltraCore 71A85, send Seven Star LLC the diameter, spool or drum type, quantity and delivery location, and we will prepare a formal quotation and confirm availability across Oman and the GCC. The manufacturer datasheet is attached to this page. Seven Star LLC supplies Lincoln Electric as a trusted supplier with engineering support in Muscat, so contact our team with your enquiry and we will respond with the details your procurement and welding engineers need.
- Datasheet Lincoln Electric UltraCore 71A85 datasheet (manufacturer publication) Download
Browse Lincoln Electric products by category: Welding Equipment.


Reviews
There are no reviews yet.