
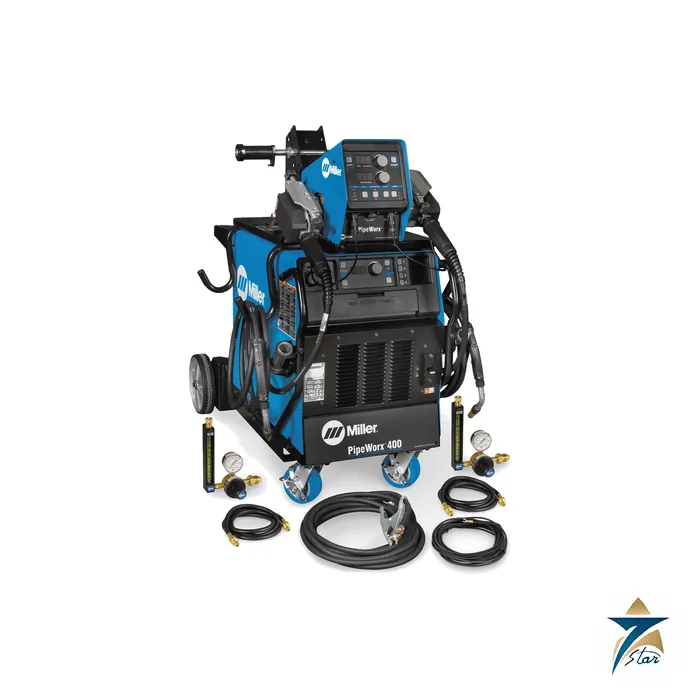
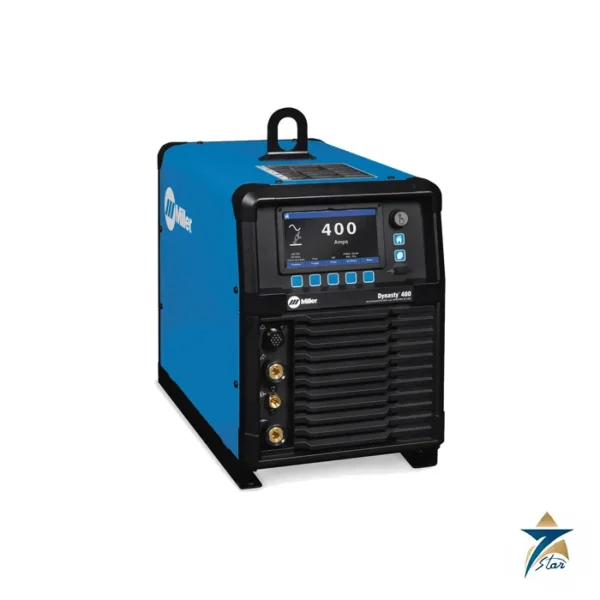
The Miller PipeWorx 400 welding system is a multiprocess package that Miller designed specifically for pipe fabrication shops. The spec sheet (index PWS/2.0, issued March 2025) describes a power source rated 400 A at 36 VDC at 100% duty cycle, a dual-wire feeder, cable and gun storage and synergic RMD and pulsed MIG programs, all tailored to process piping for refinery, petrochemical, power, HVAC and water systems. The aim is simple process setup, quick changeover between stick, TIG and wire, and an organised weld cell.
Seven Star LLC supplies the Miller PipeWorx 400 to pipe spool fabricators and EPC workshops in the Sultanate of Oman and the wider GCC. Our engineering team in Muscat helps buyers configure the power source, feeder, cooler and gun set for their procedures, and coordinates supply and technical support.
As general background, a pipe spool typically needs a sound root, a hot pass and several fill and cap passes, often with different processes. In a conventional shop that means swapping cables, gas hoses and machines. The Miller PipeWorx 400 keeps every cable connected to the power source and uses PipeWorx Quick-Select technology to choose the welding process, polarity, cable output and parameters automatically. Stick and DC TIG are selected at the press of a button, TIG starts can be high frequency or Lift-Arc, and a built-in TIG gas solenoid switches gas on and off.
The front panel was designed by welders for welders, and only the backlit controls are adjustable, which reduces confusion. Memory stores four programs for stick, TIG and each side of the MIG feeder, and a memory card slot lets each operator keep his own settings. Electrode selection automatically sets suitable conditions for common E6010 and E7018 series electrodes. Wind Tunnel Technology and Fan-On-Demand protect the Miller PipeWorx 400 in the dusty environment of a pipe shop.
RMD is a precisely controlled short-circuit transfer. According to Miller, it produces a calm, stable arc and puddle, with less chance of cold lap or lack of fusion, less spatter and a higher quality root on pipe. It is more tolerant of hi-lo fit-up and tip-to-work distance, which reduces training time, and its thicker root beads can eliminate the hot pass. In some stainless steel applications it may even be possible to omit the backing purge gas.
For fill and cap passes the Miller PipeWorx 400 uses a closed-loop pulsed MIG process with a shorter arc length, narrower arc cone and lower heat input than traditional spray pulse. Miller notes this gives easier puddle control in and out of position, better fusion at the weld toe and higher travel speed, and that combining it with RMD permits procedures that use one wire and one gas for the whole joint, eliminating process switch-over time.
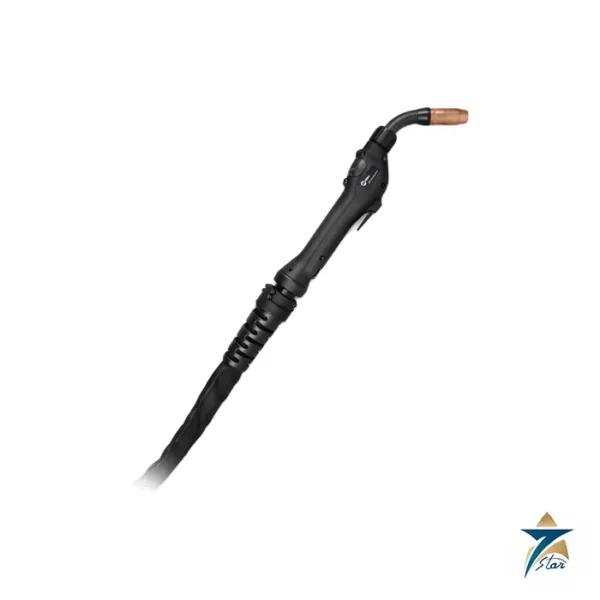
Two Bernard PipeWorx 300-15 guns are part of the standard package. Miller recommends the gun with a tapered tip and nozzle for root passes, especially in fixed-position joints where visibility is difficult, and a standard tip and nozzle for fill and cap passes. Its 60-degree neck helps the welder see the root, Centerfire drop-in tips change without tools, and the gun is rated 350 A at 100% duty cycle (NEMA) with CO2, on a 4.6 m cable weighing 4.6 kg.
The manufacturer highlights the following points for the Miller PipeWorx 400 system.
Miller lists process piping, refinery, petrochemical, power, and HVAC and water pipe as target applications for the Miller PipeWorx 400. In Oman that describes the spool shops supplying the refinery and petrochemical complexes at Sohar and Duqm, power and desalination projects along the Batinah coast, and district cooling and water networks in Muscat. Carbon steel spools benefit from RMD roots with 100% CO2 or argon/CO2 mixes, while stainless lines can use the argon/2% CO2, argon/oxygen or helium-based mixtures listed in the program tables.
Seven Star LLC supports GCC pipe shops with supply on request, help choosing feeders, guns and coolers, and engineering support from Muscat. For field work away from the shop, the Big Blue engine drives are the natural companion. Compare the Miller PipeWorx 400 with the Lincoln Electric Power Wave S500 or the compact ESAB Rebel EMP 285ic, and for heavy plate seams consider LongTeng EL8 SAW wire. All machines are listed under multi-process welding machines.
Values for the Miller PipeWorx 400 below are from the Miller PipeWorx spec sheet and are subject to change without notice.
| Parameter | Specification |
|---|---|
| Model | PipeWorx Welding System 951000094 (230/460 V, air-cooled); 951000095 (575 V); power source alone 907382 (230/460 V), 907475 (400 V), 907384 (575 V) |
| Input power | Three-phase, 50/60 Hz |
| Stick (CC) | 40–400 A; 400 A at 36 VDC, 100% duty cycle |
| DC TIG (CC) | 10–350 A; 350 A at 24 VDC, 100% duty cycle |
| MIG / flux-cored (CV) | 10–44 V; 400 A at 34 VDC, 100% duty cycle |
| Input amps, stick rating | 43.9 A at 230 V; 26.3 A at 380 V; 25.5 A at 400 V; 26.6 A at 460 V; 22.4 A at 575 V |
| Maximum open-circuit voltage | 90 V |
| Power source dimensions / weight | 724 × 495 × 806 mm; 102 kg |
| Dual feeder input | 24 VAC, 11 A; welding circuit rating 100 V, 750 A, 100% duty cycle |
| Wire feed speed | 50–780 ipm (1.3–19.8 m/min) |
| Wire diameter | 0.9–1.6 mm (.035–.062 in) |
| Maximum spool | 27 kg (60 lb) |
| Feeder dimensions / weight | 356 × 483 × 737 mm; 41 kg |
| Cooler weight | 60 kg (133 lb) |
To receive a quotation for the Miller PipeWorx 400, send Seven Star LLC the system or power source stock number, the input voltage, and the TIG torch, stick leads, remotes or cooler you need, since the standard package excludes them. The Miller spec sheet on this page lists the configurations and consumables. Our Muscat team provides quotations on request and engineering support across Oman and the GCC.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.
Reviews
There are no reviews yet.