
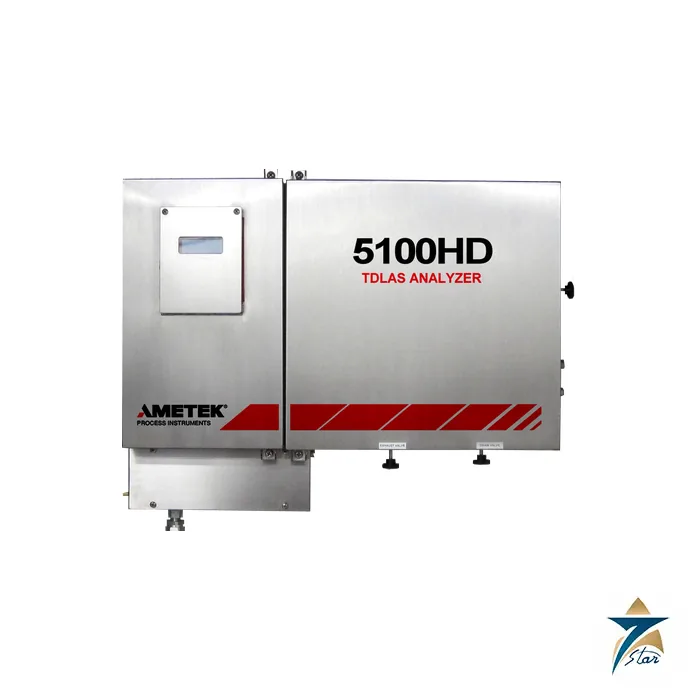
The AMETEK 5100HD is a fixed, extractive gas analyzer from AMETEK Process Instruments that uses tunable diode laser absorption spectroscopy (TDLAS) to measure water vapour in natural gas. Built for hot and wet sample analysis, it serves pipelines and transmission networks, gas processing plants, dehydration units and custody transfer points, where moisture lowers the energy value of the gas, encourages hydrate formation and drives internal corrosion of pipes and equipment. Because the measurement is optical, nothing in the gas path touches a sensing element, so the analyzer avoids the gradual contamination and slow upset response that can affect contact-type moisture sensors.
Natural gas producers, midstream operators and processing plants in Oman and the GCC must prove water content against pipeline and sales specifications every hour of the day. Seven Star LLC supplies the AMETEK 5100HD for these duties, with engineering support in Muscat for application review, sample system questions and spare parts.
In the AMETEK 5100HD, a near-infrared diode laser is tuned across a single absorption line of water. The light passes through a sample cell filled with process gas, and the amount absorbed at that wavelength is proportional to the concentration of water molecules in the beam. The analyzer uses a fully digital implementation of wavelength modulation spectroscopy (WMS), which improves sensitivity and suppresses noise compared with simple direct absorption, giving a photometric response of less than two seconds.
A key part of the design is a sealed reference cell used to line-lock the laser on the chosen absorption line. Any small shift in the observed spectrum is fed back to adjust the laser, giving a real-time confirmation that it remains locked on the correct wavelength. For natural gas service the AMETEK 5100HD needs no sample conditioning other than particulate filtering and keeping the sample above its condensation point at the integrated oven temperature of up to 150 °C.
The AMETEK 5100HD combines electronics, optics and a fully integrated, heated sample handling system in a stainless steel IP65 and Type 4X enclosure designed for outdoor installation in ambient temperatures from −20 to 50 °C. In its typical NEC/CEC Class I Division 2 or ATEX/IECEx Zone 2 configuration the cabinet measures about 880 × 674 × 302 mm and weighs around 60 kg, and versions certified to multiple ATEX, IECEx, CSA, NEC and Inmetro standards are available, including purged Zone 1 builds. It accepts 120 or 240 VAC or 24 VDC supply, drawing 25 to 45 W without heater and roughly 425 to 445 W with the oven heater active.
The AMETEK 5100HD has a local keypad and display, and communicates over Fast Ethernet with Modbus TCP/IP, an isolated RS485 port supporting Modbus RTU, up to two isolated 4–20 mA outputs and four dry relay contacts. Sample flow is 1 to 2 L/min depending on the application, at a cell pressure of 70 to 170 kPa absolute, so a simple pressure-reduced fast loop is usually sufficient.
The features below explain why gas operators choose the AMETEK 5100HD for continuous moisture measurement.
Across Oman’s gas value chain, the AMETEK 5100HD is suited to the outlet of glycol and molecular sieve dehydration units, to the inlet and outlet of gas processing trains and to custody transfer stations on the national gas network, where buyers and sellers rely on agreed water content limits. Its fast optical response lets operators spot dehydration upsets, such as glycol carry-over or saturated sieve beds, before wet gas travels downstream to compressors, meters and customers. Since the same 5100HD platform is offered for CO2, H2S, O2 and methane in other data sheets, plants can standardise spares and training across several measurement points.
In the wider GCC, gas processing complexes, LNG feed gas systems, refineries and petrochemical plants use the AMETEK 5100HD on feed stock and process streams where conventional sensors suffer from fouling. Seven Star LLC supplies the analyzer to operators and EPC contractors in Oman, the UAE, Saudi Arabia, Qatar, Kuwait and Bahrain, with engineering support in Muscat throughout the project.
The AMETEK 5100HD values below are taken from the manufacturer’s data sheet for moisture in natural gas (F-0432).
| Parameter | Specification |
|---|---|
| Model | AMETEK 5100HD (moisture in natural gas) |
| Technology | Tunable diode laser absorption spectroscopy, digital WMS, extractive |
| Measured component | H2O in natural gas |
| Minimum range | 0 to 20 ppmv (other ppm and % ranges available) |
| Accuracy | ±2% of reading or ±4 ppm, whichever is greater (typical) |
| Speed of response | < 2 s photometric; system response depends on sample flow |
| Laser verification | Sealed reference cell line-lock |
| Sample conditioning | Particulate filtering; integrated oven up to 150 °C |
| Sample flow | 1–2 L/min (2.1–4.2 SCFH), application dependent |
| Sample cell pressure | 70 to 170 kPa absolute (10 to 25 psia) |
| Ambient temperature | −20 to 50 °C; 0–90% RH non-condensing |
| Electrical | 120/240 VAC, 47–63 Hz, or 24 VDC |
| Power | 25–45 W without heater; 425–445 W with heater (typical) |
| Outputs | Keypad and display; Fast Ethernet, Modbus TCP/IP; RS485 Modbus RTU; up to 2 isolated 4–20 mA; 4 dry relays |
| Dimensions (W × H × D) | 880 × 674 × 302 mm (typical Div 2 / Zone 2) |
| Weight | Approx. 60 kg (typical Div 2 / Zone 2) |
| Enclosure | IP65 and Type 4X |
| Approvals | ATEX, IECEx, CSA, NEC and Inmetro hazardous-area standards (consult for details) |
For portable checks and sulfur plant duties, see the AMETEK 5100P transportable TDLAS analyzer, AMETEK 900 tail gas air demand analyzer and AMETEK 930 H2S in sulfur pit analyzer.
To order the AMETEK 5100HD, send Seven Star LLC a formal RFQ with your gas composition, moisture range, sample pressure and temperature, and hazardous-area classification. Our instrumentation team will confirm the right configuration, current availability and delivery to sites across Oman and the GCC. The product datasheet can be downloaded from this page, and our engineers in Muscat are ready to help with sample system layout and control system integration.
Browse AMETEK products by category: Gas Analyzer Accessories, Gas Analyzer Systems, Liquid Analytical Accessories, Level Transmitter.
Choose the option that best fits your needs to get the fastest response from our team.
Automatically fill the RFQ form with this product's details for a faster process.
Manually enter multiple part numbers, specific brands, or custom requirements.














Reviews
There are no reviews yet.