High-ferrite electrode for difficult-to-weld steels
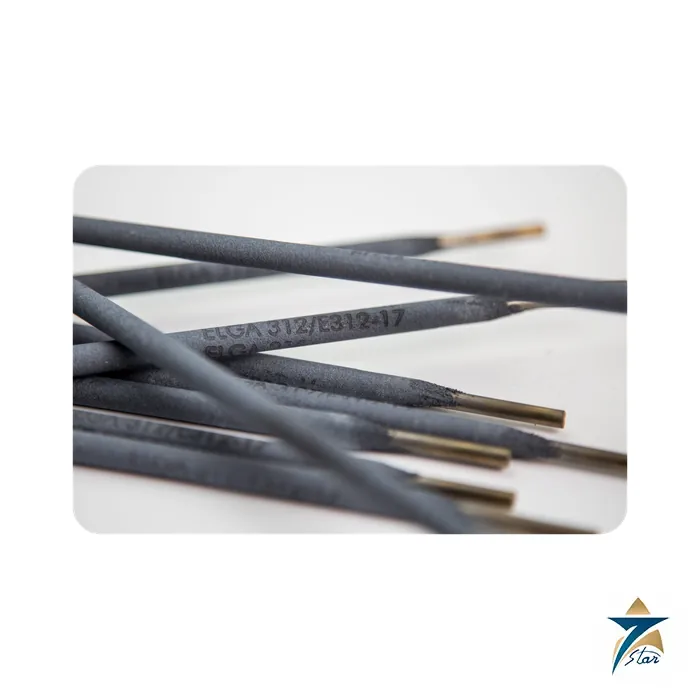
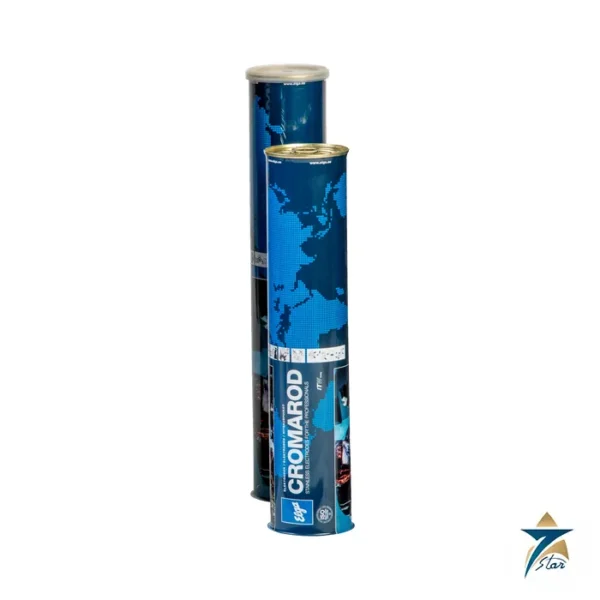
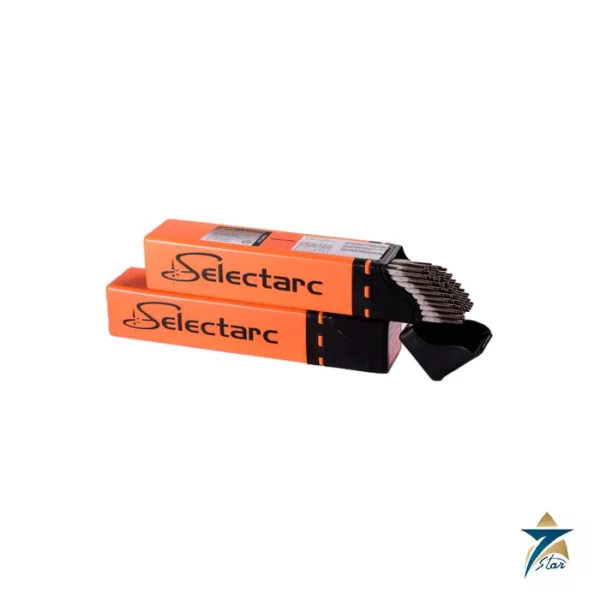
The Elga Cromarod 312 is a rutile-coated stick electrode that deposits a 29% Cr, 9% Ni austenitic-ferritic weld metal with a ferrite content of about FN 50. Elga highlights its excellent tolerance to dilution from dissimilar and difficult-to-weld materials without hot cracking.
Applications listed by Elga include high-carbon hardenable tool, die and spring steels, 13% Mn steels, free-cutting steels and non-structural high-temperature steels; dissimilar joints between stainless and high-carbon steel; and surfacing of metal-to-metal wear areas, hot-working tools and furnace components.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Elga (ITW Welding AB) / Cromarod 312 |
| Process |
SMAW (stick, MMA) |
| AWS classification |
A5.4 E312-17 (slight deviation in Si) |
| ISO 3581-A |
E 29 9 R 32 |
| Coating type |
Rutile |
| Welding current |
DC+ or AC, OCV above 39 V |
| Positions |
1, 2, 3, 4, T, 6 per data sheet |
| Ferrite content |
FN 50 (WRC-92) |
| Typical weld metal, % |
C 0.10, Si 0.9, Mn 0.8, Cr 29.0, Ni 9.0, Mo 0.2 |
| Yield strength Rp0.2 |
Specified ≥450 MPa; typical 590 MPa |
| Tensile strength Rm |
Specified ≥660 MPa; typical 760 MPa |
| Elongation A5 |
Specified ≥22%; typical 25% |
| Sizes and current |
2.5 × 300 mm, 40–80 A; 3.2 × 350 mm, 80–120 A; 4.0 × 350 mm, 100–160 A |
| Deposition |
1.1, 1.5 and 2.1 kg weld metal per arc hour for 2.5, 3.2 and 4.0 mm |
| Scaling temperature |
About 1100 °C in air |
| Redrying |
350 °C, 2 h |
| Approvals listed |
CE |
Repair welding and the limits of a 312 deposit
A 29Cr-9Ni filler is the classic “problem solver” for maintenance shops. The high ferrite content gives very good crack resistance when the weld is diluted by carbon-rich or sulphur-bearing base metals, and the high strength of the deposit suits buttering, build-up and joining of unknown steels in repair work.
The same high ferrite is also the main limitation. Above roughly 300 °C, and especially after long exposure in the 600–900 °C range, a ferrite-rich deposit can form sigma phase and lose toughness, which is why Elga restricts high-temperature use to non-structural parts. For load-bearing dissimilar joints in hot service, a nickel-base filler is usually preferred. For corrosion service, Elga gives good resistance to sulphurous gases at high temperature and to wet corrosion up to about 300 °C.
The data sheet core wire limits are P 0.030%, S 0.030% and N 0.080% max. For duplex stainless pipe rather than repair work, see the Elga Cromarod Duplex electrode.
When buttering a hardenable or high-carbon steel, preheat according to the base metal, not the filler. The 312 deposit tolerates dilution, but the heat-affected zone of a tool or spring steel can still crack if it cools too fast. Electrodes that have absorbed moisture can be redried at 350 °C for two hours. Clean the area to bright metal before welding, because oil, paint and rust on worn parts are common sources of porosity in repair welds, and peen or grind out any crater cracks before the next pass.
The typical values in the table are example results under EN ISO test conditions; the specified minimums apply for qualification.
Documents and quotation
The Elga Cromarod 312 product data sheet is attached to this page. Other stick electrodes are listed in our Welding Electrodes category.
For a quotation, give the diameter, quantity and the materials being joined or repaired.

Reviews
There are no reviews yet.