135% recovery electrode for productive fillet welding
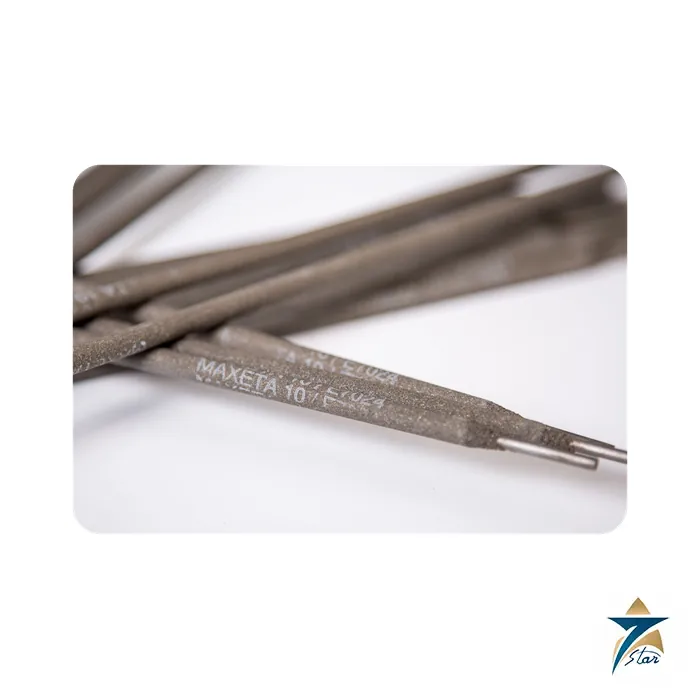
The Elga Maxeta 10 is a rutile-coated iron powder electrode with 135% metal recovery, intended for welding medium-thick sections in general construction steels. Elga optimised it to produce fillet welds with a good mitre profile and a throat thickness in the 3.5–4.0 mm range.
According to the data sheet, Maxeta 10 gives a finely rippled bead surface, minimal spatter and a self-detaching slag, so post-weld cleaning time is low. It runs on DC of either polarity or on AC.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Elga (ITW Welding AB) / Maxeta 10 |
| Process |
SMAW (stick, MMA), un-alloyed |
| AWS A5.1 |
E7024 |
| EN ISO 2560-A |
E 42 0 RR 53 |
| Coating type |
Rutile, iron powder |
| Welding current |
DC+/- or AC, OCV ≥65 V |
| Metal recovery |
135% |
| Positions |
1, 2, 3, R, T, Y per data sheet (flat and horizontal work) |
| Typical weld metal, % |
C 0.07, Si 0.7, Mn 0.6, P 0.02, S 0.01 |
| Yield strength Re |
Specified ≥420 MPa; typical 470 MPa |
| Tensile strength Rm |
Specified 500–640 MPa; typical 570 MPa |
| Elongation A5 |
Specified ≥22%; typical 24% |
| Impact energy |
Specified ≥47 J at 0 °C; typical 50 J |
| Sizes and current |
3.2 × 450 mm, 130–160 A; 4.0 × 450 mm, 140–220 A; 5.0 × 450 mm, 190–310 A |
| Deposition |
2.2, 2.6 and 3.7 kg weld metal per arc hour for 3.2, 4.0 and 5.0 mm |
| Redrying |
90 °C, 2 h |
| Approvals listed |
CE; ABS 2; BV 2Y; DNV 2Y |
Where a high-recovery rutile electrode pays off
The iron powder in the coating adds to the weld deposit, so each electrode lays down more metal than its core wire alone. That is why the deposition rate reaches 3.7 kg per arc hour in the 5.0 mm size. The 450 mm length further reduces stub losses and electrode changes on long fillet runs, for example on stiffeners, brackets and beam fabrication.
Elga lists 23 electrodes per kilogram of weld metal in 3.2 mm, 17 in 4.0 mm and 11 in 5.0 mm, with burn-off times of 61 to 78 seconds per electrode. These numbers make it simple to estimate electrode consumption and arc time for a given fillet length.
An E7024 coating is not a low-hydrogen type. Rutile electrodes only need gentle redrying (90 °C for 2 hours according to Elga), but they are not the choice for highly restrained joints or steels sensitive to hydrogen cracking, where a basic E7018-type electrode is normally specified. Impact toughness is specified at 0 °C only.
Because the rutile slag is fluid and the pool is large, Maxeta 10 is a flat and horizontal-fillet electrode; positional joints need a different consumable. Use the current window for each diameter given in the table and keep the electrode in light contact or at a very short arc for the best bead profile. Plate edges should be free of heavy mill scale, rust and primer where possible, since contamination affects slag release and bead finish more than electrode choice.
The typical values in the table are example results under EN ISO test conditions and are not guaranteed; the specified minimums apply for qualification and design.
Documents and quotation
The Elga Maxeta 10 product data sheet is attached to this page. Other stick electrodes are listed in our Welding Electrodes category.
For a quotation, give the diameter, quantity and any classification society approval required.

Reviews
There are no reviews yet.