Nickel-base electrode for Inconel 600 and dissimilar joints
The Elga Cromarod 82 is a basic-coated nickel-chromium-iron stick electrode for welding Inconel 600 and alloys of similar composition. Elga describes a deposit that tolerates high dilution and is very resistant to hot cracking, and that is not susceptible to sigma-phase embrittlement or carbon migration. That makes it suitable for service at elevated temperature.
It is also used for a wide range of dissimilar joints between nickel-base alloys, Monel, mild and low-alloy steels and austenitic stainless steels, and for cladding carbon steel with an Inconel-type surface. The weld metal keeps very good toughness down to -196 °C, so Elga lists it for 5% and 9% nickel steels in cryogenic service.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Elga / Cromarod 82 |
| Process |
SMAW (stick, MMA) |
| AWS A5.11 |
E NiCrFe-3 |
| EN ISO 14172 |
E Ni 6182 (NiCr15Fe6Mn) |
| Coating type |
Basic |
| Welding current |
DC+ |
| Positions |
1, 2, 3, 4, T, 6 per data sheet |
| Ferrite content |
FN 0 (fully austenitic) |
| Typical weld metal, % |
C 0.03, Si 0.3, Mn 7.0, Cr 16.0, Nb 2.2, Fe 5.0, Ni balance |
| Yield strength Rp0.2 |
Specified ≥360 MPa; typical 405 MPa |
| Tensile strength Rm |
Specified ≥550 MPa; typical 642 MPa |
| Elongation A5 |
Specified ≥30%; typical 44% |
| Impact energy |
Specified ≥100 J at 20 °C; typical 110 J at -20 °C and 94 J at -196 °C |
| Oxidation resistance |
In air up to 1100 °C |
| Sizes and current |
2.5 × 300 mm, 45–70 A; 3.2 × 350 mm, 70–110 A; 25–27 V |
| Redrying |
350 °C, 2 h |
| Approvals listed |
CE, TÜV |
Using a 182-type filler on mixed joints
Nickel-base fillers are chosen for carbon-steel-to-stainless and stainless-to-nickel joints because they absorb dilution from both sides without forming crack-sensitive martensite, and because their thermal expansion sits between the two base metals. In high-temperature service this reduces carbon migration from the ferritic side, which is the main reason a NiCrFe-3 electrode is preferred over a 309-type stainless filler for hot dissimilar joints.
The high manganese level of about 7% and the niobium addition in the deposit help resist hot cracking. Elga states very good resistance to general and intergranular corrosion and to stress corrosion cracking.
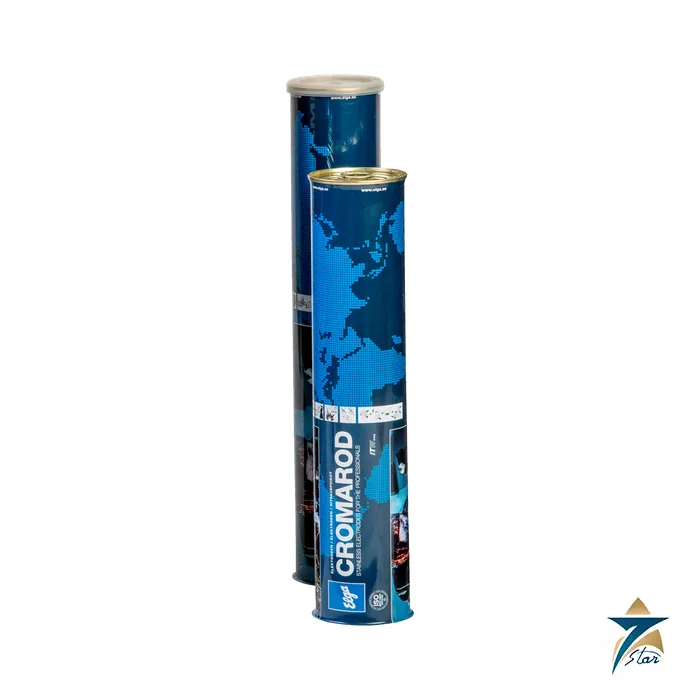
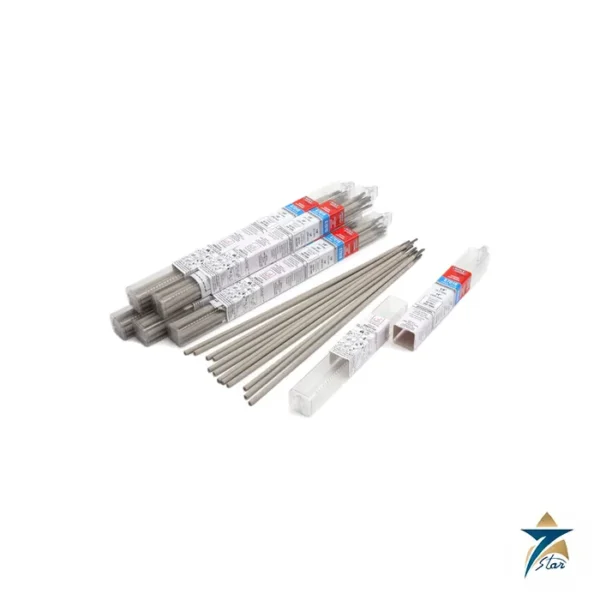
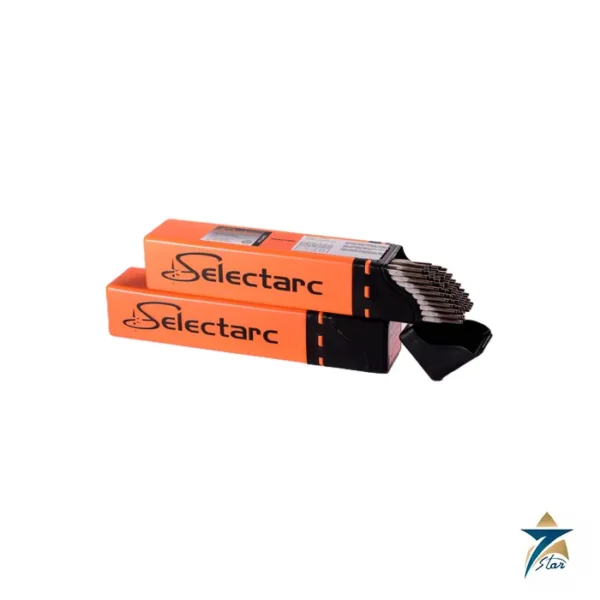
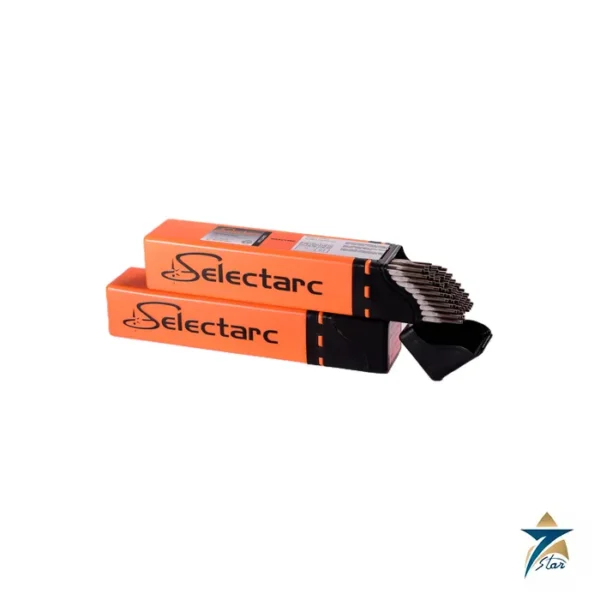
As with other nickel alloys, the weld pool is sluggish, so a slight weave and a short arc are normally used, and interpass temperature should be kept low. These are general practice notes; follow the qualified procedure for your job. The photo shows Elga Cromarod range packaging.
Joint preparation matters more with nickel alloys than with steels: a wider groove angle helps the sluggish pool wet the side walls, and the joint must be clean of sulphur, lead and paint, which can cause cracking. Electrodes that have absorbed moisture can be redried at 350 °C for two hours, according to Elga.
The typical values in the table are example results under EN ISO test conditions; the specified minimums apply for qualification and design.
Documents and quotation
The Elga Cromarod 82 product data sheet is attached to this page. Other stick electrodes are listed in our Welding Electrodes category.
For a quotation, send the diameter, quantity, both base materials of the joint and any approval or certificate required.

Reviews
There are no reviews yet.