Basic E2209-15 duplex electrode for thick sections and low-temperature service
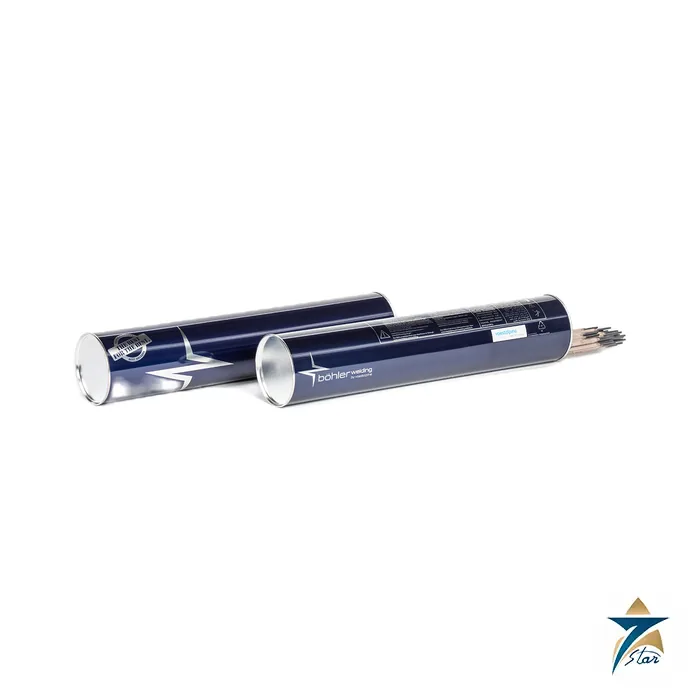
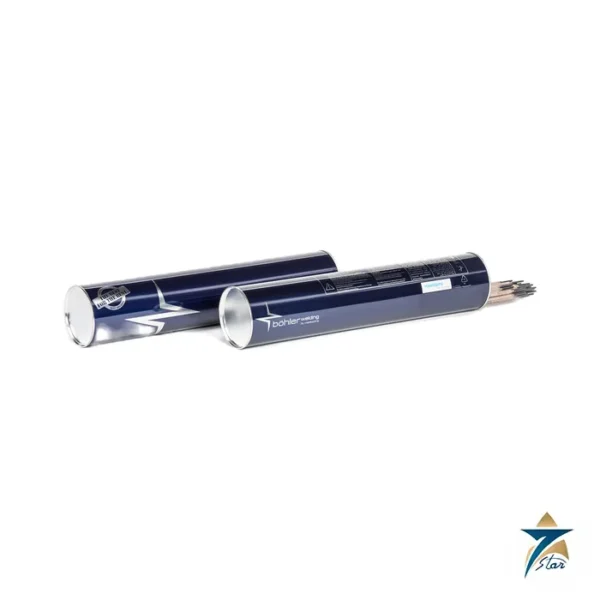
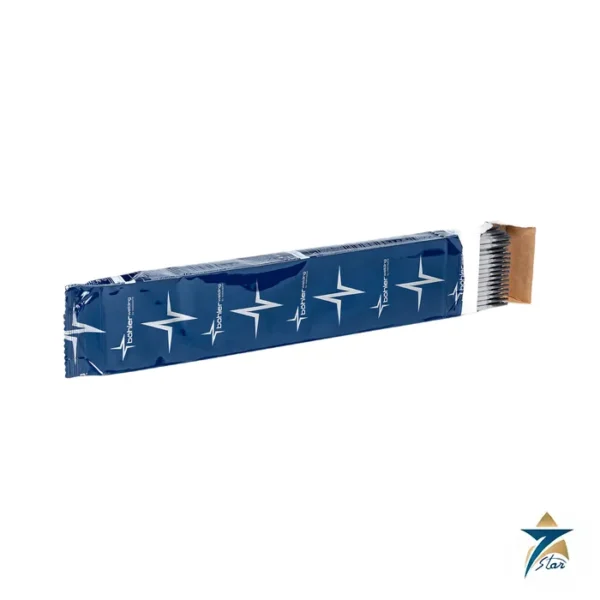
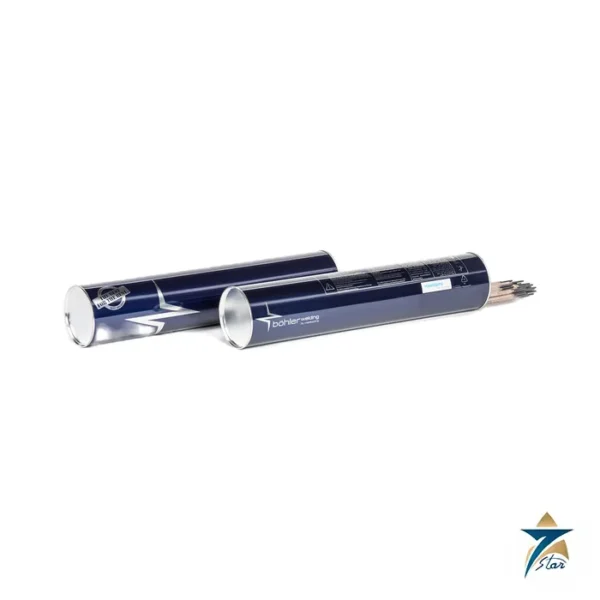
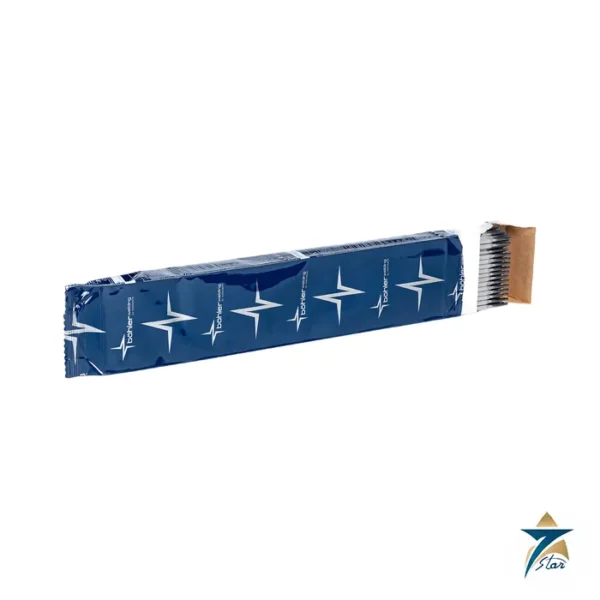
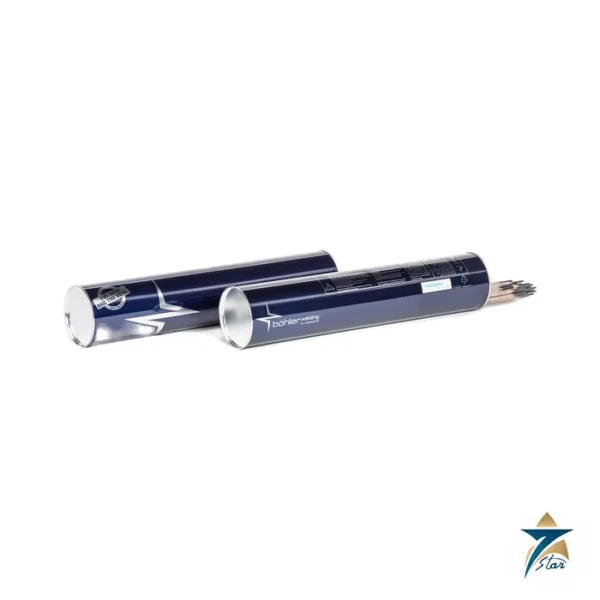
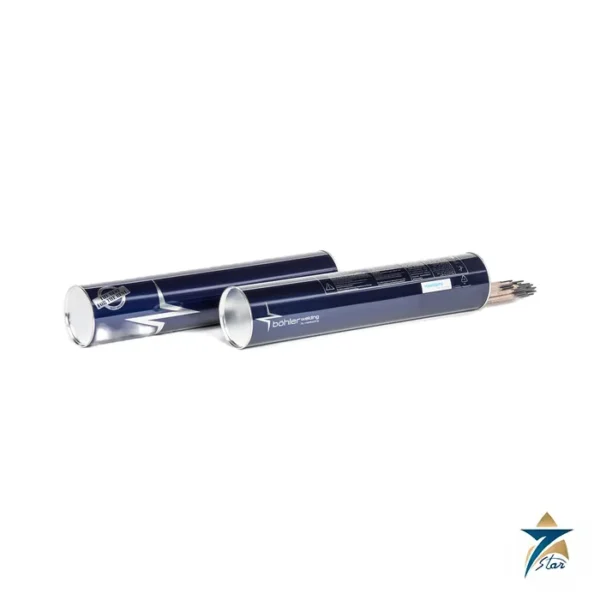
The Böhler FOX CN 22/9 N-B is a basic-coated, core-wire-alloyed electrode of E2209-15 type (EN ISO 3581-A E 22 9 3 N L B 2 2) for duplex stainless steels such as 1.4462 (UNS S31803 and S32205). Böhler Welding specifically designed it for thick-walled sections, for example above 20 mm, rigid constructions and applications with extra-low service temperatures down to -50 °C. The weld metal meets ASTM G48 Methods A, B and E corrosion test requirements at 25 °C and shows high resistance to stress corrosion cracking. Ferrite measured with a FeritScope is 34 to 36 FN, and the electrode is suited to service from -50 °C to 250 °C.
Technical specifications
| Parameter |
Specification |
| AWS classification |
A5.4 / SFA-5.4 E2209-15 |
| EN ISO classification |
3581-A E 22 9 3 N L B 2 2 |
| Typical analysis, wt % |
C 0.03; Si 0.3; Mn 1.1; Cr 22.6; Ni 8.8; Mo 3.1; N 0.16; PREN 35 or higher |
| Yield strength Rp0.2, as welded |
630 MPa typical (minimum 450) |
| Tensile strength Rm, as welded |
830 MPa typical (minimum 690) |
| Elongation A (L0=5d0) |
30 % typical (minimum 20) |
| Impact energy ISO-V |
100 J at 20 °C; 65 J at -50 °C (minimum 32) |
| Ferrite |
34 to 36 FN (FeritScope FMP30) |
| Polarity |
DC+ |
| Sizes and current |
2.5 x 350 mm: 50 to 75 A; 3.2 x 350 mm: 80 to 110 A; 4.0 x 350 mm: 100 to 145 A; 5.0 x 450 mm: 140 to 180 A |
| Heat input and interpass |
0.5 to 2.5 kJ/mm; interpass temperature maximum 150 °C |
| Heat treatment |
Generally not needed; solution annealing at 1100 to 1150 °C with water quench in special cases |
| Redrying |
250 to 300 °C, minimum 2 h, if necessary |
| Approvals |
TÜV (07084), CE |
Base materials and selection
Listed base materials are 1.4462, 1.4362 and 1.4162, UNS S32205, S31803, S32304 and S32101, and the grades 2205, 2304, LDX 2101 and SAF 2205 and 2304. Typical jobs are thick-wall process piping, pressure vessels, offshore and desalination equipment. The data sheet notes that for root runs the Böhler FOX 22/9 N electrodes or Thermanit 22/09 solid wire and rods may be preferred, which is why the TIG rod
Thermanit 22/09.
is the matching root-pass product. The duplex flux-cored option is the
FOXcore 2209-T1.
. Respect the heat-input window, since too low or too high a heat input shifts the ferrite-austenite balance.
| Related Böhler Welding electrode |
Classification (AWS A5.1 / A5.5 / A5.4) |
Typical use |
| FOX EAS 4 M-VD |
E316L-17 |
Vertical-down 316L stainless sheet and pipe |
| FOX SAS 2-A |
E347-17 |
Ti/Nb stabilised 321 and 347 stainless |
Handling and what to confirm
Keep the electrodes dry, use the redrying range only if required, and control interpass temperature at or below 150 °C. If the specification demands ASTM G48 testing, ferrite counts or impact tests at -46 °C or -50 °C, state this in the enquiry together with diameter, quantity, plate thickness and the certificate type.
The ferrite figure of 34 to 36 FN and a PREN of 35 or higher describe the phase balance and pitting resistance of the deposit. Yield strength is typically 630 MPa against a minimum of 450 MPa and tensile strength typically 830 MPa, so a strength overmatch of 2205 plate is expected; corrosion testing and ductility then become the main points to verify in the procedure qualification.
How the FOX CN 22/9 N-B electrode works
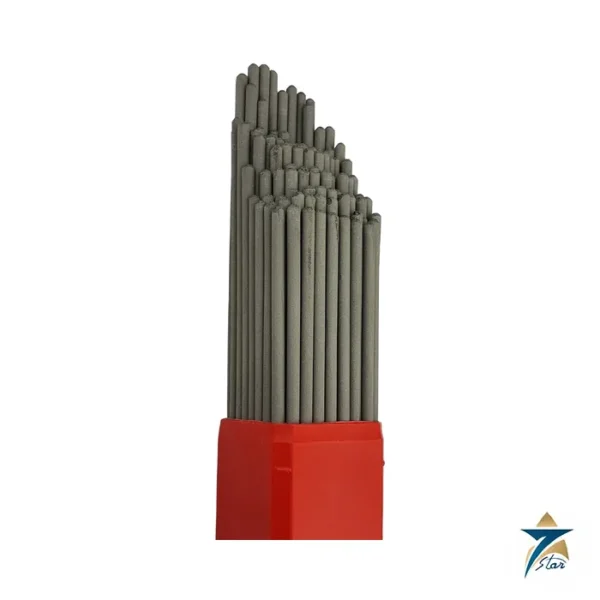
The FOX CN 22/9 N-B is a stick electrode with a basic coating. When the arc burns, the coating makes a slag and a gas shield that protect the weld pool. The core wire carries the alloy, including nitrogen, so the weld metal has a duplex structure with about 34 to 36 FN ferrite. This balance of ferrite and austenite gives high strength and a good resistance to pitting and stress corrosion cracking. The basic coating gives good toughness at low temperature.
Where the FOX CN 22/9 N-B is used
- Welding of duplex 1.4462, S31803 and S32205 steels
- Thick-wall process piping and pressure vessels
- Offshore equipment
- Desalination plant
- Rigid constructions and service down to -50 degrees C
Selection checklist for the FOX CN 22/9 N-B
- AWS A5.4 E2209-15
- EN ISO 3581-A E 22 9 3 N L B 2 2
- Electrode diameter of 2.5, 3.2, 4.0 or 5.0 mm
- DC+ polarity
- Base steel such as 1.4462, 1.4362 or 1.4162
- Wall thickness, above 20 mm
- Service temperature from -50 to 250 degrees C
- Heat input and interpass limits
Installation, commissioning and maintenance notes for FOX CN 22/9 N-B
Keep the heat input between 0.5 and 2.5 kJ/mm and the interpass temperature below 150 degrees C. Redry the electrodes at 250 to 300 degrees C for at least 2 hours if they have taken up moisture. Use DC+ and set the current to the diameter. Heat treatment is generally not needed.
Requesting a quotation for the FOX CN 22/9 N-B
Please send the electrode diameter, the pack size, the quantity and the delivery location. Seven Star LLC serves industrial customers in Oman and the GCC and replies with a quotation based on the information provided.
FOX CN 22/9 N-B weld metal analysis
The typical analysis is 0.03 percent carbon, 0.3 percent silicon, 1.1 percent manganese, 22.6 percent chromium, 8.8 percent nickel, 3.1 percent molybdenum and 0.16 percent nitrogen. The PREN is 35 or higher.
FOX CN 22/9 N-B mechanical values
As welded, the typical yield strength is 630 MPa, the tensile strength is 830 MPa and the elongation is 30 percent.
FOX CN 22/9 N-B impact energy
The typical impact energy is 100 J at 20 degrees C and 65 J at -50 degrees C.
FOX CN 22/9 N-B current settings
The ranges are 50 to 75 A for 2.5 mm, 80 to 110 A for 3.2 mm, 100 to 145 A for 4.0 mm and 140 to 180 A for 5.0 mm.
Welding records for FOX CN 22/9 N-B
Keep the batch number, the redrying log and the procedure number with the weld file.
Choosing the right FOX CN 22/9 N-B product
For root runs the data sheet suggests the FOX 22/9 N electrode or Thermanit 22/09 solid wire and rods.
Documents and quotation
This listing includes the Böhler Welding data sheet for FOX CN 22/9 N-B. See welding electrodes for related consumables. For an offer please give the dimensions, packaging, quantity, material to be welded and the inspection certificate type.

Reviews
There are no reviews yet.