Mn-Ni-Mo electrode for cast steel, valves and oil tools
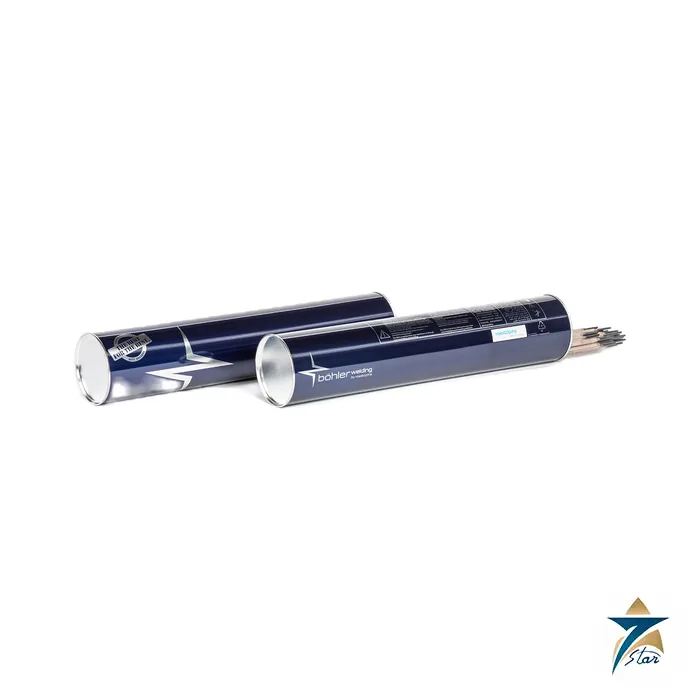
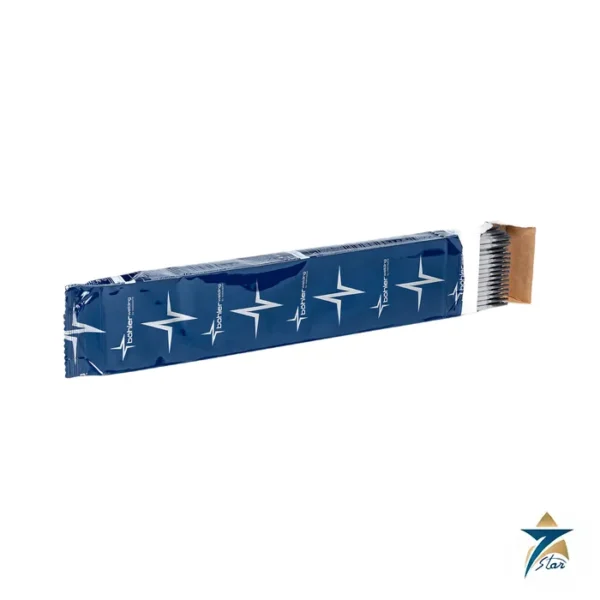
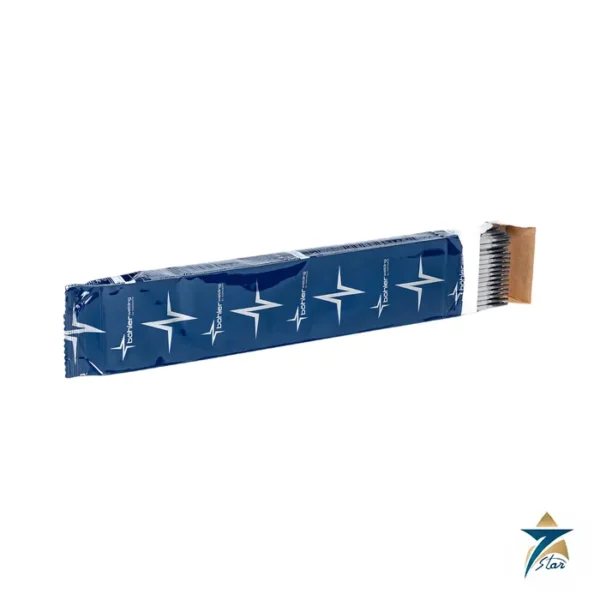
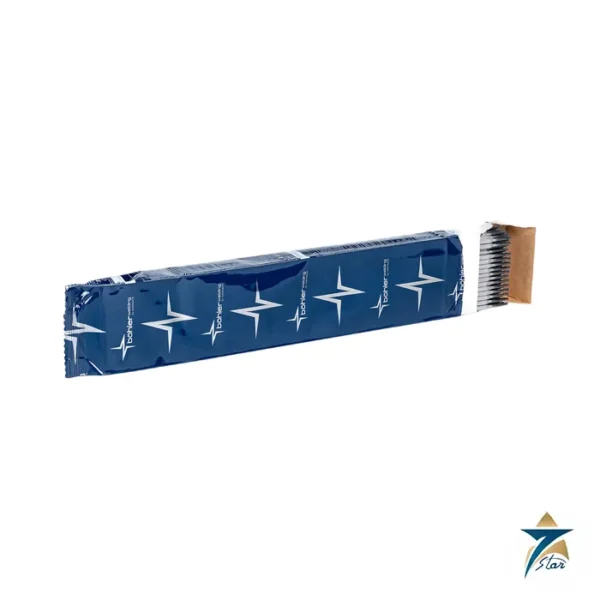
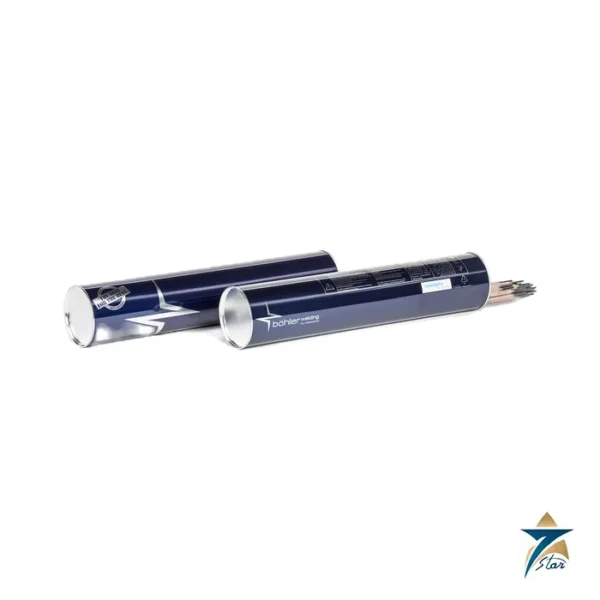
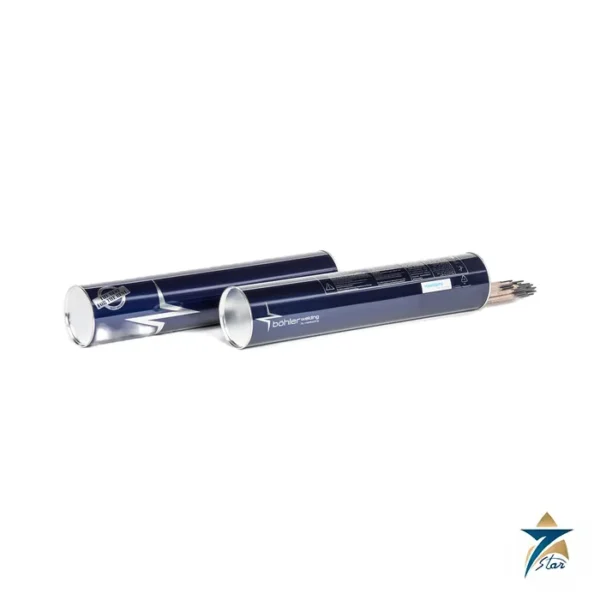
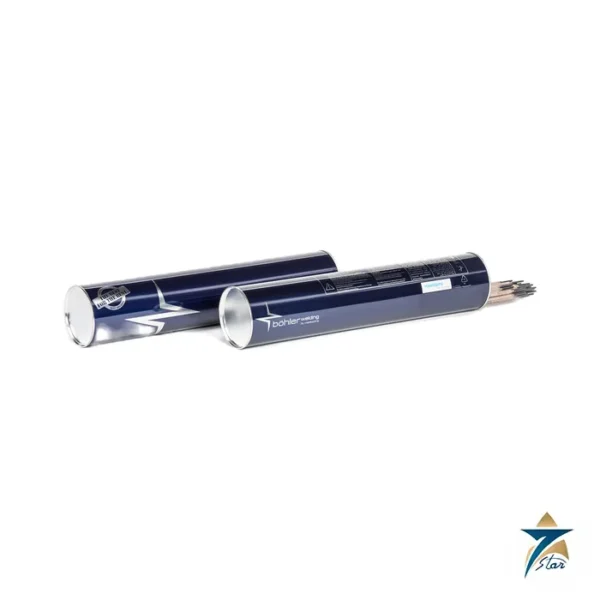
The Böhler FOX NiMo is a basic-coated, MnNiMo alloyed stick electrode, designated E10018-D2 (AWS) and E 62 4 Mn1NiMo B on the electrode identification. Böhler Welding gives it a very low hydrogen content below 5 ml per 100 g, extremely high resistance to cracking and high toughness down to -40 °F. It is intended for creep-resistant steels and cast steel grades, and for valves and oil tools made to sour gas specifications. Post-weld heat treatment is stress relieving according to the parent metal.
Technical specifications
| Parameter |
Specification |
| Electrode identification |
FOX NiMo / E 62 4 Mn1NiMo B / E10018-D2 |
| Typical analysis, wt % |
C 0.09; Si 0.3; Mn 1.9; Ni 0.9; Mo 0.4 |
| Yield strength Rp0.2, as welded |
94 ksi typical (minimum 90) |
| Tensile strength Rm, as welded |
112 ksi typical (100 to 129) |
| Elongation A (L0=5d0) |
20 % typical (minimum 18) |
| Impact energy ISO-V, as welded |
89 ft-lb at 68 °F; 52 ft-lb at -40 °F (minimum 35); 44 ft-lb at -58 °F |
| Stress relieved 1175 °F / 4 h |
Yield 91 ksi; tensile 106 ksi; elongation 21 %; 96 ft-lb at 68 °F; 52 at -40 °F; 44 at -58 °F |
| Hydrogen |
Below 5 ml per 100 g |
| Polarity |
DC+ |
| Sizes and current |
3/32 in x 14 in: 70 to 100 A; 1/8 in x 14 in: 100 to 150 A; 5/32 in x 14 and 18 in: 140 to 200 A; about 3/16 in x 18 in: 180 to 250 A |
| Approvals |
None listed on the data sheet |
Base materials and selection
The base materials named are G30CrMoV6-4 and GS-30CrMoV6-4 cast steels, ASTM A 487 Grade 4Q and AISI 4130. The class is a 100 ksi tensile electrode, so it is for matching strength on cast valve bodies and oil-tool parts rather than for ordinary structural steel. Sour-service parts are normally governed by NACE or API hardness limits that the data sheet does not cover, so check the specification and ask for test values where needed. For plate steels in the 550 MPa class see the
FOX EV 70.
, which carries TÜV approval.
| Related Böhler Welding electrode |
Classification (AWS A5.1 / A5.5 / A5.4) |
Typical use |
| FOX EV 70 |
E9018-G H4R |
High-strength fine-grained steel, 550 MPa class |
| FOX EV 85 |
E11018-G H4R |
Quenched and tempered steel up to 690 MPa yield |
| FOX CM 2 Kb |
E9018-B3 H4R |
2.25 % Cr, 1 % Mo refinery and power-plant steel |
Heat treatment and what to confirm
Choose preheat, interpass temperature and post-weld heat treatment from the base material, as the data sheet says. The data sheet prints no redrying range or approvals for this electrode, so confirm packaging, storage instructions and certificate scope with your enquiry. Give the diameter, quantity and the cast or forged grade being welded.
Reading the figures: the as-welded yield strength is typically 94 ksi against a minimum of 90 ksi, which places this electrode in the 100 ksi tensile class. After stress relieving at 1175 °F for four hours the values change only slightly, to 91 ksi yield and 106 ksi tensile, and the toughness at minus 40 °F and minus 58 °F stays at 52 and 44 ft-lb. That small shift is useful on cast parts, where the casting specification often calls for a post-weld heat treatment.
How the FOX NiMo electrode works
The FOX NiMo is a stick electrode with a basic coating. The coating forms a slag that protects the weld pool and keeps the hydrogen in the weld metal very low, below 5 ml per 100 g. Manganese, nickel and molybdenum in the weld metal raise the strength to the 100 ksi class and keep the toughness high at low temperature. The electrode runs on DC with the electrode connected to the positive pole. The joint must be clean and the electrodes dry for a sound weld.
Where the FOX NiMo is used
- Cast steel valve bodies
- Oil tools and wellhead parts
- Creep-resistant steels
- Repair of 4130 steel parts
- Welding of G30CrMoV6-4 castings
Selection checklist for the FOX NiMo
- AWS class E10018-D2
- Electrode diameter from 3/32 in to about 3/16 in
- Length of 14 in or 18 in
- DC+ power source
- Base steel and its carbon content
- Preheat and interpass temperature
- Stress relief at 1175 degrees F for 4 hours
- Impact test requirement at -40 degrees F
Installation, commissioning and maintenance notes for FOX NiMo
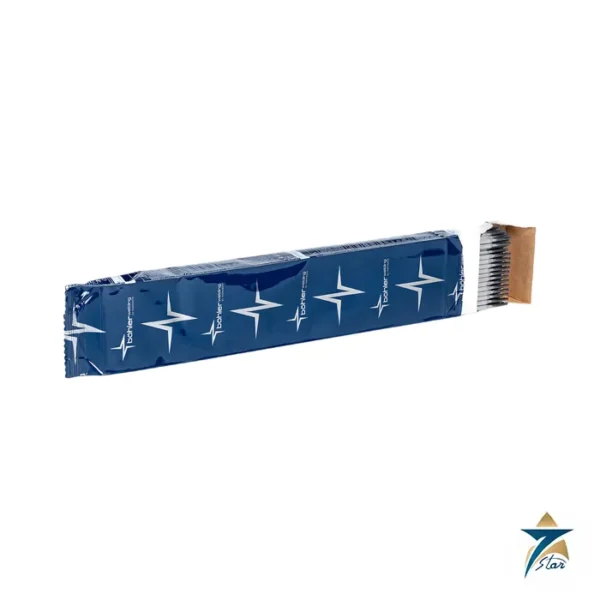
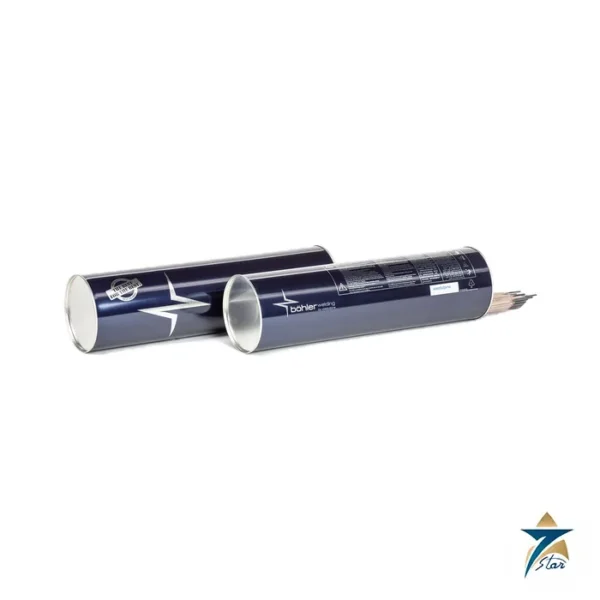
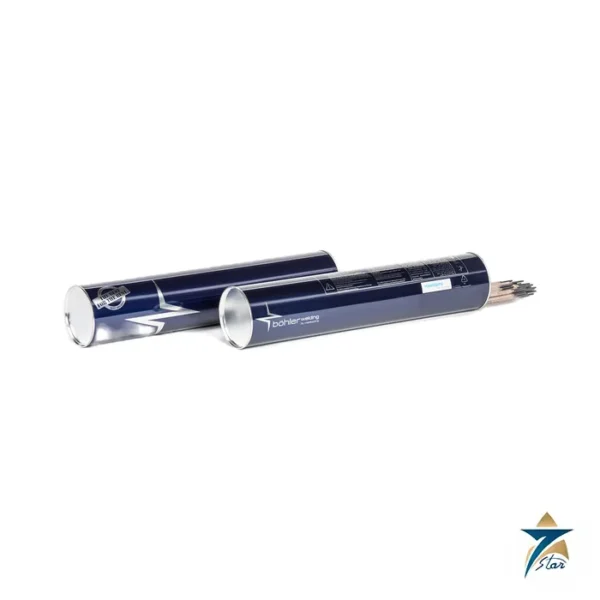
Store the electrodes dry and re-bake them if they have taken up moisture, following the pack label. Preheat thick cast parts as the base metal requires. Hold a short arc, keep the weave narrow and clean each pass before the next. Let the part cool slowly. If the part will be stress relieved, check the values after the heat treatment.
Requesting a quotation for the FOX NiMo
Please send the electrode diameter, the pack size, the quantity and the base material. Seven Star LLC serves industrial customers in Oman and the GCC and replies with a quotation based on the information provided.
FOX NiMo weld metal analysis
The typical analysis is 0.09 percent carbon, 0.3 percent silicon, 1.9 percent manganese, 0.9 percent nickel and 0.4 percent molybdenum.
FOX NiMo mechanical values
As welded, the typical yield strength is 94 ksi, the tensile strength is 112 ksi and the elongation is 20 percent. The impact energy is 89 ft-lb at 68 degrees F and 52 ft-lb at -40 degrees F.
FOX NiMo current settings
The ranges are 70 to 100 A for 3/32 in, 100 to 150 A for 1/8 in, 140 to 200 A for 5/32 in and 180 to 250 A for about 3/16 in.
FOX NiMo related electrodes
The data sheet lists the FOX EV 70, FOX EV 85 and FOX CM 2 Kb for other steel grades.
Welding records for FOX NiMo
Keep the batch number, the preheat record and the heat treatment chart with the weld file.
Choosing the right FOX NiMo size
Use the smaller diameters for root and position welds and the larger ones for fill passes on thick castings.
Documents and quotation
This listing includes the Böhler Welding data sheet for FOX NiMo. See welding electrodes for related consumables. For an offer please give the dimensions, packaging, quantity, material to be welded and the inspection certificate type.

Reviews
There are no reviews yet.